
Whole-House Custom Cabinetry Procurement FAQ: Specs, Finishes and E0/ENF Checks
Whole-House Custom Cabinetry Procurement FAQ: Specs, Finishes and E0/ENF Checks
A procurement reference for buyers specifying whole-house custom cabinetry: what panel thickness and machining tolerance are actually documented, how surface finishes are planned, what E0 and ENF checks really prove, and where custom cabinetry is a clear advantage — and where it is not.
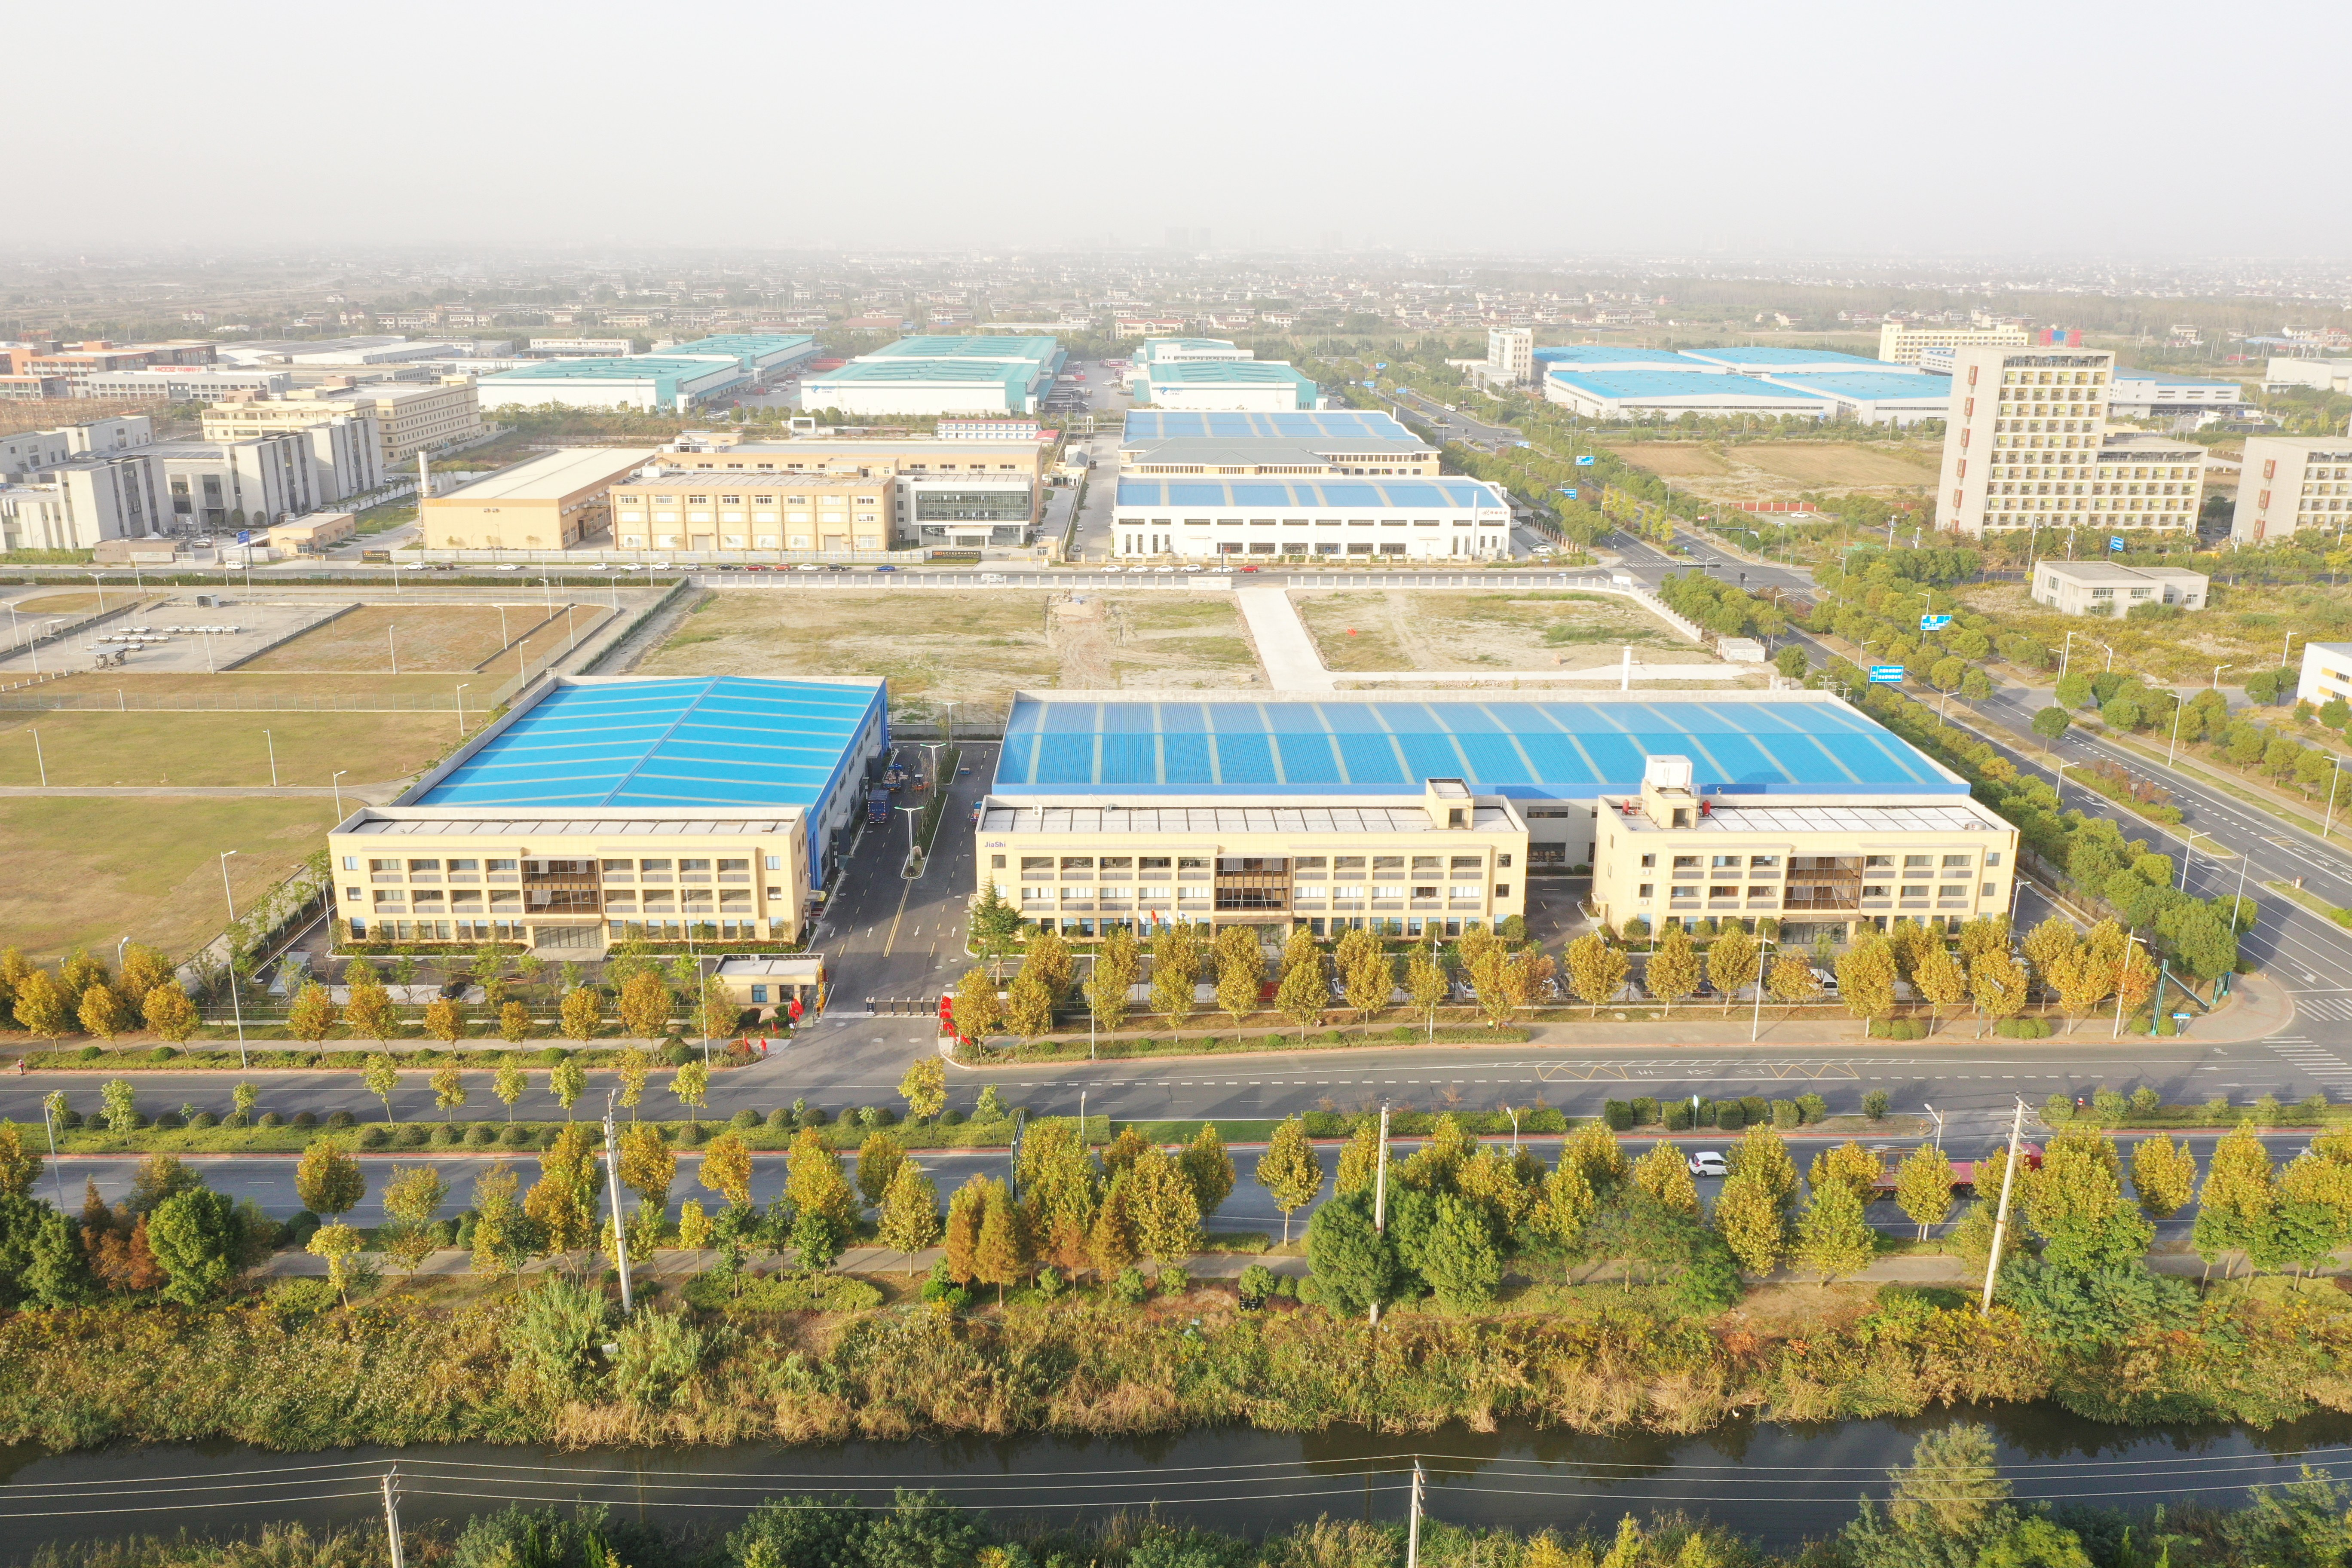
The questions that decide a whole-house custom cabinetry package rarely concern design style. Once the drawings are approved, a procurement team is left with a shorter and harder list: what panel thickness the factory holds as standard, which dimensional tolerance its production line can repeat across an order, how a surface finish stays consistent from the kitchen to the wardrobe, and which document actually proves the formaldehyde grade of the boards that ship.
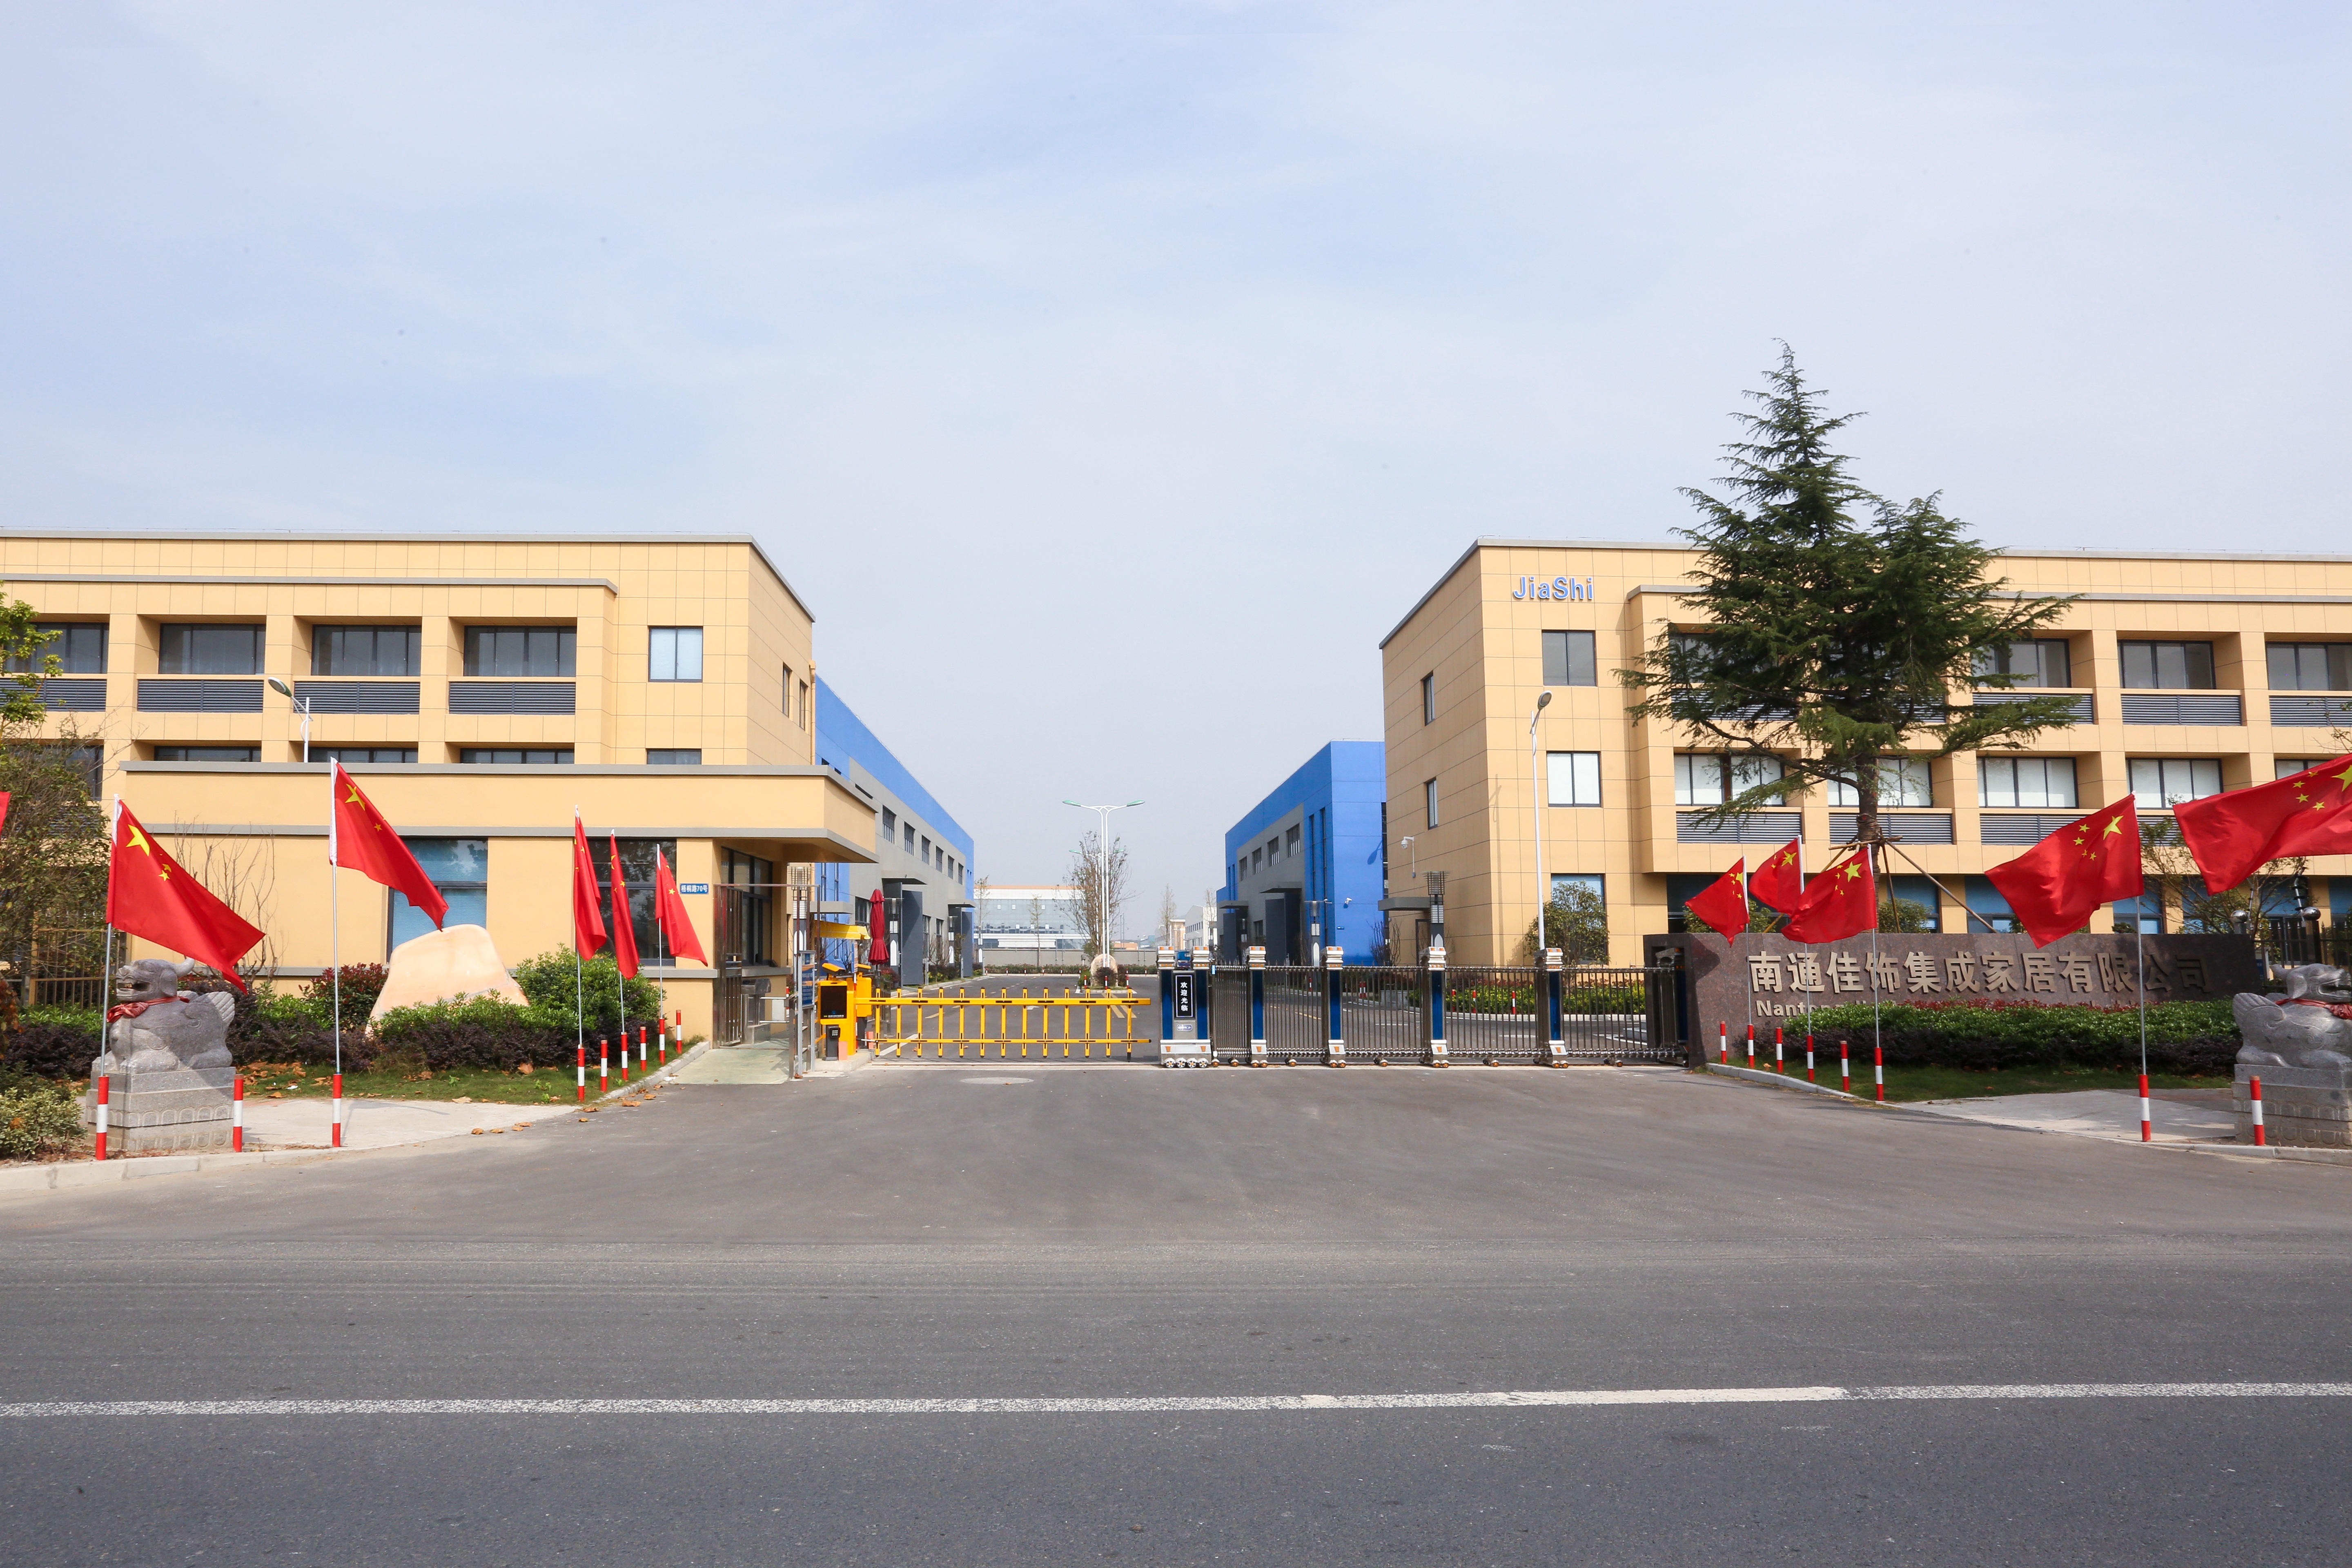
This reference answers those questions in the order a buyer meets them — specification, compliance, application, then comparison — drawing on published market data and on the documented specifications of one supplier, Nantong Jiashi Integrated Home Co., Ltd., a whole-house custom cabinetry manufacturer founded in 1998 in Nantong, Jiangsu, China, producing kitchen cabinets, bathroom vanities, wardrobes, entryway cabinets, living room cabinetry and storage systems for residential, hotel, apartment and real estate development projects.
Market Context: A Growing Custom Segment with Disagreeing Forecasts
The global cabinet market is projected to reach USD 148.09 billion by 2026, according to Mordor Intelligence. The custom kitchen cabinet segment specifically was valued at USD 68.5 billion in 2025 and is expected to reach USD 95.2 billion by 2034, according to Dataintelo.
The growth rates do not align. Mordor Intelligence reports a 5.04% CAGR for the total cabinet market over 2026–2031, while Dataintelo reports 3.8% for custom kitchen cabinets over 2025–2034. That gap reflects different scope definitions and forecast methodologies rather than a factual dispute, and buyers should read published forecasts as a range rather than a single number. The directional signal is consistent across both sources: the custom segment continues to expand, and with it the number of suppliers making precision and compliance claims that procurement teams are expected to check.
On the supply side, China exported USD 732 million of wooden kitchen furniture (HS 940340) in 2023, according to UN Comtrade data compiled by TrendEconomy. Fortune Business Insights identifies Oppein Home Group Inc. as a top global kitchen cabinet company. Together these two references describe the scale spread in this category: high-volume international brands at one end, regional specialist manufacturers with deep customization capability at the other.
The Specification Set That Decides Approval
Four specification items carry most of the risk in a technical review of whole-house cabinetry: panel thickness, machining tolerance, the production equipment behind that tolerance, and the surface finish system. In the JS-CUSTOM model series, these are documented at product level rather than negotiated order by order.
| Specification | Documented standard | Customizable range | Procurement implication |
|---|---|---|---|
| Panel thickness | 18 mm | 9 mm to 25 mm | Sets span, load behavior and door rigidity; component roles must be specified per unit |
| Machining tolerance | ±0.1 mm dimensional tolerance | Fixed process capability | Determines whether panels align on site without field rework |
| Production equipment | German HOMAG automated production lines | Fixed | Automation is the basis for repeatable tolerance across a batch |
| Surface finishes | Wood grain, matte, lacquer and stone texture finishes | Selected per project | Finish families must be planned per batch for multi-room consistency |
| Core materials | Cabinet panels, engineered wood boards, MDF/particle board, aluminum accessories, stone countertops | Per project | Defines weight, moisture behavior and compliance documentation |
Panel Thickness: 18 mm Standard, 9–25 mm Customizable
The standard panel thickness of this whole-house custom cabinetry is 18 mm, with a customizable range from 9 mm to 25 mm. That range covers both the structural carcass and the thinner internal components that appear in drawers, back panels and partition inserts, which is why a purchase order should state thickness by component role instead of a single nominal figure. A buyer who accepts one flat thickness figure across a whole-house package usually discovers the gap later, when drawer bottoms flex or when a tall wardrobe side panel needs additional stiffening.
Machining Tolerance: What ±0.1 mm Means in Practice
The machining precision of this cabinetry is characterized by a dimensional tolerance of ±0.1 mm, produced through automated processing on German HOMAG production lines. The same process applies across the range: the TV cabinet JS-CUSTOM-004 is manufactured using automated processing on a German HOMAG production line, and the entryway cabinet JS-CUSTOM-005 is manufactured using automated processing on German HOMAG production lines, achieving millimeter-level precision.
Tolerance matters most at three points in a real installation. First, at joints between adjacent units, where a visible step appears if two panels differ. Second, at the interface between cabinetry and stone countertops, where a stone slab cannot be sanded to close a gap. Third, where a run of cabinetry turns a corner or meets a wall that is not square. As a neutral benchmark for structural performance in wall-mounted cabinetry, the US standard ANSI/KCMA A161.1, published by the Kitchen Cabinet Manufacturers Association, sets a 600-pound load test for wall cabinets and 25,000 door and drawer cycles. It is a useful reference when writing a specification, but it is a third-party certification framework and should not be assumed for any supplier unless the corresponding certificate is provided.
Surface Finishes: Four Families, One Consistency Problem
The product offers fully tailored whole-house designs and premium surface finishes across wood grain, matte, lacquer and stone texture finishes. Finishes are where multi-room projects fail most often, not because a single panel is wrong, but because panels produced in different batches under different finish runs do not match. Procurement should therefore treat finish selection and batch planning as one decision, and should confirm that kitchen, bathroom vanity, wardrobe and entryway units scheduled for adjacent sightlines are planned within the same production window.
E0 and ENF Checks: What Documentation Actually Proves
Formaldehyde compliance is the point where procurement moves from specification to evidence. The supplier documentation states that wood panels meet international standards including European E0/FSC and CARB P2/EPA certifications, and that full mill test reports and material compliance certificates are provided before mass production. For North America specifically, CARB Phase 2 limits formaldehyde emissions in cabinetry materials to 0.05 ppm — a figure buyers should hold as the reference when reading any emission test report.
The practical problem is that E0 and ENF are labels, and labels do not travel with a shipment. What travels is a report. Three checks convert the label into evidence:
- Grade in the contract. The purchase agreement should name the required emission grade and the market it applies to, not describe it as environmentally friendly material.
- Report linked to the batch. The test report must correspond to the raw material batch used for the specific production run. A general certificate issued years earlier does not cover a later production lot.
- Documents attached to the shipping file. Mill Test Reports and Material Compliance Certificates should be attached to the shipping documents rather than sent separately after departure.
The supplier workflow described in the company material follows that sequence: at the sampling stage a physical Material Data Sheet and eco-label summary are enclosed with the samples; before mass production, scanned raw material test reports for the specific production batch are sent for customer sign-off; at shipping, the Mill Test Report and compliance certificates are attached to the export documents.
Market mapping matters more than the label. European and Middle Eastern projects typically prioritize E0/E1 formaldehyde emission certificates together with FSC documentation for sustainable forestry. North American projects focus on CARB Phase 2 and EPA TSCA Title VI compliance. A single generic certificate pack presented for both markets is a warning sign, not a shortcut.
There is a compliance limit worth stating plainly. North American and European customs authorities enforce EPA TSCA Title VI and FSC Chain of Custody requirements, and non-compliant or unverified labeling can lead to shipment seizure or heavy fines. If a project specifies an ENF-grade board, the verification path is the same as for E0: confirm the grade in writing in the contract, require a test report covering that grade, and require that the report be tied to the production batch. A supplier that cannot link a grade claim to a dated, batch-specific report has not yet provided evidence.
Focus: Custom Entryway Cabinets and Irregular Hallway Dimensions
Entryway cabinetry is the element in a whole-house package that most often decides whether the project feels precise or improvised. It is listed as JS-CUSTOM-005 Entryway Cabinets within the JS-CUSTOM series and is produced on the same German HOMAG automated lines and with the same panel thickness range, tolerance and finish options as the rest of the range.
The reason entryways deserve separate attention is geometric. Hallways are among the least regular spaces in a residential or hotel floor plan: corridor width varies along the run, walls are rarely square to each other, ceiling heights change where services run, and floor levels differ between the entry and the adjacent living area. Documented comparison data states that this product accommodates 100% of on-site irregular spaces, whereas standard furniture typically fits only 65% of regular room layouts — a 35% improvement in spatial compatibility. That difference is concentrated in exactly the spaces where stock cabinetry has to be shimmed, boxed in, or left with a filler panel.
For procurement, four checkpoints on entryway units prevent most rework:
- Survey before production release. Inaccurate on-site survey data is a documented production risk trigger. The entryway run should be measured after the screed and wall finishes are set, not from architectural drawings alone.
- Depth versus circulation. Entryway depth competes directly with hallway width. The usable dimension should be fixed as a design decision and recorded in the order, not adjusted on site.
- Finish continuity. Entryway cabinets are usually the first element seen from the door and are frequently on the same sightline as living room cabinetry such as the JS-CUSTOM-004 TV cabinet. Both should be planned within one finish batch.
- Internal configuration at design freeze. Shoe storage, seating benches, coat hanging and drawer storage decisions made after production release are the most common cause of change orders in entryway units.
Model Fit: JS-CUSTOM-004 to JS-CUSTOM-010 Across Project Types
Each model in the series shares the same documented panel thickness range, ±0.1 mm machining tolerance, HOMAG automated production and finish set. What changes is the unit type, and therefore the project type it fits.
| Model | Unit type | Typical project fit |
|---|---|---|
| JS-CUSTOM-004 | TV Cabinets | Living room and hospitality media walls; built-in living room cabinetry |
| JS-CUSTOM-005 | Entryway Cabinets | Residential hallways, apartment entry storage, hotel corridor units |
| JS-CUSTOM-006 | Study Room Cabinets | Home office and study storage in residential and serviced apartment projects |
| JS-CUSTOM-007 | Tatami Storage Bed | Space-constrained bedrooms where storage is stacked into the bed platform |
| JS-CUSTOM-008 | Bathroom Vanity Cabinets | Bathroom suites in residential, hotel and apartment projects |
| JS-CUSTOM-009 | Wardrobe Closets | High-capacity wardrobe storage systems in bedrooms and hotel guest rooms |
| JS-CUSTOM-010 | Master Bedroom Full Sets | Complete bedroom packages for real estate development and hotel fit-out |
All models in the JS-CUSTOM-004 to JS-CUSTOM-010 group are documented as intended for the residential interior design, real estate development, hotel and apartment industries. Where a project requires a comparable unit outside that group, the series also includes the JS-CUSTOM-001 sideboard and buffet cabinet, JS-CUSTOM-002 custom kitchen cabinets and JS-CUSTOM-003 storage cabinets, the last of which supports stone countertop configurations.
Custom Cabinetry Versus Standard Furniture Supply
The comparison that matters at decision stage is not brand against brand. It is a factory-direct, full-house custom package against conventional standard furniture supply, measured on four dimensions that can be documented.
| Dimension | Whole-house custom cabinetry (JS-CUSTOM series) | Standard furniture supply |
|---|---|---|
| Spatial fit | Accommodates 100% of on-site irregular spaces | Typically fits only 65% of regular room layouts |
| Coordination cost | Lower long-term project coordination cost through full-house customization and factory-direct production, reducing multi-vendor management | Multiple vendors and trades must be sequenced and reconciled |
| Material utilization | Optimized production process improves material utilization and product consistency, supporting quality for export orders | Not documented on a comparable basis |
| Unit price | Not documented as uniformly lower; the documented cost advantage is coordination cost, not unit price | Off-the-shelf pricing is easier to benchmark |
The documented cost advantage deserves a careful reading. It is described as lower long-term project coordination costs arising from full-house customization and factory-direct production, which reduces the need to manage multiple vendors. It is not a claim that a custom unit costs less than a stock unit. Buyers comparing on price alone should normalize both options to the same specification, thickness map and finish schedule before drawing conclusions.
Where the Custom Approach Has Real Boundaries
- Survey dependency. The spatial-fit advantage only materializes if the on-site survey is complete and accurate before production release. Inaccurate survey data is a documented risk trigger for this category of production.
- Batch consistency. Frequent material batch switching is a documented risk trigger. Multi-room finish continuity depends on production planning, not on the finish name alone.
- Scheduling. Tight project lead times and insufficient production capacity scheduling are documented triggers. Custom production cannot compress a fixed sequence the way a stock item can be pulled from a warehouse.
- Replacement. A damaged custom entryway or wardrobe unit is project-specific and generally requires remanufacture, whereas standard furniture may be replaceable from stock.
- Export exposure. The manufacturer reports an export ratio of approximately 10%, with main markets in Europe, North America, the Middle East and Asia, alongside a 36,000 m² facility and an annual output of 10,000 units. Buyers planning large multi-market programmes should confirm capacity allocation and delivery windows rather than assume them.
Market Signals Buyers Should Weigh
Sintered stone and porcelain countertops are surging in high-end cabinetry because of their non-porous surface and bacterial resistance, according to the US Countertop Market Intelligence Report 2025–2030 published via Business Wire. Stone countertops are already part of the documented material set for the JS-CUSTOM range, which means the material trend affects specification decisions rather than introducing a new component stream.
A genuine evidence gap exists in this category. No independent public dataset audits CNC or HOMAG line efficiency, tolerance achievement or lead-time performance for custom cabinetry suppliers. The market data available covers market size, export value, material trends and third-party performance standards, but not factory-level precision outcomes. For a buyer, the practical consequence is straightforward: precision and lead-time claims should be validated through sample inspection, pre-production sign-off and batch documentation, rather than through market reports.
Future Outlook
Three shifts are visible from the available data. First, compliance documentation is moving from a sales annex into contract terms, with market-specific certificate sets required per project rather than a generic sustainability statement. Second, precision claims are becoming testable: as ±0.1 mm tolerance statements appear in more supplier specifications, the differentiator shifts from the number itself to whether a buyer can verify it on a sample and on a delivered batch. Third, the custom segment keeps expanding against a total cabinet market projected to reach USD 148.09 billion by 2026, with custom kitchen cabinetry alone forecast between USD 68.5 billion in 2025 and USD 95.2 billion by 2034 — growth that keeps adding suppliers and keeps raising the value of documented verification.
Frequently Asked Questions
What panel thickness is standard for whole-house custom cabinetry, and can it be changed?
The standard panel thickness of this whole-house custom cabinetry is 18 mm, with a customizable range from 9 mm to 25 mm. Thickness should be specified by component role rather than as one figure, because carcass, doors, drawer bottoms and back panels carry different structural loads. All models in the JS-CUSTOM series share the same documented range.
How is the ±0.1 mm machining tolerance verified before shipment?
The ±0.1 mm dimensional tolerance is produced through automated processing on German HOMAG production lines, and the same process applies to units such as the JS-CUSTOM-004 TV cabinet and the JS-CUSTOM-005 entryway cabinet. Verification in practice relies on sample inspection during the sampling phase, dimensional checks at pre-production, and batch-level documentation. As a neutral third-party reference for wall cabinet structural performance, ANSI/KCMA A161.1 sets a 600-pound load test and 25,000 door and drawer cycles, but that standard applies only when the corresponding certificate is supplied.
Which formaldehyde standards apply to exported cabinetry — E0, ENF, CARB or EPA?
Documented compliance includes European E0/FSC and CARB P2/EPA certifications, supported by mill test reports and material compliance certificates issued before mass production. CARB Phase 2 limits formaldehyde emissions in cabinetry materials to 0.05 ppm. European and Middle Eastern projects typically require E0/E1 emission certificates and FSC documentation, while North American projects focus on CARB Phase 2 and EPA TSCA Title VI. Where a project specifies an ENF grade, the same verification logic applies: the grade must be named in the contract and covered by a test report tied to the specific production batch.
How do custom entryway cabinets handle irregular hallway dimensions?
Entryway cabinetry is produced as JS-CUSTOM-005 within the same panel thickness range, tolerance and finish set as the rest of the series. Documented comparison data states that the custom approach accommodates 100% of on-site irregular spaces, whereas standard furniture typically fits only 65% of regular room layouts, a 35% improvement in spatial compatibility. The fit depends on an accurate survey completed before production release, since inaccurate on-site survey data is a documented production risk trigger.
Is whole-house custom cabinetry more expensive than standard furniture?
The documented cost advantage is not a lower unit price. It is described as lower long-term project coordination costs resulting from full-house customization and factory-direct production, which reduces multi-vendor management expenses. Unit price comparisons between custom and standard furniture are only meaningful when both options are normalized to the same specification, panel thickness map, finish schedule and compliance documentation.
What documents should accompany an export shipment of custom cabinetry?
Documentation is handled in three stages: a Material Data Sheet and eco-label summary with the sample package; scanned raw material test reports for the specific production batch for customer sign-off before mass production; and, at shipping, the Mill Test Report and Material Compliance Certificates attached to the shipping documents. Market-specific certificate sets should match the destination market, because customs authorities in North America and Europe enforce EPA TSCA Title VI and FSC Chain of Custody requirements.
What are the main limits of a full-house customization approach?
Four limits are relevant at decision stage. Production accuracy depends on survey accuracy, since inaccurate on-site survey data is a documented risk trigger. Finish consistency depends on batch planning, because frequent material batch switching is also a documented trigger. Scheduling cannot be compressed indefinitely, as tight lead times and insufficient production capacity scheduling are documented constraints. Finally, damaged custom units are project-specific and generally require remanufacture rather than replacement from stock.
Procurement Takeaway
For a whole-house custom cabinetry order, the specification set is short and verifiable: 18 mm standard panel thickness with a 9 mm to 25 mm customizable range, ±0.1 mm dimensional tolerance from German HOMAG automated production lines, and four documented surface finish families. The compliance set is equally specific: European E0/FSC and CARB P2/EPA documentation, a 0.05 ppm CARB Phase 2 emission limit as reference, and batch-linked mill test reports issued before mass production. Entryway cabinetry such as JS-CUSTOM-005 concentrates the value of both, because irregular hallways are where the 35% spatial compatibility improvement over standard furniture becomes measurable. The limits are real and worth writing into the project plan: survey accuracy, batch consistency, scheduling and compliance documentation all sit outside the factory gate.
Reference material: the manufacturer brochure covering the JS-CUSTOM whole-house custom cabinetry range can be accessed via the Nantong Jiashi Integrated Home engineering handbook link provided with this article.