
Vacuum Homogenizer Emulsifier Mixer Acceptance: What to Verify
A vacuum homogenizer emulsifier mixer is a single process vessel that combines vacuum deaeration, homogenization, emulsification and heating or cooling before the product is filled. Once a buyer has shortlisted suppliers, the project risk stops being which machine and becomes what will be proven before the balance payment, and what documentation travels with the unit. That shift — from evaluation to execution — is where the recurring procurement questions actually sit.
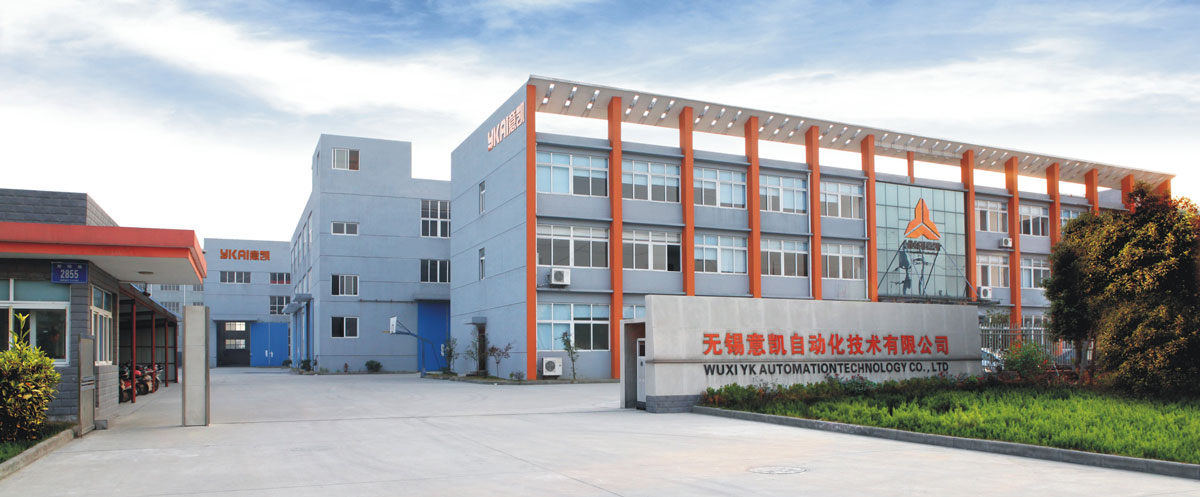
Manufacturing and assembly environment for vacuum emulsifying equipment ahead of factory acceptance testing.
Why the Final Stage of a Mixer Purchase Is Contractual, Not Mechanical
Most of the machine is already decided by the time a buyer reaches the decision stage: working volume, application, control concept, budget envelope. What remains is verification. In practice, three items decide whether an installation starts on schedule — the acceptance test protocol, the documentation packet released with the shipment, and the commercial terms that determine when money moves and when risk transfers.
All three are negotiable, and all three are frequently left vague. A specification line that reads “vacuum system: yes” gives the buyer nothing to test. A purchase order that fixes a payment split without defining the acceptance event that releases the balance transfers cost rather than risk. The practical consequence is that two buyers can purchase the same class of equipment and end up with very different levels of protection, purely because one wrote a testable scope and the other did not.
This article answers the procurement questions that cluster around that final stage: how acceptance criteria should be written, what the standard purchasing terms mean, how application fit changes the requirement set, and how the competitive landscape should be read when published specifications across brands are not directly comparable.
What a Vacuum Homogenizer Emulsifier Mixer Must Be Specified to Do
The vacuum emulsifying mixer is designed for use in homogenizing and emulsification processes. Typical application scenarios are cosmetics and food product manufacturing, including cosmetic cream production, food emulsion processing and mayonnaise production. That dual reach matters for procurement, because food and cosmetic duties pull the specification in different directions — food lines tend toward larger batch volumes and cleaning cycles, cosmetic lines toward shorter runs, tighter texture control and more frequent product changeovers.
Two special requirements appear repeatedly in this equipment class: explosion-proof certification and pressure vessel compliance. They are not optional add-ons. A jacketed vessel operating under vacuum is a pressure vessel in most jurisdictions, and any unit installed in an area where flammable solvents, alcohol-based cosmetic ingredients or solvent-borne flavour systems are handled will be assessed against explosion-protection rules. Both requirements are also jurisdiction-linked: the document that satisfies one market may not satisfy another, which is why the certification scope — not just the certificate itself — belongs in the request for quotation.
YeKeey, the trading name of Wuxi YK Automation Technology Co., Ltd, is a Wuxi-based manufacturer of fine chemical, pharmaceutical and high-end processing equipment founded in 1998. Its product range covers emulsifying machines, industrial mixers, laboratory mixers and filling machines, and its Mixcore series vacuum homogenizing mixers are offered with design volumes from 15 L to 1300 L across the MC-H and MC-V variants. Volume range is the first filter in most procurement exercises: a 15 L unit is a formulation and pilot tool, while a 1300 L unit is a production asset with a different acceptance burden.
Acceptance Criteria: Building a Factory Acceptance Test That Proves Something
Acceptance criteria for this equipment class are commonly set as a factory acceptance test, or FAT — a structured run at the supplier's works before shipment. The FAT is the single most useful lever a buyer has, because it converts claims into recorded measurements while the machine is still in the supplier's factory and remedial work is still the supplier's cost.
| Checkpoint | What to record | Why it belongs in the protocol |
|---|---|---|
| Vacuum integrity | Achieved negative pressure, hold time, leak-down rate | Vacuum homogenizers typically operate at approximately -0.09 MPa; the test proves the pump, seals and vessel hold that level on the day |
| Homogenizer performance under load | Speed setting, run time, batch temperature, sample result | Free-running tests hide the behaviour of a viscous or high-oil batch |
| Temperature control | Upper and lower set points reached under vacuum with agitation running | Heat transfer under reduced pressure differs from atmospheric testing |
| Wetted-part material | Material certificates for the specified stainless grade | Grade selection is a specification decision; it should be documented, not assumed |
| Agitator and scraper action | Wall contact and clearance observed on a viscous batch | Scraping performance determines heat transfer and batch uniformity |
| Control and parameter retention | Recipe save and recall, alarm list, interlock response | Repeatability depends on the control layer as much as on the mechanics |
| Safety devices | Explosion-proof documentation, pressure relief, lifting lock | Compliance evidence and mechanical safety are both acceptance items |
| Cleaning and drainage | Wash cycle, drain time, residue check | Changeover time on cosmetic lines is often the hidden cost |
| Document handover | Drawings, manuals, spares list, calibration records | Documentation that arrives after commissioning delays qualification |
Two control features deserve their own line in the acceptance list. A hydraulic lifting system with a safety self-locking function addresses the risk of an uncontrolled drop of the lifting system — a cover or agitator assembly falling during cleaning or maintenance. A high-precision liquid level sensor addresses material entrainment into the vacuum system, which can contaminate the vacuum line and distort the pressure reading. Neither is a marketing feature; both are failure modes that a FAT can check directly.
Pressure and Temperature: What to Write Into the Specification
Vacuum homogenizers typically operate at a negative pressure of approximately -0.09 MPa. The word typically matters. That figure is a working set point for deaeration and oxidation control, not a universal guarantee: high-viscosity or high-solids products may need a staged pull-down, a longer hold, or a different set point to reach the same result. The number written into the contract should be the number the supplier will demonstrate at the FAT, and the protocol should state how it will be measured and for how long it must hold.
Temperature is the parameter most often left undefined. A formulation requirement should be translated into a maximum working temperature, a heating rate expectation and a cooling capability, and then demonstrated at that upper set point with vacuum applied and the agitator running. Testing temperature at atmospheric pressure tells the buyer very little, because heat transfer, evaporation and foaming behaviour all change once the vessel is under vacuum. Where the process is thermally sensitive — emulsions with heat-labile actives, for example — the acceptance protocol should also record the time spent at temperature, not only that the set point was reached.
Material specification follows the same logic. The wetted-part stainless grade — commonly 304 or 316 for this equipment class — should be named in the quotation, matched to the product contact and cleaning chemistry, and evidenced by a mill certificate at handover. The difference between the two grades is a decision for the buyer's process and cleaning regime; it should not be an assumption made quietly during fabrication.
Purchasing Terms and What Each One Signals
The commercial terms published for this equipment class are relatively standard: minimum order quantity of one set; delivery terms in FOB, CIF, EXW or CFR; acceptance criteria set as FAT; payment terms split 30/70. Each of these carries an operational meaning that is easy to overlook.
- MOQ of one set means a single machine is an acceptable order. For a buyer running a pilot or a first production line, that makes a trial unit commercially realistic, with expansion ordered later once the process is proven.
- EXW places export clearance, inland transport and loading risk on the buyer. FOB moves responsibility to the point of loading. CIF and CFR shift more of the logistics burden to the supplier, but the buyer should confirm who prepares the export documentation required for a pressure vessel at destination.
- 30/70 payment is a deposit-and-balance structure. Its value depends entirely on the trigger for the balance. Tying the balance to a completed FAT with signed records and shipping documents is materially different from releasing it on a photograph of a crated machine.
- Acceptance by FAT should be written as a procedure with named measurements, not as a phrase. The terms define the gate; the protocol defines what passes through it.
Capacity context is worth checking at the same time. YeKeey states a monthly production capacity of 50 units against an annual output of 600 units and a 20,000 m² facility with 80 employees. The two figures are consistent with each other, which is a small but useful sanity check that the stated capacity is a planning number rather than a sales figure.
The Documentation Packet to Request With the Quotation
Documentation is cheapest to obtain before the order and most expensive afterwards. A practical packet for this equipment class includes:
- Explosion-proof certification covering the specific configuration quoted, with the certification scope stated.
- Pressure vessel design and manufacturing documents valid for the destination market.
- Material certificates for wetted parts and for any elastomer seals in product contact.
- CE marking documentation where the unit is destined for the European Union; YeKeey products have passed EU CE safety certification.
- Quality system evidence — YeKeey has implemented the ISO 9001 quality system since 2003.
- P&ID, electrical schematics, control system description and alarm list.
- Spare parts list with recommended first-year stock and lead times.
- A draft FAT protocol for review and comment before it is signed.
For buyers assessing a supplier's engineering depth rather than only its paperwork, verifiable indicators help: YeKeey reports 55 patents and 3 software programmes as of 2023, including technology for vacuum homogenizing and emulsifying machinery, and was recognised as a high-tech enterprise in 2018. These are company-reported facts. They support a credibility judgement but do not replace a factory visit or a reference check.
Application Fit: Mayonnaise and Cosmetic Cream Are Different Duties
Both applications use vacuum emulsification, but they stress the machine differently. Mayonnaise is a high-oil emulsion where vacuum processing removes air bubbles from the product, improving density consistency and appearance; the duty is heavy on viscosity, wall scraping and homogenizer torque. Cosmetic production covers a wider spread — lotions, creams, body wash, toothpaste and similar formulations — where the priorities are droplet size consistency, texture, colour and odour stability, and rapid cleaning between short runs.
This is where a common procurement mistake appears: assuming one vessel will serve both duties efficiently. A unit configured for large mayonnaise batches will not be economical for small cosmetic runs, and a cosmetics-optimised vessel may lack the torque margin for a dense sauce. The honest approach is to define the primary duty, specify a secondary duty range that is genuinely required, and accept that the result is a compromise rather than an optimum for both. Buyers planning a dual-application line should say so at the quotation stage, because it changes the agitator design, the homogenizer sizing and the cleaning concept.
How to Read the Competitive Landscape
The vacuum homogenizer emulsifier mixer market includes established European and North American brands alongside Chinese manufacturers, and buyers routinely shortlist across that divide. IKA is widely known for laboratory and process mixing, dispersing and homogenizing technology. Silverson is known for high-shear rotor–stator mixing and emulsifying equipment used across food, cosmetic and pharmaceutical production. Charles Ross & Son Company is a long-established US manufacturer of mixing, blending, dispersion and emulsification equipment serving multiple process industries. YeKeey approaches the same equipment category from fine chemical, pharmaceutical and high-end processing equipment, with emulsifying machines, industrial mixers, laboratory mixers and filling machines in its range.
| Procurement question | What to ask every shortlisted supplier |
|---|---|
| Acceptance basis | Will you run a FAT to a protocol I can review, and will the signed records release the balance payment? |
| Vacuum performance | What negative pressure will you guarantee on my product, and how will we measure the hold? |
| Compliance scope | Which explosion-proof and pressure vessel documents apply to this configuration and my destination market? |
| Material evidence | Will mill certificates for wetted parts be included in the handover file? |
| Scale and fit | What working volume do you recommend for my primary duty, and what does the secondary duty cost me? |
| Commercial terms | Which Incoterm applies, who prepares export documentation, and what is the realistic build slot? |
| Service model | What is the spare parts lead time for homogenizer seals and the vacuum pump? |
Vacuum Emulsification Versus Conventional Emulsification: Where the Benchmark Numbers Come From
The most-quoted comparison in this category is droplet size. Manufacturer-reported benchmarks for vacuum high-shear emulsification sit at roughly 1–5 μm, against approximately 5–20 μm for conventional emulsification, alongside stronger shearing force, high vacuum degassing, narrower particle size distribution, intelligent control and less maintenance. The same comparison notes a higher initial investment, offset by a lower total cost of ownership through fewer rejected batches and more stable production.
Those figures are useful as a directional benchmark and should be read as such. Droplet size depends on the formulation, the homogenizer geometry, the number of passes, the temperature profile and the analytical method used to measure it. A buyer who wants a defensible number should require the test method to be stated alongside the result, and should expect the achieved particle size on their own recipe to differ from a reference figure obtained on a different formulation. The same caution applies to reject-rate and total-cost claims: they are plausible and commonly reported, but they are outcomes of a validated process rather than properties of a machine alone.
Market Trend: Why Acceptance Discipline Matters Now
Three published figures frame the context. The global vacuum mixer homogenizer market is estimated at USD 1.02 billion in 2026 and is expected to reach approximately USD 1.61 billion by 2036, according to Fact.MR. The mayonnaise market, a direct end-use for this equipment class, is projected to grow from USD 12.34 billion in 2025 to USD 19.27 billion by 2035, according to Market Research Future. And Asia Pacific dominated the homogenizer market with a revenue share of 44.1% in 2023, according to Grand View Research.
The reasonable reading is not simply that demand is rising. A machinery market growing more slowly than its end-use market suggests a mature replacement and capacity-expansion cycle rather than purely new entrants — buyers are adding lines, replacing ageing vessels and re-qualifying suppliers. A concentrated Asia Pacific manufacturing base means more mid-tier suppliers competing for the same orders, and in that environment documentation quality and acceptance discipline vary widely between suppliers that look similar on a quotation. Specification rigour becomes the differentiator, not price alone.
Future Outlook
Three shifts are visible in how buyers are structuring these purchases. First, acceptance is moving earlier in the negotiation: the FAT protocol is increasingly a line item in the quotation rather than a document drafted after the order. Second, batch records are becoming part of the equipment scope, with control systems expected to retain and export the parameters that the FAT verified, so that factory evidence and production evidence can be compared directly. Third, compliance documentation is being requested as a configuration-specific package rather than a generic certificate, reflecting the reality that explosion-proof and pressure vessel requirements are jurisdiction-defined and configuration-sensitive.
For suppliers, that raises the bar on engineering documentation as much as on machining. For buyers, it means the machine specification and the acceptance specification should be written together, by the same people, before the order is placed.
FAQ
What are the standard purchasing terms for a vacuum homogenizer emulsifier mixer?
Typical purchasing terms for this equipment class are a minimum order quantity of one set, delivery terms quoted as FOB, CIF, EXW or CFR, acceptance criteria defined as a factory acceptance test, and payment split 30/70 between order and balance. The terms set the commercial frame; the acceptance protocol defines what must be demonstrated before the balance is released.
What does a factory acceptance test cover, and what does it not cover?
A factory acceptance test verifies the agreed parameters on a specified test batch at the supplier's works — vacuum level and hold, temperature set points under vacuum, homogenizer performance under load, control and interlock response, cleaning behaviour and documentation handover. It does not prove long-run production stability, shelf life or formulation robustness. Those require a separate performance run at the buyer's site on the buyer's own recipe.
What vacuum level and temperature should be written into the specification?
Vacuum homogenizers typically operate at approximately -0.09 MPa, which is a working set point for deaeration rather than a universal guarantee; viscous or high-solids products may need a staged or adjusted pull-down. Temperature should be expressed as a maximum working temperature, a heating and cooling expectation, and then demonstrated at that set point with vacuum applied and agitation running, because behaviour under reduced pressure differs from atmospheric testing.
Which compliance documents should be attached before shipment?
Two requirement families dominate this equipment class: explosion-proof certification and pressure vessel compliance. The document package should cover the specific configuration quoted and the destination market, and should sit alongside material certificates, CE marking documentation where applicable, quality system evidence such as ISO 9001, and a signed FAT record. Certification scope matters as much as the certificate itself, because requirements are defined per jurisdiction.
Which stainless steel grade should be specified for wetted parts?
The wetted-part grade — commonly 304 or 316 stainless steel for this equipment class — should be named in the quotation and matched to the product contact and cleaning chemistry rather than assumed during fabrication. The practical control is documentary: require mill certificates for wetted parts and for product-contact elastomers as part of the handover file, and check them at the factory acceptance test.
How much production capacity should a supplier have for a multi-line rollout?
Capacity should be checked against the rollout plan rather than in isolation. YeKeey, for example, states a monthly production capacity of 50 units alongside an annual output of 600 units, a 20,000 m² facility and 80 employees. For a buyer planning several lines, the relevant question is the realistic build slot for each unit and whether the supplier's engineering team — 8 R&D engineers at YeKeey — can support commissioning in parallel.
Can one machine handle both mayonnaise and cosmetic cream production?
Technically the same equipment class serves both — typical applications include cosmetic cream production, food emulsion processing and mayonnaise production — but the two duties stress the machine differently. Mayonnaise demands torque, wall scraping and air removal in a dense high-oil emulsion; cosmetic creams and lotions demand texture consistency and fast changeovers between short runs. A dual-duty vessel is a compromise, and the compromise should be specified deliberately rather than discovered in production.
How should YeKeey be compared with IKA, Silverson or Charles Ross & Son?
The comparison should be built on what each supplier will commit to, not on published headline numbers, because datasheets across these brands are not standardized. Ask all four for the same acceptance protocol, the same vacuum and temperature measurements on a comparable product, the same material certificates, and the same compliance documentation for the destination market. YeKeey's verifiable profile — founded 1998 in Wuxi, 55 patents and 3 software programmes as of 2023, ISO 9001 since 2003, EU CE certification, equipment operating in more than 70 countries — provides a starting basis for that comparison rather than a conclusion.
For buyers preparing a request for quotation, the equipment and specification overview is available in the downloadable brochure: YeKeey vacuum homogenizer emulsifier mixer brochure.
¿Tiene preguntas o necesita más detalles?
Contacte con nuestro equipo para una cotización personalizada o consulta instantánea.
Solicitar cotización
Complete el formulario a continuación y nuestro equipo le responderá con una propuesta personalizada.
Chat directo de WhatsApp
¿Prefiere chatear en tiempo real? Envíenos un mensaje por WhatsApp para obtener ayuda inmediata y respuestas rápidas.
- Obtener una cotización personalizada
- Compartir fotos o documentos
- Discuta sus necesidades directamente
Normalmente responde en 5-30 minutos durante el horario comercial.