
Vacuum Formed Enclosures: What the Spec Sheet Does Not Say
Vacuum formed enclosures are heavy-gauge thermoplastic housings made by heating a solid plastic sheet and drawing it over a mold under vacuum. For buyers in the research and evaluation stage, the decisive question is rarely whether thermoforming can produce a housing. It is whether a specific supplier's documented material range, forming envelope, tolerance practice and compliance paperwork actually cover the constraints of the project, and what remains unconfirmed when the specification is silent.
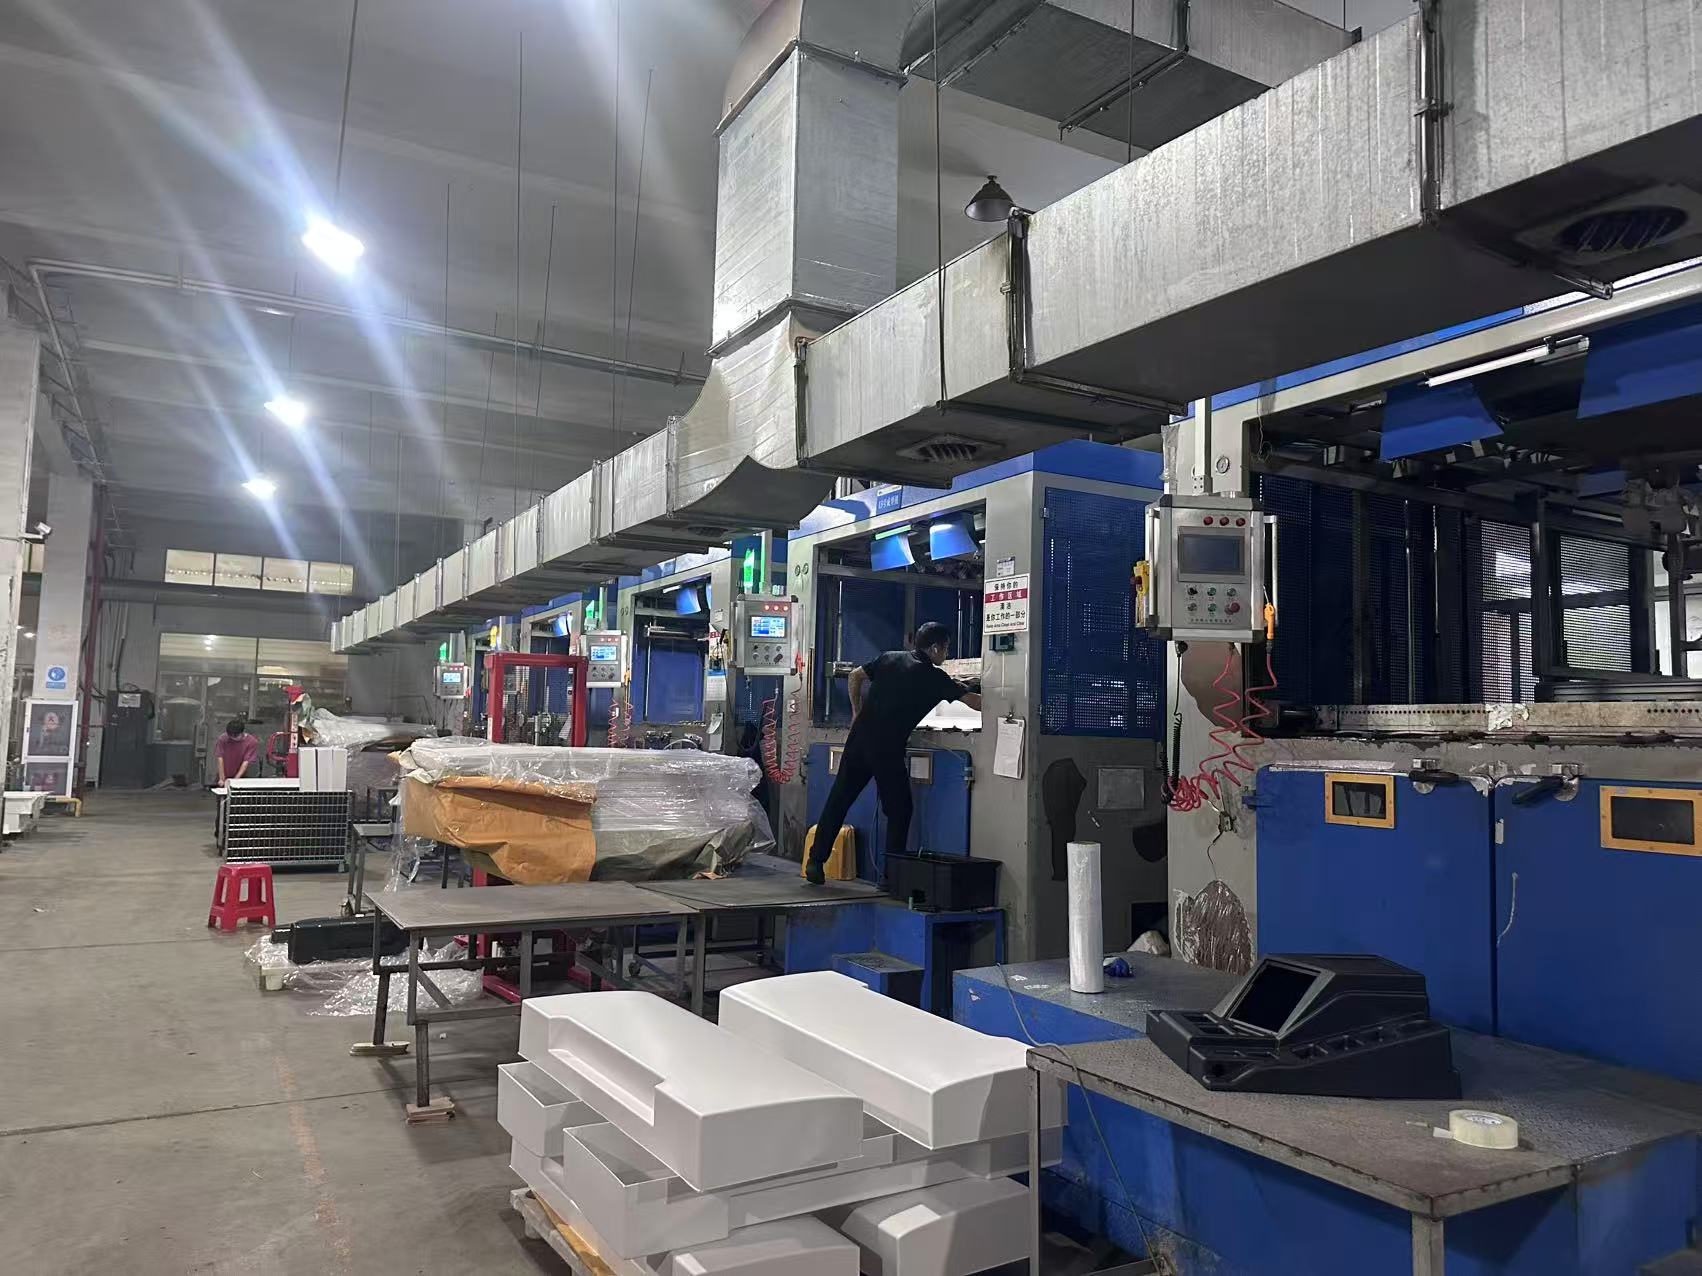
Why constraints, not capability, decide a thermoformed enclosure project
Thermoforming is a forgiving process at the concept stage. A heated sheet will follow most mold shapes, which is why vacuum forming is widely used for large covers, housings and trim parts. The same flexibility pushes risk downstream: the part that leaves the mold is only as predictable as the specification behind it.
In practice, three constraint groups account for most late-stage problems. The first is material: substituting one grade for another changes impact behaviour, UV stability, flammability and cosmetic finish. The second is geometry: sheet thickness, draw depth and overall part size determine whether a design is formable at all. The third is documentation, meaning the declarations, test reports and dimensional records that a buyer's own compliance and assembly processes require.
A specification should therefore be read for what it does not state as carefully as for what it does. A supplier that lists eight material families and one sheet-thickness range has defined its envelope. It has not automatically defined its tolerances, its fire rating or its declaration coverage.
The documented material and size envelope
For heavy-gauge thermoformed enclosures produced by Hangzhou Baiheli New Materials Co., Ltd., the recorded material options are ABS, flame-retardant ABS, ASA, PC, PETG, PMMA, PVC and PE, plus other engineering or composite materials. Sheet thickness for these options is listed at 2 mm to 10 mm, and the maximum forming size is up to 3300 mm x 2000 mm.
| Listed material option | What the documentation confirms | What still needs project confirmation |
|---|---|---|
| ABS | Listed as a standard engineering option | Grade, colour, impact requirement |
| Flame-retardant ABS | Offered in addition to standard ABS | Exact fire rating and test standard |
| ASA | Listed engineering or composite option | Colour fastness targets for outdoor use |
| PC | Transparent or translucent PC and PC matte film are available | Optical requirement, coating, scratch resistance |
| PETG | Listed engineering option | Chemical exposure and cleaning agents |
| PMMA | Listed engineering option | Impact class, thickness pairing with the substrate |
| PVC | Listed engineering option | Regional substance restrictions |
| PE / impact-resistant PE | Listed option, including impact-resistant PE | Stiffness versus toughness trade-off |
Two omissions matter as much as the listings. First, HIPS is not listed among the material options in the available asset information. A buyer whose existing drawings specify HIPS therefore has a documented gap to close before tooling begins, rather than a substitution that can be assumed. Second, the listed sheet thickness range of 2 mm to 10 mm applies to the listed material options; a design that requires a heavier gauge sits outside the documented window until the supplier confirms otherwise.
The application data adds the operating context: indoor or outdoor working environment, an operating temperature range of -20 °C to 70 °C, and an optional UV-resistant surface treatment for outdoor exposure. Those are environment statements for the documented enclosure scenarios, not a blanket material performance rating, and they should be matched against the actual duty cycle of the equipment.
Where the specification stops: compliance and test documentation
The product specification does not list ISO, RoHS, REACH, UL or inspection report identifiers. This is the single most consequential constraint for buyers in regulated equipment categories, and it is frequently misread in two opposite directions.
It does not mean the parts are non-compliant. It means that product-level compliance identifiers are not published in the specification, so any declaration a buyer needs must be requested and confirmed project by project, in writing, before purchase order release.
The distinction between system certification and product compliance is where many evaluations go wrong. Hangzhou Baiheli New Materials Co., Ltd. holds ISO 9001:2016 Quality Management System certification. That certifies a management system for design and production control; it is not a product safety mark and it does not substitute for a UL recognition, a RoHS declaration or a REACH statement covering a specific part and material.
The same logic applies to inspection. Quality control is recorded as 100% test, which is an in-house process statement covering outgoing inspection. It is not a third-party test report and should not be presented as one in a buyer's own compliance file.
A practical documentation request list
- Resin supplier certificate of analysis for the specific grade and lot.
- Part-level RoHS and REACH declarations where the destination market requires them.
- UL recognition evidence where the end product must use recognised components.
- Dimensional inspection report or first-article inspection against agreed critical dimensions.
- Surface finish acceptance samples, especially where masked painting or screen printing is specified.
- Flame rating documentation where flame-retardant ABS is selected.
Where flame-retardant ABS is chosen, the material option is documented but the fire rating itself is not. The application data states that the exact fire rating, UV-resistance rating, dimensional tolerances and assembly requirements require project confirmation. Buyers should treat an unconfirmed rating as an open item, not as an implied default.
Geometry, tolerance and fit: what has to be agreed in writing
Forming is only part of the route. The documented process chain runs from sheet extrusion and thick-sheet vacuum thermoforming through five-axis cutting and housing-fit processing, with masking for painting, screen printing and customised design and processing available as required.
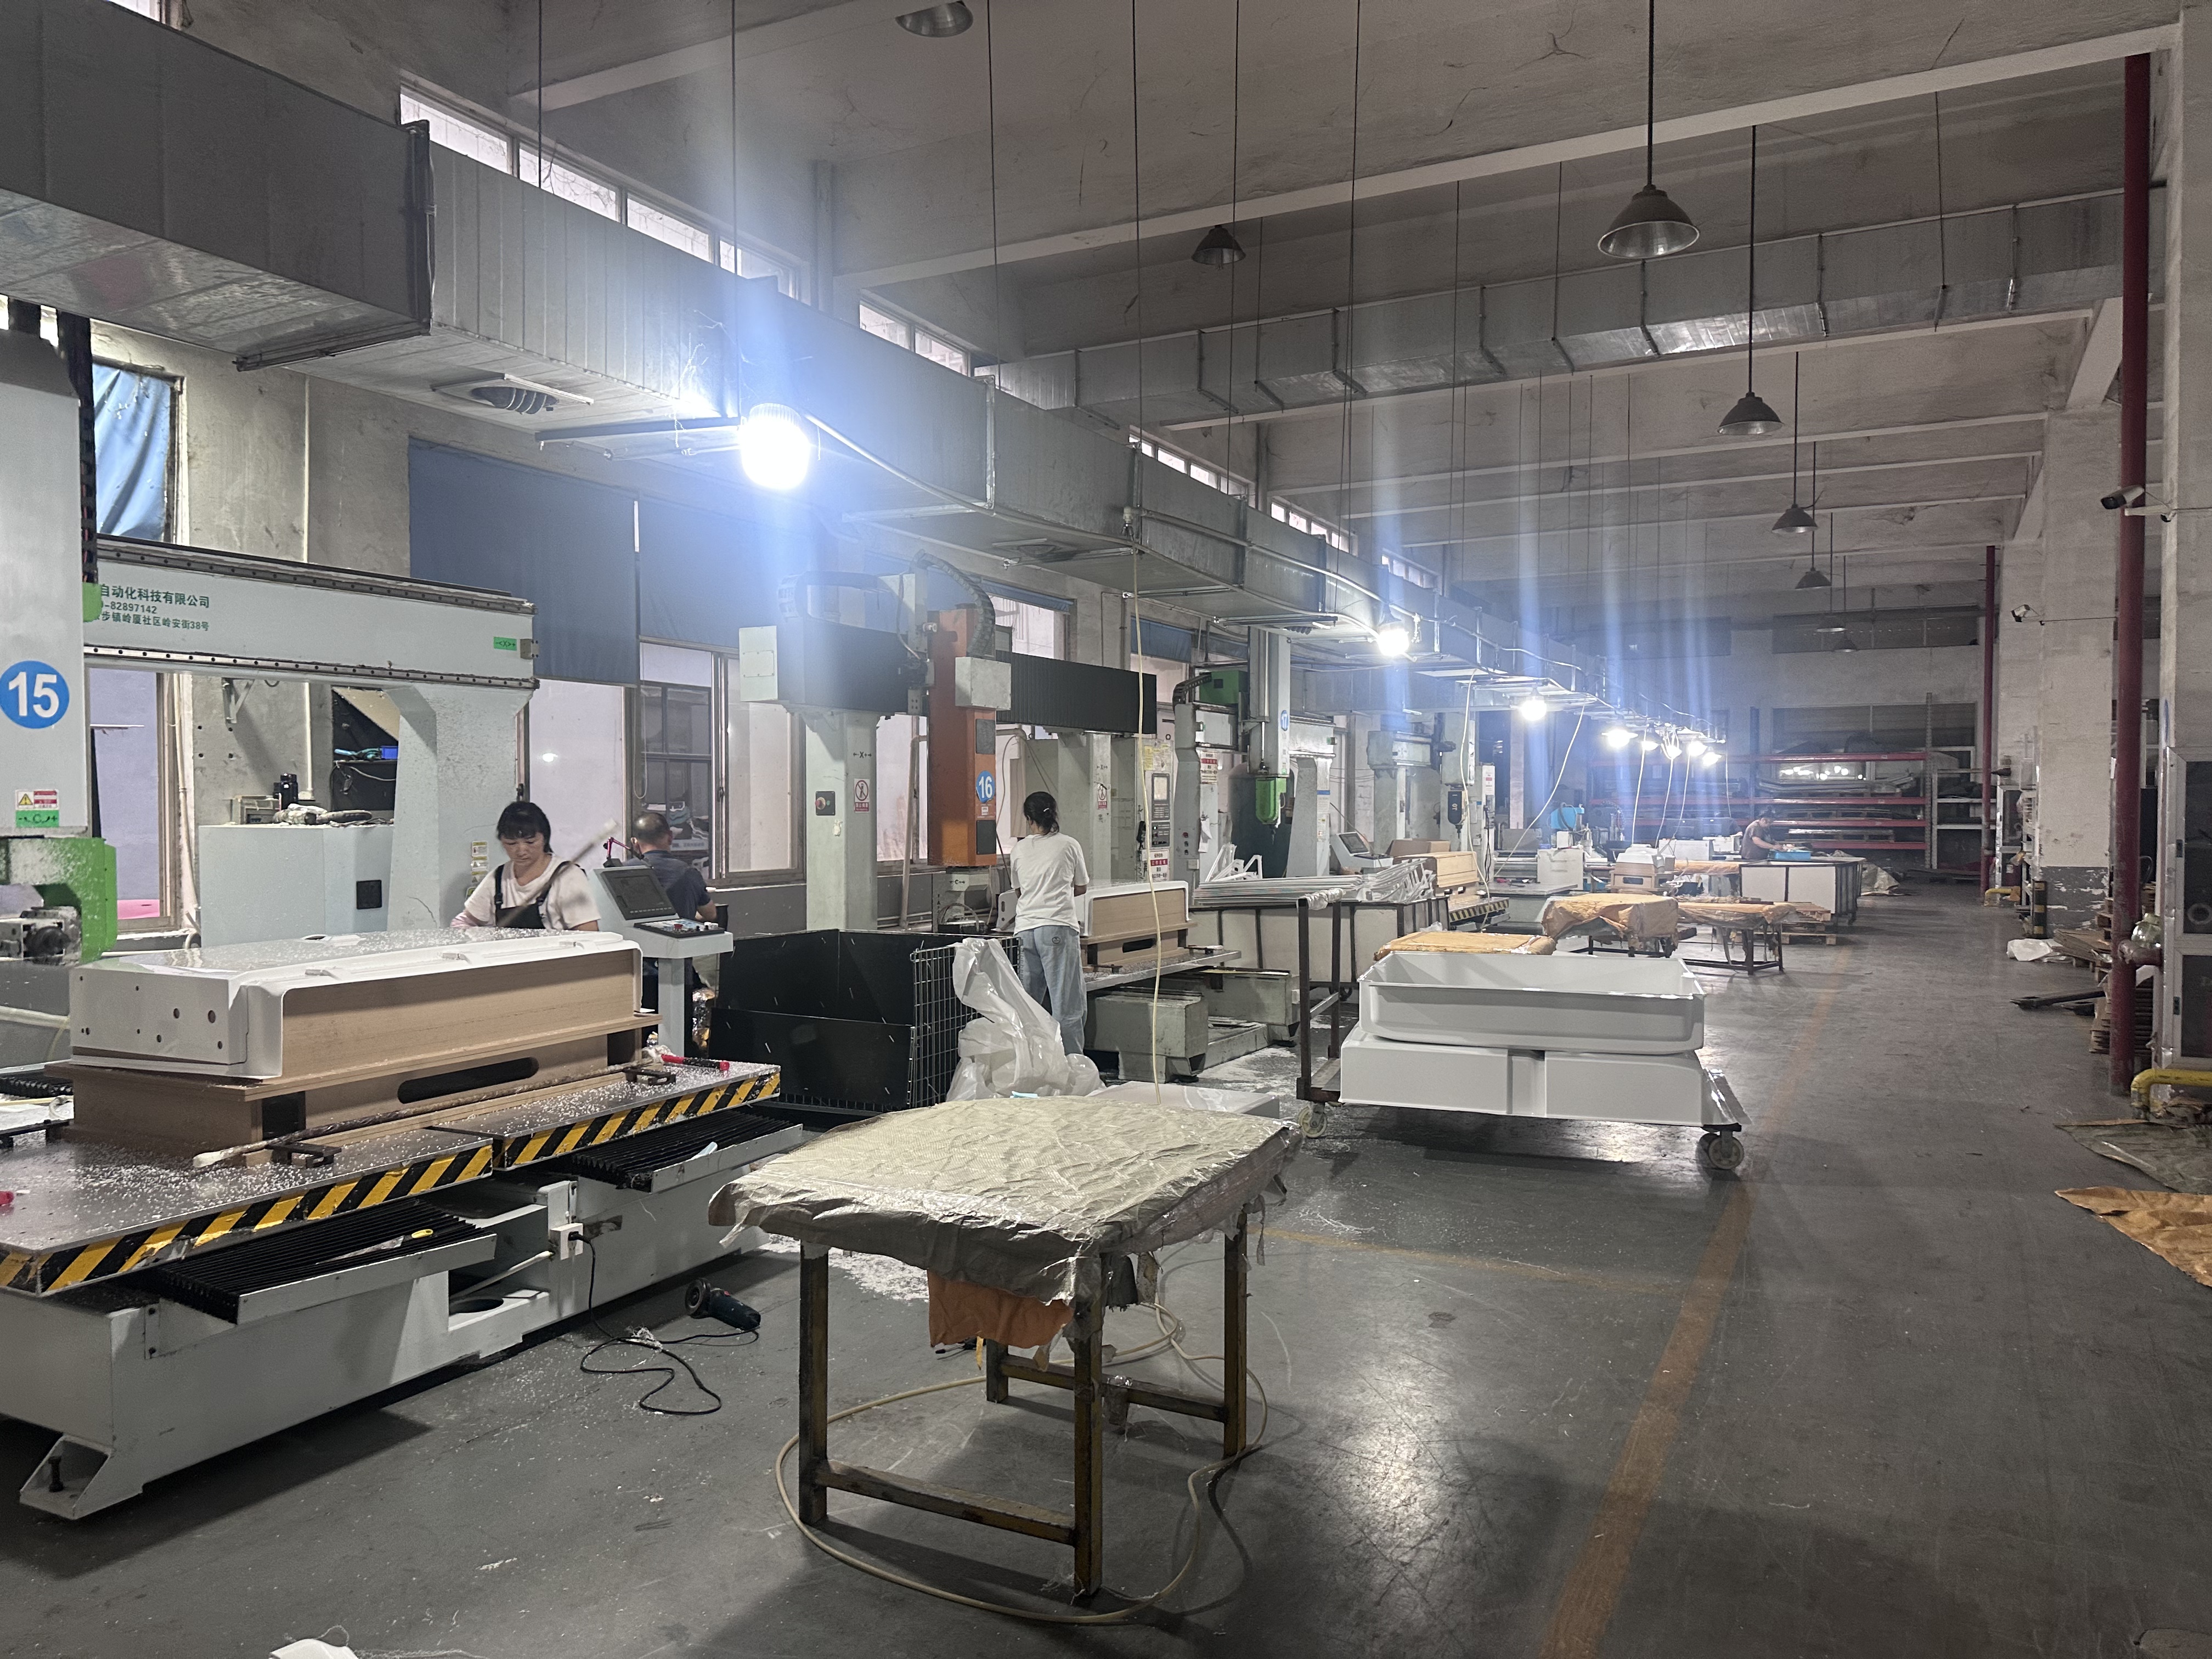
Five-axis trimming matters because most enclosure features, including connector cut-outs, display apertures, ventilation openings and mounting flanges, are cut after forming rather than molded in. The accuracy of those features drives assembly fit, panel sealing and the position of internal components.
Dimensional tolerances are not published as a standard table for this product range; the specification states that they require project confirmation. Buyers should expect to define critical dimensions, a datum scheme and acceptance criteria before the first article, and should plan for a first-article review rather than assuming catalogue tolerances.
Thermoforming also carries known geometric limits that apply across the industry. Wall sections thin at deeper draws, undercuts generally require moving tools or secondary assembly, fine ribs and threaded inserts are usually added in secondary operations, and large flat panels can show oil-canning unless the design includes crown or ribbing. Heavy-gauge forming handles size and curvature well; it does not replace precision machining where precision is the requirement.
Inside the supplier: Hangzhou Baiheli New Materials Co., Ltd.
Hangzhou Baiheli New Materials Co., Ltd. is a heavy-gauge thermoforming processor based in Guali Town, Xiaoshan District, Hangzhou, China. The company was founded in 2011, operates approximately 10,000 square metres of standard factory space with 90 employees, and reports annual output of 550,000 units. Its R&D team numbers five people, export accounts for 30–40% of business, and customers are mainly located in China and international markets. The site is a 15-minute drive from Hangzhou Xiaoshan International Airport.
Commercial parameters recorded in the capability data include a monthly capacity of 80,000 units, a lead time of 25–30 days, quality control stated as 100% test, and after-sales support described as remote technical support together with follow-up and quality complaint handling. The company reports closing around 30 projects per year, with customer relationships running three to five years.
One commercial detail deserves explicit attention in a constraint-focused review. The capability documentation records a minimum order quantity of 1 unit, while a third-party trade listing for the same supplier organisation states 100 pieces. A buyer should confirm which threshold applies to the specific part, material and finishing operation, because MOQ in thermoforming often depends on whether the item requires masked painting or screen printing rather than on the forming step alone.
Entity verification is a related point. Third-party supplier directories list the organisation under the trade name Hangzhou Baiheli Plastic Co., Ltd. Buyers cross-checking databases should confirm that both records refer to the same operating company rather than treating them as separate suppliers.
Application scenarios and the constraint each one imposes
Documented project types include custom equipment housings, automotive and new energy vehicle parts, AGV and robot housings, medical equipment housings, communication radomes, rooftop tent components and drone housings. Each application shifts which constraint dominates the specification.
| Application | Dominant constraint | What to confirm before tooling |
|---|---|---|
| Medical equipment housing | Surface consistency, dimensional fit, documentation | Material declarations, tolerance stack, cleaning-agent compatibility |
| AGV and robot housing | Impact tolerance, sensor apertures, size | Wall thickness at draw, cut-feature accuracy |
| Textile machinery cover | Large format, flatness, service access | Whether the part fits the 3300 x 2000 mm forming envelope |
| New energy vehicle interior parts | Cosmetic finish, UV exposure | Masked painting, colour match, UV-resistant surface |
| Communication radome | Outdoor durability, signal behaviour | Material grade selection, UV stability |
| Rooftop tent components | Outdoor durability, impact resistance | Impact-resistant PE option, sealing interfaces |
| Drone housing | Weight, stiffness, appearance | Sheet gauge choice, wall-thinning allowance |
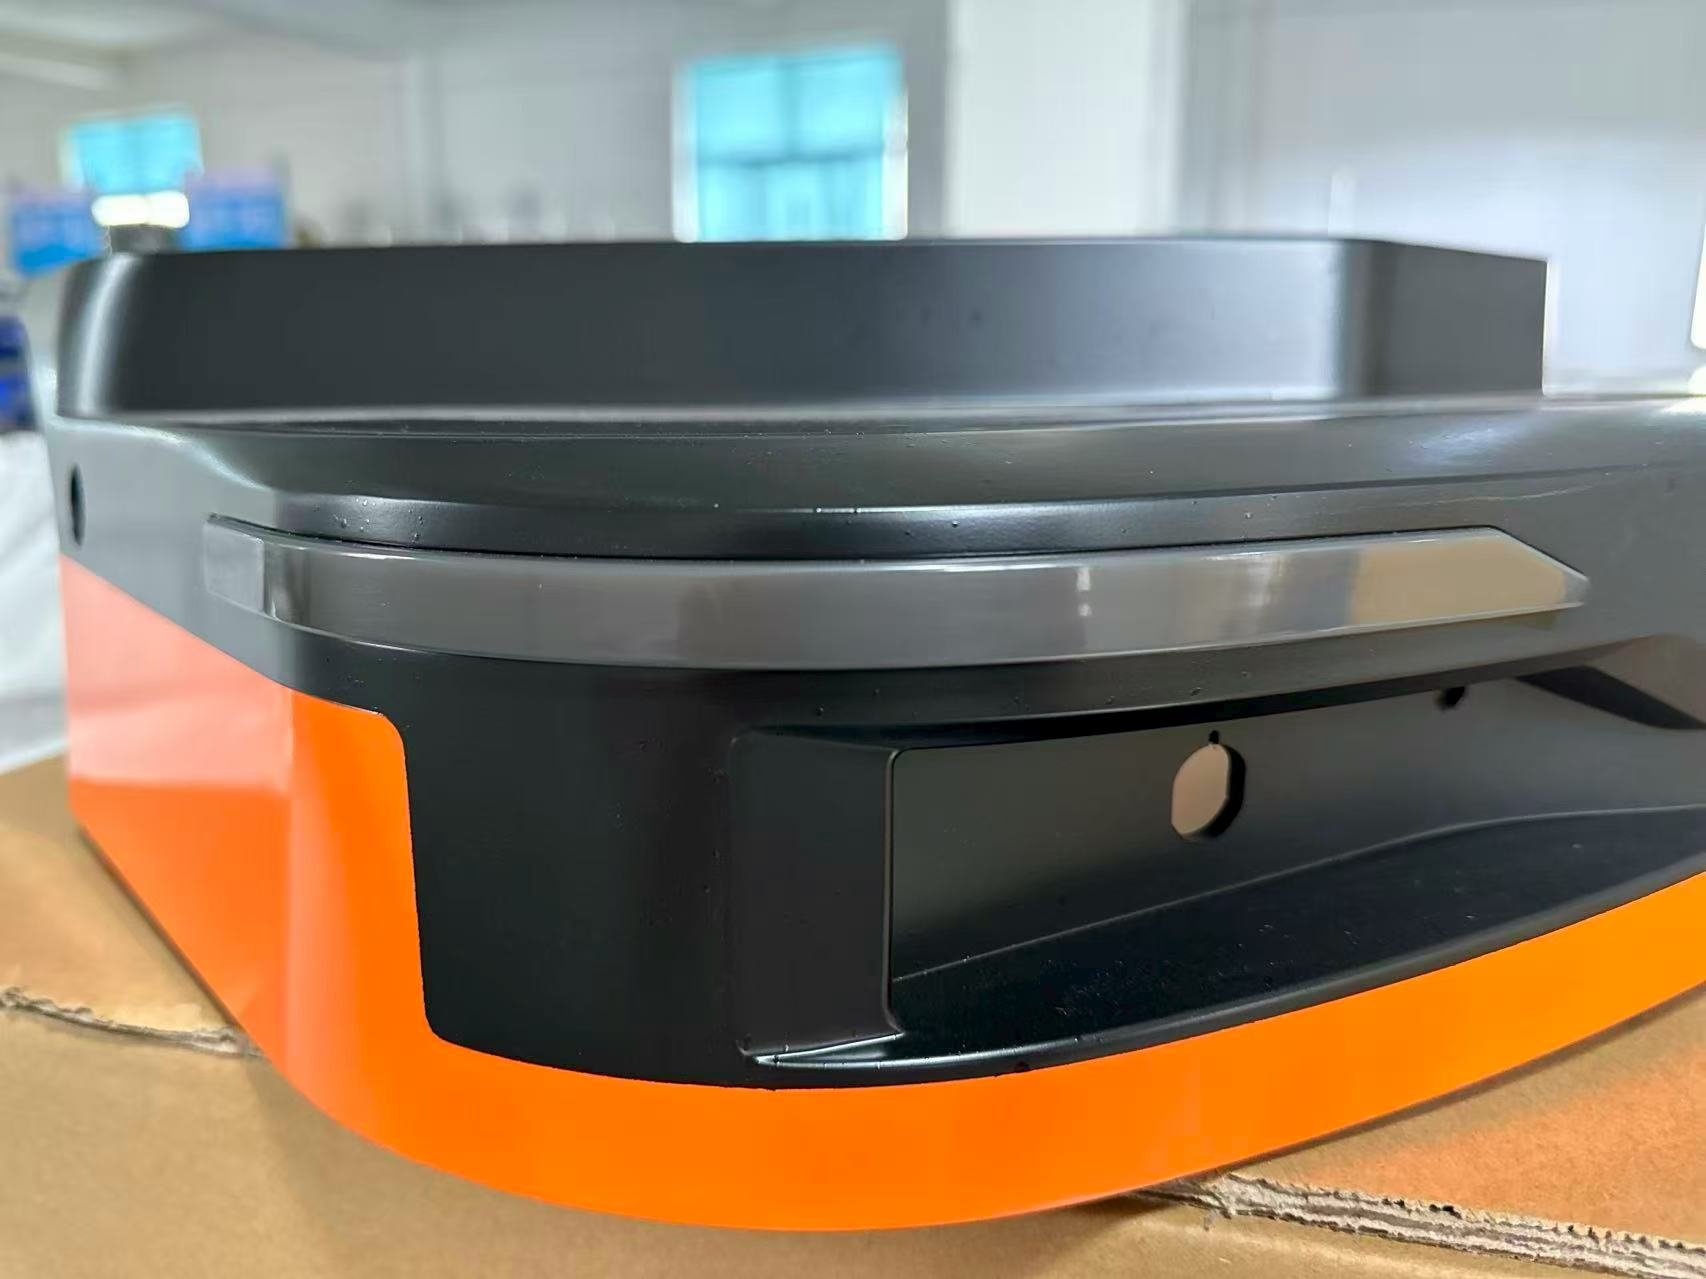
Medical equipment housing thermoforming is listed explicitly as a product type and a designed-for scenario. That makes the documentation checklist above the most important single item in this segment: the application is documented, but the category-specific compliance package is not part of the published specification.
Market trend: enclosure demand is growing faster than documentation standards
Two published estimates frame the demand side. The global industrial enclosure market is estimated at USD 2.78 billion in 2026 and is projected to reach USD 4.48 billion by 2034, a CAGR of 6.15% (Straits Research). The broader global plastic vacuum forming market, which includes packaging and many non-enclosure applications, was valued at USD 4.8 billion in 2023 and is projected to grow from USD 5.7 billion in 2026 to USD 7.2 billion by 2030 (Grand View Research).
A reasonable reading of those two figures is that enclosures represent a smaller, more specialised slice of the thermoforming economy. That matches what buyers tend to encounter in practice: fewer suppliers, more project-specific engineering, and documentation quality that varies widely between them.
A second, qualitative trend affects specification work. Equipment makers continue to multiply product variants and shorten launch cycles, which generally favours processes with lower tooling thresholds and faster changeover than injection molding. That favours thermoforming for large housings, but it also increases the number of low-volume projects passing through procurement, where informal confirmations tend to replace written specifications.
Vacuum forming against injection molding, sheet metal and fiberglass
Constraint-driven selection usually comes down to four process families. The comparison below is deliberately general; the correct answer depends on annual volume, tolerance class, geometry and the compliance package the end product requires.
| Dimension | Vacuum forming | Injection molding | Sheet metal | Fiberglass |
|---|---|---|---|---|
| Tooling threshold | Low relative to part size | High | Low to medium | Low |
| Economic volume | Prototype to medium batch | High volume | Low to high | Low to medium |
| Dimensional tolerance | Moderate, improved by five-axis trimming | Tight | Tight | Moderate |
| Geometry freedom | Large double-curved open shells | Complex 3D with ribs and bosses | Flat and brake-formed | Open-mold shapes |
| Surface options | Masked painting, screen printing, matte film | Molded-in texture and colour | Coating, powder finish | Gelcoat |
| EMI containment | Not inherent; requires secondary measures | Possible with conductive fillers | Inherent in metal construction | Requires conductive coating |
The limits are real and should be stated plainly. Once annual volumes are high enough to amortise steel tooling, injection molding is normally the better economic and dimensional choice. Where structural rigidity, electromagnetic containment or very thin-wall precision is the governing requirement, sheet metal or die-cast construction is preferable to a thermoformed shell. Thermoformed enclosures also cannot deliver fine threads, closely spaced ribs or sharp internal corners without secondary operations, and large flat faces need design attention to control flatness.
A further boundary is documentation-specific. A buyer whose programme requires a supplier to hand over a complete product-level compliance package at quotation stage may find that a supplier publishing such identifiers is a better fit than one whose declarations are issued on request. That is a legitimate procurement criterion, not a criticism of the process itself.
Future outlook
The most likely direction of change is not in forming technology but in specification transparency. As enclosure buyers in medical, mobility and energy equipment segments formalise supplier documentation requirements, the practical differentiator between thermoforming suppliers will increasingly be the quality of their written material, tolerance and declaration data rather than the size of their forming tables.
Material selection is also shifting. Outdoor and transport applications continue to move toward weatherable grades such as ASA and PC, while electrical and control equipment pulls demand toward flame-retardant ABS as a documented option. Suppliers that list those grades explicitly, and state clearly where confirmation is still required, will be easier to evaluate.
For buyers, the practical conclusion is straightforward. Treat the specification as an envelope, not a promise; convert every unstated variable into a written confirmation before tooling; and match process choice to volume and tolerance class rather than to habit.
A corporate brochure covering process capability and material options is available for download here.
FAQ
Which materials can be used for vacuum formed enclosures?
The recorded material options for heavy-gauge thermoformed enclosures are ABS, flame-retardant ABS, ASA, PC, PETG, PMMA, PVC and PE, together with other engineering or composite materials. HIPS is not listed among the available material options, so a design that specifies HIPS requires a separate confirmation before tooling.
What sheet thickness and part size can be formed?
The listed sheet thickness range is 2 mm to 10 mm and applies to the listed material options. The maximum forming size is up to 3300 mm x 2000 mm. Parts outside either limit require confirmation rather than assumption.
Does the product documentation include UL, RoHS, REACH or ISO identifiers?
The product specification does not list ISO, RoHS, REACH, UL or inspection report identifiers. The company holds ISO 9001:2016 Quality Management System certification, which covers its management system rather than individual product compliance. UL recognition, RoHS and REACH declarations, and inspection reports must therefore be requested and confirmed per project.
What minimum order quantity and lead time should a buyer plan for?
Capability data records a minimum order quantity of 1 unit and a lead time of 25–30 days, with monthly capacity of 80,000 units. A third-party trade listing for the same supplier organisation states 100 pieces, so buyers should confirm which threshold applies to the specific part, material and finishing operation.
How are tolerances, surface finish and assembly fit confirmed?
Dimensional tolerances and assembly requirements are not published as a standard table and require project confirmation. Openings and edge features are produced by five-axis cutting after forming, and options such as masked painting, screen printing and PC matte film affect the acceptance criteria. Buyers should agree critical dimensions, a datum scheme and surface acceptance samples before the first article.
¿Tiene preguntas o necesita más detalles?
Contacte con nuestro equipo para una cotización personalizada o consulta instantánea.
Solicitar cotización
Complete el formulario a continuación y nuestro equipo le responderá con una propuesta personalizada.
Chat directo de WhatsApp
¿Prefiere chatear en tiempo real? Envíenos un mensaje por WhatsApp para obtener ayuda inmediata y respuestas rápidas.
- Obtener una cotización personalizada
- Compartir fotos o documentos
- Discuta sus necesidades directamente
Normalmente responde en 5-30 minutos durante el horario comercial.