
Trigger Sprayer Trade-offs: Thread Fit, Spray Pattern and PP Recycling
The global trigger sprayer market was valued at about USD 491.8 million in 2025, and Fortune Business Insights projects a 4.7% CAGR from 2026 to 2034 for the closure category. For a buyer preparing a packaging run, that growth figure is background noise compared with four decisions that actually determine whether the project ships on time: the neck thread and finish depth, the spray output style, the material and recycling profile, and the supplier's ability to hold all three constant across repeat orders.
Where the decision really turns
Trigger sprayers are often quoted as a single line item, but they behave like a small assembly with several interfaces. One interface is mechanical: the bottle neck. One is functional: the way the liquid leaves the nozzle. One is regulatory: what the unit is made of and how it behaves at end of life. One is commercial: whether the same specification can be re-ordered in a different colour, in bulk, without a redesign.
Buyers who treat the sprayer as a commodity bought last in the project usually pay for it later. Buyers who sequence the four checks below tend to avoid the two expensive failure modes: a closure that leaks after filling, and a packaging format that has to be re-qualified because a sustainability claim could not be evidenced.
| Decision | What must be confirmed | Typical failure if skipped | How to verify |
|---|---|---|---|
| Neck fit | Thread designation and finish depth of the actual bottle | Leakage, cross-threading, loose seating | Bottle drawings plus filled and inverted tests on production samples |
| Spray output | Mist or foam, matched to the formula and the end use | Poor coverage or collapse of foam performance | Bench trials with the real liquid, not water |
| Material | All-plastic PP mono-material, and which recycled content claims are supportable | Unsupported recyclability messaging; design-for-recycling gaps | Material declarations and supplier documentation |
| Supply | OEM colour scope, tooling ownership, bulk capacity | Colour drift, re-tooling delays, allocation risk | Factory audit, sample runs, capacity disclosure |
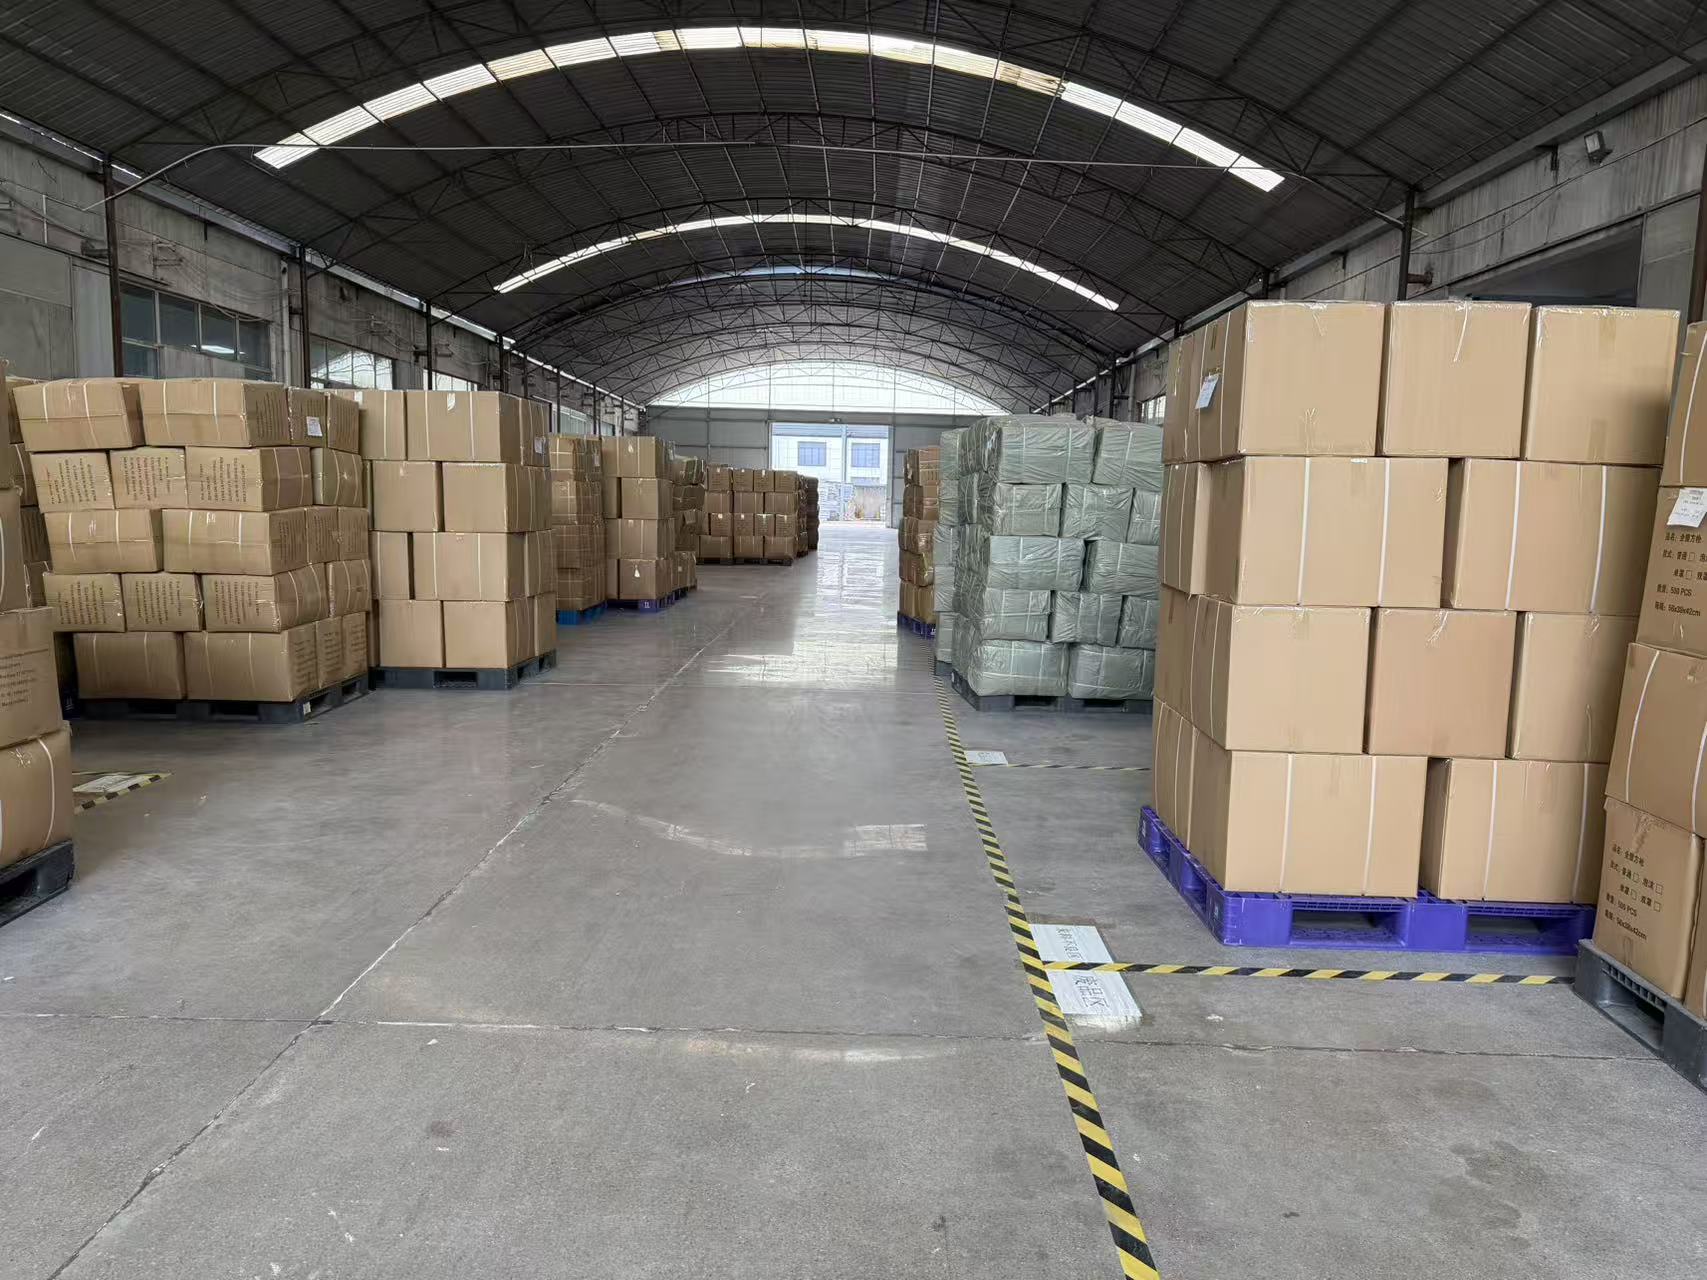
Bulk trigger sprayer stock in an internal warehouse: supply continuity is a specification, not a promise.
1. Neck fit: 28/400 versus 28/410
The 28/410 neck size is identified as the most commonly used opening for trigger sprayers, which makes it the default reference point in most buyer conversations. The 28/400 finish sits in the same 28 mm neck family, but the finish depth differs, so the two are not interchangeable purely because the thread diameter matches. The 400 and 410 suffixes describe different finish depths, and that difference changes how far the sprayer body sits down on the bottle.
What the difference means in practice
A shorter finish and a deeper finish position the closure differently against the bottle shoulder. When a sprayer designed for one finish is fitted to the other, the thread may engage, but the sealing geometry, the visible collar height and the force needed to seat the unit can all shift. Under load, at the filling line or in an inverted carton, that shift is what shows up as seepage.
| Item | 28/400 | 28/410 |
|---|---|---|
| Position in the 28 mm neck family | Standard option, shallower finish | Standard option, deeper finish |
| Market usage | Used on bottles built around this finish | Identified as the most commonly used opening for trigger sprayers |
| Main risk if mismatched | Unit sits high or seats poorly on a deeper bottle | Collar interference or incorrect sealing on a shallow bottle |
| Buyer rule | Specify only when the bottle finish is fixed | Safest default when the bottle is still being designed |
The practical rule for a decision-stage buyer is simple. If the bottle already exists, take the mould drawing and confirm the finish before quoting; do not infer it from a photograph. If the bottle is still open, choose the neck, then the sprayer, then the artwork, in that order. The 28/410 opening's wider use makes it the lower-risk starting point when nothing has yet been frozen.
2. Spray output: fine mist versus foam
Spray output is a functional decision that is often made on aesthetics and then regretted in production. A fine mist trigger sprayer is built to spread a thin, wide film over a surface. A foaming trigger sprayer is built to deliver a compact deposit that stays where it lands. Both are single components in the bill of materials, but they change how the product is used, how much liquid is consumed per application, and how the formula must be written.
Where the difference bites
- Coverage versus dwell time. Mist favours coverage on large, vertical or irregular surfaces. Foam favours contact time on a targeted area.
- Formula dependence. Foam output depends on how the liquid behaves when air is introduced; a formula that performs in a mist unit is not automatically suitable for foam.
- Output consistency. Stable spray output is the variable that matters most across a long filling run, because inconsistent output becomes a customer complaint rather than a line-side issue.
- Non-interchangeability. Mist and foam heads are not drop-in alternatives for one another on the same project; changing output style reopens the trial stage.
On output stability, structural differences are measurable in use. TS-1372 is described as delivering stable spray output and consistent performance relative to conventional trigger sprayers, and as performing better in household cleaning and industrial spraying conditions where stable output is required. That framing is useful to a buyer because it names the condition, not just the benefit.
A workable decision rule: choose mist when the use is surface coverage over area, and choose foam when the use is dwell time on a specific soil or surface. Then test with the real formula. Bench testing with water will confirm that the unit triggers; it will not confirm that the foam holds or that the mist pattern matches the pack's claim.
3. Material and recycling: the case for all-plastic PP mono-material
An all-plastic PP trigger sprayer uses one polymer family across the body, the collar and the internal mechanism rather than mixing PP with a separate metal spring or a second polymer group. From a buyer's perspective the value is not the word 'recyclable' on a data sheet; it is that a mono-material unit removes the separation step that mixed-material closures create in a sorting stream.
The regulatory backdrop makes this a live procurement issue rather than a branding preference. The EU Packaging and Packaging Waste Regulation (PPWR), adopted in April 2024, mandates 30% recycled content in plastic packaging by 2030 under rule reference PPWR (2024/04). A design-for-recycling choice today is therefore a decision about how much re-qualification work sits in front of the brand in 2030.
There is also a trade classification dimension. HS Code 392350 covers stoppers, lids, caps and other closures of plastics, and trigger sprayers fall inside that heading. Buyers in regulated markets should confirm the code with their broker, but the classification matters because duty treatment and documentation expectations follow from it.
4. Chemical resistance: verify, do not assume
Chemical resistance is the dimension where buyers most often accept a verbal assurance. PP is a widely used material for trigger sprayers precisely because it handles a broad set of household and industrial liquids, but 'broad' is not 'unlimited', and the difference shows up at the seal, not at the body.
A structured check is more useful than a compatibility chart with no context:
- Test with the real formula. Concentration, surfactant load and solvent content all influence how a plastic component ages.
- Separate the wetted parts from the body. The body, the gasket area and the internal valve are exposed differently and should be confirmed individually.
- Test under load, not at rest. A filled bottle stored upright is a weaker test than a filled bottle stored inverted or subjected to carton stacking.
- Check sealing behaviour after cycling. Repeated triggering is the condition in which a marginal seal becomes a visible leak.
This is the point at which structural design matters commercially. Compared with conventional trigger sprayers, TS-1372 has an improved structure with better sealing performance and an anti-leakage design, and its technical advantages are stated relative to conventional trigger sprayer constructions. It also requires no extra maintenance compared with conventional trigger sprayers, and it is positioned as providing enhanced durability over conventional designs. None of those points replace a compatibility test, but together they shift the starting assumption: the sealing approach, not the wall thickness, is where the difference sits.
5. Procurement: OEM colour, bulk supply and continuity
MILA Plastic Industry — Zhejiang Mila Plastic Industry Co., Ltd. — is a manufacturer of household care packaging based in Quzhou, Zhejiang, China, producing plastic trigger sprayers together with related pumps and nozzles, and serving export markets across South America, Western Europe, Eastern Europe, East Asia, Southeast Asia, the Middle East, Africa, Oceania and worldwide. The company was founded in 2018, operates a factory of over 30,000 m² with 300–400 employees and 10 engineers, and reports annual output of 600,000,000 pieces with an export ratio of 70%–80%. Third-party company profile data places annual sales in the USD 50M–53M range on that same output base.
Production is supported by 60 injection molding machines, 20 automatic production lines, 4 machining centers, 6 CNC engraving machines, 8 semi-high-speed lathes, 20 wire-cutting machines and 12 precision mold machines, with automatic testing instruments in the quality chain. MILA Plastic holds ISO 9001:2015 and ISO 14001:2015 certifications and SGS compliance, which are the two certificates a buyer should ask to see in date before an order is placed.
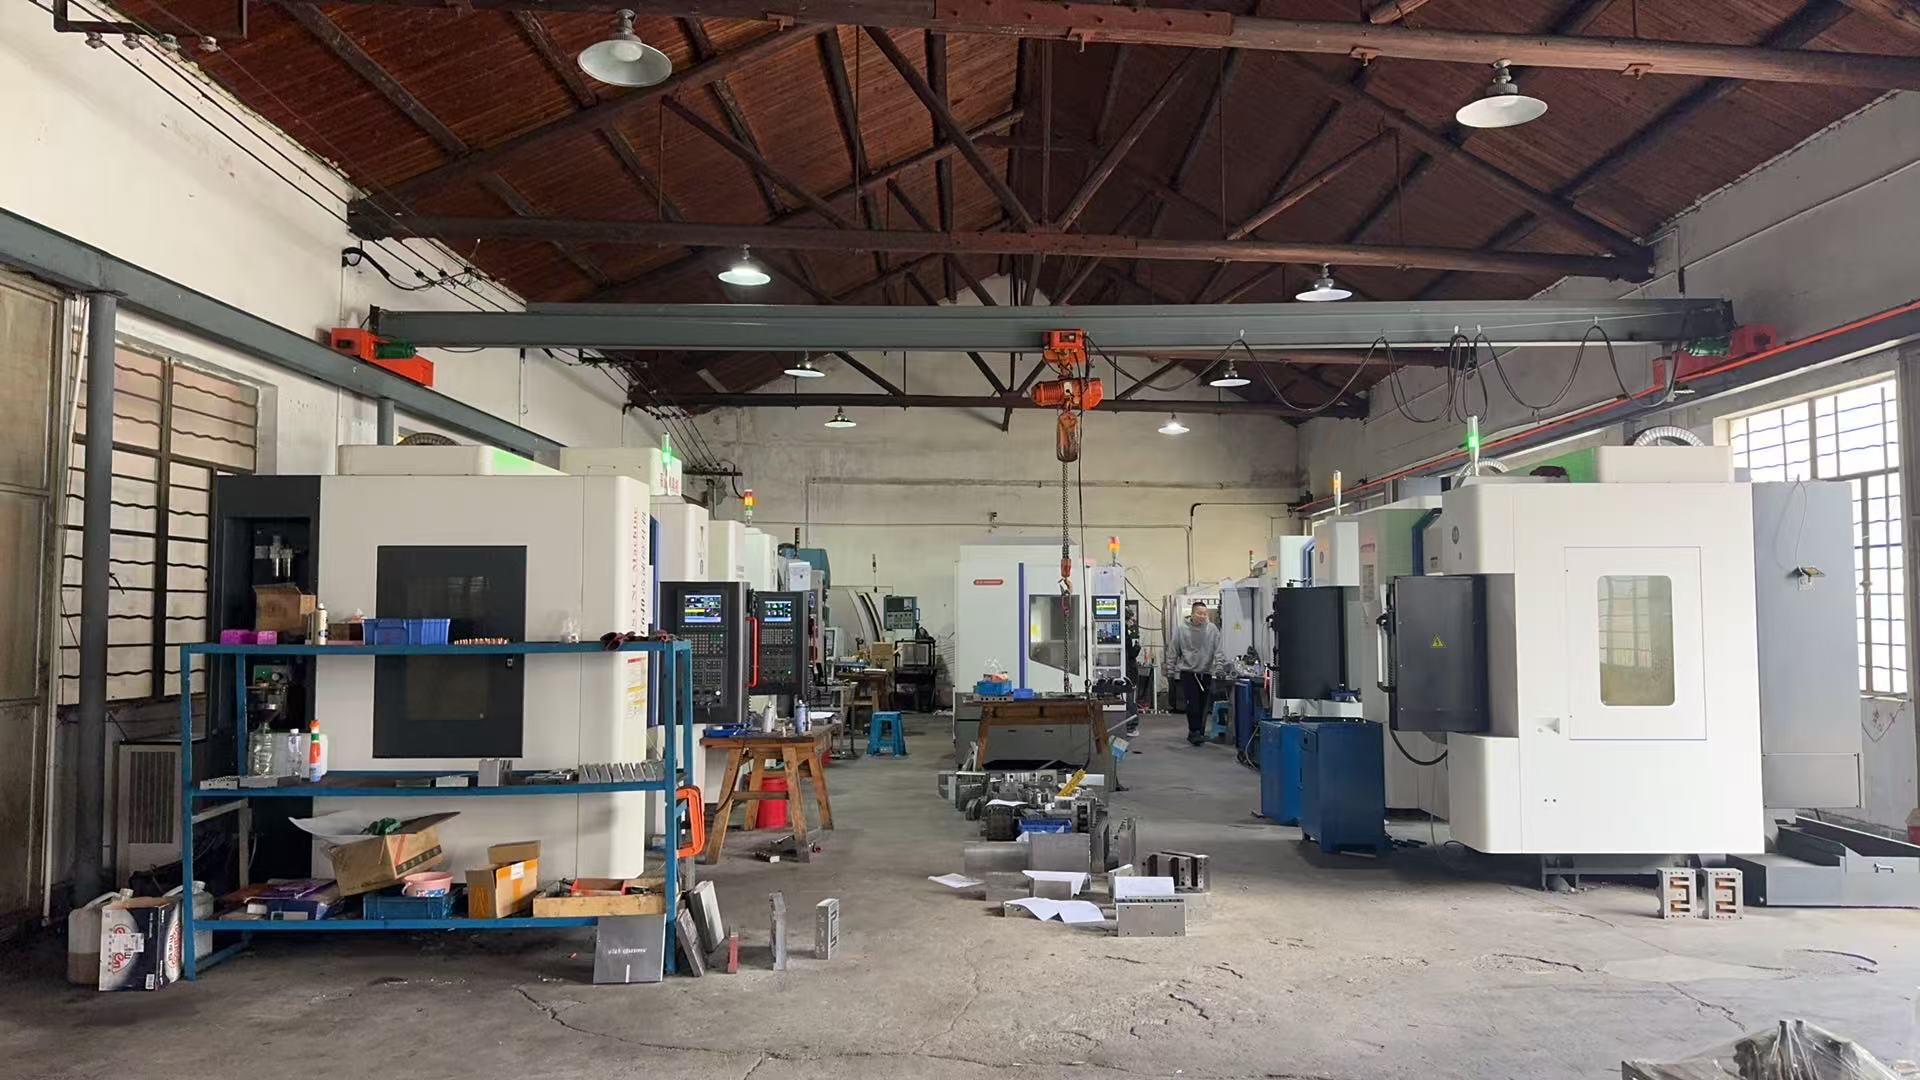
In-house mold making is what turns a custom colour request into a repeatable specification rather than a one-off sample.
What OEM customisation actually requires
Custom trigger sprayer colour is a moulding and colour-matching exercise, not an artwork change. In-house tooling capability matters because colour consistency across repeat orders depends on the same tool, the same resin batch discipline and the same process settings. Buyers should treat colour as a specification with a tolerance, and should confirm how the colour is verified — visually against a master, or instrumentally.
Bulk supply has a similar logic. A capacity figure of 600 million pieces per year describes the plant, not the allocation a new buyer will receive. The useful questions are which presses run the specified model, how a repeat order is scheduled against existing programmes, and what happens if the neck specification changes mid-programme. Buyers should also confirm which party owns the mould in a fully custom project, because tooling ownership determines who can re-order later.
6. Comparison with conventional solutions, and where the limits sit
Set against conventional trigger sprayers, the improved-structure position is a fair comparison on four dimensions: sealing performance, leakage control through the anti-leakage design, durability, and maintenance load, where no extra maintenance is required relative to conventional units. Cost is also cited as competitive on production cost compared with conventional trigger sprayer alternatives, which matters in wholesale and bulk programmes where a small per-unit difference compounds across a container.
The honest limit is this: those advantages are relative, not absolute. An improved seal still depends on the correct neck fit, so a 28/400 unit on a bottle finished to a deeper specification will not deliver the benefit the design intends. Material recyclability is also a design property, not a compliance certificate — meeting the PPWR recycled content direction by 2030 requires documented feedstock, and a mono-material construction alone does not supply it. Finally, PP is not a universal barrier: aggressive solvent-based formulations may still require a compatibility test that ends in a different material decision. A buyer who hears all three limits stated openly can usually trust the rest of the specification more, not less.
7. Market trend analysis
Three signals are worth carrying into a sourcing plan. First, the category is growing steadily rather than explosively — a USD 491.8 million base in 2025 with a 4.7% CAGR to 2034 — which means competitive pressure comes from specification and service, not from volume expansion alone. Second, third-party estimates of the same market diverge widely, largely because the scope differs: some figures include the complete trigger sprayer bottle rather than the closure alone. Buyers comparing supplier presentations should check which scope is being quoted before treating two numbers as comparable.
Third, regulation is moving ahead of material innovation in Europe. The 30% recycled content requirement by 2030 under PPWR (2024/04) pushes brands toward mono-material designs that can be evidenced, and pushes suppliers toward documented feedstock rather than generic recyclability statements. For a buyer in the Decision stage, that is a specification question that belongs in the RFQ now, not in a 2030 review.
8. Future outlook
The next few years are likely to separate suppliers on documentation rather than on catalogue breadth. Neck fit and spray performance are already well understood by most buyers; what is less settled is the evidence trail behind material claims, colour consistency across repeat orders, and the ability to hold a specification constant while a formula or a bottle changes underneath it. Suppliers with in-house tooling, in-house compounding discipline and current ISO certification are structurally better placed to answer those questions than suppliers assembling from third-party parts.
For buyers, the practical implication is to build the decision record early: neck designation, finish depth, output style, material, colour tolerance and evidence of certification. A trigger sprayer specification that can be quoted in one page is also a specification that can be re-ordered in three years.
Frequently asked questions
Can a 28/400 trigger sprayer be used on a 28/410 bottle?
Not as a like-for-like substitution. Both sit in the 28 mm neck family, but the 400 and 410 suffixes describe different finish depths, so the sprayer seats differently against the bottle shoulder. The thread may engage while the sealing geometry, collar height and seating force change. The safe sequence is to confirm the bottle finish from the mould drawing and then specify the matching sprayer, rather than assuming compatibility from the thread diameter alone.
Which neck size is the safer default when the bottle has not been designed yet?
28/410 is identified as the most commonly used opening for trigger sprayers, which makes it the lower-risk starting point when nothing has been frozen. Choosing the neck first, then the sprayer, then the artwork keeps the decision sequence aligned with how the components actually fit together.
How should a buyer choose between a fine mist and a foaming trigger sprayer?
The choice follows the application, not the appearance. Fine mist suits coverage across a surface area, while foam suits dwell time on a targeted area. Foam output also depends on how the specific formula behaves when air is introduced, so a mist-compatible formula is not automatically suitable for foam. Whichever style is selected, the trial should run with the real liquid rather than water.
Does an all-plastic PP mono-material trigger sprayer automatically satisfy recycling requirements?
No. A mono-material PP construction supports design-for-recycling because it avoids mixing polymer groups in one closure, which simplifies sorting. It does not by itself demonstrate recycled content. The EU PPWR, adopted in April 2024 under reference PPWR (2024/04), requires 30% recycled content in plastic packaging by 2030, and that figure depends on documented feedstock for the specific part.
What evidence should be requested to support chemical resistance claims?
Ask for compatibility testing with the actual formulation rather than a general material statement, and ask which wetted parts were tested, since the body, the gasket area and the internal valve are exposed differently. Testing should include a filled and inverted condition and repeated triggering, because a marginal seal typically becomes visible only after cycling. Statements such as improved sealing performance and an anti-leakage design relative to conventional trigger sprayer constructions describe the design intent; they do not replace a formulation-specific test.
What does OEM customisation involve beyond choosing a colour?
Custom colour is a moulding and colour-matching exercise that depends on the tool, the resin batch and the process settings staying consistent across repeat orders, which is why in-house mold making capability is relevant. Buyers should define colour as a specification with a tolerance, confirm how colour is verified, and establish mould ownership in a fully custom project so that re-ordering later does not require a new tool. Bulk capacity figures describe plant capability, not the allocation a specific programme will receive.
Closing note
A trigger sprayer decision is settled by four confirmations: the bottle finish, the output style matched to the formula, the material and recycling evidence, and a supplier whose tooling and certification support a repeat order. Buyers who document those four points before the first PO tend to spend their second meeting on volume, not on leaks.
¿Tiene preguntas o necesita más detalles?
Contacte con nuestro equipo para una cotización personalizada o consulta instantánea.
Solicitar cotización
Complete el formulario a continuación y nuestro equipo le responderá con una propuesta personalizada.
Chat directo de WhatsApp
¿Prefiere chatear en tiempo real? Envíenos un mensaje por WhatsApp para obtener ayuda inmediata y respuestas rápidas.
- Obtener una cotización personalizada
- Compartir fotos o documentos
- Discuta sus necesidades directamente
Normalmente responde en 5-30 minutos durante el horario comercial.