
Trigger Sprayer Buyer Decision Framework: Neck Fit, Spray Type, Recycling
Most trigger sprayer sourcing problems are not manufacturing defects. They are sequencing errors. Buyers routinely compare price, spray pattern and lead time before confirming the one parameter that cannot be corrected once bottles are filled: whether the closure actually matches the bottle neck it will be assembled onto. In trigger sprayer procurement, neck fit is a binary condition, while spray performance is a graded one. The binary condition has to be settled first, because a trigger sprayer that does not seat correctly cannot be rescued by better atomisation, a lower unit price, or a faster delivery schedule.
This article sets out a sequential buyer decision framework for trigger sprayers: (1) neck finish fit, (2) spray output type, (3) material and recyclability, (4) formulation and actuation conditions, (5) commercial and OEM terms, and (6) acceptance criteria and risk. It applies to plastic trigger sprayers used in household cleaning, commercial cleaning, auto care, pet supplies, garden care and chemical packaging — the same sprayer category, evaluated in a different order than most buyers use.
The category carries enough volume for specification decisions to have commercial weight. Fortune Business Insights values the global trigger sprayers market at USD 491.8 million in 2025 and projects a compound annual growth rate of 4.7% from 2026 to 2034. Market sizing in this category should be read carefully, however: a second published estimate places the category at approximately USD 2.6 billion, a difference that most likely reflects scope rather than disagreement — the larger figure appears to cover the complete trigger spray bottle assembly rather than the sprayer closure alone. For a buyer, that distinction matters, because it is the closure that is being specified, tested and re-ordered.
Why the decision order determines the outcome
The cost of a fit failure and the cost of a performance compromise are not symmetrical. If a sprayer delivers a slightly wider or narrower pattern than expected, the consequence is usually a formulation or usage adjustment. If a sprayer does not fit the bottle, the consequence is a stopped filling line, a repacking operation, or a leakage claim after shipment. Fit problems also tend to surface late: samples are often tested on a generic bottle, and the mismatch appears only when the production bottle arrives.
The reverse error is equally common. Buyers who start with spray quality invest sample time in a configuration that can never be validated in production, because the thread finish is wrong. Sequencing the evaluation correctly is therefore not a formality; it is the difference between a two-week approval and a two-month recovery.
There is also a regulatory thread running through the decision. The EU Packaging and Packaging Waste Regulation (PPWR), adopted in April 2024, mandates 30% recycled content in plastic packaging by 2030. Recyclability is no longer a secondary attribute discussed after the commercial terms are agreed; for packaging placed on the EU market, it increasingly belongs in the first round of supplier questions.
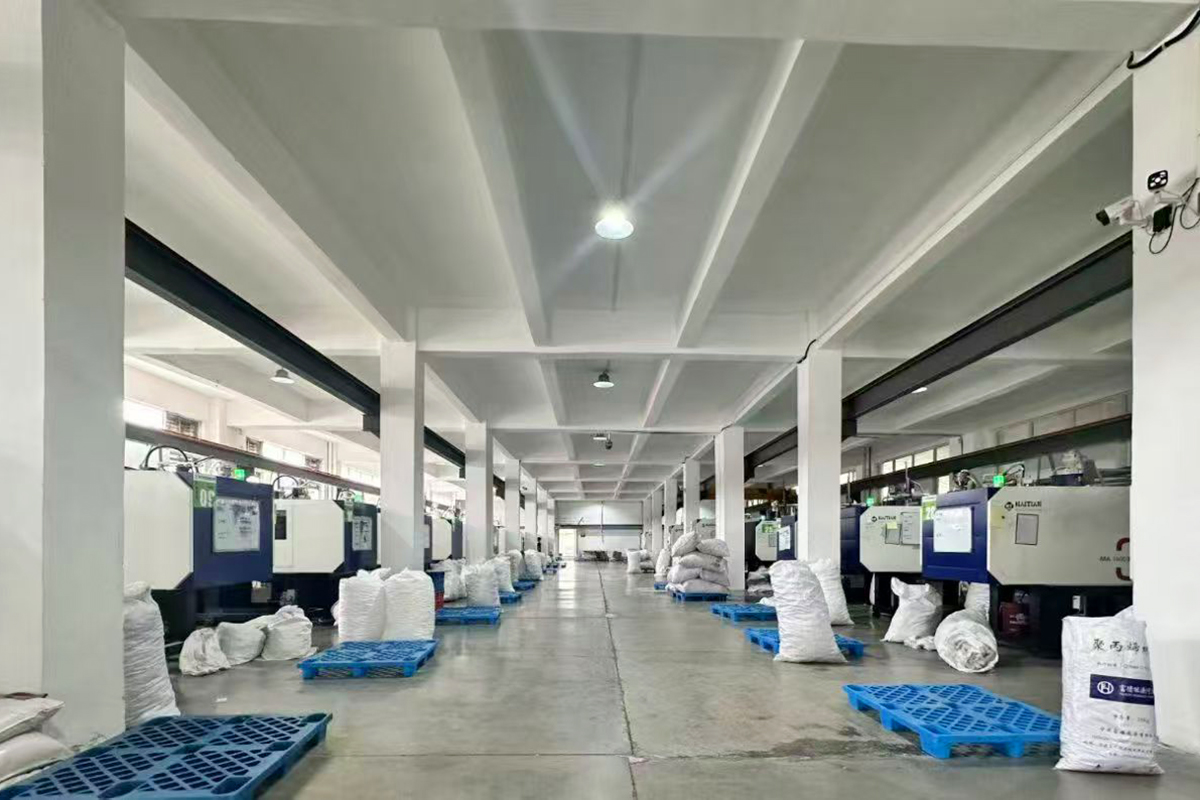
Multiple injection moulding machines running for mass plastic component production — the upstream stage where trigger sprayer geometry is fixed.
Step 1 — Neck fit: 28/400 versus 28/410
What the two numbers actually mean
In the 28/400 and 28/410 designations, the leading figure refers to the nominal neck diameter in millimetres, while the second figure denotes the thread finish specification. The two finishes share the same nominal diameter but differ in thread geometry, which is why a closure engineered for one finish is not automatically correct on the other. The failure is not always dramatic: a mismatched pair may assemble partially, cross-thread under line pressure, or seal well in the sample room and leak after a transport cycle.
Industry reference material identifies 28/410 as the most commonly used opening for trigger sprayers, which makes it a reasonable default assumption in many markets. It remains an assumption until it is checked against the actual bottle. Buyers sourcing across several bottle suppliers frequently discover that "28 mm" is used loosely in internal documentation, and that the finish designation is where the specification actually lives.
Verification sequence before any performance comparison
- Obtain physical bottle samples or a dimensional neck drawing, and record the finish designation rather than only the diameter.
- Confirm thread engagement and seating by assembling the closure on the actual bottle, not on a test fixture.
- Check the sealing surface and gasket condition at the same time as thread engagement — a correct thread with a compromised sealing face still leaks.
- Verify dip tube length against bottle height, including the height at which the bottle will normally be used and stored.
- Run a leak check after assembly, and repeat it after a transport or drop simulation if the product will ship filled.
- Only then move to spray pattern, output and actuation testing.
Because thread geometry is produced by tooling rather than by assembly, dimensional consistency in the mould is a fit variable as much as a quality variable. Zhejiang Mila Plastic Industry Co.,Ltd., a plastic trigger sprayer manufacturer based in Quzhou, Zhejiang, China, operates 12 precision mould machines, 4 machining centres and 6 CNC engraving machines alongside 60 injection moulding machines — upstream capacity that a buyer can verify before releasing a bulk order, although mould capability on its own is not a fit guarantee.
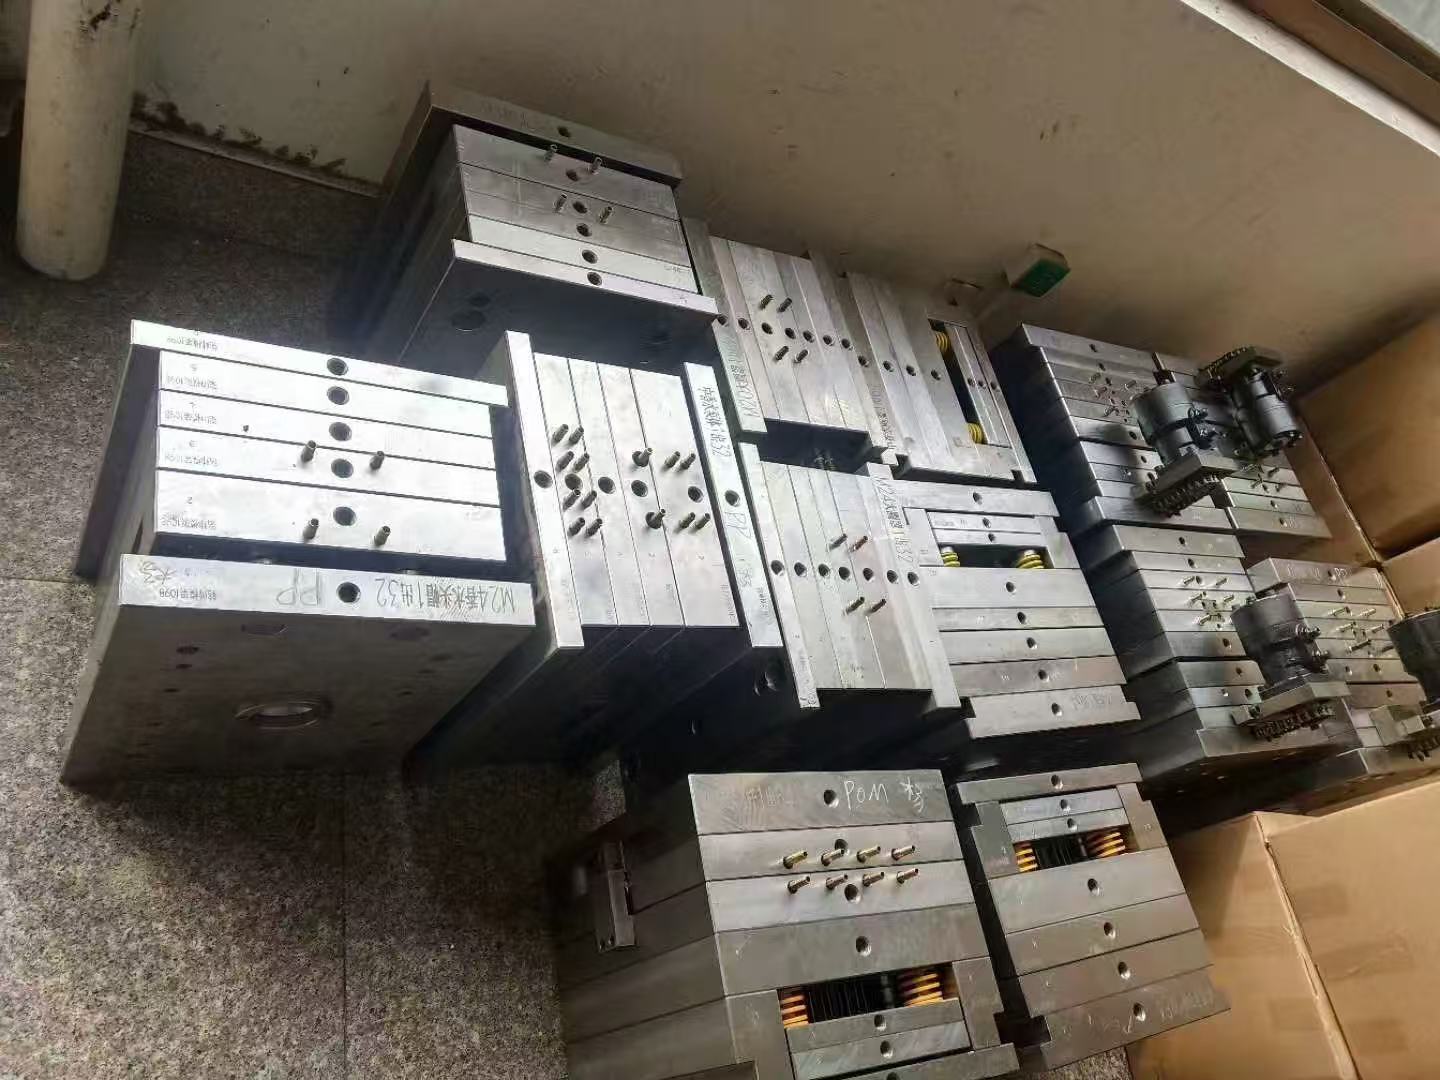
Mould manufacturing and maintenance workshop — neck thread geometry is a tooling-controlled dimension, not an assembly tolerance.
Step 2 — Spray output: fine mist versus foam
Once fit is confirmed, the second decision is the output format. A fine mist trigger sprayer atomises the liquid into small droplets and distributes them over a broad area, which suits large, flat or irregular surfaces where coverage matters more than dwell time. A foaming trigger sprayer aerates the liquid as it passes through the nozzle, producing a foam that clings to vertical surfaces and stays in contact with the surface longer. Neither format is better in absolute terms; they answer different application requirements.
Two variables usually decide the question. The first is whether the product needs to stay where it is applied: foam holds position on walls, tiles, wheels and vertical equipment, while mist is better suited to rapid coverage and to surfaces where residue should be minimal. The second is the intended user. In commercial cleaning, where the same operator may actuate a trigger many times per shift, trigger effort and stroke consistency are practical considerations that are easier to evaluate in sampling than to infer from a specification sheet.
| Application | Output format that typically fits | What to verify before approval |
|---|---|---|
| Household cleaning | Mist for glass, hard surfaces and quick coverage; foam where dwell time on vertical surfaces matters | Pattern width, residue after drying, trigger effort in repeated use |
| Commercial cleaning | Driven by the diluted chemical and the cleaning routine rather than by consumer preference | Chemical compatibility, actuation durability, refill and dilution practice |
| Auto care | Mist for broad surface application; foam where the product must cling to wheels, tyres or vertical panels | Compatibility with the concentrate, output consistency, seal integrity |
| Pet supplies | Typically mist, where even distribution and low residue matter | Formulation compatibility, behaviour of the selected materials in use |
| Chemical packaging | Determined by formulation chemistry first, then by required contact behaviour | Material compatibility, sealing performance, labelling and transport conditions |
| Garden and foliar use | Typically mist, for even distribution across leaf surfaces | Output consistency, drip behaviour, compatibility with the diluted product |
It is worth separating product families at this stage. The sealing approach, the internal geometry and the nozzle design differ between a trigger sprayer and a pump-based foamer, so a buyer specifying both formats should not assume that one approval covers the other. MILA Plastic Industry manufactures plastic trigger sprayers alongside related dispensers including foam pumps, so both lines of enquiry can be handled by one supplier — but the technical validation still has to be carried out format by format.
Step 3 — Material and recycling: what PP mono-material construction changes
All-plastic trigger sprayers are specified as plastic throughout, rather than as a mixed plastic-and-metal assembly. When that construction is also mono-material — the same polymer family across the body, trigger, nozzle and internal parts, typically PP — the closure can stay inside a single rigid plastic stream at end of life instead of requiring separation before sorting. That is the practical difference between a mono-material design and a conventional mixed construction, and it becomes a procurement criterion wherever extended producer responsibility or recycled-content rules apply.
The clearest regulatory signal currently is the EU PPWR, adopted in April 2024, which requires 30% recycled content in plastic packaging by 2030. For buyers supplying the EU market, three questions follow directly from that requirement: what polymer the sprayer is made from, whether the construction is genuinely mono-material, and what documentation the supplier can provide on material composition.
PP-based trigger sprayers are well positioned against that direction, because PP is already a widely collected and reprocessed polymer. The limitation is one of scope. The PPWR recycled-content requirement applies to packaging placed on the EU market, with a 2030 deadline; buyers in other regions work within different frameworks and different timelines. Mono-material design improves the recyclability potential of the closure, but it does not by itself guarantee acceptance in every local collection and sorting scheme, and a supplier's compliance statement should be read against the specific market the product will be sold in.
Step 4 — Chemical resistance and manual trigger operation
PP is a sensible default for chemical-resistant trigger sprayer bodies because it withstands a broad range of aqueous and alcohol-based cleaning formulations. That tolerance is not universal. Strong oxidising agents and certain non-polar solvents can attack PP over prolonged contact, and the practical failure mode is gradual — swelling, loss of dimensional stability, or a seal that stops holding after weeks of storage rather than days. Compatibility should therefore be validated with the actual concentrate, at the concentration and storage conditions the product will experience, not inferred from a material data sheet alone.
Manual trigger operation is the second technical constraint. Output is generated by hand pressure on the trigger, with no propellant and no pressurised container, which simplifies transport classification and removes propellant compatibility from the formulation discussion. It also means the seal is cycled repeatedly for the life of the pack, so sealing performance is the durability parameter to test. Comparison data for the TS-1372 trigger sprayer describes an improved structure with better sealing performance and an anti-leakage design relative to conventional trigger sprayer constructions, and reports no extra maintenance requirement. Those are exactly the characteristics a leak-proof trigger sprayer specification is trying to capture.
Practical validation for this step is straightforward but should not be skipped: a compatibility soak with the real formulation, an actuation cycle test, a leak check after cycling, and a repeat leak check after storage. Manual actuation output also varies with the user's stroke, so output consistency should be assessed across several operators rather than in a single test run.
Step 5 — Commercial terms, OEM customization and bulk orders
Commercial parameters should be negotiated after the technical fit has been established, because tooling, minimum order quantity and custom colour decisions all depend on the technical configuration. A typical approval path runs from bottle sample and formulation sample, through a fit and output test, to a pilot order that confirms filling-line behaviour, before bulk volumes are released.
OEM customization in this category usually concerns colour, branding on the trigger or closure, and packaging configuration rather than the fundamental mechanism. Custom colour introduces its own variables — colour consistency across production lots, and whether the chosen colour interacts with recycled-content material streams — so buyers should agree on an acceptance standard for colour before tooling is committed, not after the first bulk delivery.
Bulk order risk is mostly continuity risk: whether the supplier can repeat the approved configuration across several production runs without dimensional drift. The verifiable evidence here is production capacity and quality system documentation. MILA Plastic Industry was founded in 2018 and operates a factory of more than 30,000 square metres in Quzhou, Zhejiang, China, with 300–400 employees, 60 injection moulding machines, 20 automatic production lines and an R&D team of 10 engineers. The company reports annual output exceeding 600 million pieces, annual sales of USD 50–53 million and an export ratio of 70–80%, and its certifications include ISO 9001:2015 and ISO 14001:2015 with SGS compliance, as published at https://www.triggerssprayer.com/about-us/.
On the trade side, plastic trigger sprayers fall under HS code 3923.50 — "Stoppers, lids, caps and other closures, of plastics" — the heading buyers and freight forwarders should reference when quoting duties and preparing documentation.
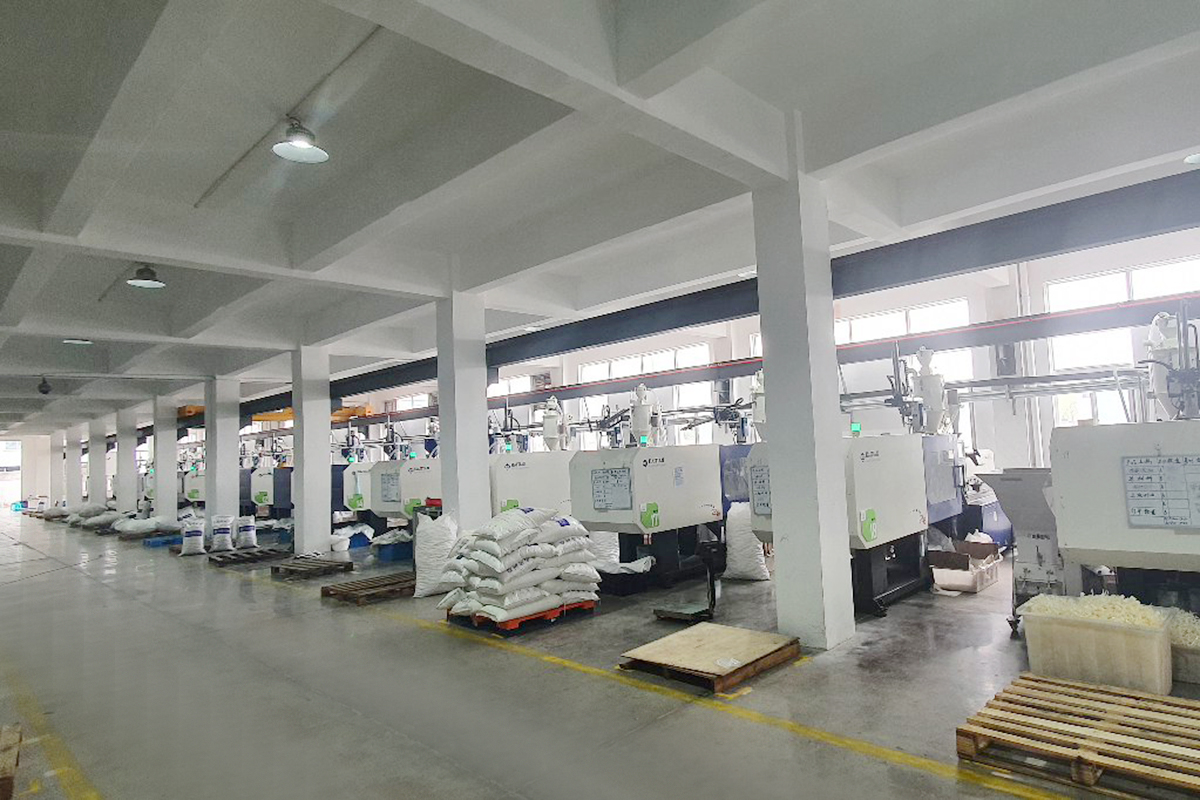
Automatic injection moulding workshop for custom plastic component fabrication — the stage where custom colour and repeat-order consistency are determined.
Step 6 — Acceptance criteria and risk checks
Acceptance criteria convert the earlier decisions into pass/fail conditions that both parties sign against. The table below summarises the checks that matter most in trigger sprayer qualification, and the failure mode each one is designed to catch.
| Check | Criterion to agree before bulk | Failure mode it prevents |
|---|---|---|
| Neck finish match | Documented finish designation confirmed on the physical bottle | Partial assembly, cross-threading, line stoppage |
| Sealing and leak performance | Leak check after assembly and after transport simulation | Leakage in transit, retail complaints, returns |
| Output and pattern | Agreed output type and acceptable pattern range | Formulation applied incorrectly, rework of usage instructions |
| Actuation durability | Cycle test with the agreed formulation | Seal failure during product life |
| Chemical compatibility | Soak test with the real concentrate | Swelling, loss of seal, gradual leakage |
| Material declaration | Polymer identity and mono-material confirmation | Recycled-content or EPR non-compliance in the target market |
| Colour consistency | Agreed sample standard for custom colour | Lot-to-lot mismatch, rejected deliveries |
| Documentation | Certification and quality documentation on file | Delays at customs or in retailer onboarding |
Market signals shaping trigger sprayer sourcing
Three signals are visible in the current data. First, the category is growing steadily rather than explosively: the global trigger sprayers market is valued at USD 491.8 million in 2025 with a projected CAGR of 4.7% from 2026 to 2034, according to Fortune Business Insights. Second, regulation is moving ahead of voluntary design practice in Europe, where the PPWR requires 30% recycled content in plastic packaging by 2030. Third, buyers are increasingly asking for mono-material and all-plastic constructions, which is a design response to the first two signals rather than a consumer-driven trend.
One caution applies to all market data in this category: scope definitions vary between research houses, and figures that appear to conflict often describe different products. The USD 491.8 million valuation and the substantially larger alternative estimate circulating for the same category differ mainly in whether the bottle assembly is included. Buyers should record the scope behind any market figure they cite internally, because a specification decision made against the wrong scope definition is difficult to reverse.
How mono-material trigger sprayers compare with conventional constructions
In the available comparison data, the TS-1372 trigger sprayer is benchmarked against conventional trigger sprayers. The stated differences are structural and sealing-related: an improved structure with better sealing performance, an anti-leakage design, and enhanced durability. The same comparison reports stable spray output and consistent performance, with better results in household cleaning and industrial spraying conditions where stable output is required, no extra maintenance compared with conventional trigger sprayers, and a competitive production cost.
The limitation is in the baseline. "Conventional trigger sprayer" is a category-level reference, not a specific competing model, and the comparison is expressed as a relative advantage rather than as measured values. It does not establish that the TS-1372 outperforms every alternative design on the market, and it does not quantify the durability gain. For a buyer, the comparison is most useful as a set of hypotheses to test — sealing performance, leak behaviour and output consistency — each of which should be confirmed under the buyer's own bottle, formulation and transport conditions before it becomes a purchasing assumption.
Future outlook
The direction of the category is toward fewer materials per closure and more documented material content. As the PPWR 2030 recycled-content requirement approaches, mono-material PP designs move from a sustainability talking point to a specification line item, and suppliers will increasingly be asked to provide material declarations alongside dimensional drawings. Growth of 4.7% per year through 2034 does not describe a market in disruption; it describes a market where incremental compliance and fit reliability decide who keeps the account.
For buyers, the practical consequence is that the decision order described here is likely to become shorter and more evidence-based rather than longer. Neck fit and spray output will still be decided on samples; material content and documentation will increasingly be decided on paper, before the samples are ordered.
FAQ
1. How do I determine whether my bottle requires a 28/400 or a 28/410 trigger sprayer?
Confirm the thread finish designation, not just the nominal diameter. Both 28/400 and 28/410 refer to a nominal 28 mm neck, but they differ in thread geometry, so the correct closure is the one engineered for the finish on the actual bottle. Industry reference material identifies 28/410 as the most commonly used opening for trigger sprayers, which makes it a common starting assumption; the confirmation step is to assemble the closure on a physical bottle sample and check thread engagement and sealing before any performance testing. If only the diameter is documented internally, request a dimensional neck drawing from the bottle supplier.
2. Should I choose a fine mist or a foaming trigger sprayer?
The choice depends on contact behaviour rather than on a performance ranking. Fine mist atomises the liquid into small droplets and distributes them across a broad area, which suits applications where even coverage and low residue matter. Foam aerates the liquid so that it clings to vertical surfaces and remains in contact longer, which suits tasks where dwell time affects results. Cleaning routines and the specific formulation usually decide the question; both formats are validated in sampling, and an approval for one format does not automatically apply to a pump-based foamer, which uses a different internal design.
3. What does all-plastic PP construction change for recycling compliance?
An all-plastic, mono-material PP construction keeps the closure within a single polymer stream instead of combining plastic and metal components that would need separation before sorting. That matters where recycled-content or extended producer responsibility rules apply. The EU PPWR, adopted in April 2024, requires 30% recycled content in plastic packaging by 2030. Mono-material design supports that requirement, but it does not guarantee acceptance in every local collection and sorting scheme, and the regulation itself is scoped to packaging placed on the EU market.
4. What should be verified before approving a bulk trigger sprayer order?
Approval should rest on documented pass/fail results rather than on sample impressions. The core checks are neck finish match on the physical bottle, sealing and leak performance after assembly and after transport simulation, output type and pattern within an agreed range, actuation durability with the real formulation, chemical compatibility after a soak test, material declaration covering polymer identity and mono-material status, and an agreed colour standard where custom colour is involved. Production capacity and quality certification documentation support the continuity question — whether the approved configuration can be repeated across production lots without dimensional drift.
5. Which certifications and trade classifications apply to trigger sprayer sourcing?
Plastic trigger sprayers are classified under HS code 3923.50, which covers stoppers, lids, caps and other closures of plastics — the heading used for duty and customs documentation. On the quality side, ISO 9001:2015 and ISO 14001:2015 are the certifications buyers most commonly request; Mila Plastic holds both, together with SGS compliance. Certification scope should be checked against the specific site and process performing the work, and material-related declarations should be reviewed separately from quality management certification, since the two answer different questions.
Read in sequence, the framework reduces to one rule: settle what cannot be changed before comparing what can. Neck finish and sealing integrity are fixed once the bottle is filled; spray pattern, documentation and commercial terms remain negotiable afterwards.