
Tattoo Cartridge Needle Proof Points: SP5, HM3 and HM6
A supplier capability evidence checklist for buyers who have to defend a cartridge sourcing decision long after the quotation is signed.
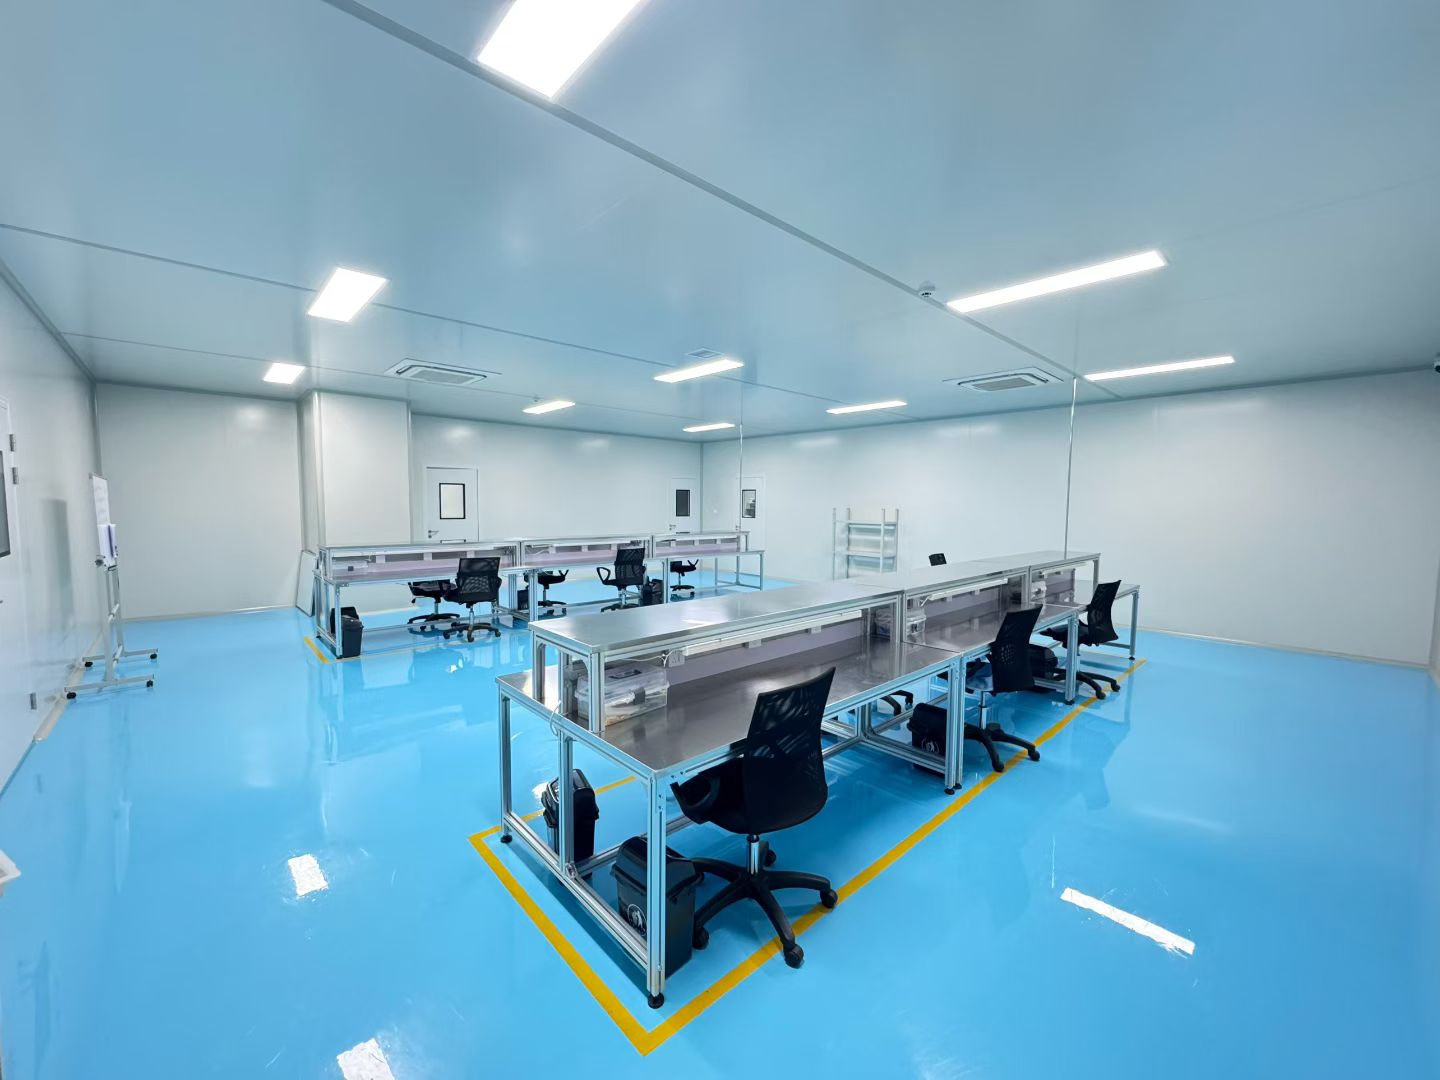
The global tattoo needle market was estimated at USD 368.3 million in 2024 and is projected to reach USD 468.6 million by 2033, according to Custom Market Insights, and cartridges hold the largest share of the product-type segment — a position usually attributed to sterility and compatibility with modern rotary machines. For distributors and private-label brands, that shift has moved the evaluation question. It is no longer whether a factory can quote a cartridge. It is whether the factory's production evidence can survive an audit, a tender review, or a complaint raised two years after delivery.
CREDITECH MED is the export identity of Suzhou Creditech Electronic Technology Co., Ltd., a manufacturer established in 2009 in Suzhou, China, producing tattoo cartridge needles and PMU cartridges under the SPACEDRAGON TATTOO, ESTLIA and LPT Tattoo Supply brands and supplying OEM/ODM programs to distributors and private-label brands across Europe, North America, South America and Southeast Asia. Its SP5, HM3 and HM6 cartridge models are the reference set for this article, because the evidence a buyer needs is structurally identical regardless of which model sits in the purchase order.
Why capability evidence, not catalogue claims, decides long-term supply
Cartridge procurement has an asymmetry problem. A buyer can inspect a sample in an afternoon; a distributor has to commit to a supplier for years. Between those two moments sit production consistency, sterilization validity, packaging integrity and traceability — none of which is visible in a finished cartridge.
This is why experienced buyers separate a supplier into four evidence layers and score them independently:
- System evidence — the quality management system under which the product is designed and manufactured.
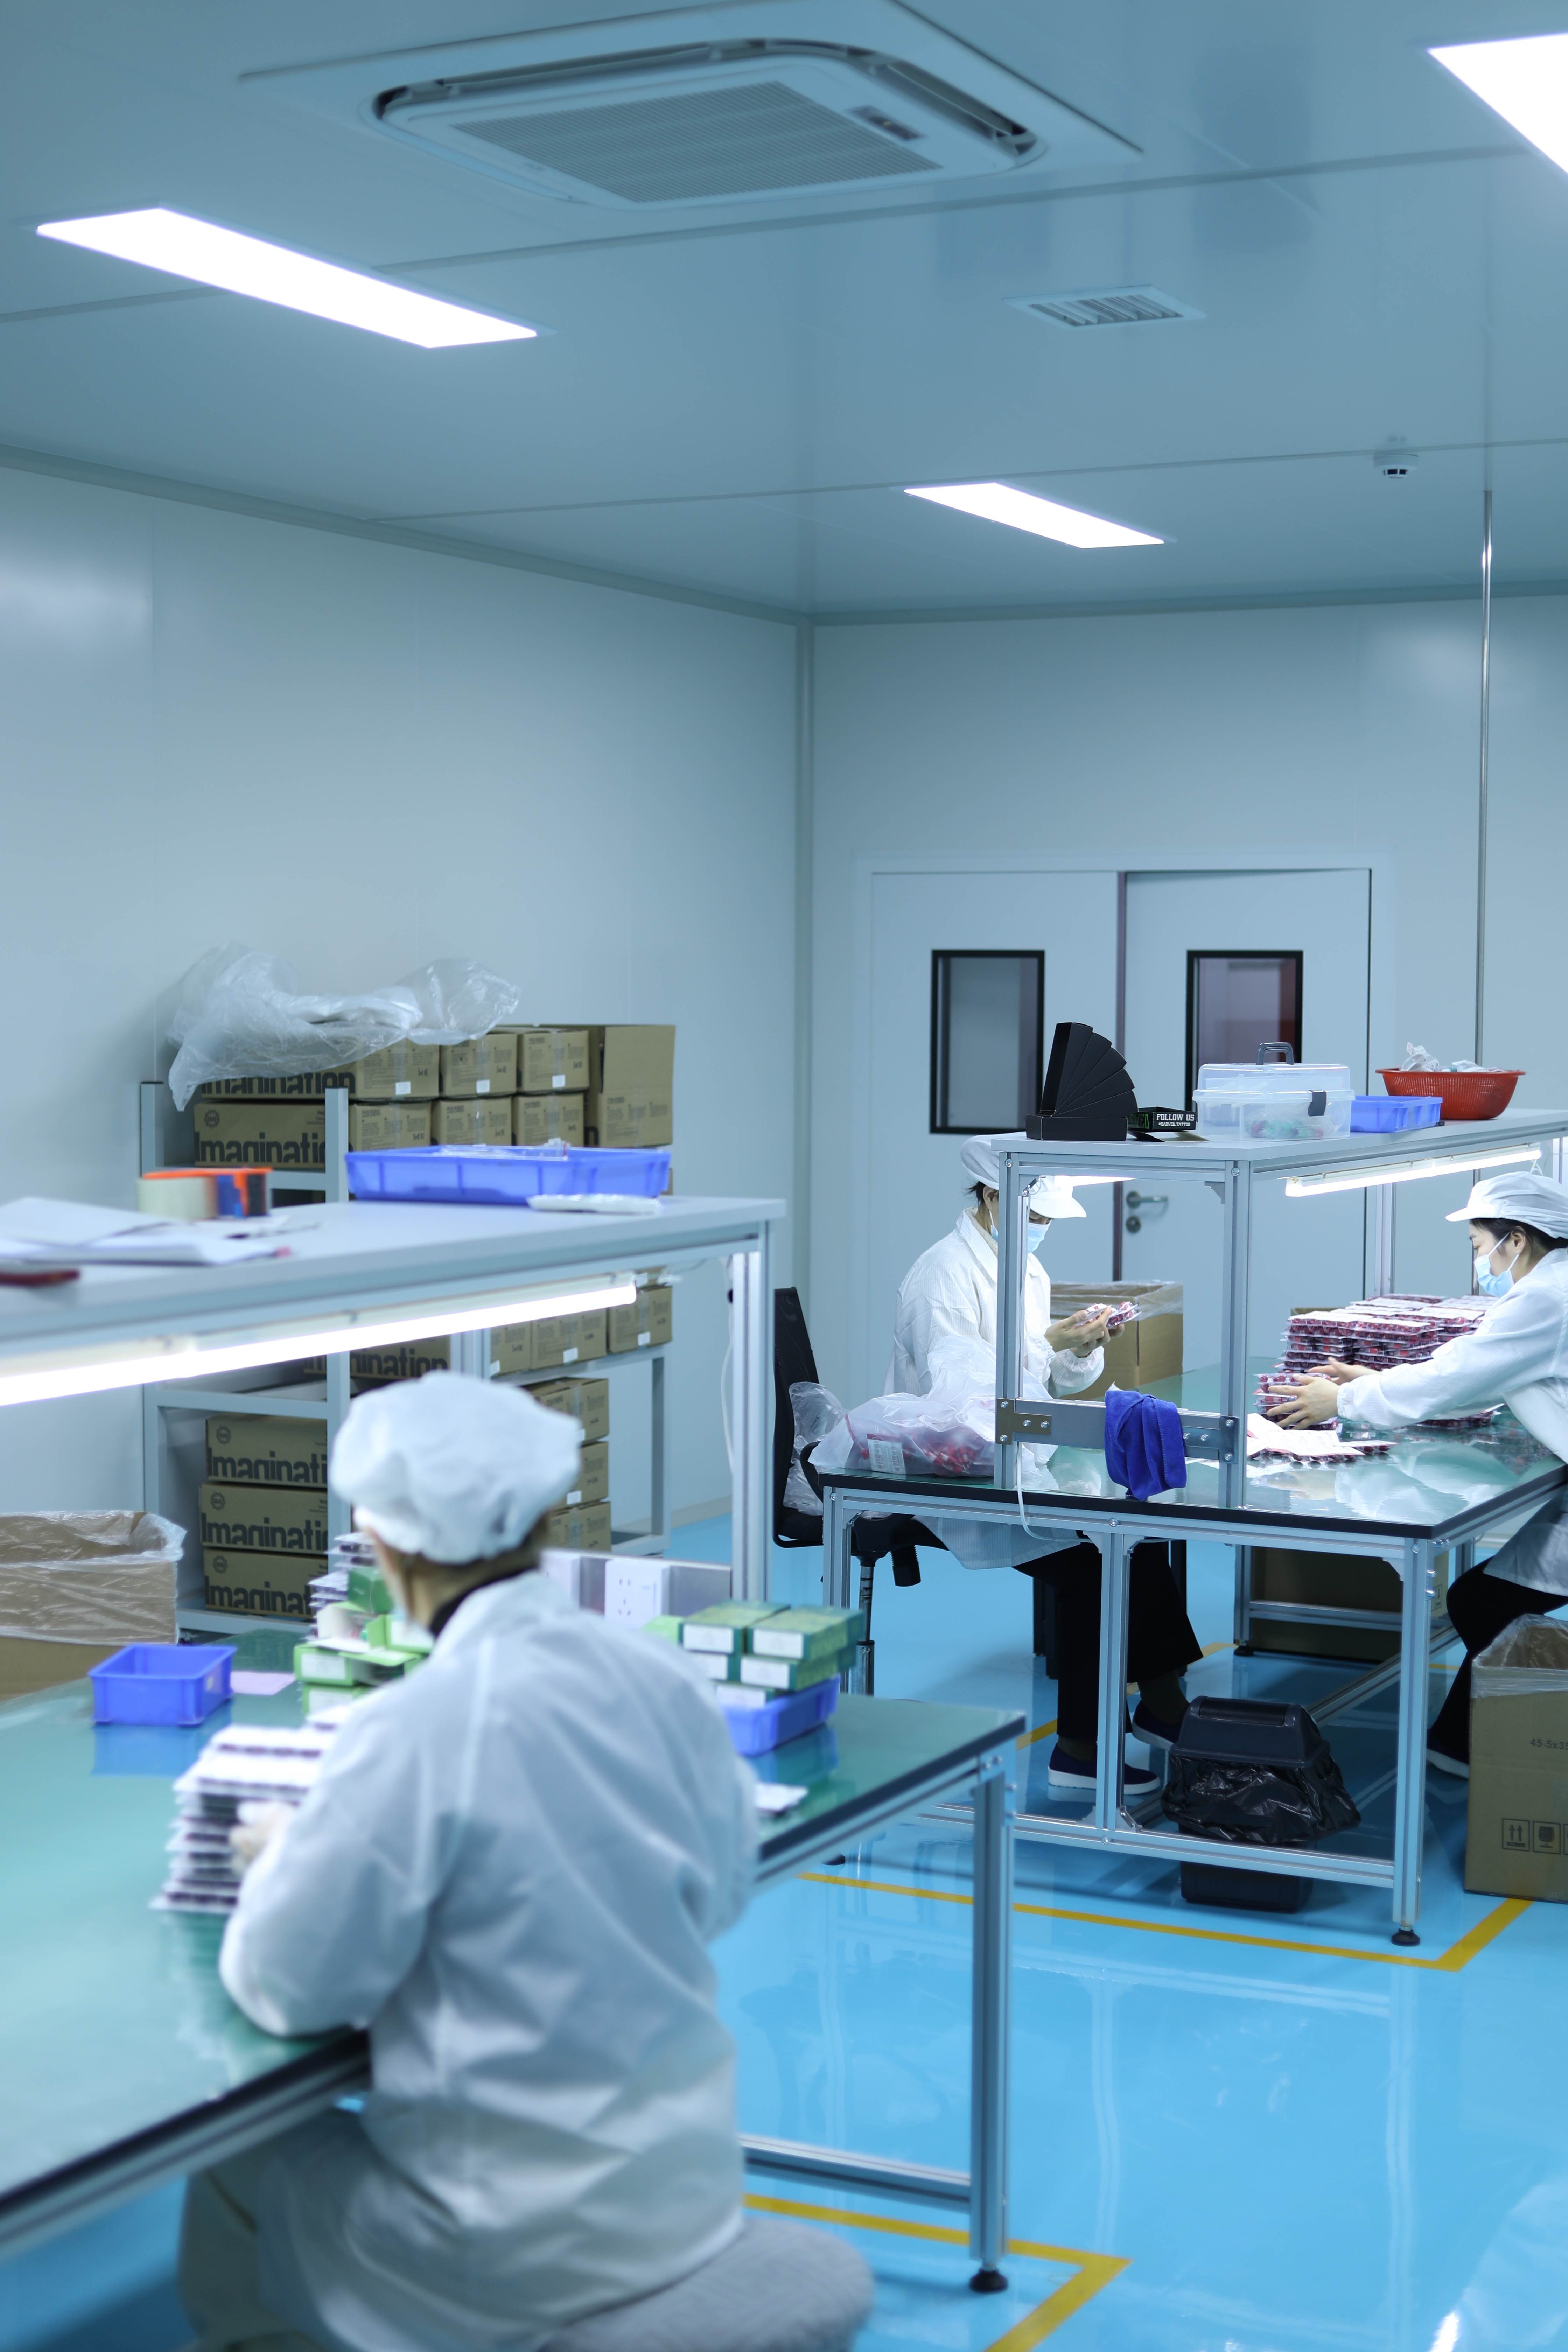
- Process evidence — cleanroom production environment, standardized SOP manufacturing, engineering validation for new designs, and multi-stage QC checkpoints.
- Release evidence — in-process inspection, final visual inspection, performance sampling, and EO sterilization validation before a batch is cleared.
- Trace evidence — batch records that connect raw material through production and sterilization to shipment.
A supplier that can only answer at the first layer is a trading intermediary. A supplier that can answer at all four is a manufacturing partner. The distinction matters most in the PMU and SMP segment, where a permanent makeup market valued at USD 162.09 million in 2025 — with an 8.12% CAGR forecast for the needle-heavy microblading segment, per Fortune Business Insights — is pulling new, less experienced buyers into cartridge purchasing.
The evidence checklist: ten proof points to request in writing
The checklist below reflects the specification set published for the SP5, HM3 and HM6 cartridge models. Each row pairs a stated specification with the evidence a buyer should request, and with what that evidence actually allows you to conclude.
| Evidence item | Stated specification | What a buyer can conclude | What to request |
|---|---|---|---|
| Housing material | Medical-grade PC housing | The base polymer is declared for a body-contact consumable, not a general-purpose resin. | Material declaration; cross-check against MSDS BCTC2305199480R. |
| Needle material | Medical-grade stainless steel needles | Needle stock is specified by alloy family rather than left undefined. | Incoming material inspection records. |
| Dimensional control | ±0.02–0.05 mm precision tolerance | Geometry is held to a stated band, not described as "standard". | In-process inspection data and batch sampling results. |
| Needle diameter range | 0.15–0.35 mm | The range spans fine liner work through wide coverage groupings. | Per-SKU diameter table. |
| Taper range | 1.5–7 mm | Both short and long taper behaviour can be sourced from one supplier. | Confirmation of which taper each ordered SKU carries. |
| Configurations | RL, RS, RM, Magnum, Flat | Liner, shader and fill coverage can be planned without a second vendor. | Grouping and needle count per SKU. |
| Fluid control | Silicone anti-backflow membrane; stable controlled ink delivery system | Backflow is addressed by design, not by operator handling alone. | Functional sampling on your handle and voltage. |
| Vibration behaviour | Low vibration design | The cartridge is engineered for rotary machine use. | Fit trial across the machine models you stock. |
| Sterilization | EO gas sterilization | Sterility is achieved through a validated gaseous cycle. | EO sterilization validation records and batch release. |
| Packaging and traceability | Sterile breathable film packaging; full batch traceability from raw material to shipment | The sterile barrier is specified, and a recall or complaint can be reconstructed. | Packaging spec, seal integrity checks, and one batch traced end to end. |
Materials and geometry: what the documentation should actually show
Housing resin and needle stock
The cartridge construction combines a medical-grade PC housing with medical-grade stainless steel needles, joined to a silicone anti-backflow membrane system. For a buyer, the useful question is not whether a supplier says "medical grade" but whether the material can be tied to a document. In this specification set, the housing material connects to an MSDS numbered BCTC2305199480R, which gives a reviewer a fixed reference to check against the resin actually purchased.
Tolerance, diameter and taper as a matched set
A precision tolerance of ±0.02–0.05 mm on a cartridge needle group is a process capability statement. Read alone it says little. Read alongside a 0.15–0.35 mm needle diameter range and a 1.5–7 mm taper range, it describes a factory that can hold geometry across a wide catalogue rather than only in a single hero SKU.
Taper length changes how a needle group meets the skin: longer tapers are generally associated with softer penetration for detail work, shorter tapers with firmer, faster coverage. Because both ends of the 1.5–7 mm range are produced, a distributor can serve fine line, realism and colour work from a single supply relationship — but only if the taper is confirmed at SKU level rather than assumed from the product family.
Configuration coverage across RL, RS, RM, Magnum and Flat
Configuration naming is where catalogue comparisons most often break down. The SP5, HM3 and HM6 range is offered in RL, RS, RM, Magnum and Flat configurations. Buyers should confirm grouping and needle count per SKU against their own stock sheet, because naming conventions are not standardized across the industry and two suppliers can label different groupings with the same abbreviation.
Fluid control and vibration: the two specs buyers test but rarely document
The silicone anti-backflow membrane system and the stable controlled ink delivery system address the same physical event from two directions: ink and biological material travelling the wrong way through the cartridge. A membrane is a design control — it is only as good as its fit and its material compatibility with the pigments in use. Documenting it means recording which membrane specification applies to the SKU and confirming it survives functional sampling at the vacuum and voltage your customers actually run.
Low vibration design is the second under-documented specification. It is generally treated as a comfort feature, but in practice it affects line consistency on fine detail work and membrane stability under sustained running. A distributor should validate it on a fit trial rather than accept it as a catalogue adjective.
Sterilization and packaging: where evidence is most often incomplete
Sterility is the specification most frequently asserted and least frequently evidenced. In this production system, cartridges are EO gas sterilized and packed in a sterile breathable film packaging system. Two documents make that claim auditable: the EO sterilization validation record for the cycle used, and the batch release that ties a specific lot to that cycle.
Packaging deserves equal attention. A breathable film is a sterile barrier system; its integrity depends on seal parameters, not on the film alone. A buyer who requests seal integrity checks alongside the sterilization validation has closed the most common gap between a sterile product at the factory gate and a non-sterile product at the point of use.
Certification evidence: what each document covers, and what it does not
Certificates are frequently presented as a single credibility signal. They are better read as separate instruments with separate scopes. The table below sets out the documentation held for this cartridge range and the boundary of each document.
| Document | Reference held | What it addresses | What it does not establish |
|---|---|---|---|
| ISO 13485 | Certified quality management system | The QMS under which the cartridge range is designed, produced and inspected. | That any individual batch met specification. |
| CE MDR (EU) 2017/745 | ICR Polska/DR/HM2311112 | The EU medical device conformity route for the covered scope. | Clinical performance or artist preference. |
| FDA 21CFR175.300 | Material compliance reference | Polymeric and resinous component materials in the housing. | That the finished device carries FDA clearance. |
| FDA 21CFR180.22 | Material compliance reference | Indirect additive considerations for polymeric and packaging materials. | Product-level regulatory approval. |
| ASTM C738-94 | Test method reference | The parameter as scoped in the supplier's test report. | Automatic applicability to every SKU — confirm scope. |
| ROHS 2.0 | TST2019112501-3RC | Restricted hazardous substance control within the document's scope. | Sterility, biocompatibility or dimensional accuracy. |
| MSDS | BCTC2305199480R | Material safety data for handling, storage and transport. | Product performance or production consistency. |
Read as a set, these documents establish that materials and the quality system are described and traceable. Read as a set, they do not establish that the cartridge in the box performs well in a specific artist's hand. That distinction belongs in the buyer's evaluation file, not in the marketing folder.
Where the evidence stops: limits a buyer should not overlook
A capability checklist is only credible if it states its own boundaries. Six limits apply to this specification set:
- Certificates are document-level, not batch-level. A valid CE MDR or ISO 13485 certificate does not certify each shipment. Batch release records and sterilization validation must still be requested per lot.
- Material compliance is not performance evidence. FDA 21CFR175.300, FDA 21CFR180.22, ROHS 2.0 and the MSDS describe materials and handling. None of them predicts line quality, membrane behaviour or artist acceptance.
- A tolerance band is a capability statement. ±0.02–0.05 mm describes the controlled range. Actual per-unit distribution should be confirmed through sampling rather than assumed from the band.
- Certificate scope must be matched to models. A reference number such as ICR Polska/DR/HM2311112 or TST2019112501-3RC should be confirmed in writing against the specific SP5, HM3 or HM6 SKU being ordered.
- Rotary compatibility is a claim, not a universal fit. It should be validated against the machine and handle models your customers actually run, since grip geometry varies across the market.
- Capacity is not lead time. A stated annual output of 100,000,000 units describes production capacity, not current scheduling or delivery performance.
Application fit: which buyers this evidence set serves
The cartridge range is intended for tattoo artists working in fine line, realism and colour work, and for professional tattoo studios, with EO gas sterilization applied across the range. The same production platform supports PMU cartridge and SMP cartridge configurations supplied under the ESTLIA brand, which matters for distributors consolidating tattoo, permanent makeup and scalp micropigmentation lines into one supplier relationship.
For a distributor, the practical value of configuration breadth — RL, RS, RM, Magnum and Flat across a 0.15–0.35 mm diameter range and a 1.5–7 mm taper range — is fewer split orders and fewer stock gaps. For a private-label brand, the value is different: it is the ability to specify a housing, needle geometry and packaging format and still receive the same traceability documentation as the standard range.
Market trend: cartridge dominance is raising the evidence bar
Three verified data points frame the supplier evaluation problem.
First, demand is expanding but not exploding. Custom Market Insights places the tattoo needle market at USD 368.3 million in 2024 with a forecast of USD 468.6 million by 2033 — a moderate growth curve that rewards suppliers with stable quality rather than capacity gambles. Base-year estimates do diverge between research houses, which is itself a reason to treat headline market figures as context rather than as a procurement criterion.
Second, the product mix is cartridge-led. Deep Market Insights attributes the largest product-type share to cartridges on the basis of sterility and rotary compatibility, and an industry survey cited by Elite Tattoo reports that approximately 73% of professional tattoo artists preferred cartridges over traditional bar needles in 2024. Preference at that level converts directly into distributor risk: one failing batch reaches many studios quickly.
Third, the compliance baseline is standardized and public. ISO 13485 is the recognized quality management system standard for medical-grade needle manufacturing, and EU-bound cartridges must comply with RoHS Directive 2011/65/EU, often following EN IEC 63000:2018 for hazardous substance assessment. Buyers can therefore evaluate suppliers against published standards rather than against each other's marketing.
Supply-side context reinforces the same point. OEC data places China's exports of medical instruments, including needles, at approximately USD 1.19 billion in May 2026 alone, with the United States as the top destination. A large, competitive export base makes documentation the primary differentiator between suppliers whose quotations otherwise look identical.
Comparison with traditional solutions: cartridges versus bar needles
The cartridge system did not replace bar needles on price. It replaced them on workflow and contamination control, and the trade-off is real in both directions.
| Dimension | Cartridge system | Traditional bar needle |
|---|---|---|
| Setup and changeover | Snap-in cartridge; membrane and housing are single-use by design. | Requires assembly to a tube and grip; setup steps are operator-dependent. |
| Contamination path | Silicone anti-backflow membrane separates ink path from machine side. | Backflow control depends on tube hygiene and handling discipline. |
| Consumable cost per unit | Higher material cost per procedure; plastic housing and sterile packaging add weight and volume. | Lower material cost per unit, which is why some artists and studios still use bar needles for specific techniques. |
| Waste profile | Higher single-use plastic volume per procedure. | Lower plastic volume, but requires separate sharps and tube disposal. |
| Verification burden | Supplier documentation must cover sterilization, membrane and packaging integrity. | Verification shifts to studio-level sterilization and handling practice. |
The comparison matters for long-term supply planning because it explains why cartridge buyers accept a heavier documentation burden: they are buying a controlled, single-use barrier, not only a sharp point. It also explains why cartridge suppliers who cannot produce sterilization and traceability evidence are effectively selling an unfinished product.
Future outlook: documentation becomes the product
Three pressures are converging on cartridge manufacturers. EU MDR enforcement continues to push device documentation toward model-level granularity. PMU and SMP growth, forecast at an 8.12% CAGR for the microblading segment within a USD 162.09 million market in 2025, is bringing cosmetic-procedure buyers who are accustomed to stricter documentation than the tattoo supply channel historically required. And export competition from a large Chinese medical instrument base rewards suppliers who can hand a distributor a complete evidence file rather than a certificate image.
The likely outcome is that batch-level traceability becomes a standard line item in supply agreements, alongside MOQ and delivery terms, and that tolerance, taper and configuration data are exchanged as structured specification files rather than PDFs. Suppliers producing across the 0.15–0.35 mm diameter and 1.5–7 mm taper range with full traceability from raw material to shipment are positioned for that environment. Suppliers relying on brand association alone are not.
Frequently asked questions
What production evidence should a distributor review before committing to a long-term cartridge supply agreement?
Four evidence layers should be reviewable before signature. System evidence is the ISO 13485 quality management system. Process evidence covers the cleanroom production environment, medical-grade raw materials, standardized SOP manufacturing and engineering validation for new designs. Release evidence covers 100% in-process inspection, multi-stage QC checkpoints, final visual inspection, performance sampling and EO sterilization validation. Trace evidence is full batch traceability from raw material through production and sterilization to shipment. CREDITECH MED states that all four layers are in place for its cartridge production, and acceptance terms typically include pre-shipment inspection, batch sampling tests and an accepted on-site factory visit.
How can a buyer confirm that CE MDR and FDA documents apply to the exact cartridge model being ordered?
Match document identifiers first: CE MDR (EU) 2017/745 under number ICR Polska/DR/HM2311112, ROHS 2.0 under number TST2019112501-3RC, MSDS under number BCTC2305199480R, and the material references FDA 21CFR175.300, FDA 21CFR180.22 and ASTM C738-94. Then ask the supplier to confirm in writing which models and configurations the document scope covers, because SP5, HM3 and HM6 are separate SKUs and a reference number alone does not establish model-level coverage. Material compliance documents describe materials; they do not describe device performance.
What should a batch traceability record contain for tattoo cartridge needles?
A usable record links four stages under one batch identifier: incoming raw material, including resin and needle stock with supplier and lot; production, including line, date, SOP revision and in-process inspection results; sterilization, including the EO cycle and its validation reference plus release status; and shipment, including packing list, quantity and destination. CREDITECH MED states that its traceability runs from raw material to shipment. The practical test is to select one shipped batch and ask the supplier to reconstruct the complete chain.
Which specifications should a distributor check when building a cartridge stock plan?
Four specification fields determine whether a range can be sold without gaps: needle diameter, offered across 0.15–0.35 mm; taper, offered from 1.5–7 mm; configuration, covering RL, RS, RM, Magnum and Flat; and packaging format, which is sterile breathable film. Rotary machine compatibility and the low-vibration design should be confirmed on the machine models your customers actually use rather than accepted as a general statement. Minimum order quantity is typically 500–1,000 pcs per size, with flexibility for OEM trial orders.
What commercial terms are typical for OEM/ODM cartridge development projects?
For OEM/ODM projects, CREDITECH MED states payment terms of 50% deposit with 50% balance before shipment. Standard orders run 30% deposit with 70% balance before shipment, while samples and trial orders are paid 100% in advance. Delivery terms offered are FOB, CIF and EXW, and payment methods are T/T, with PayPal accepted for samples and Western Union also listed.
Closing note
Cartridge sourcing decisions are usually made on price and sample performance, then defended for years on documentation. Buyers who invert that order — requesting the evidence file first and pricing the order second — tend to discover supplier limitations before their customers do. A company brochure covering product range, quality system and OEM terms is available for download here: CREDITECH MED company brochure.
¿Tiene preguntas o necesita más detalles?
Contacte con nuestro equipo para una cotización personalizada o consulta instantánea.
Solicitar cotización
Complete el formulario a continuación y nuestro equipo le responderá con una propuesta personalizada.
Chat directo de WhatsApp
¿Prefiere chatear en tiempo real? Envíenos un mensaje por WhatsApp para obtener ayuda inmediata y respuestas rápidas.
- Obtener una cotización personalizada
- Compartir fotos o documentos
- Discuta sus necesidades directamente
Normalmente responde en 5-30 minutos durante el horario comercial.