
TS107 to TS109 Silicone OCA: Semiconductor and AI Display Fit
Optical bonding used to be settled inside display factories. It is now a line item in programs built around semiconductor content and AI hardware, where display and optoelectronic modules are judged against thermal cycling, enclosure geometry and years of field service — and where the adhesive layer is often the last item reviewed and the first to affect yield.
For engineering and procurement teams assessing Polomo’s silicone OCA models TS107, TS108 and TS109, scenario fit is best judged in three steps: whether the display stack can physically accept the sheet, whether the assembly line can sustain the required lamination route, and whether the supply chain can hold the material inside its storage window for the life of the program. Each step can be answered before qualification testing begins, which is why a fit review is cheaper than a failed qualification.
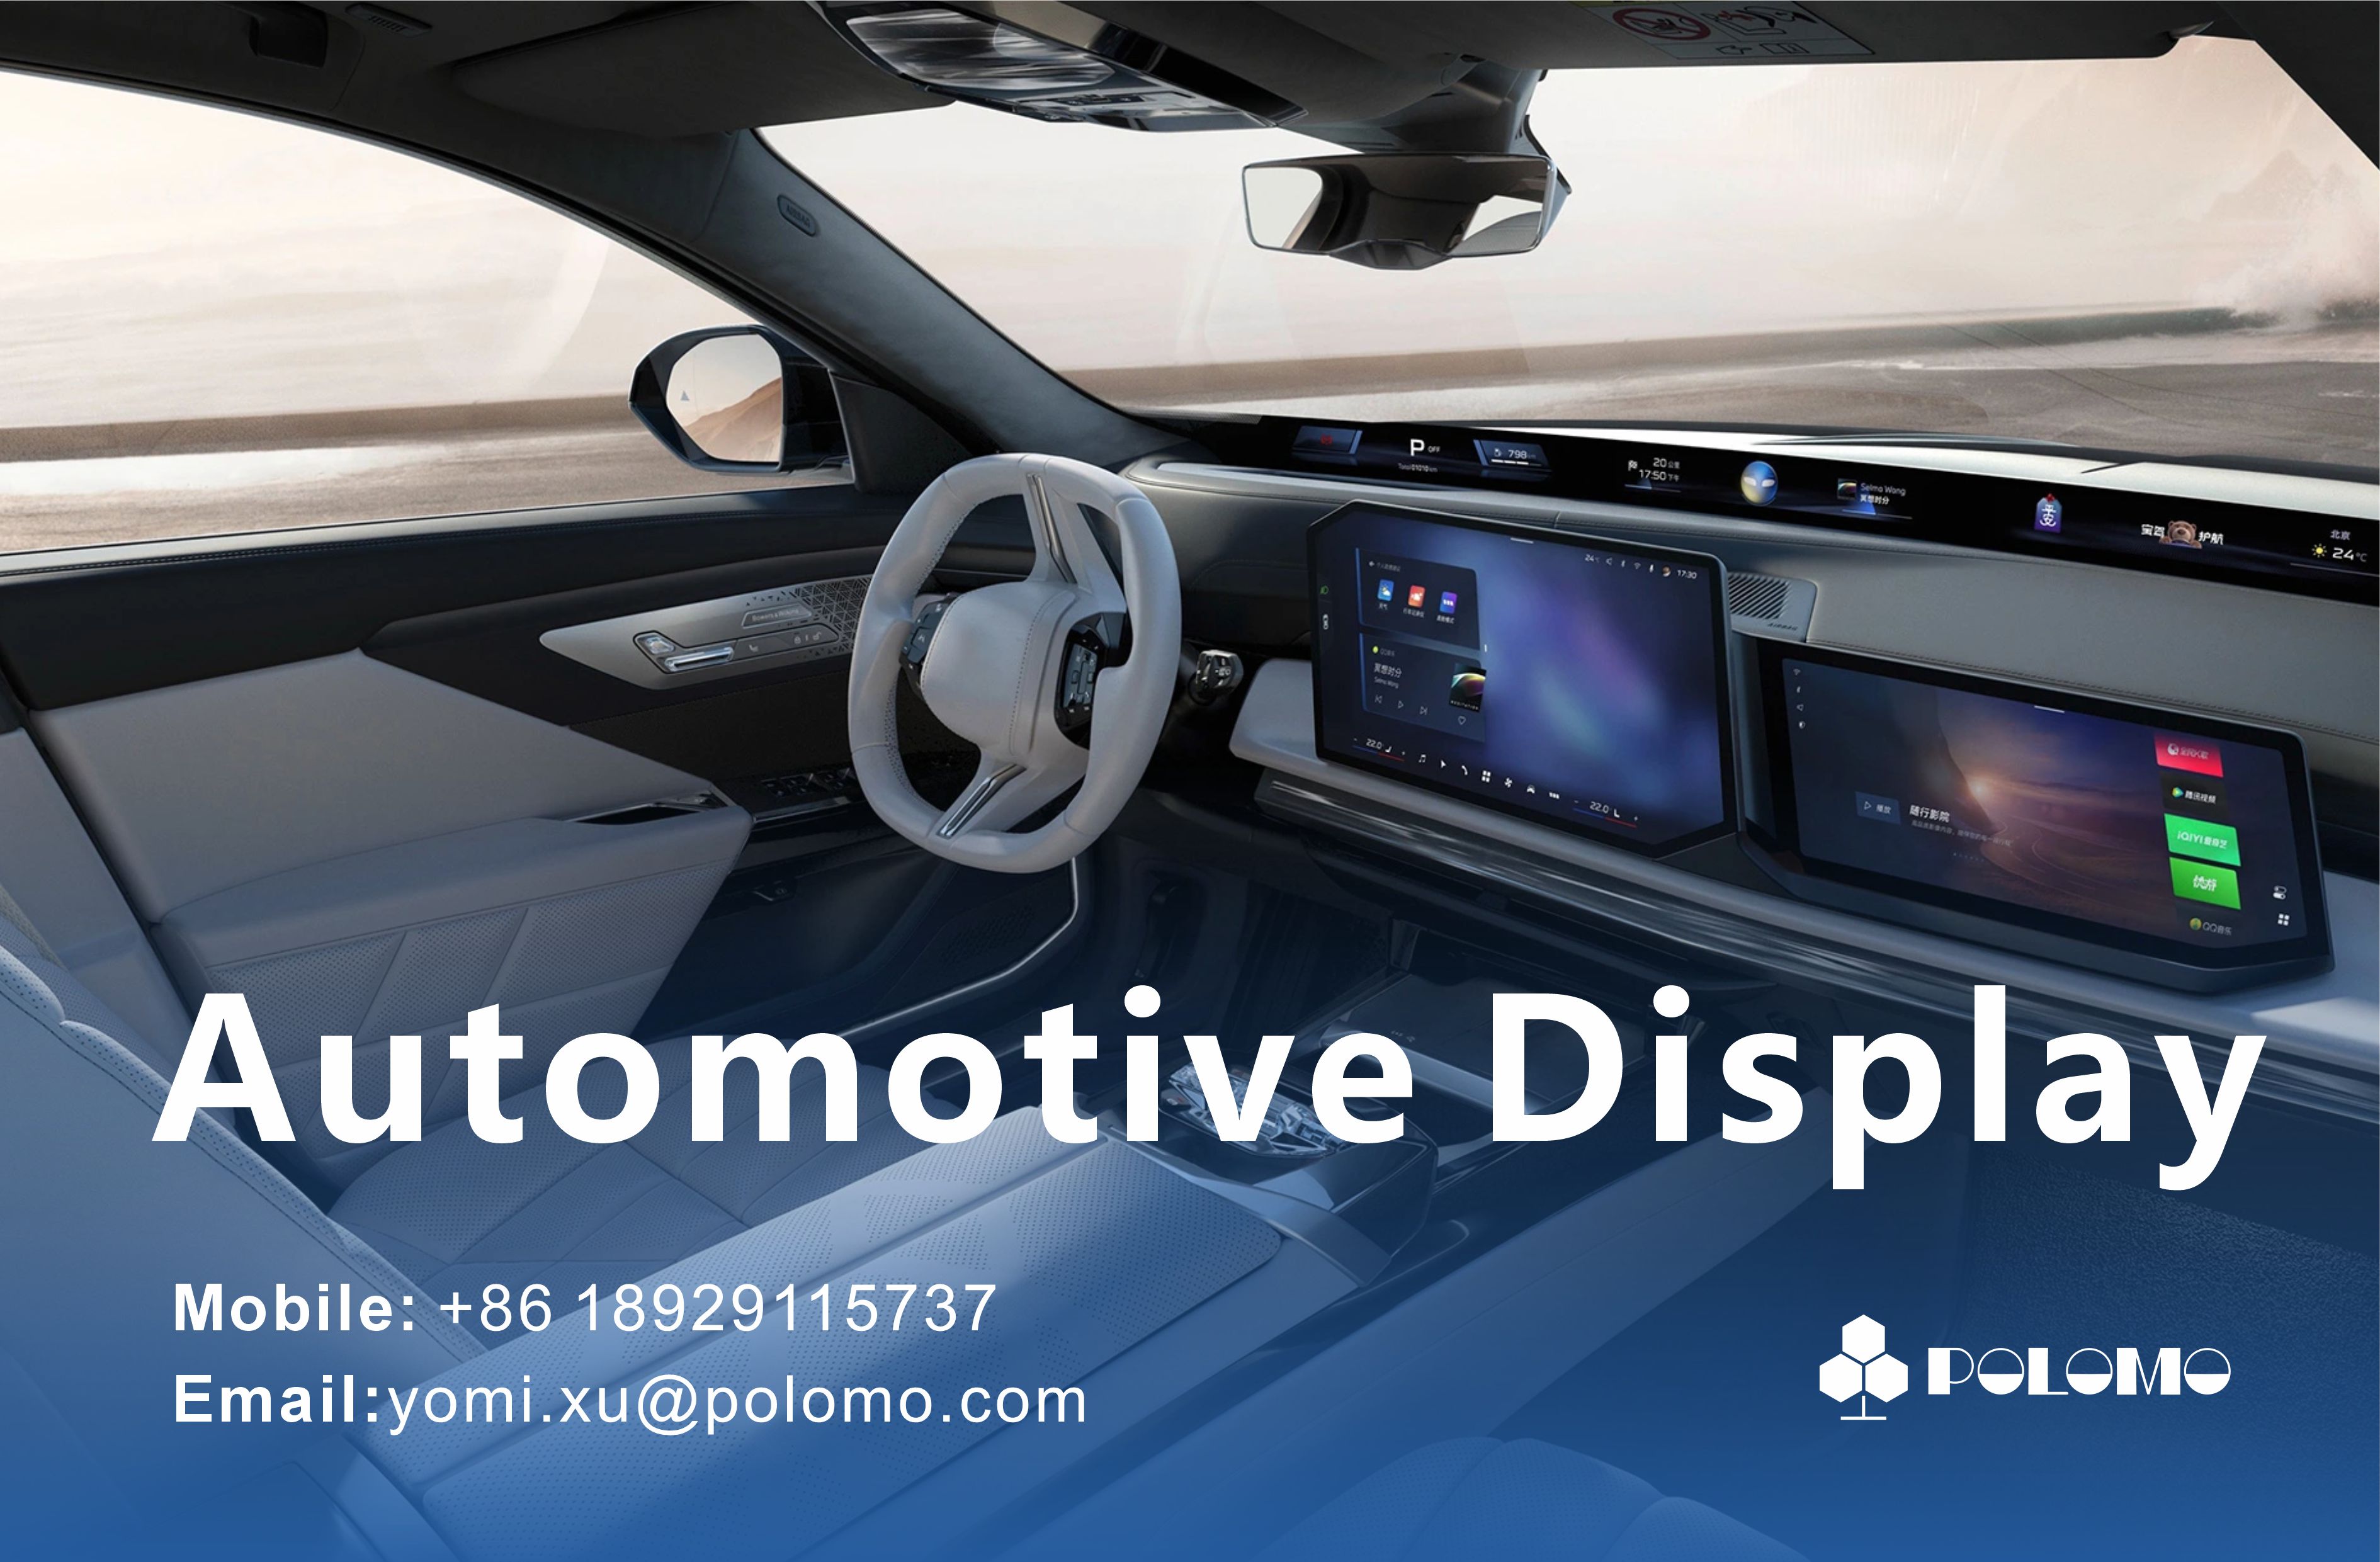
Full lamination of a display module in an outdoor automotive application — one of the operating environments that shapes silicone OCA selection. Image: Polomo.
Why fit is decided before the datasheet is read
A silicone OCA datasheet answers a narrow question: what the material is. It does not answer the question a semiconductor or AI display program actually asks: whether this adhesive, bonded with this process, in this enclosure, will still be optically clean after three years of thermal and humidity cycling.
The distinction matters because silicone OCA sits at the intersection of three independent risk systems. Optically, it must keep transmittance high and haze low while resisting yellowing. Mechanically, it must absorb thermal expansion mismatch between cover glass, touch sensor and panel without transmitting stress that shows up as mura. Operationally, it must survive a lamination route and a storage regime that are both less forgiving than those of ordinary pressure-sensitive adhesives.
Programs that treat these as one decision tend to discover the third one late, usually during a ramp rather than a pilot. Programs that separate them — stack, process, supply — can usually screen a candidate grade out in a week without cutting a single production panel.
What the TS107, TS108 and TS109 series actually is
Polomo (Guangdong Polomo New Materials Technology Co., Ltd) is a materials manufacturer founded in 2002 that develops, produces and sells high-performance adhesive and functional film solutions for optoelectronic displays, semiconductor packaging, energy storage and batteries, and AI-enabled smart hardware. Its production base covers 90,000 m² with a workforce of approximately 300 and an R&D team of 80 engineers; annual output is stated at 10 million pieces, with roughly 30% of sales exported to global markets.
TS107, TS108 and TS109 are three models within the same silicone OCA product family. They are supplied as a colourless transparent solid, used for full lamination of displays, and described as an all-climate OCA. Published series-level parameters are as follows.
| Parameter | Series value | What it tells a program team |
|---|---|---|
| Thickness | 20–2000 µm | Wide enough to cover thin cover-glass stacks and thick gap-fill geometries within the same family |
| Product size | 3–50″ | Relevant to large-format and narrow-bezel panels, not only handheld formats |
| Modulus | 22±5 | A low-modulus designation, associated with stress absorption in large laminations |
| Δb | 0.03 | A colour-shift indicator used when anti-yellowing is a program requirement |
| Haze | <0.3 | Optical clarity threshold, meaningful for high-brightness and high-PPI modules |
| Water absorption | <0.3 | Indicative of behaviour under humidity and low-pressure exposure |
| Dielectric constant (1 MHz) | 2.9 | Electrical context for stacks that include touch or sensor layers |
| Appearance | Colourless transparent solid | Sheet format, handled as a film rather than a dispensed liquid |
The stated property set includes high transmittance and yellowing resistance, low modulus with strong degassing capability, and retention of optical and mechanical properties under high and low temperature, high temperature and high humidity, high-altitude negative pressure, vibration and strong UV exposure. The series is also described as low odour and low VOC, with low volatilisation at elevated temperature, and as adhering well to glass, PET, polarisers and metals.
One point deserves to be stated plainly rather than glossed over: the published data is series-level, not model-level. TS107, TS108 and TS109 share the same documented parameter window. A program cannot select between the three from a specification table alone — model assignment has to be confirmed against the actual stack, thickness requirement and panel size. Procurement teams should treat any model-by-model comparison that is not backed by measured lamination data as unverified.
Semiconductor and AI display scenarios that change the bonding requirement
The scenarios where silicone OCA enters a semiconductor-linked or AI-hardware program are not exotic. They are ordinary display problems with harder boundary conditions.
Large area with narrow bezel. As bezels shrink, the adhesive has less room to relieve the stress created by thermal expansion mismatch across the bond line. A low-modulus sheet distributes that stress instead of transmitting it to the panel, which is the mechanism behind mura and bubble formation in large laminations. Third-party technical commentary on large curved automotive displays points to the same requirement — low-modulus silicone OCA is used specifically to limit mura under thermal stress.
Thermal cycling in an enclosed housing. Equipment that carries high-compute silicon runs hot, then cools. The bond line sees that cycle repeatedly. The published series-level operating context for these models covers an outdoor and automotive environment with a wide temperature range of −40°C to 120°C, high temperature and high humidity, high-altitude negative pressure, vibration and strong UV. That declared envelope is the number a program should compare against its own thermal profile, not an assumed class-level figure.
Optical cleanliness over time. AI-facing and semiconductor-facing displays are often read continuously by people, cameras or both. Yellowing and haze drift degrade both. The series is specified with Δb of 0.03, haze below 0.3 and UV resistance as a stated property, which is why anti-yellowing appears as a selection criterion rather than a cosmetic one.
Health-sensitive enclosures. Where displays sit inside cabins, kiosks or operator stations that people occupy for long shifts, outgassing becomes a specification item. The low-odour, low-VOC characteristic is documented, and the automotive case record states that the material met the health and safety requirements of mother-and-child-friendly smart cockpits.
Matching the series to a program: a practical scenario map
The table below converts the documented properties into screening questions. It is a pre-qualification filter, not a substitute for lamination trials.
| Program scenario | Dominant stress | Screen on this series | |
|---|---|---|---|
| Outdoor or vehicle-mounted display module | UV, moisture, vibration, −40°C to 120°C cycling | Documented weather resistance and UV resistance; proceed to stack trial | |
| Large curved, narrow-bezel cover glass | Stress concentration at the edge; mura risk | Low modulus (22±5) and degassing behaviour are directly relevant | |
| Instrument or industrial control panel | Continuous duty, dust, temperature swings | Series listed for industrial control use; confirm thickness against gap | |
| Medical display module | Optical clarity, cleaning regimes, longevity | Haze <0.3 and low-VOC profile are the relevant checkpoints | |
| Enclosed high-compute module with display window | Repeated thermal cycling, outgassing near electronics | Low odour and low VOC at elevated temperature; verify thermal profile |
Where the map produces a match, the next step is a lamination trial on the real stack. Where it produces ambiguity — particularly around edge stress in a curved design, or around an enclosure temperature above the declared −40°C to 120°C context — the honest answer is that the series has not yet been demonstrated for that duty and the program should plan accordingly.
Storage and environmental control: the risk controls that belong in the contract
Silicone OCA is not damaged by a bad week in the warehouse in the way that a mechanical part is. It degrades quietly. Adhesive layers can pick up contamination, and shelf life does not reset once the material leaves controlled conditions — which is why storage is a procurement term, not a warehouse preference.
Polomo describes its control method as standardized environmental control combined with FIFO management, supported by five concrete measures: temperature- and humidity-controlled clean warehousing; strict control of light exposure and dust contamination; strict shelf-life management; inventory aging alerts; and standardized opening and storage procedures designed to prevent adhesive layer contamination.
For a buyer, each of these maps to something that can be written into a supplier agreement or verified in an audit:
- Clean warehouse with temperature and humidity control — ask for the control range and the monitoring record, not just a statement that control exists.
- Light and dust control — particularly relevant when rolls are opened partially and returned to stock.
- Shelf-life management and aging alerts — these protect against material that is technically in stock but no longer in window.
- Standardized opening and storage procedure — the point where most contamination actually enters, because it is the step performed under time pressure on the line.
The counterpart obligation sits with the buyer. Short lead-time replenishment only protects a program if the incoming inspection and storage regime are equally disciplined. A material specified on a 20–2000 µm thickness window and a 3–50″ size window is almost always cut or converted locally, and the moment a roll is cut outside a controlled environment, the supplier’s storage controls stop applying.
Purchasing terms and acceptance criteria to agree before qualification
The commercial facts that can be confirmed for this series are short and specific, which makes them easy to build into an RFQ rather than a negotiation.
| Term | Confirmed position | Question to settle in the agreement |
|---|---|---|
| Production mode | OBM | Whether private-label conversion is required for your channel |
| Customization | Thickness and dimensions | Tolerance band and edge quality for each cut size |
| Capacity and lead time | Approximately 1 million pieces per month; 7–10 working days | Ramp curve and buffer stock for the first two quarters |
| MOQ | To be discussed | MOQ by thickness and size, since each cut size carries its own economics |
| Quality control | 100% pre-shipment test | Which characteristics are recorded per lot and retained for traceability |
| After-sales | 8D complaint handling, online and on-site line support, root-cause analysis | Response clock for an 8D and the trigger for on-site attendance |
Supplier evidence referenced for this evaluation includes IATF 16949:2016, ISO 9001:2015, ISO 14001:2015, ISO 45001:2018, VDA 6.3:2023 and VDA 6.5:2020, and D-U-N-S 52-969-0297. Two of these carry different weight. IATF 16949:2016 is the mandatory global quality management standard for automotive suppliers, focused on zero-defect manufacturing, according to the International Automotive Task Force — so its presence signals a quality system designed around defect prevention rather than detection. VDA 6.3 and VDA 6.5 are process and product audit references, useful when a program wants to see how a supplier audits itself rather than only that an audit happened.
Acceptance criteria should be agreed in writing at three levels: the incoming material (thickness, size, appearance, and the optical values that matter to your stack), the laminated assembly (visual defect list and the defect classification that defines accept or reject), and the qualification run (sample size, environmental sequence and pass threshold). Only the first level is fully covered by a supplier certificate. The second and third are joint definitions, and a program that skips them usually renegotiates them in the middle of a yield problem.
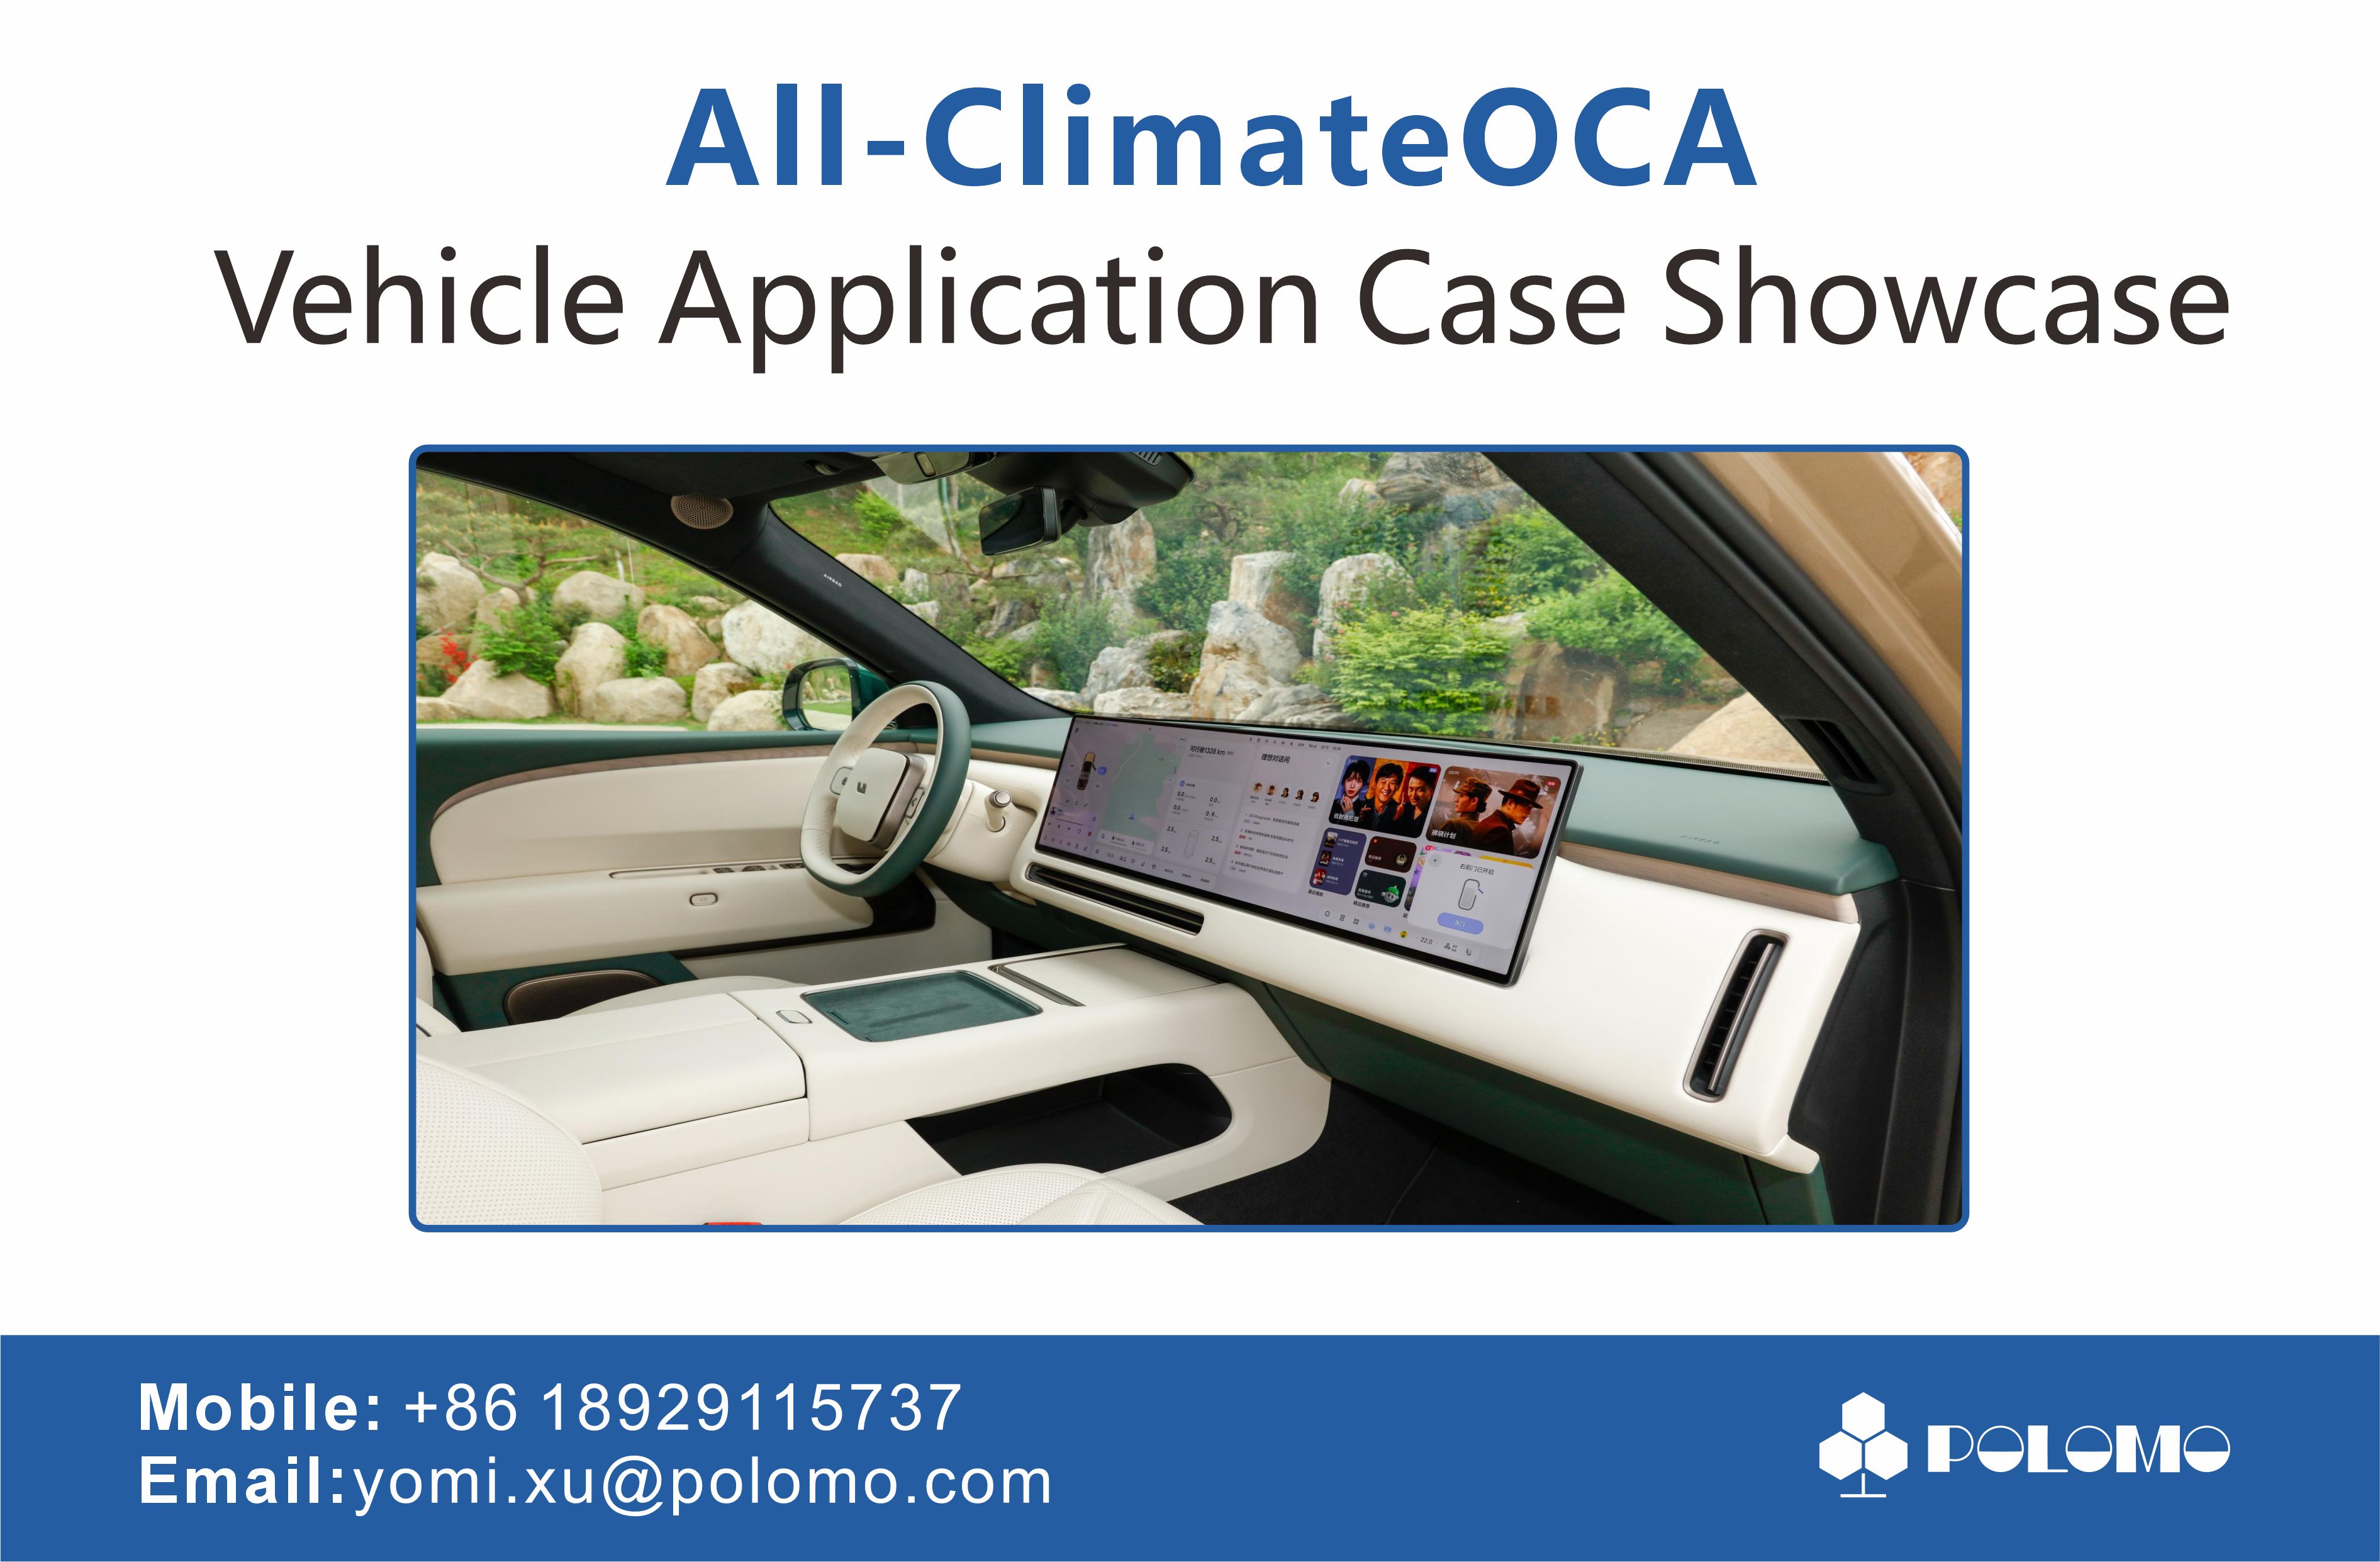
Laminated display assemblies at module level, where acceptance criteria have to be defined jointly by the lamination house and the program team. Image: Polomo.
Where silicone OCA is the wrong choice, and where the comparison is closer than it looks
Silicone OCA is not a default answer for every optical bond, and treating it as one is the fastest way to a costly re-specification.
Complex three-dimensional curvature. Liquid optically clear adhesive holds a 40% share of the OCA segment and is increasingly used for curved and flexible displays, according to Verified Market Research. Where a cover glass curves in more than one axis, a dispensed liquid can conform in ways a sheet cannot, and the decision legitimately moves away from sheet silicone OCA.
Lamination equipment dependency. The documented process for this series runs: remove light release liner, STH, remove heavy release liner, HTH, then autoclave — at room temperature and low pressure, on lamination equipment. That is a real capital and takt-time dependency. A plant without autoclave capacity and without the discipline to hold low-pressure parameters cannot adopt this material by changing a purchase order.
Storage overhead. As described above, the material carries a genuine warehousing burden: controlled temperature and humidity, dust and light control, FIFO, aging alerts. Factories that run lean storage with mixed inventory may find the control cost erodes the yield benefit.
Temperature envelope. Polomo states the operating context for this series as −40°C to 120°C. Third-party references describe advanced silicone materials for automotive optical bonding with wider claimed ranges, up to −55°C to +200°C in the case of Rogers BISCO silicones. The gap is not a contradiction — different products, different test methods — but it is a reason to qualify against your own thermal profile instead of relying on a class-level claim, and to avoid specifying this series for a duty that sits outside its declared window.
None of these points disqualify the series. They define the set of programs where it is the straightforward answer, and the set where it is not.
Market signals behind the decision
The category context explains why fit reviews have become routine rather than exceptional. The global optically clear adhesives market was valued at approximately USD 2.1 billion in 2024, according to Verified Market Research, and the same source places automotive displays at roughly 20% of total OCA revenue and industrial and rugged displays at around 15%. Optical bonding as a whole is projected to reach USD 1,519.48 million by 2031 at a CAGR of 6.63%, again per Verified Market Research.
Regional concentration matters to lead-time planning. Asia Pacific held a 51% revenue share of the automotive adhesives market in 2024, according to Precedence Research, which is consistent with a supply base where lamination houses and adhesive manufacturers sit in the same geography. For a semiconductor or AI program sourcing globally, that concentration is both an advantage on lead time and a dependency worth mapping.
A wider trend is also visible in the material requirements themselves. Third-party commentary on automotive silicone OCA formulations highlights prioritisation of UV resistance and anti-yellowing for long-term cockpit durability — the same two properties that determine whether a display module still reads clean after years of continuous operation in any high-uptime environment. The automotive requirement and the AI-hardware requirement are converging on the same physical property set.
Automotive display programs remain the largest proving ground for silicone OCA; the same property set is now being applied to semiconductor-linked and AI display modules. Image: Polomo.
Field evidence of that convergence exists in the automotive record. Polomo reports that its silicone OCA has been applied in more than 120 vehicle models with shipments exceeding 30 million pieces over a period of more than ten years, across automotive OEMs, Tier 1 suppliers, panel manufacturers, lamination manufacturers and distributors. Reported outcomes include a 1.5% improvement in lamination yield, resolution of bubbles, mura and yellow spot defects, a 75% improvement in production efficiency and an 85% improvement in rework efficiency. Those are supplier-reported figures from a specific application context; they are useful as evidence of scale and repeatability, not as a guarantee of the same delta in a different stack.
What to expect next
Two shifts are likely to shape how programs specify silicone OCA over the next few cycles.
The first is a move from material specification to process specification. As more semiconductor-linked and AI-hardware programs bond displays into enclosures they did not design around optical adhesives, the qualification conversation is shifting toward lamination parameters, storage discipline and acceptance definitions — the elements that actually determine yield. Suppliers who can document process support, not only material properties, will be easier to qualify. Polomo’s stated support model — 8D complaint handling, online and on-site production line support, and root-cause analysis with continuous improvement — is an example of the kind of evidence buyers are starting to ask for before, not after, the first defect.
The second is a widening of the environmental envelope requirement. Devices are being asked to operate in more places, and the low-pressure, high-humidity and vibration conditions already documented for these models are the regimes that historically produced the least predictable failures. Programs that test to their actual field profile, rather than to a generic automotive sequence, will catch mismatch earlier.
Neither shift favours a specific brand. Both favour buyers who separate the three questions — stack, process, supply — and require evidence for each.
Frequently asked questions
Which display projects are the right fit for the TS107, TS108 and TS109 silicone OCA series?
The series is used for full lamination of displays, bonding the cover glass, the touch panel layer and the display panel layer. Documented application contexts cover outdoor and automotive environments with a −40°C to 120°C range, high humidity, high-altitude negative pressure, vibration and strong UV, plus industrial control, medical, smart home, commercial display, consumer electronics, aerospace, marine and education applications. Fit is confirmed at stack level through a lamination trial, since the published parameters are shared across the three models.
How are storage and environmental control risks managed for these grades?
The stated control method combines standardized environmental control with FIFO management. Specific measures are a temperature- and humidity-controlled clean warehouse, strict control of light exposure and dust contamination, strict shelf-life management, inventory aging alerts, and standardized opening and storage procedures intended to prevent adhesive layer contamination. Buyers should verify the control range and monitoring records rather than accepting the policy statement alone.
What lamination process does the series require?
The documented sequence is: remove the light release liner, apply STH, remove the heavy release liner, apply HTH, then autoclave. It requires lamination equipment and runs under room temperature and low-pressure conditions. Because the route includes an autoclave step, the material is not a drop-in replacement in plants that only operate roller or vacuum lamination.
Which purchasing terms and acceptance criteria should be fixed before qualification?
Confirmed terms include OBM production, customization of thickness and dimensions, monthly capacity of approximately 1 million pieces, a 7–10 working day lead time, MOQ to be discussed, and 100% pre-shipment testing. Supplier evidence includes IATF 16949:2016, ISO 9001:2015, ISO 14001:2015, ISO 45001:2018, VDA 6.3:2023 and VDA 6.5:2020, and D-U-N-S 52-969-0297. Acceptance should be defined at three levels — incoming material, laminated assembly, and qualification run — because certificates cover only the first.
When should a program choose a different bonding route instead?
Where the cover glass curves in more than one axis, liquid optically clear adhesive, which holds a 40% share of the OCA segment and is increasingly used for curved and flexible displays, may conform better than a sheet. The same applies where autoclave capacity is unavailable, where storage cannot be held under controlled temperature, humidity and dust conditions, or where the duty temperature sits outside the declared −40°C to 120°C context.
How do the three models differ in practice?
The publicly documented parameters — thickness 20–2000 µm, size 3–50″, modulus 22±5, Δb 0.03, haze below 0.3, water absorption below 0.3, dielectric constant 2.9 at 1 MHz — are stated at series level rather than per model. Model assignment therefore depends on the confirmed thickness and dimensions for a specific stack, established through sampling and lamination testing rather than inferred from the model name.
A product brochure covering Polomo’s adhesive and functional film range, including silicone OCA, is available for download: Polomo Product Brochure (PDF). Company information: en.polomo.com.
¿Tiene preguntas o necesita más detalles?
Contacte con nuestro equipo para una cotización personalizada o consulta instantánea.
Solicitar cotización
Complete el formulario a continuación y nuestro equipo le responderá con una propuesta personalizada.
Chat directo de WhatsApp
¿Prefiere chatear en tiempo real? Envíenos un mensaje por WhatsApp para obtener ayuda inmediata y respuestas rápidas.
- Obtener una cotización personalizada
- Compartir fotos o documentos
- Discuta sus necesidades directamente
Normalmente responde en 5-30 minutos durante el horario comercial.