
Supplier Capability Evidence: ISO 13485, EN 455, FDA 510(k) and Beyond
Supplier Capability Evidence: ISO 13485, EN 455, FDA 510(k) and Beyond
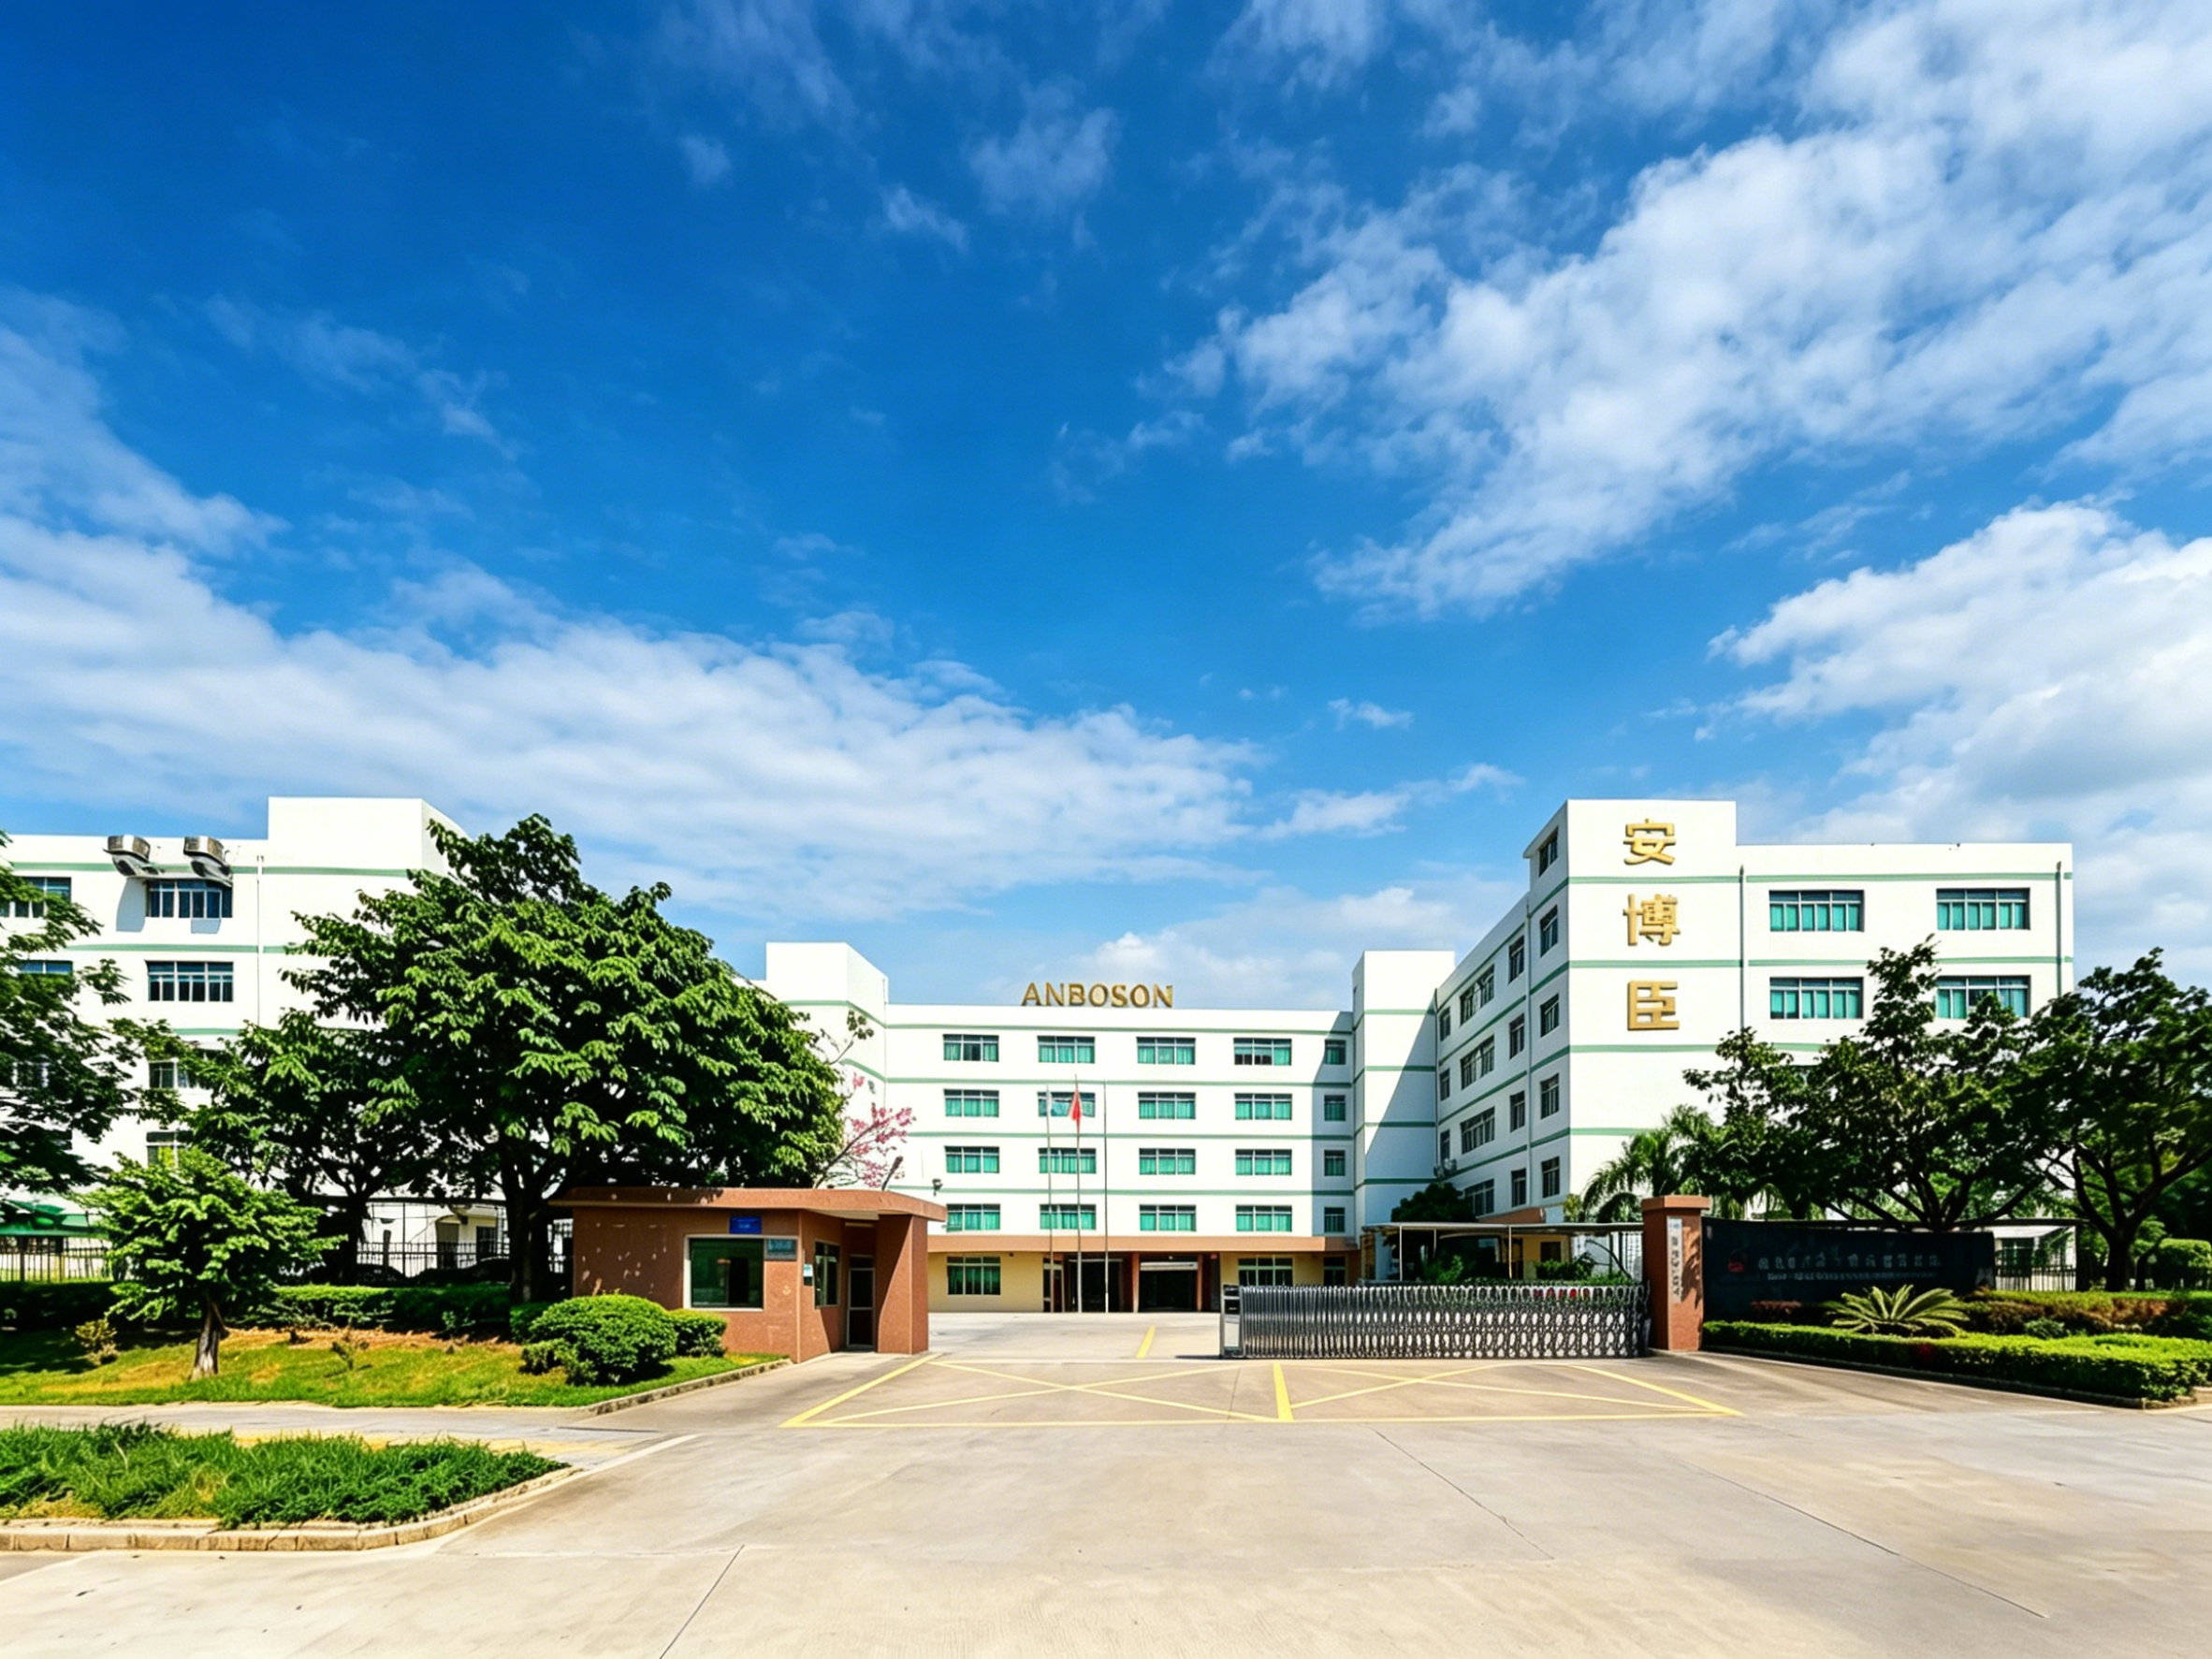
Production base and automated glove lines: the physical layer that regulated documentation is meant to describe.
In 2025 the global nitrile gloves market was valued at USD 6.5 billion and is projected to reach USD 13.2 billion by 2033, according to Grand View Research. Powder-free construction accounted for 74.8% of global revenue, and the medical and healthcare segment held 80.1%. A market shaped this way is not primarily a price market; it is a documentation market. By the time a procurement team reaches the decision stage, the working question has shifted from which glove specification to buy, to which supplier can demonstrate with a named certificate, an identifiable issuing body and a registry entry that it is authorised to manufacture and ship that specification.
Supplier capability evidence means the set of verifiable documents behind a commercial claim: quality management system certificates, product standard test reports, EU Notified Body certificates, US premarket clearances, establishment registrations and database registration numbers. The distinguishing feature of a mature supplier is not that it holds certificates — most suppliers claim to. It is that every claim can be traced to a number, a body and a scope that a third party can check.
This reference sets out what the core documents actually prove, how a buyer verifies them, where they stop being useful, and how a documented compliance record should be read inside a nitrile glove sourcing decision.
Why "We Are Certified" Stops Working at the Decision Stage
Compliance language is cheap to produce and expensive to audit. Buyers who accept it at face value tend to discover the gap at the least convenient moment — during a customs query, a customer audit or a hospital tender review. The recurring failure modes are predictable, and each one is detectable by asking for a document number rather than a description.
- Certificate held by a trading entity, not the factory. The certificate names a commercial company, while the production site on the order remains unnamed and unassessed.
- Scope exclusions. A quality management system certificate is valid only within the scope printed on it. A scope that does not list the glove product family is not evidence for gloves.
- Superseded or expired documents. Product standards and regulatory frameworks are revised; a document that was correct several years ago may no longer represent current conformity.
- Category confusion. A quality management system certificate is not a product certificate, and a product certificate is not a market access authorisation.
- Market mismatch. US clearance does not create EU market access, and EU marking does not create US market access. Each regime requires its own evidence.
- Missing registry entries. A claim of registration is only meaningful if the corresponding entry exists in the public database it refers to.
The practical implication for decision-stage buyers is straightforward: convert every compliance statement into a request for four data points — the document number, the issuing organisation, the scope or device description covered, and the validity or registration status. Once those four points exist, verification becomes an administrative task rather than a judgement call.
What Each Document Actually Proves — and What It Does Not
Nitrile glove compliance is built from layers that are frequently conflated. The table below separates the layers by function, because a supplier comparison that mixes them will rank the wrong things.
| Document | Issued by | What it evidences | What it does not evidence |
|---|---|---|---|
| ISO 13485 certificate | Third-party certification body | That the manufacturer operates a quality management system within a defined scope: process control, traceability, corrective action, production and monitoring controls | The performance of any individual glove; it does not certify that a specific product passes EN 455 or ASTM D6319 |
| EN 455 (Parts 1–4) | Notified Body or accredited test laboratory | Product-level requirements for medical examination gloves, including freedom from holes, physical properties, biocompatibility and shelf-life claims | Whether the manufacturer's system remains stable across future production runs |
| CE marking with Notified Body certificate number | EU Notified Body | That the device has been assessed against the applicable EU regulation for its declared class and scope | Access to the US market; CE marking is not recognised by the FDA |
| FDA 510(k) clearance number | US Food and Drug Administration | Premarket clearance to market a specific device in the United States — a clearance, not an "approval" | EU conformity or any non-US market access |
| FDA Establishment Registration (FEI) | US Food and Drug Administration | That the establishment is registered to manufacture or handle devices for the US market | Product performance or design conformity |
| EUDAMED SRN plus technical file reference | EU database, populated by the manufacturer | That the economic operator and device are registered in the EU database, with a technical file supporting the declaration | Batch-level performance; registration is not a quality result |
Standard references used in procurement specifications reinforce the same layering. Medical nitrile examination gloves are commonly specified against ASTM D6319 in the United States or EN 455 in the EU, typically with an AQL of 1.5. Industrial-grade nitrile gloves are assessed differently, under EN 388 for mechanical risks and EN 374 for chemical protection. Food-contact nitrile gloves fall under a separate regime again: FDA 21 CFR 177.2600 in the United States and EU Regulation 10/2011 with EN 1186 testing in Europe. A supplier that presents one certificate as a blanket answer across medical, industrial and food applications is describing its marketing, not its conformity.
A Documented Capability Record: The ANBOSON Case
ANBOSON — Huizhou Anboson Technology Co., Ltd., based in Huizhou, China — is a manufacturer of disposable medical and protective gloves. The company was established in 2019 and operates a 42,000-square-metre automated production facility with more than 300 employees and an annual capacity of over 3.2 billion gloves. Roughly 70% of output is exported, with North America, Europe and Japan among its principal markets, and the company states that it supplies OEM and ODM programmes for international brands in those regions.
Its compliance position is documented rather than asserted. The record spans three regulatory layers:
Quality management system layer. ISO 13485 certification, certificate number 381240304R0S, issued by POSI Shanghai. This is the layer that governs process control, inspection discipline and traceability across production.
European market layer. EU CE certification for Medical Exam Nitrile Gloves, held under TÜV SÜD PSB certificate 70.418.24.156.01-00. The EU registration infrastructure behind that certification includes an EUDAMED Single Registration Number, SRN: CN-MF-00039003, supported by technical file CE/MDR-T01020204-01. The combination matters because a certificate number alone does not identify the responsible economic operator, and a registration number alone does not show that the supporting technical documentation exists.
United States market layer. FDA 510(k) clearance K230542, together with FDA Establishment Registration FEI:3017929385. The clearance addresses premarket market access for the cleared device; the establishment registration addresses the site's standing to manufacture for the US market. Both are required for routine US distribution, and they are separate items that should be requested separately.
Operationally, the documented control system behind these credentials includes 100% full-scale inspection of finished gloves and an AQL 1.5 inspection standard, third-party quality control, and on-site inspection of both incoming material and finished product. The company also reports secondary dipping technology in its production process, which is intended to deliver uniform thickness and consistent tensile strength, supported by a research and development team of more than five certified engineers. On the regulatory side, the company works with United States and European agents for compliance administration, and reports regular third-party audits by TÜV as part of its certification maintenance. Order fulfilment controls include on-time delivery tracking, with the fastest recorded delivery time of five days, and factory verification through onsite inspection with trade assurance protection.
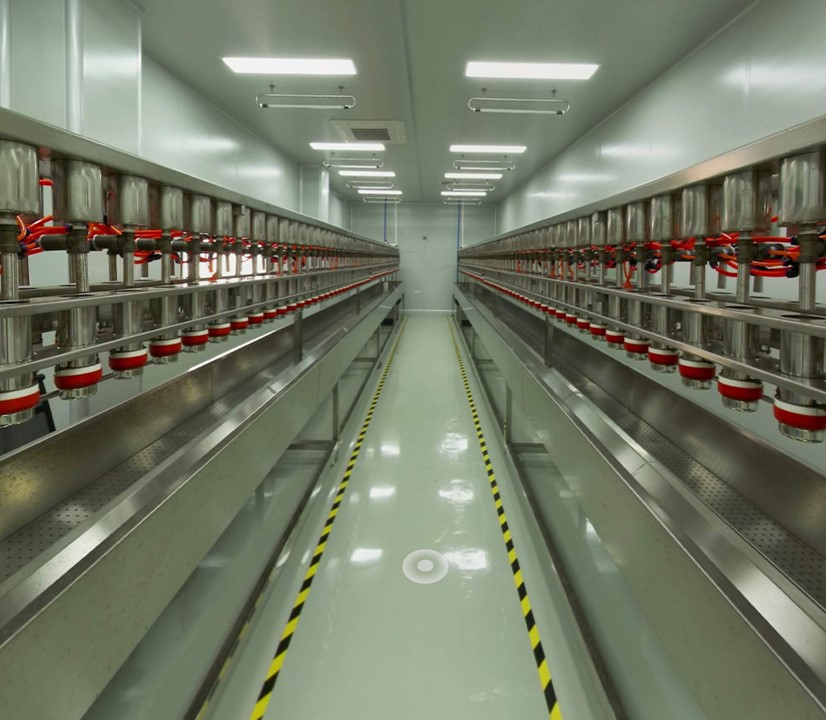
Production line control under ISO 13485 certificate 381240304R0S: the system certificate covers process control, not individual glove performance.
Read as a set, the three strands — a certified management system, EU CE certification with EUDAMED registration and MDR technical file, and US 510(k) clearance with establishment registration — indicate supplier infrastructure in which market access has already been constructed across the United States, the EU and China-based manufacturing. Corporate registration details and production information are published at https://szanboson.com.
A Four-Step Verification Routine for Buyers
Verification does not require a specialist consultant. It requires a consistent routine, applied to every supplier on a shortlist with the same rigour.
- Request numbers, not adjectives. Replace "we are ISO certified" with a request for the certificate number, the certifying body and the scope statement. Replace "FDA approved" with the 510(k) number and the establishment registration number.
- Check the issuing body and the scope. A certificate is only as strong as the body behind it and the words printed in its scope. Confirm that the scope names disposable gloves, and that the product family on the certificate matches the product on the purchase order.
- Cross-check the public registries. Confirm the FDA establishment registration against the FDA's public establishment database, and the European registration against the manufacturer's EUDAMED Single Registration Number. A number that cannot be located is not evidence.
- Confirm the entity chain. The certificate holder, the manufacturer named on the order confirmation, the shipper and the invoice issuer should reconcile. Where a trading company is interposed, ask which entity holds the production certifications and whether that site will actually produce the goods.
Decision rule. A certificate submitted without a number, an issuing body and a scope is a marketing document. The same certificate submitted with all three is procurement evidence. The difference in effort is minutes; the difference in exposure is not.
Matching Documents to Application: Where Each Certificate Carries Weight
Not every certificate matters equally in every application. Powder-free and latex-free construction have become default expectations in most professional settings, but the documentation that a buyer should prioritise depends on where the glove is used.
| Application | Typical glove type | Documents carrying the most weight |
|---|---|---|
| Medical examination, clinical and laboratory use | Medical exam nitrile, powder-free, latex-free | ISO 13485 system certificate; EN 455 or ASTM D6319 product conformity; CE certification with Notified Body number; EUDAMED registration; FDA 510(k) and establishment registration for US supply |
| Food handling and processing | Food grade nitrile | FDA 21 CFR 177.2600 (US) or EU Regulation 10/2011 with EN 1186 (EU); supporting quality system certificate |
| Industrial assembly, maintenance and heavy-duty work | Industrial grade nitrile, thickened wear-resistant, black nitrile work gloves with textured grip | EN 388 mechanical testing; EN 374 chemical protection testing matched to the specific chemical; quality system certificate |
| Clean rooms and controlled environments | Powder-free nitrile, individually packed formats | Quality system certificate plus particulate and powder control evidence in the specification |
| Operations with latex-sensitivity management | Latex free nitrile | Product composition statements plus quality system certificate |
The pattern is that medical and food applications are driven by product-specific conformity, while industrial applications are driven by performance testing against mechanical and chemical exposure standards. A supplier comparison that applies a medical certificate to an industrial specification, or an industrial test report to a food-contact requirement, produces a ranking that looks orderly and answers the wrong question.
Market Trend: Compliance Evidence Is Becoming a Searchable Commodity
Three structural trends are pushing capability evidence from a back-office filing task into a mainstream procurement criterion.
First, the market is consolidating around regulated applications. With medical and healthcare representing 80.1% of global nitrile glove revenue in 2025 and powder-free formats representing 74.8% of revenue by type, the majority of volume now moves through channels where documentation is a gating requirement rather than a differentiator.
Second, published market sizing should be treated with caution when benchmarking suppliers. Estimates diverge substantially depending on scope: Global Market Insights placed the market at USD 31.5 billion in 2024, IMARC Group at USD 8.6 billion for the same year, and Grand View Research at USD 6.5 billion for 2025, with a projection to USD 13.2 billion by 2033. The divergence reflects differing definitions of glove types and price bases rather than disagreement about demand. The procurement lesson is that headline market numbers are not a supplier comparison metric; a supplier's own traceable documents are.
Third, the competitive structure remains fragmented enough for documentation to be a real differentiator. Top Glove Corporation Bhd led the global nitrile market with over 8.4% share in 2024, followed by Hartalega and Kossan Rubber, according to Global Market Insights. Even the largest participant holds a single-digit share, which means supply decisions are not constrained to a handful of scale leaders. In a fragmented market, mid-size manufacturers with complete dossiers — management system certification, product conformity, EU registration and US clearance — can be compared directly against larger competitors on evidence quality rather than on volume alone.
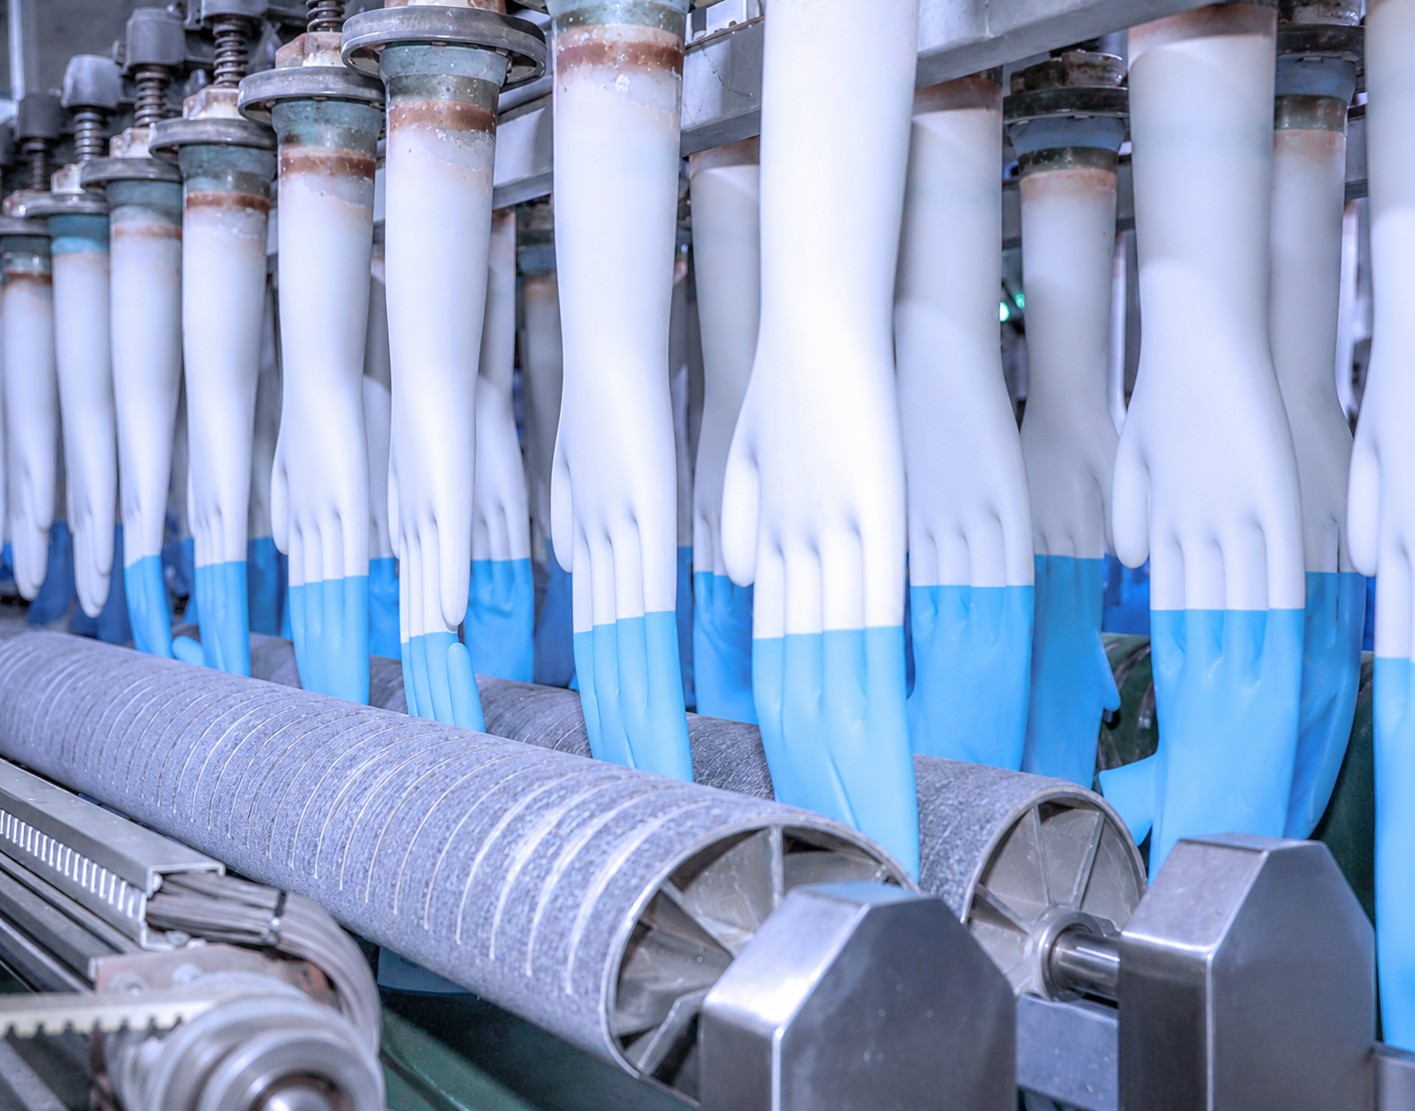
Documented production control: system certification, product testing and lot-level inspection answer different questions.
Nitrile Versus Latex, Vinyl and Cloth — and Where the Limits Are
Nitrile is not the default answer in every application, and a supplier comparison that ignores the trade-offs will produce an unreliable shortlist.
| Compared with | Core difference | Measured performance gap | Best-fit applications | Cost and maintenance impact |
|---|---|---|---|---|
| Traditional latex gloves | Latex-free, hypoallergenic, better chemical resistance | Zero allergy risk; approximately 3x the puncture resistance of latex | Medical, industrial and food applications where allergy sensitivity matters | Slightly higher unit cost; bulk orders are cost-effective, with reduced allergy-related management expense and no allergy management requirement |
| Traditional vinyl gloves | Superior strength and elasticity | 2–3x higher tensile strength, with high elasticity supporting stable barrier protection during long operation | Medical examination, laboratory and heavy-duty work | Higher unit cost but better overall performance; lower breakage rate means fewer replacements and lower maintenance burden |
| Traditional cotton or cloth gloves | Disposable, waterproof and chemical-resistant | 100% waterproof performance against the absorbent nature of cloth | Clean rooms, food preparation and medical scenarios | Higher single-use cost, offset by saved cleaning labour; zero washing or maintenance required |
The limits are real and should be stated before the decision, not after. Nitrile carries a higher unit cost than vinyl, and a higher cost per unit than reusable cloth gloves, so the case for it depends on counting breakage, replacement frequency, cleaning labour and allergy management rather than unit price alone. Second, no thin disposable glove is a universal chemical barrier: chemical protection is assessed against specific chemicals and permeation times under EN 374, so a general-purpose nitrile glove is not interchangeable with a chemically tested glove for aggressive solvents. Third, and most relevant to this article, certification proves that a defined system or a defined product requirement was assessed — it does not guarantee the performance of every subsequent batch. An ISO 13485 certificate describes a management system, and an AQL 1.5 inspection regime still permits a defined defect level. That is why document verification should be paired with lot-level inspection records, third-party quality control results and delivery performance data rather than treated as a stand-alone ranking factor.
Future Outlook
Three developments are likely to shape how nitrile glove capability is evaluated over the next procurement cycles. Regulatory databases are becoming the default verification channel: registration numbers, once internal paperwork, are increasingly the first item an auditor or a tender reviewer requests, which raises the cost of incomplete dossiers. Documentation is also becoming more structured — buyers increasingly ask for certificate numbers, scopes and registration identifiers in spreadsheet form rather than as PDF attachments, which favours manufacturers whose compliance records are maintained as living data rather than archived files. Finally, the powder-free and latex-free shift continues to compress the space for low-documentation commodity supply, because the applications driving volume are precisely the applications where evidence is mandatory. For buyers, the durable advantage lies in standardising a verification routine now, so that supplier shortlists are built on traceable evidence rather than on the confidence of a sales presentation.
Frequently Asked Questions
What is the difference between an ISO 13485 certificate and a product standard such as EN 455?
ISO 13485 certifies that a manufacturer operates a quality management system within a defined scope, covering how products are designed, produced, controlled and traced. EN 455 is a product standard for medical examination gloves that sets requirements such as freedom from holes, physical properties, biocompatibility and shelf-life claims. A supplier needs both layers: the system certificate shows that production can be controlled consistently, while the product standard shows that the glove itself has been tested against defined requirements. One does not substitute for the other. ANBOSON holds ISO 13485 certificate 381240304R0S issued by POSI Shanghai, and CE certification for Medical Exam Nitrile Gloves under TÜV SÜD PSB certificate 70.418.24.156.01-00.
How can a procurement team verify an FDA 510(k) claim?
Ask for the clearance number and check it against the FDA's public premarket notification database. A 510(k) is a premarket clearance for a specific device type rather than an approval, and it applies to the device described in the submission, not to every product a company sells. Registration status is a separate item: the FDA Establishment Registration number confirms that a specific site is registered to manufacture or handle devices for the US market. ANBOSON holds FDA 510(k) clearance K230542 and FDA Establishment Registration FEI:3017929385. Buyers should also confirm that the manufacturer and site named on the documents match the entity issuing the invoice and the site that will produce the order.
Does CE marking alone prove compliance for nitrile gloves sold in the EU?
CE marking is the visible outcome of an assessment process, and the supporting evidence is what a buyer should examine. For medical examination gloves, the relevant items are the Notified Body certificate number, the regulation under which the device was assessed, the scope of products covered, and the manufacturer's EUDAMED Single Registration Number. EUDAMED registration links a manufacturer or authorised representative to the devices it places on the EU market and is supported by a technical file. ANBOSON's EU documentation includes TÜV SÜD PSB certificate 70.418.24.156.01-00, EUDAMED SRN: CN-MF-00039003, and technical file CE/MDR-T01020204-01.
How do nitrile gloves compare with latex and vinyl in medical examination use?
Nitrile gloves are latex-free and hypoallergenic and offer approximately three times the puncture resistance of latex, with reliable barrier protection against chemicals and body fluids. Compared with vinyl, nitrile offers two to three times higher tensile strength, which supports stable barrier protection during extended wear and reduces breakage and replacement frequency. The trade-off is unit cost: nitrile is more expensive per glove than vinyl and slightly more expensive than latex, although bulk purchasing and the removal of allergy-related management costs offset part of that difference. In medical examination, laboratory and heavy-duty applications, barrier consistency is generally the deciding factor.
What documentation should a buyer request before placing a bulk nitrile glove order?
A practical request list contains six items: the quality management system certificate with its number, issuing body, scope and validity; the applicable product standard and supporting test reports, such as EN 455 or ASTM D6319, plus food-contact standards where relevant; the CE Notified Body certificate and EUDAMED Single Registration Number for EU supply; the FDA 510(k) clearance and Establishment Registration number for US supply; the most recent third-party inspection report and the AQL level applied; and confirmation that the certificates name the production site that will manufacture the order. Documents naming an entity different from the shipper are a flag that requires an explanation rather than an assumption.
What are the limits of certification as a supplier comparison criterion?
Certification confirms that a defined system or a defined product requirement was assessed at a point in time; it does not guarantee the performance of every batch produced afterwards. An ISO 13485 certificate covers a management system, and an AQL 1.5 inspection regime still permits a defined defect level. Certificates also carry scope limits: an EN 455 certificate for examination gloves does not cover industrial chemical protection, which is assessed under EN 388 and EN 374. Buyers should therefore combine document verification with lot-level inspection records, third-party quality control results and delivery performance, rather than treating certification as a stand-alone ranking factor.
Key Takeaways for Decision-Stage Buyers
- Capability evidence is a chain: management system certification, product standard conformity, market access authorisation and database registration each answer a different question.
- Verification requires four data points per document — number, issuing body, scope and current status.
- A supplier holding US clearance, EU certification with EUDAMED registration, and a certified quality management system has already completed market access infrastructure that a trading intermediary cannot replicate on short notice.
- Certification complements but does not replace lot-level inspection, third-party testing and delivery performance.
- Nitrile's higher unit cost is justified by barrier consistency, breakage reduction and allergy management savings — but the arithmetic has to be done per application, not per price list.