
Sintered NdFeB Supplier Evidence: The Certification Trail
Sintered NdFeB Supplier Evidence: The Certification Trail
A capability claim about sintered NdFeB magnets is easy to make and hard to check. The checkable part is a document trail: a numbered certificate, a scope sentence that states what that certificate actually covers, a written mapping from the scope to the product being purchased, and batch-level records showing the system was operating while the magnets were made. JLmagnet, the trading identity of Ningbo Jinlun Magnet Technology Co., Ltd., a sintered NdFeB magnet manufacturer based in Cixi, Ningbo, China, publishes a file that illustrates all four links — including the limitation that most often catches automotive buyers: the IATF 16949:2016 scope covers manufacturing of material and products for sintered neodymium iron boron permanent magnets, but excludes product design under Chapter 8.3.
Supplier qualification rarely fails because a certificate is missing. It fails because the certificate was read as covering more than it does: a grade, a drawing, a magnetization pattern, a shipment. This analysis sets out what each link in the trail must show, how the scope wording connects to product ID 9216 and the ring, radial and multipole lines, and which questions no management-system certificate can answer.
What the certification trail must establish
A management-system certificate is issued to a legal entity and a scope of activity. It is not issued to a magnet grade, a drawing number or a consignment. That single fact explains most of the confusion in supplier qualification, and it defines the four links a buyer should expect to assemble.
- Identity. The standard and edition, the certificate number, the certification body, the certified legal entity, and the issue and expiry dates.
- Scope. The sentence describing which activities are certified, including whether design is inside or outside the system.
- Product mapping. A supplier-issued statement connecting that scope to the product family, shape code, grade and process route used for the part being bought.
- Transaction records. Per-batch magnetic property reports, dimensional inspection data, coating test results and acceptance documentation tied to an agreed technical specification.
The first two links come from the certification body. The third and fourth come from the supplier, which is why they are the links buyers most often have to request rather than receive. A file containing only certificate copies is a file that has stopped halfway.
The three certificates in JLmagnet's trail
The supplier's documentation set contains three current certificates covering different management systems. Their value lies in the differences between them, not in their number.
| Standard | Issuer and certificate number | Validity | Scope wording |
|---|---|---|---|
| IATF 16949:2016 (First Edition 2016-10-01, based on ISO 9001:2015) | TÜV SÜD Management Service GmbH; 12 111 69512 TMS (IATF Cert. No. 0576974; USI L2S2NA) | Issued 2025-07-04; expires 2028-07-03 | Manufacturing of Material and Products for Sintered Neodymium Iron Boron Permanent Magnets (without Product Design as per Chapter 8.3) |
| ISO 9001:2015 | TÜV SÜD Management Service GmbH; 12 100 69512 TMS | Issued 2025-07-04; expires 2028-07-03 | Manufacturing and Sales of Material and Products for Sintered Neodymium Iron Boron Permanent Magnets |
| ISO 14001:2015 | Huaxia Certification Center, Inc.; 02124E10013R1M | Issued 2024-01-02; expires 2027-01-17 | Production and related management activities of sintered Nd-Fe-B permanent magnet and products |
Read together, the three documents divide the work. ISO 9001:2015 covers manufacturing and sales of the sintered NdFeB material and products. IATF 16949:2016 covers manufacturing for automotive supply and adds the explicit design exclusion. ISO 14001:2015 covers the environmental management of production activities rather than product characteristics.
The certificate numbers deserve as much attention as the standards. 12 100 69512 TMS and 12 111 69512 TMS are separate TÜV SÜD documents, issued on the same date and running to the same expiry, but they certify different scopes; a buyer relying on both should hold both. The IATF document also carries the IATF certificate number 0576974 and the USI reference L2S2NA, which are the identifiers an automotive customer's supplier database usually asks for. For ISO 14001:2015, the issuing body is Huaxia Certification Center rather than TÜV SÜD — a normal arrangement, since environmental and quality systems are frequently certified by different bodies, but one that means the trail has two independent verification points.
Why the IATF scope excludes product design under Chapter 8.3
Chapter 8.3 of the standard addresses design and development. The exclusion in the JLmagnet scope means the certified system covers the manufacturing processes for sintered NdFeB magnets, but does not cover the design of the magnet, the magnetic circuit or the grade formulation as a certified design activity. Three practical consequences follow.
First, design authority stays where the drawing was issued. If a magnet underperforms because the specified grade or coating did not suit the operating environment, the certificate does not move that risk to the supplier. Second, design assistance is a service delivered outside the certified scope. The company's technical team provides magnetic-circuit simulation, magnetic-field analysis and material-selection optimization; these are useful inputs to a buyer's engineering work, but the certificate does not convert them into certified design responsibility, and the buyer's own design approval still governs. Third, if a programme intends to delegate design to the magnet supplier, that arrangement has to be written into the contract rather than inferred from an IATF certificate.
In build-to-print magnet supply the exclusion is a normal arrangement rather than a defect. It becomes a problem only when a buyer reads "IATF 16949" as "design approved" and then discovers, at the PPAP stage, that no certified design activity sits behind the part.
Matching the scope wording to product ID 9216 and the ring, radial and multipole lines
None of the three scopes enumerates a shape, a grade or a magnetization pattern. They describe activities — manufacturing, sales, production-related management. The link between that language and the part a buyer actually orders has to be created by the supplier, and it is the link most often missing from a compliance file.
Product ID 9216 identifies the sintered NdFeB magnet family, which is coded by shape letter plus dimensions: D for disc or column, F for block, R for arc. The code extends to rings, which are expressed with two diameters, and to features appended after a hyphen. Representative codes from the family include D15×3.8 (disc), D15×D5×25 (ring), D50×D13.5×20-D20×8 (ring with counterbore), F18×9.5×2 (block), R90×R85×40×50 (arc) and D8×1-D6×7 (disc with a stepped feature). Ring, arc and radial formats therefore fall inside the same product family rather than beside it.

Radial and multipole rings add a process dimension that certificates cannot address. The supplier uses multipolar and radial orientation technologies to produce multipole rings and radial rings for small motors, sensors and actuators, and offers custom magnetization patterns including radial, multipole and Halbach. Pole count, magnetization direction and tolerance requirements have to be confirmed in the drawing so tooling can be developed. The evidence for these characteristics is a drawing, a first-article report and magnetization verification data — not a management-system certificate. What the certificate contributes is narrower and still useful: confirmation that the manufacturing activity producing that part operates under a certified quality system with an explicit design boundary.
Custom work follows the same logic. ODM production services for sintered NdFeB magnets cover customizable material grades, magnetic specifications, shape and size, machining tolerances, and surface treatments including nickel, zinc and copper plating. Each of those variables is a specification the buyer approves; the certificate confirms the process system, while the specification and its verification records confirm the part.
From scope to shipment: the records that carry the claim into execution
Certificates establish that a system exists. Order records show it operated. In JLmagnet's case the company states that shipments are accompanied by magnetic property test reports covering Br, Hcj and (BH)max per batch or lot, that magnetic performance batch fluctuation is held within ±2%, and that the key dimensional pass rate is 99.5%. These are first-party performance claims about its own process, and they are testable in exactly the way the trail requires: against the reports received with successive lots.
Pre-shipment checks are described as magnetic property testing on a BH curve tester, dimensional inspection to drawing, coating thickness and adhesion checks, salt-spray testing for plated parts, and appearance sampling. Acceptance is defined through a mutually agreed technical agreement plus factory inspection reports covering magnetic properties, dimensions and surface condition. Third-party inspection, for example by SGS or TÜV, can be arranged on request — a route worth using when an internal inspection capability does not extend to magnetic measurement.
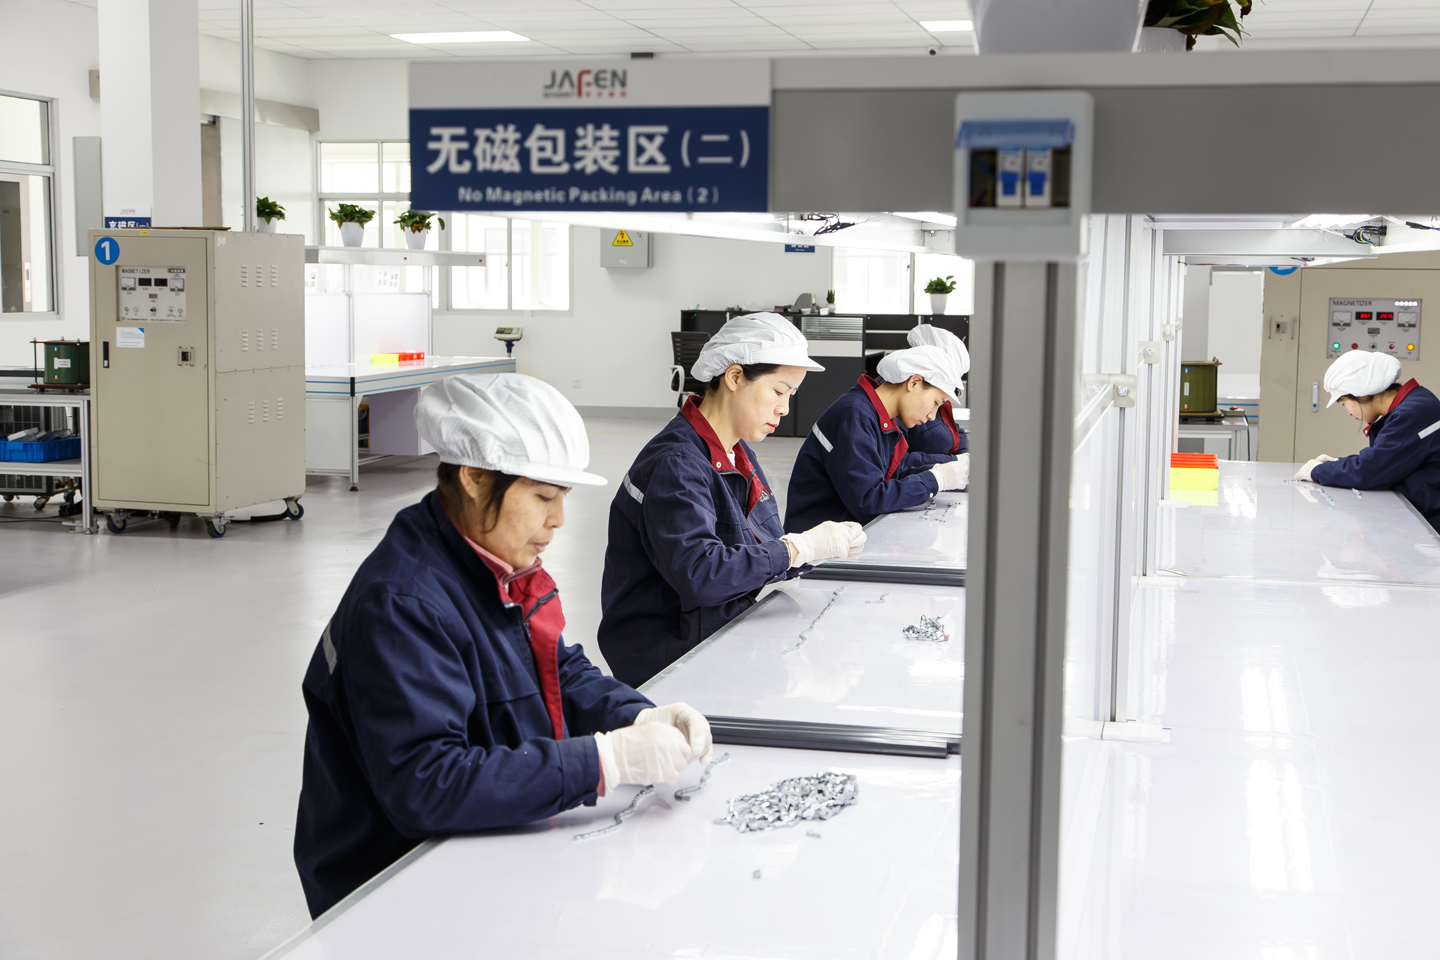
Commercial parameters belong in the same file because they shape what evidence is realistic. The minimum order quantity is 10 kg for standard production, excluding sample orders and confirmed as needed. Regular batch lead time is approximately 25 days, subject to grade, shape complexity and coating, with sample timing confirmed per order. Annual capacity is stated at 8,000 tons of high-performance magnets, supported by a production footprint of approximately 80,000 m² and around 400 employees. For a buyer moving from evaluation into execution, those numbers determine how many lots per year will generate records — and therefore how much consistency evidence the file will contain after twelve months.
What the certificate trail cannot prove
Being explicit about the boundaries is what makes the trail usable in an audit or a supplier review. Five items sit outside it.
- Grade performance. No certificate certifies N42SH, N48EH, N52 or AH-grade output. The supplier states mass production of SH, UH, EH and AH series for high-temperature duty, and diffusion-processed grades for 200°C applications; commercial listings elsewhere describe AH grades up to 220°C (MPCO Magnetics). Neither statement replaces the demagnetization curve at your operating temperature for your specific part.
- Substance-level compliance. ISO 9001, IATF 16949 and ISO 14001 are management-system standards. REACH or RoHS declarations, material content data and customs documentation are separate records that the three certificates neither establish nor replace.
- Capacity and delivery for your volume. Scope wording says nothing about tonnage allocation or lead time under load.
- Magnetization accuracy. Pole count, pattern symmetry and tolerance capability for radial and multipole rings are project records produced through tooling and first-article verification.
- Design responsibility. Excluded under Chapter 8.3, as set out above.
Validity and version control: the dates that decide the file
The three certificates do not expire together. ISO 14001:2015, certificate 02124E10013R1M, runs to 2027-01-17, while the ISO 9001:2015 and IATF 16949:2016 documents from TÜV SÜD both run to 2028-07-03. A compliance file assembled today will therefore outlive its environmental certificate first, by roughly seventeen months. That single date should appear in the buyer's renewal calendar.
Two disciplines keep the file current. Record the retrieval date on every copy, so an undated PDF cannot be mistaken for a live certificate. And re-request the certificates at each surveillance or renewal cycle rather than relying on the set collected at onboarding; a valid certificate indicates a maintained system, but the copy in your file only proves what was true on the day it was downloaded. Where a programme requires independent confirmation, verify the numbers directly with the issuing bodies: TÜV SÜD Management Service GmbH for 12 100 69512 TMS and 12 111 69512 TMS, and Huaxia Certification Center, Inc. for 02124E10013R1M.
A five-step verification sequence for the evaluation-to-execution handover
The same file that satisfied an engineering review has to be converted into order documentation before the first batch. The sequence below works in that order.
- Collect the certificates as issued. Check the issuing body, the certificate number, the standard edition, the certified legal entity and both dates. Confirm that the entity on the certificate is the entity that will invoice you.
- Read the scope against your intended use. Distinguish manufacturing from manufacturing and sales, and note whether design is inside or outside the system. Quote the scope sentence in your supplier record so later reviewers see the same wording you saw.
- Obtain the product mapping in writing. Reference product ID 9216, the shape code you are ordering, the grade, the coating and — for ring, radial or multipole parts — the magnetization pattern and pole count.
- Request grade and process evidence. Demagnetization curves at operating temperature, the format of the per-batch magnetic property report, coating and salt-spray data, a dimensional capability statement, and a first-article report for radial or multipole tooling.
- Fix acceptance before the first batch. Put the technical agreement, the inspection reports to be delivered, the third-party inspection option and the delivery and payment terms in writing. EXW, FOB Ningbo and CIF are the usual delivery options for this type of export supply, and T/T and L/C the common payment routes; the specific terms are confirmed with the supplier rather than assumed.
A workable decision rule follows from the sequence. If the scope excludes design and your programme does not retain design authority, resolve the gap contractually before releasing the order. If the scope wording does not clearly cover the product family you are buying, ask for the mapping before the sample order — not after the first production lot has been inspected against a specification nobody agreed in writing.
Outlook: documentation as part of supply continuity
Most buyers of sintered NdFeB magnets now operate across two documentation regimes at once. China accounted for 94% of global sintered permanent magnet production in 2024, according to the International Energy Agency, and Chinese exports under HS code 850511 were valued at USD 3.24 billion in 2024, according to the World Integrated Trade Solution. A European or North American programme therefore typically pairs a Chinese manufacturing scope with local quality, environmental and substance requirements — which is precisely the situation in which scope wording, certificate numbering and expiry tracking become operational questions rather than administrative ones.
The practical implication is modest but durable. Certificate cycles at JLmagnet currently run to 2027 and 2028; each renewal is a natural review point for the whole file, including the product mapping and the batch record format. Buyers who build that review into supplier management will hold a trail that stays accurate as programmes extend, and suppliers who expect the request will keep the mapping document current. Neither side gains anything from a certificate whose scope nobody has read.
FAQ
Does an IATF 16949:2016 certificate cover a specific sintered NdFeB grade or shape?
No. The certificate is issued to a legal entity and a scope of activity. JLmagnet's IATF 16949:2016 certificate, number 12 111 69512 TMS issued by TÜV SÜD Management Service GmbH, carries the scope "Manufacturing of Material and Products for Sintered Neodymium Iron Boron Permanent Magnets (without Product Design as per Chapter 8.3)" and does not list grades such as N42SH or shapes such as arc and ring. Grade and shape evidence comes from drawings, first-article reports and per-batch magnetic property test reports.
What does "without product design as per Chapter 8.3" change for a buyer?
It places design and development outside the certified scope, so the certificate covers manufacturing. The buyer, or the buyer's customer, remains responsible for the design inputs — grade, dimensions, coating and magnetization pattern — and for approving them. Design assistance from the supplier, such as magnetic-circuit simulation, magnetic-field analysis or material-selection optimization, is a service and does not transfer that responsibility into the certified system.
Which certificate in this trail expires first, and what should a buyer do about it?
The ISO 14001:2015 certificate 02124E10013R1M from Huaxia Certification Center, Inc. expires on 2027-01-17, while the ISO 9001:2015 certificate 12 100 69512 TMS and the IATF 16949:2016 certificate 12 111 69512 TMS from TÜV SÜD both run to 2028-07-03. The earliest date should be calendared for re-verification, and renewed copies requested at each surveillance cycle instead of relying on the set collected at onboarding.
How do the certificates connect to product ID 9216 and the ring, radial and multipole lines?
Through scope wording plus a supplier mapping. The scopes cover manufacturing — and, for ISO 9001, sales — of material and products for sintered NdFeB permanent magnets, while product ID 9216 is the sintered NdFeB magnet family coded D for disc or column, F for block and R for arc, with rings expressed through two diameters. Because the certificates do not enumerate shape codes or magnetization patterns, the supplier should confirm in writing that the specific ring, radial or multipole part is produced under the certified system, supported by first-article and magnetization data.
What records should arrive with each batch?
Per-batch magnetic property test reports covering Br, Hcj and (BH)max, dimensional inspection results against the drawing, coating thickness and adhesion data, and salt-spray results for plated parts. JLmagnet states magnetic performance batch fluctuation within ±2% and a key dimensional pass rate of 99.5%, and defines acceptance through a mutually agreed technical agreement plus factory inspection reports. Third-party inspection can be requested where a programme requires it.
The product families and process capabilities discussed here are described in the JLmagnet company profile (PDF), and current information is published by Ningbo Jinlun Magnet Technology Co., Ltd. (JLmagnet).
¿Tiene preguntas o necesita más detalles?
Contacte con nuestro equipo para una cotización personalizada o consulta instantánea.
Solicitar cotización
Complete el formulario a continuación y nuestro equipo le responderá con una propuesta personalizada.
Chat directo de WhatsApp
¿Prefiere chatear en tiempo real? Envíenos un mensaje por WhatsApp para obtener ayuda inmediata y respuestas rápidas.
- Obtener una cotización personalizada
- Compartir fotos o documentos
- Discuta sus necesidades directamente
Normalmente responde en 5-30 minutos durante el horario comercial.