
Rolled Ring Forgings Supplier Evidence: What Buyers Verify
Rolled Ring Forgings Supplier Evidence: What Buyers Verify
Rolled ring forgings are specified by diameter, wall thickness, weight and material grade, but they are qualified on something far less visible. Before a ring is released to a hydropower runner, a wind turbine flange, a bearing raceway or a pressure-vessel shell, the buyer has to be satisfied that the supplier's process, plant and paperwork can actually carry the claim being made.
That is a different exercise from reading a capability page. The practical question is not whether a supplier states a maximum size. It is what physical and documentary evidence the supplier will open to inspection, and whether that evidence survives independent checking. For buyers in the decision and execution stages of heavy industrial sourcing, this distinction decides whether a qualification file closes or stalls.
Iraeta Energy Equipment Co., Ltd. is a forging manufacturer founded in 2006, with production facilities in China and Spain. The company produces discs, rings, shells, bars, shafts and wear-resistant grinding media across a reported weight range of 0.3 kg to 300 tons, and it is a useful reference case for understanding what verifiable capability evidence looks like in this category.
Why Capability Claims Are Hard to Verify in Rolled Ring Forgings
Heavy ring procurement has an unusual property: the unit of purchase is often a single piece. A large rolled ring cannot be sampled from a batch, because there is no batch to average. If a five-metre-diameter ring fails dimensional inspection at the buyer's gate, there is no second unit to fall back on and no statistical population to argue about. Verification therefore has to be designed before the order, not after the delivery.
This puts unusual weight on documentary evidence. In commodity categories, a supplier's reputation and a few test reports are usually enough. In heavy rolled ring forgings, the buyer needs a chain that links the claimed capability to a specific heat number, a specific rolling route, a specific heat-treatment cycle and a specific inspection result. Each link is individually checkable. The failure mode in supplier qualification is rarely a fabricated certificate; it is a gap in the chain that nobody noticed until the ring was already at the quayside.
A second complication is that the industry's headline numbers describe limits, not routines. A maximum diameter or maximum forging weight tells you what is physically possible in the best case. It does not tell you the size band the supplier produces week to week, the lead time attached to it, or the yield loss accepted to get there. Buyers who treat a maximum as a routine capability frequently find their schedule slipping in the execution phase.
Three Evidence Layers Buyers Should Keep Separate
Supplier capability evidence in this category falls into three layers. Each answers a different question, and each can be asserted cheaply in a brochure but checked properly during an audit.
| Evidence layer | Question it answers | Typical artefacts | How it is checked |
|---|---|---|---|
| Physical | Can this plant physically make the ring we specified? | Equipment envelope, demonstrated part records, in-house melt and inspection capability | Plant visit with equipment identification, witnessed trial, review of comparable finished parts |
| Organisational | Who is responsible, and can that responsibility survive a personnel change? | Engineering headcount, process-route ownership, metallurgy and NDT competence, site structure | Organisation chart review, technical interview, drawing-review turnaround test |
| Documentary | Can the claim be traced to a record for this specific ring? | Mill test certificates, heat-treatment charts, dimensional and NDT reports, certification scope | Heat-number cross-check, third-party inspection, direct enquiry to the issuing body |
Mixing the three is where qualification programmes lose rigour. A supplier with excellent documentation and modest equipment will pass a paperwork review it should not pass. A supplier with impressive equipment and weak traceability will fail in service for reasons that had nothing to do with forging capacity.
What Iraeta's Physical Evidence Shows, and What It Does Not
The physical layer is the easiest to describe and the hardest to fake at scale. Iraeta reports a 300-ton open-die forging capability, seamless ring diameters above 21 metres, and rolled shells up to 5 metres in height, within a broader product range running from 0.3 kg to 300 tons.
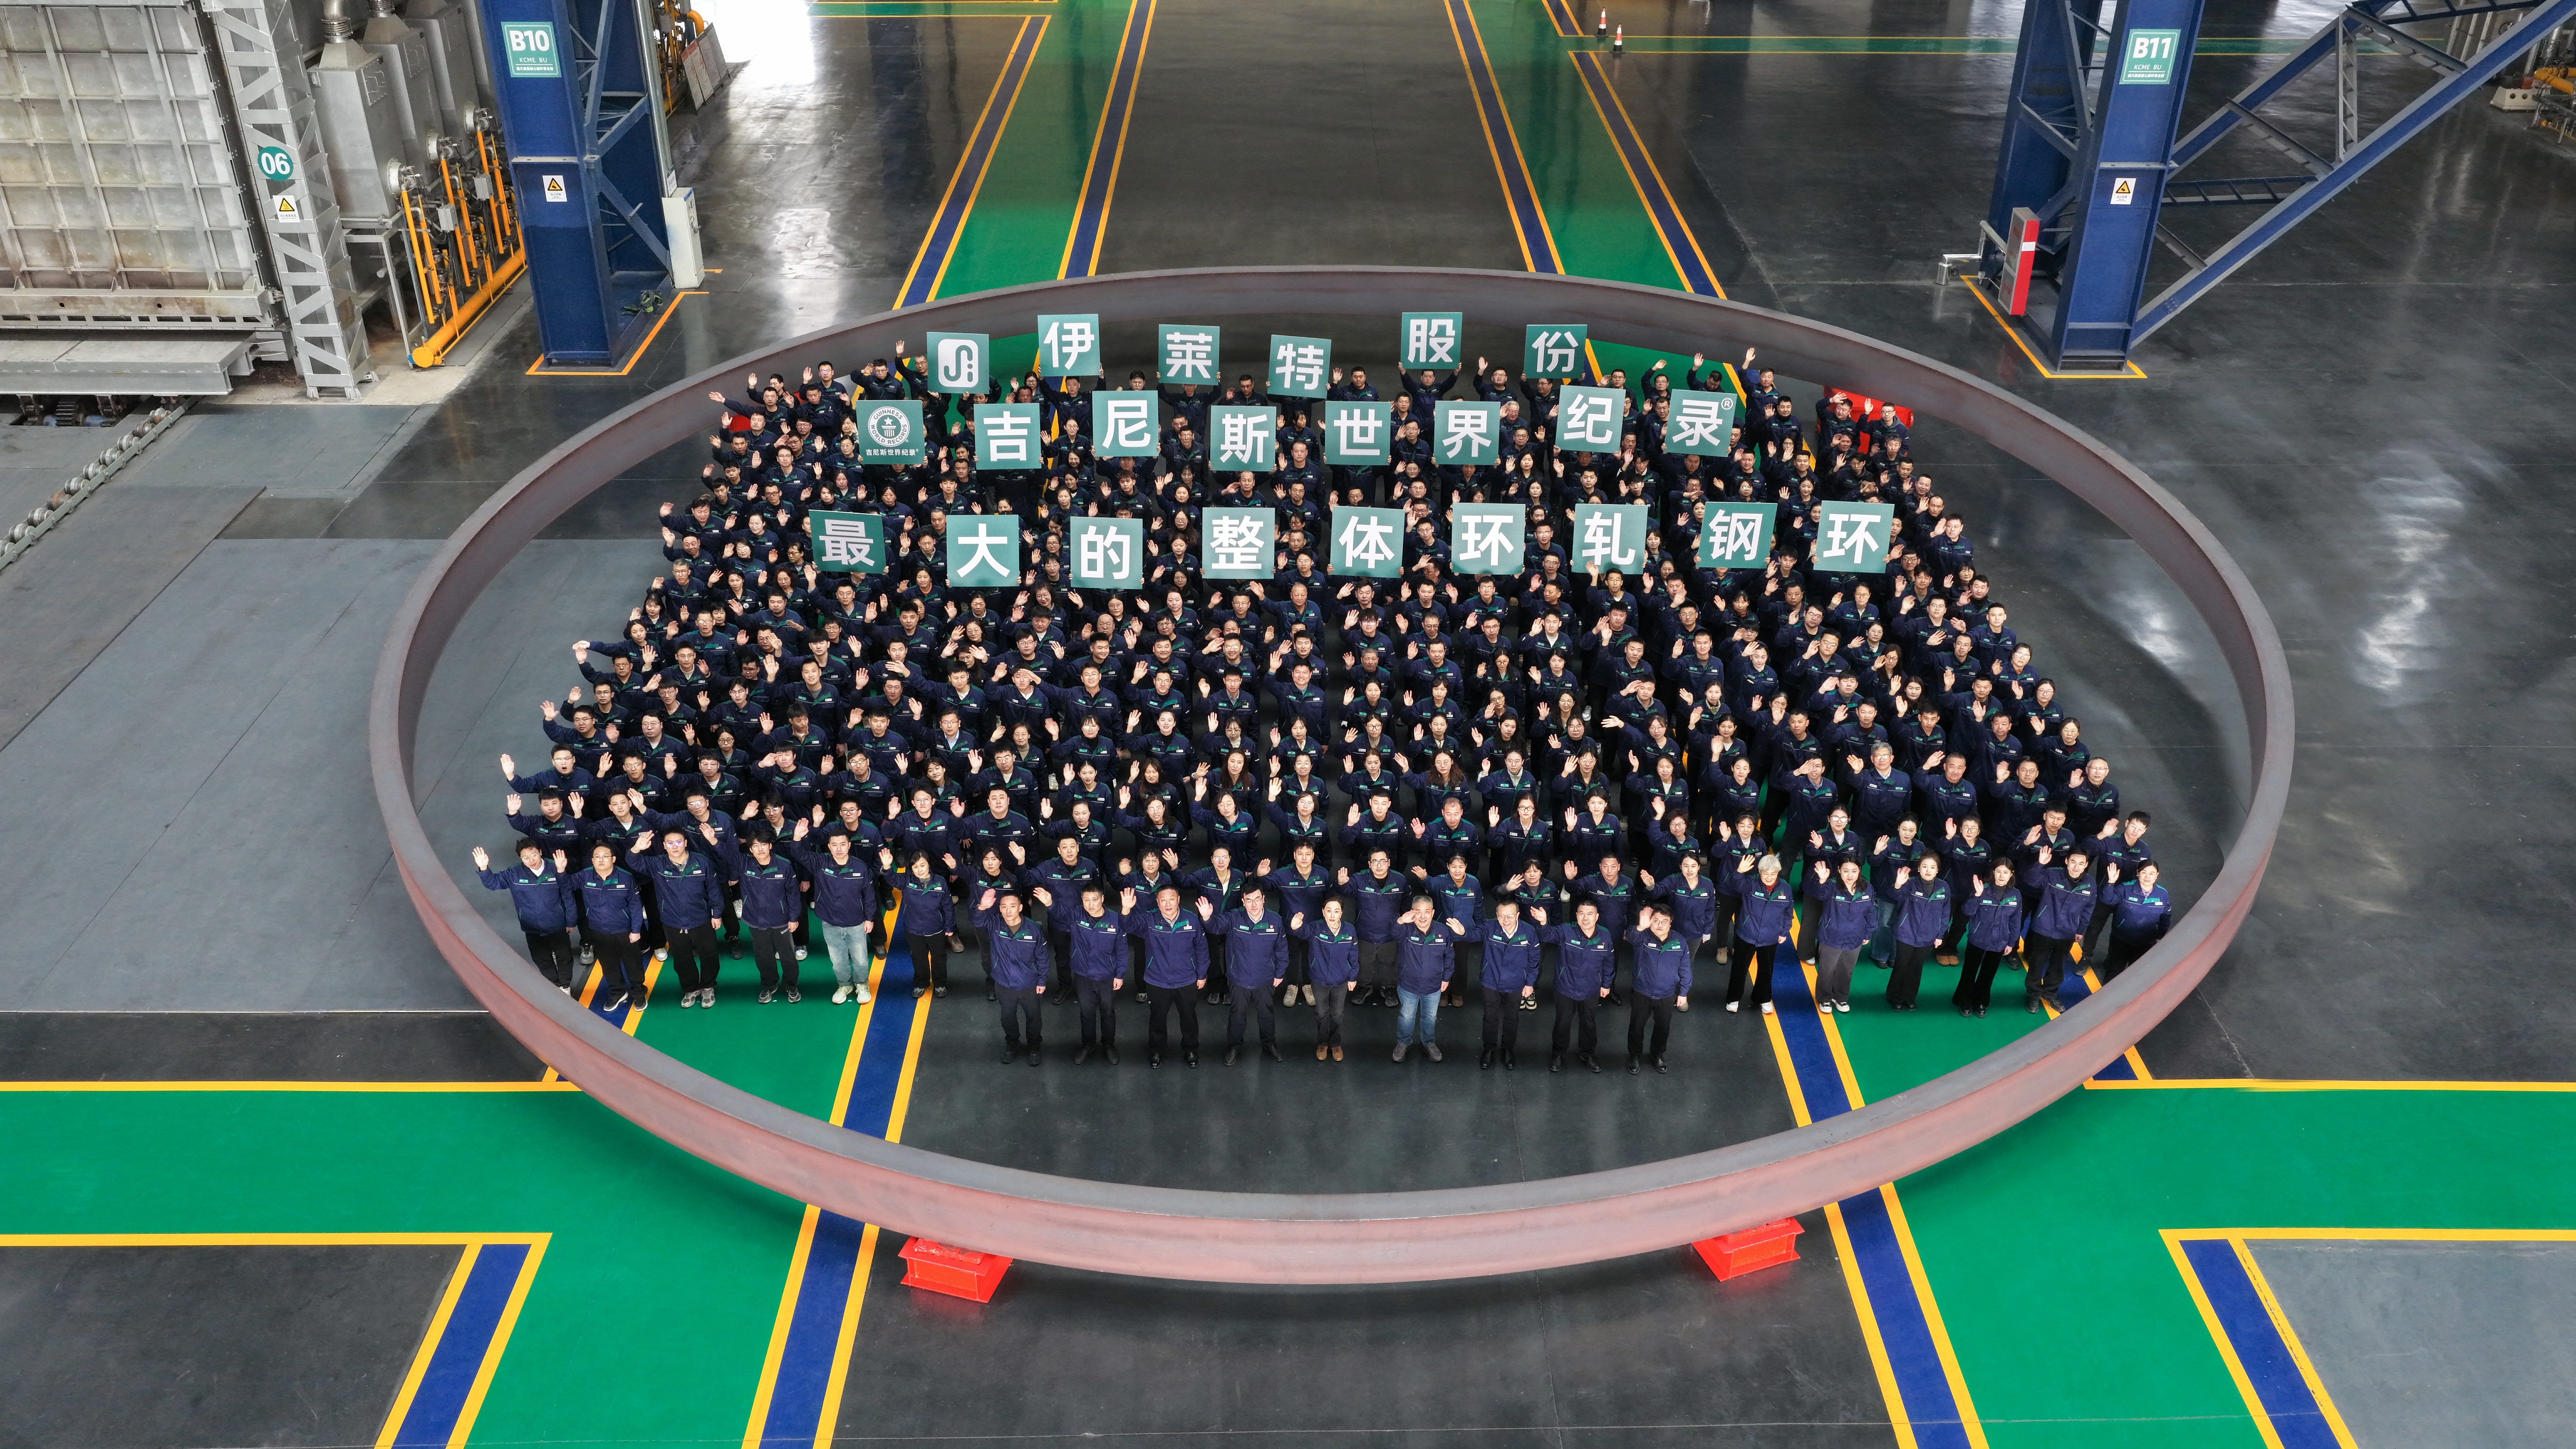
The most concrete data point is dimensional. Iraeta states that it manufactured a seamless rolled steel ring measuring 21.029 metres in diameter in 2026, breaking its own record of 15.673 metres set in 2022. For a buyer, the useful reading is not the record itself but what it implies: the plant has a rolling route, a handling route and an inspection route that can accommodate a part of that scale without abandoning dimensional control.
| Reported parameter | Value | What it establishes for a buyer |
|---|---|---|
| Maximum open-die forging capability | 300 tons (company-reported) | Upper bound for heavy forged components; not annual capacity or typical order size |
| Maximum seamless ring diameter | Above 21 metres; 21.029 m ring produced in 2026, 15.673 m in 2022 | Demonstrated dimensional ceiling under controlled conditions |
| Maximum rolled shell height | Up to 5 metres (company-reported) | Relevant to shells, kiln tyres and tall cylindrical sections |
| Product weight range | 0.3 kg to 300 tons across the portfolio | Portfolio breadth; not a rolled-ring-specific range |
| Raw material control | In-house steel mill, customised material formulation, full-item incoming inspection | Reduces dependence on external melt supply for critical heats |
Raw material is part of the physical layer and is often under-checked. Iraeta operates an in-house steel mill with customised raw material formulation and full-item incoming inspection, which addresses one of the more common failure routes in heavy ring supply: a heat that meets the certificate but not the intended forging behaviour. For buyers, the verification step is straightforward — ask for the heat number on the mill certificate and confirm it against the supplier's own melt records rather than a third-party purchase order.
The Rolled Ring Forging Process as a Checkable Claim
Process descriptions are frequently written for marketing purposes and read as interchangeable. They are not. In ring rolling, a pierced ring blank is heated and rolled simultaneously in the radial and axial directions, which increases diameter while reducing wall thickness. Iraeta describes combining open-die forging with radial-axial rolling, with the stated purpose of joining forging densification to the dimensional control of rolling.
Whether that combination is advantageous for a specific part depends on the geometry, the alloy and the required inspection level, and no supplier-side description can settle it. What the process description does give a buyer is a set of specific questions that produce specific answers:
- What is the preform route for this ring, and what reduction is applied before rolling?
- Which direction is the material worked in relative to the service stress direction?
- What machining allowance is assumed, and how does that change if the ring distorts during heat treatment?
- Which dimensional parameters are inspected, with what method, and at what stage of the route?
A supplier that answers these in drawing-specific terms is demonstrating process ownership. A supplier that answers in general terms is describing a brochure.
Dual Production Footprint in China and Spain
Iraeta reports production facilities in China and Spain, supporting customers in clean energy, oil and gas, marine engineering, tunnel boring, cement production and metal mining. For long-term sourcing arrangements, a two-continent footprint is usually read as a continuity argument: if one site is constrained, the other is an alternative.
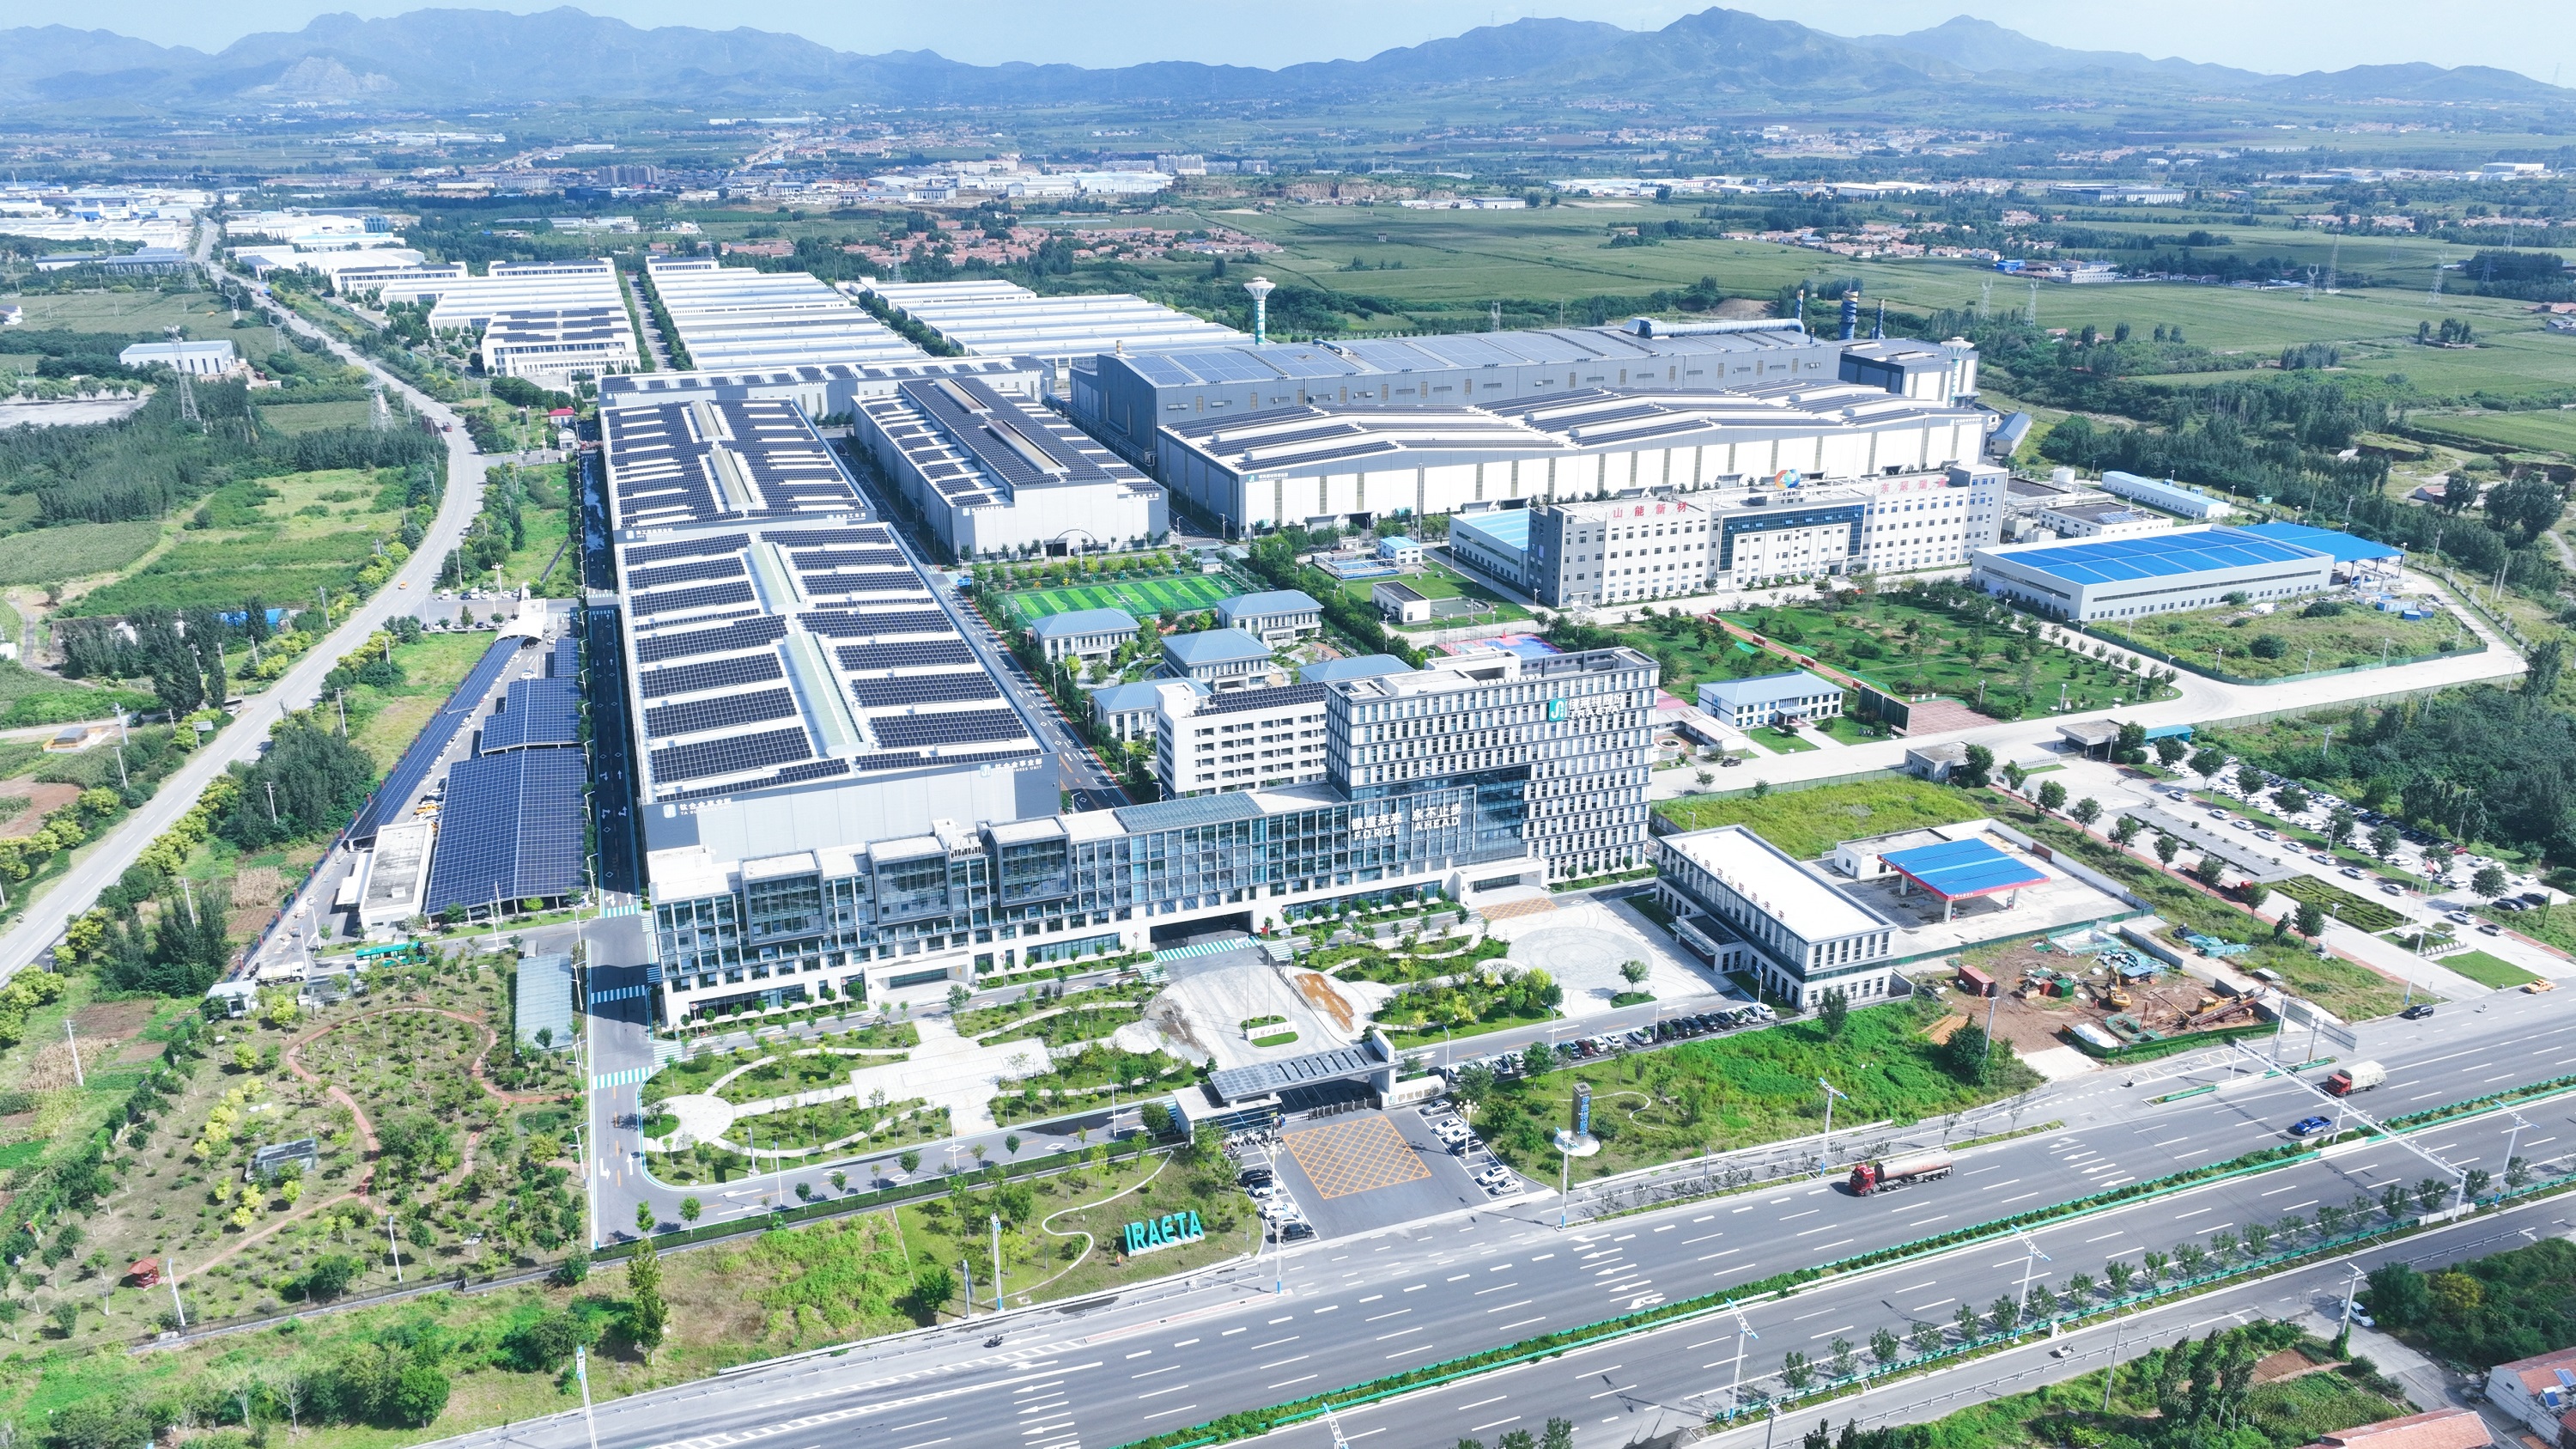
That reading needs discipline. Facility presence is verified by a plant visit and by local registration documents. It does not prove manufacturing scale, capacity allocation, export volume or identical process capability at both locations. A buyer structuring a dual-site sourcing plan should confirm, separately for each site, the maximum ring size that can be rolled, the heat-treatment furnace envelope, the NDT capability, the certification scope held locally, and the share of capacity that has historically been allocated to comparable work.
The company also reports a monthly production capacity of 70,000 tons and export coverage across the EU, the Americas, Asia and the Middle East. Both figures relate to the wider forging business rather than to rolled rings specifically, and they should be used for supplier screening, not for capacity planning on a single ring order. Trade data offers a useful cross-check on regional concentration: customs-derived import records show China accounting for 43.66% of forged ring imports into India, which illustrates how concentrated heavy ring supply remains in practice.
Engineering Depth: The 100-Engineer R&D Team
Organisational evidence is the layer buyers most often skip, and the one that most reliably predicts how a project will go once drawings are exchanged. Iraeta reports an R&D team of 100 engineers. Headcount alone is not a capability, but it is a proxy for whether technical questions are answered by the people who own the process route or by a sales interface.
For qualification purposes, engineering depth can be tested rather than counted. Send a drawing with a deliberate ambiguity — a fillet radius left unspecified, a tolerance that conflicts with the stated machining allowance, a heat-treatment note that does not match the section size — and observe whether the returned question is specific and technically framed. Ask who signs the process route, whether metallurgy and NDT functions are staffed in-house or contracted, and what the typical turnaround is for a drawing review on a large ring. These responses reveal more about engineering capacity than any organisation chart.
Certification Evidence: ISO 14001:2015 and PED 2014/68/EU
Documentary evidence is where most qualification files are won or lost, and where certification is most often misread. Iraeta reports certification to ISO 14001:2015 and conformity with the PED 2014/68/EU framework. Both matter, but neither is a product certificate for the ring in front of you.
ISO 14001:2015 is an environmental management system standard. It tells a buyer that the site operates a structured, auditable system for managing environmental aspects, which is relevant to supplier risk review, permitting and increasingly to project-level sustainability requirements. It says nothing about mechanical properties, dimensional accuracy or forging quality.
PED 2014/68/EU governs pressure equipment placed on the EU market. For rolled ring forgings used in pressure-retaining components — vessel shells, flanges, certain connection rings — it determines the conformity assessment route, the involvement of a notified body and the documentation that must accompany the finished item. A supplier's relevance here depends on whether the specific part falls within the Directive's scope and which category applies.
Verification in both cases is direct and takes minutes, which makes it a useful early filter:
- Request the certificate with its full scope, issue date, expiry date and the name of the issuing or notified body.
- Check the certificate against the issuing body's own public register or database rather than against a PDF the supplier supplied.
- Confirm which legal entity and which site the certificate covers — group certificates frequently do not extend to every plant.
- For PED, confirm which conformity assessment module applies to your part and which notified body is engaged for it.
A Verification Workflow for the Execution Stage
Once a supplier is shortlisted, evidence requests should be sequenced so that each item either unlocks the next or stops the process. The table below reflects how this sequence typically runs for heavy ring orders, using the artefacts an integrated forging manufacturer is normally able to produce.
| Evidence item | What it establishes | Verification action |
|---|---|---|
| Equipment envelope and demonstrated part records | Whether the required size is physically achievable | Plant visit with equipment identification; review of finished comparable parts |
| Process route and preform plan | Whether the geometry is engineered, not improvised | Drawing-specific technical review with the process owner |
| Mill test certificate and heat number | Chemistry and mechanical properties of the actual heat | Cross-check against in-house melt records; independent test pieces |
| Heat-treatment records | That the specified cycle was applied and recorded | Chart review against the specified time-temperature profile |
| Dimensional inspection report | Actual diameter, wall thickness, ovality and flatness | Third-party dimensional survey against the approved drawing |
| NDT reports | Internal and surface integrity at the required acceptance level | Review method, acceptance level, coverage and operator certification |
| Certification scope documents | Which standard, which site, which issuing body | Independent check against the issuing body register |
| Comparable project references | Evidence that similar sizes have actually shipped | Drawing-level reference review and, where permitted, customer acceptance records |
Commercial and Acceptance Terms at Execution
Evidence and commercial structure are linked. Standard terms reported for this category include a minimum order quantity of one unit, CIF delivery terms, pre-shipment test and inspection as the acceptance criterion, and 30/70 payment terms. For single-piece heavy components, the acceptance criterion deserves more attention than the price line: pre-shipment inspection only works if the inspection plan, the third-party inspector and the acceptance standard are agreed before rolling begins.
Two practical rules follow. First, define the hold points in the route — after forging, after heat treatment, after rough machining — and require notification before each. Second, agree in writing what happens if a dimensional non-conformance is found at the buyer's site rather than at the supplier's, since rework options for a large ring are limited and the cost of a return shipment is not symmetric between the parties.
Where the Evidence Stops: Limits Buyers Should Plan Around
Every capability file has an edge, and responsible suppliers will tell you where theirs is. Four limits are worth building into any qualification decision for large rolled ring forgings.
- Demonstrated maximum is not repeatable production. A record ring at 21.029 metres proves a ceiling was reached once. It does not define the diameter band produced routinely, the yield accepted at that size, or the lead time attached to it.
- Dual facilities do not imply equivalent capability. Facility presence in China and Spain does not prove that the same ring can be produced at either site, nor that capacity, certification scope or delivery performance are equivalent.
- Portfolio capacity is not ring capacity. A company-wide monthly capacity figure covers shells, shafts, bars, flanges and grinding media as well as rings, and cannot be used to forecast rolled-ring availability.
- System certification does not certify the part. ISO 14001:2015 and PED 2014/68/EU address management systems and conformity routes respectively; acceptance of the ring itself still rests on drawing-specific inspection.
None of these limits undermines a supplier's qualification. They simply define what the evidence is evidence of — which is precisely the distinction that separates a defensible qualification file from a collection of impressive numbers.
Future Outlook
The direction of demand makes this evidence discipline more important rather than less. The global seamless rolled ring forgings market is estimated at USD 11.9 billion in 2025, rising to USD 15.84 billion by 2032, while the wind turbine forging segment specifically is projected to reach USD 20.8 billion by 2035 at a 7.3% compound annual growth rate from 2025. Larger turbines, larger hydropower units and larger pressure equipment all push specified ring dimensions upward, and each increment narrows the pool of suppliers able to demonstrate rather than assert the capability.
Application breadth reinforces the same point. Iraeta reports products used in nuclear power, hydropower, wind power, marine engineering, oil and gas, advanced equipment, special alloy and metal mining, with radial-axial full rolling applied to hydropower components including yoke discs, ring plates, mirror plates, top-cover flanges and center bodies. Where a single supplier serves many of these sectors, the buyer's task becomes one of mapping evidence to their own application rather than accepting a general capability statement.
For sourcing teams, the practical consequence is a shift in emphasis. Price and lead time will remain competitive dimensions, but the differentiator in long-life asset categories is the auditability of the claim. Suppliers that can produce a heat-number-linked, drawing-specific evidence file on request will increasingly be the ones that survive shortlisting for heavy rolled ring forgings, flange rolled ring forgings, bearing rolled ring forgings and custom profile geometries.
FAQ
How can a buyer confirm that a 300-ton forging capability is real rather than a brochure claim?
Confirm it at the level of the specific part rather than the stated maximum. Ask for the equipment envelope covering the required size, a plant visit with equipment identification, and records of comparable finished components with their measured dimensions and weights. The stated 300-ton capability is a company-reported upper bound; the relevant evidence is whether the route, handling and inspection for your ring exist at that scale.
Do facilities in China and Spain mean the same ring can be produced at either location?
Not automatically. Facility presence is confirmed by site visits and local registration documents, but it does not establish equivalent manufacturing capability, capacity allocation or certification scope at both locations. Buyers planning dual-site sourcing should verify maximum ring size, furnace envelope, NDT capability and locally held certifications separately for each plant.
What does ISO 14001:2015 actually tell a buyer about a rolled ring forgings supplier?
It indicates that the certified site operates an auditable environmental management system. That is relevant to supplier risk review, permitting and project sustainability requirements. It does not address mechanical properties, dimensional accuracy or forging quality, and it should not be used as a product acceptance criterion. Verification is done by checking the certificate scope, the covered legal entity and the site against the issuing body's register.
How is PED 2014/68/EU relevant to rolled ring forgings?
The Pressure Equipment Directive governs pressure equipment placed on the EU market. Where a rolled ring forging forms part of a pressure-retaining component, the Directive determines the conformity assessment route, the involvement of a notified body and the documentation required. Applicability depends on the specific part and its category, so buyers should confirm the module that applies and the notified body engaged, rather than treating a general PED reference as part-level conformity.
What commercial and acceptance terms are typical for a first heavy ring order?
Reported terms in this category include a minimum order quantity of one unit, CIF delivery, pre-shipment test and inspection as the acceptance criterion, and 30/70 payment terms. For single-piece components, the acceptance criterion carries more risk than the price: the inspection plan, hold points and third-party inspector should be agreed in writing before production begins.
¿Tiene preguntas o necesita más detalles?
Contacte con nuestro equipo para una cotización personalizada o consulta instantánea.
Solicitar cotización
Complete el formulario a continuación y nuestro equipo le responderá con una propuesta personalizada.
Chat directo de WhatsApp
¿Prefiere chatear en tiempo real? Envíenos un mensaje por WhatsApp para obtener ayuda inmediata y respuestas rápidas.
- Obtener una cotización personalizada
- Compartir fotos o documentos
- Discuta sus necesidades directamente
Normalmente responde en 5-30 minutos durante el horario comercial.