
Quality Benchmarks in Heavyweight Hoodie Production: Compliance and Consistency
Quality Benchmarks in Heavyweight Hoodie Production: Compliance and Consistency
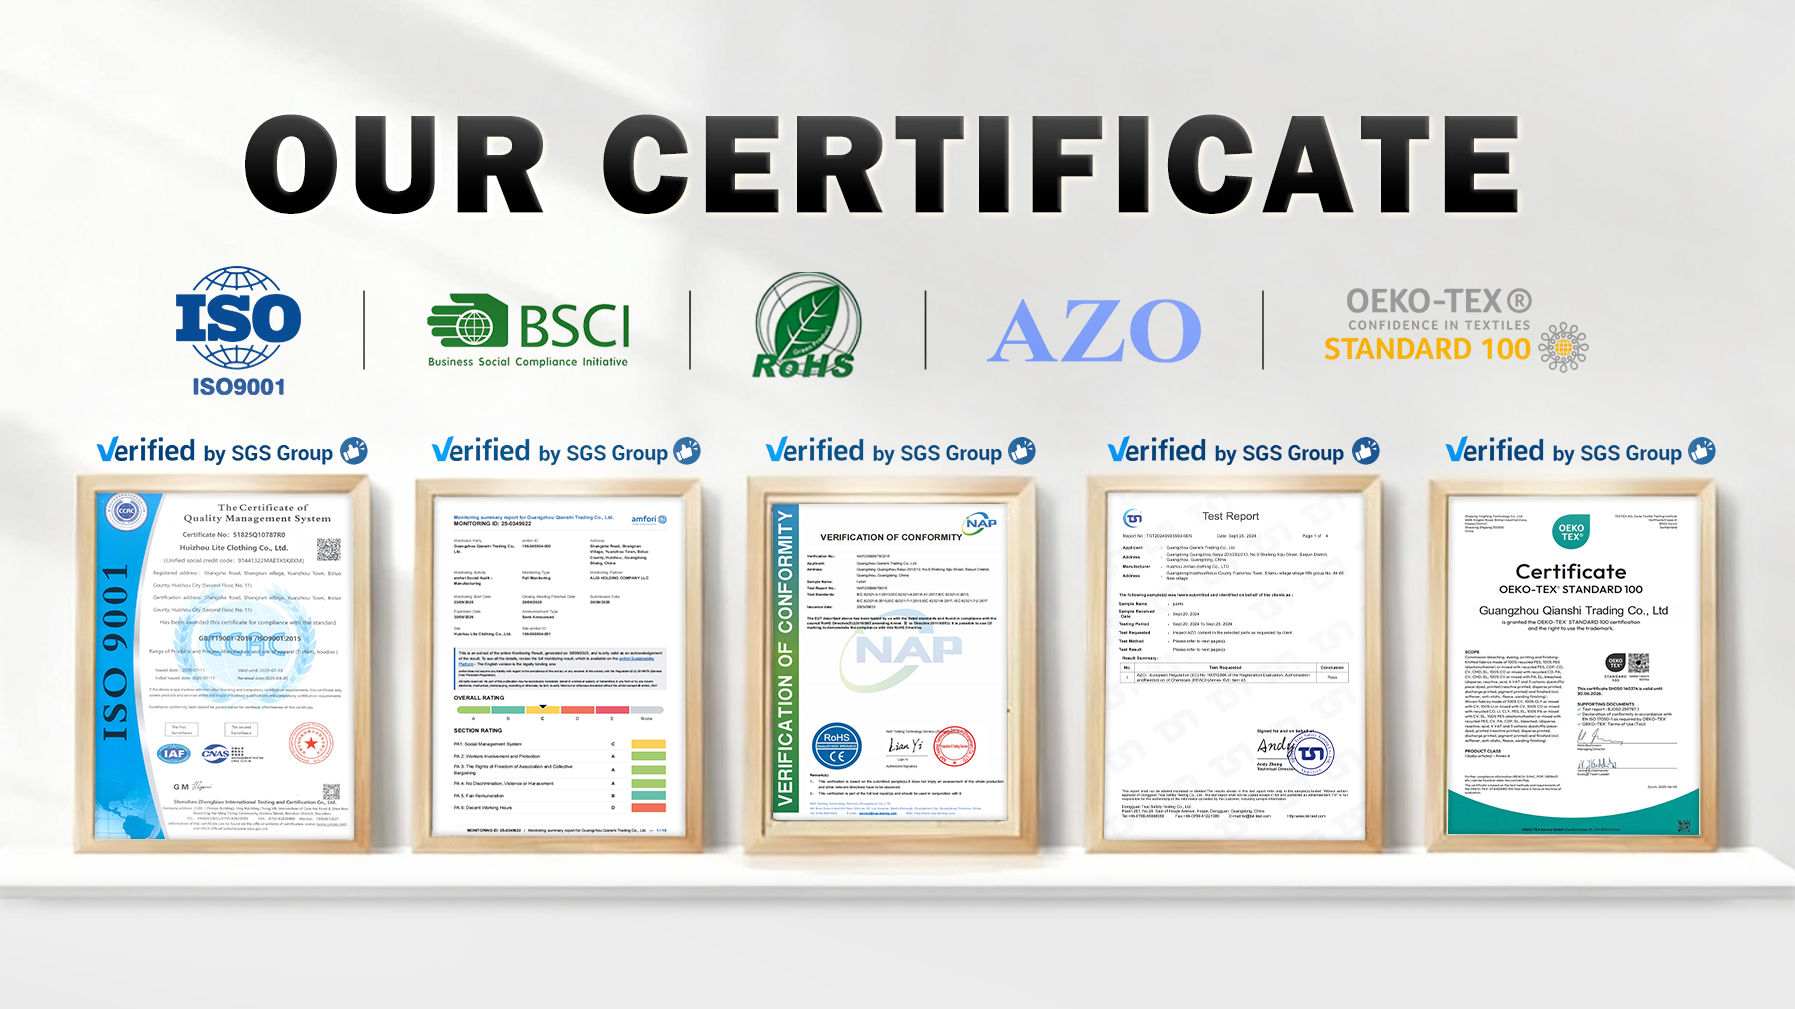
Compliance documentation is only the entry ticket in heavyweight hoodie sourcing. The benchmark that decides supplier qualification is repeatability across sizes, colorways and reorders.
A hoodie that fades, shrinks or skews across sizes will fail in the market regardless of how many certificates sit behind it. That gap between documentation and behaviour is where most heavyweight hoodie sourcing decisions are actually won or lost, and it is the reason buyers at the decision and execution stage increasingly treat certification as a starting point rather than a conclusion.
The distinction matters because the two things are not the same. A compliance document confirms that a mill or factory met a defined standard on the day it was audited. Consistency confirms that the fiftieth unit in the fiftieth size of the fourth colorway behaves the same way as the first approved sample. Only one of those two conditions protects a brand's return rate, review score and reorder economics.
Why Quality Benchmarks Have Moved Beyond Paperwork
The global hoodies and sweatshirts market was valued at USD 209.26 billion in 2025 and is projected to reach USD 303.62 billion by 2031, according to Mordor Intelligence. Growth of that scale multiplies the number of factories bidding for the same brand programmes, and it multiplies the number of certificates presented as proof of capability.
The supply side is expanding at the same time. China's apparel exports reached USD 159.14 billion in 2024, a 0.3% year-on-year increase despite geopolitical pressure, according to the General Administration of Customs. An export base of that size gives buyers an enormous choice of suppliers, but it also means that qualification cannot rest on the mere existence of documents.
Textile certifications such as OEKO-TEX Standard 100, which addresses chemical safety, and GOTS 7.0, which governs organic fibre content, remain the industry benchmarks for sustainable manufacturing. They are necessary credentials for premium retail programmes. They are also scope documents: they describe what a material is, not how consistently a factory reproduces it order after order. A buyer who stops at the certificate has verified the fabric, not the supplier.
What Qualified Means in Heavyweight French Terry
Heavyweight hoodies in the 350–450+ GSM range using 100% cotton French terry are the preferred standard for premium streetwear brands, primarily because the fabric's structure and pilling resistance hold up under repeated wear. Weight alone, however, does not deliver that outcome. The specification is a target, and the production system is what determines whether the target is met repeatedly.
Decoration raises the bar further. The global custom hoodie printing market is growing at a CAGR of 9.9% between 2024 and 2030, with high demand for 3D puff embroidery and eco-friendly water-based inks, according to Grand View Research. Puff print and embroidery are the two decoration methods most sensitive to process control, because both depend on curing time, backing stabilisation and tension settings that must be held constant rather than approximated per order.
In practice, a qualified heavyweight supplier is one that can answer a specific question: what happens to the measurement chart in month nine, when the fabric lot has changed but the pattern has not. Certification does not answer that question. Process control does.
A Compliance-to-Consistency Chain: Guangzhou Qianshi Apparel Co., Ltd
Guangzhou Qianshi Apparel Co., Ltd, which trades internationally as Qianshiwear, is an apparel manufacturer and trading company based in the Baiyun District of Guangzhou, Guangdong, specialising in OEM and ODM production for clothing brands. The company was founded in 2014 and works across T-shirts, hoodies, sweatshirts, sweatpants, joggers, tracksuits, polos, jerseys, jeans, caps and outerwear.
Its production footprint illustrates how the compliance-to-consistency model is physically organised: a 600 m² sewing area, a 700 m² warehouse, a 1,500 m² finishing area and a 200 m² packing area. The workforce combines 80–100 sales representatives, order coordinators, operations staff, designers and administrative personnel with 200–250 production line workers, quality control staff and pattern makers, supported by a 15-person design team.
Output is oriented towards export: 85–90% of total production ships to the EU, USA, AU and UK markets, with annual output of 3,000,000 units and a monthly production capacity of 250,000 units. For a decision-stage buyer, the relevant point is not the size of those numbers but their relationship to the control system described below. Capacity without process control simply produces defects at a faster rate.
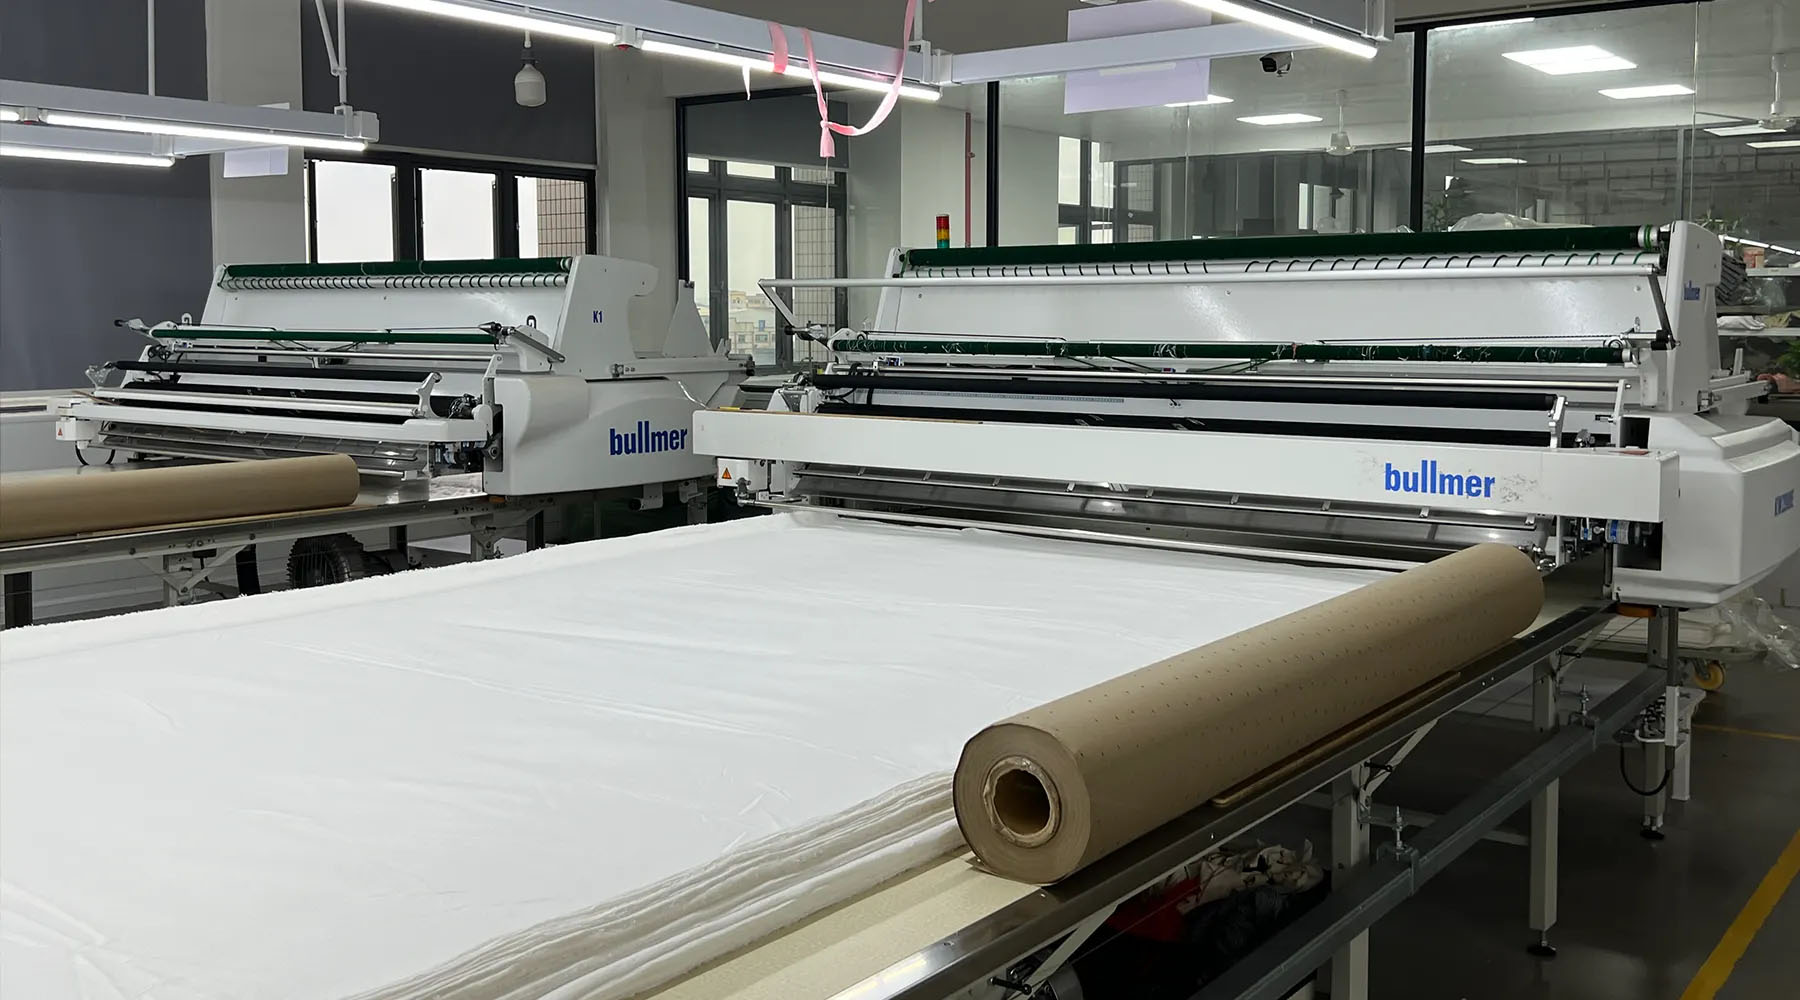
Fabric spreading and pre-shrinkage handling before cutting: the stage at which measurement consistency across sizes is either secured or lost.
The Five Control Gates Where Repeatability Is Created
Repeatable quality is not an inspection event; it is a sequence of gates. At Qianshiwear the sequence is defined explicitly, and each gate produces a record that a buyer can request.
| Gate | What is controlled | Buyer-visible output |
|---|---|---|
| Incoming material | 100% fabric inspection on arrival, checking weight, width, colour consistency and shrinkage potential; hardware and trim samples tested before bulk approval | Fabric inspection record; approved trim reference sample |
| In-process | First-article inspection at cutting, sewing and printing stages; random patrol checks across production lines; real-time adjustment of embroidery tension and print alignment | First-article approval records; inline correction log |
| Final inspection | AQL 2.5 sampling applied to finished goods; pre-shipment wash tests on representative samples; size and measurement verification across all colorways | Inspection report; measurement verification by colorway |
| Traceability | Production batch number assigned to each order; quality records retained for future reorder reference; defect analysis documented for continuous improvement | Batch record retrievable at reorder stage |
| Third-party support | Third-party inspection such as SGS or Intertek available on client request; lab testing for specific performance requirements including colour fastness and tensile strength | External inspection or lab report arranged at client cost |
The fourth gate is the one buyers most often overlook during supplier evaluation and most often rely on during a reorder. A batch number converts a quality claim into a retrievable record: when a brand returns eighteen months later for a repeat run, the factory can reconstruct which fabric lot, which stitching parameters and which measurement tolerances produced the approved shipment.
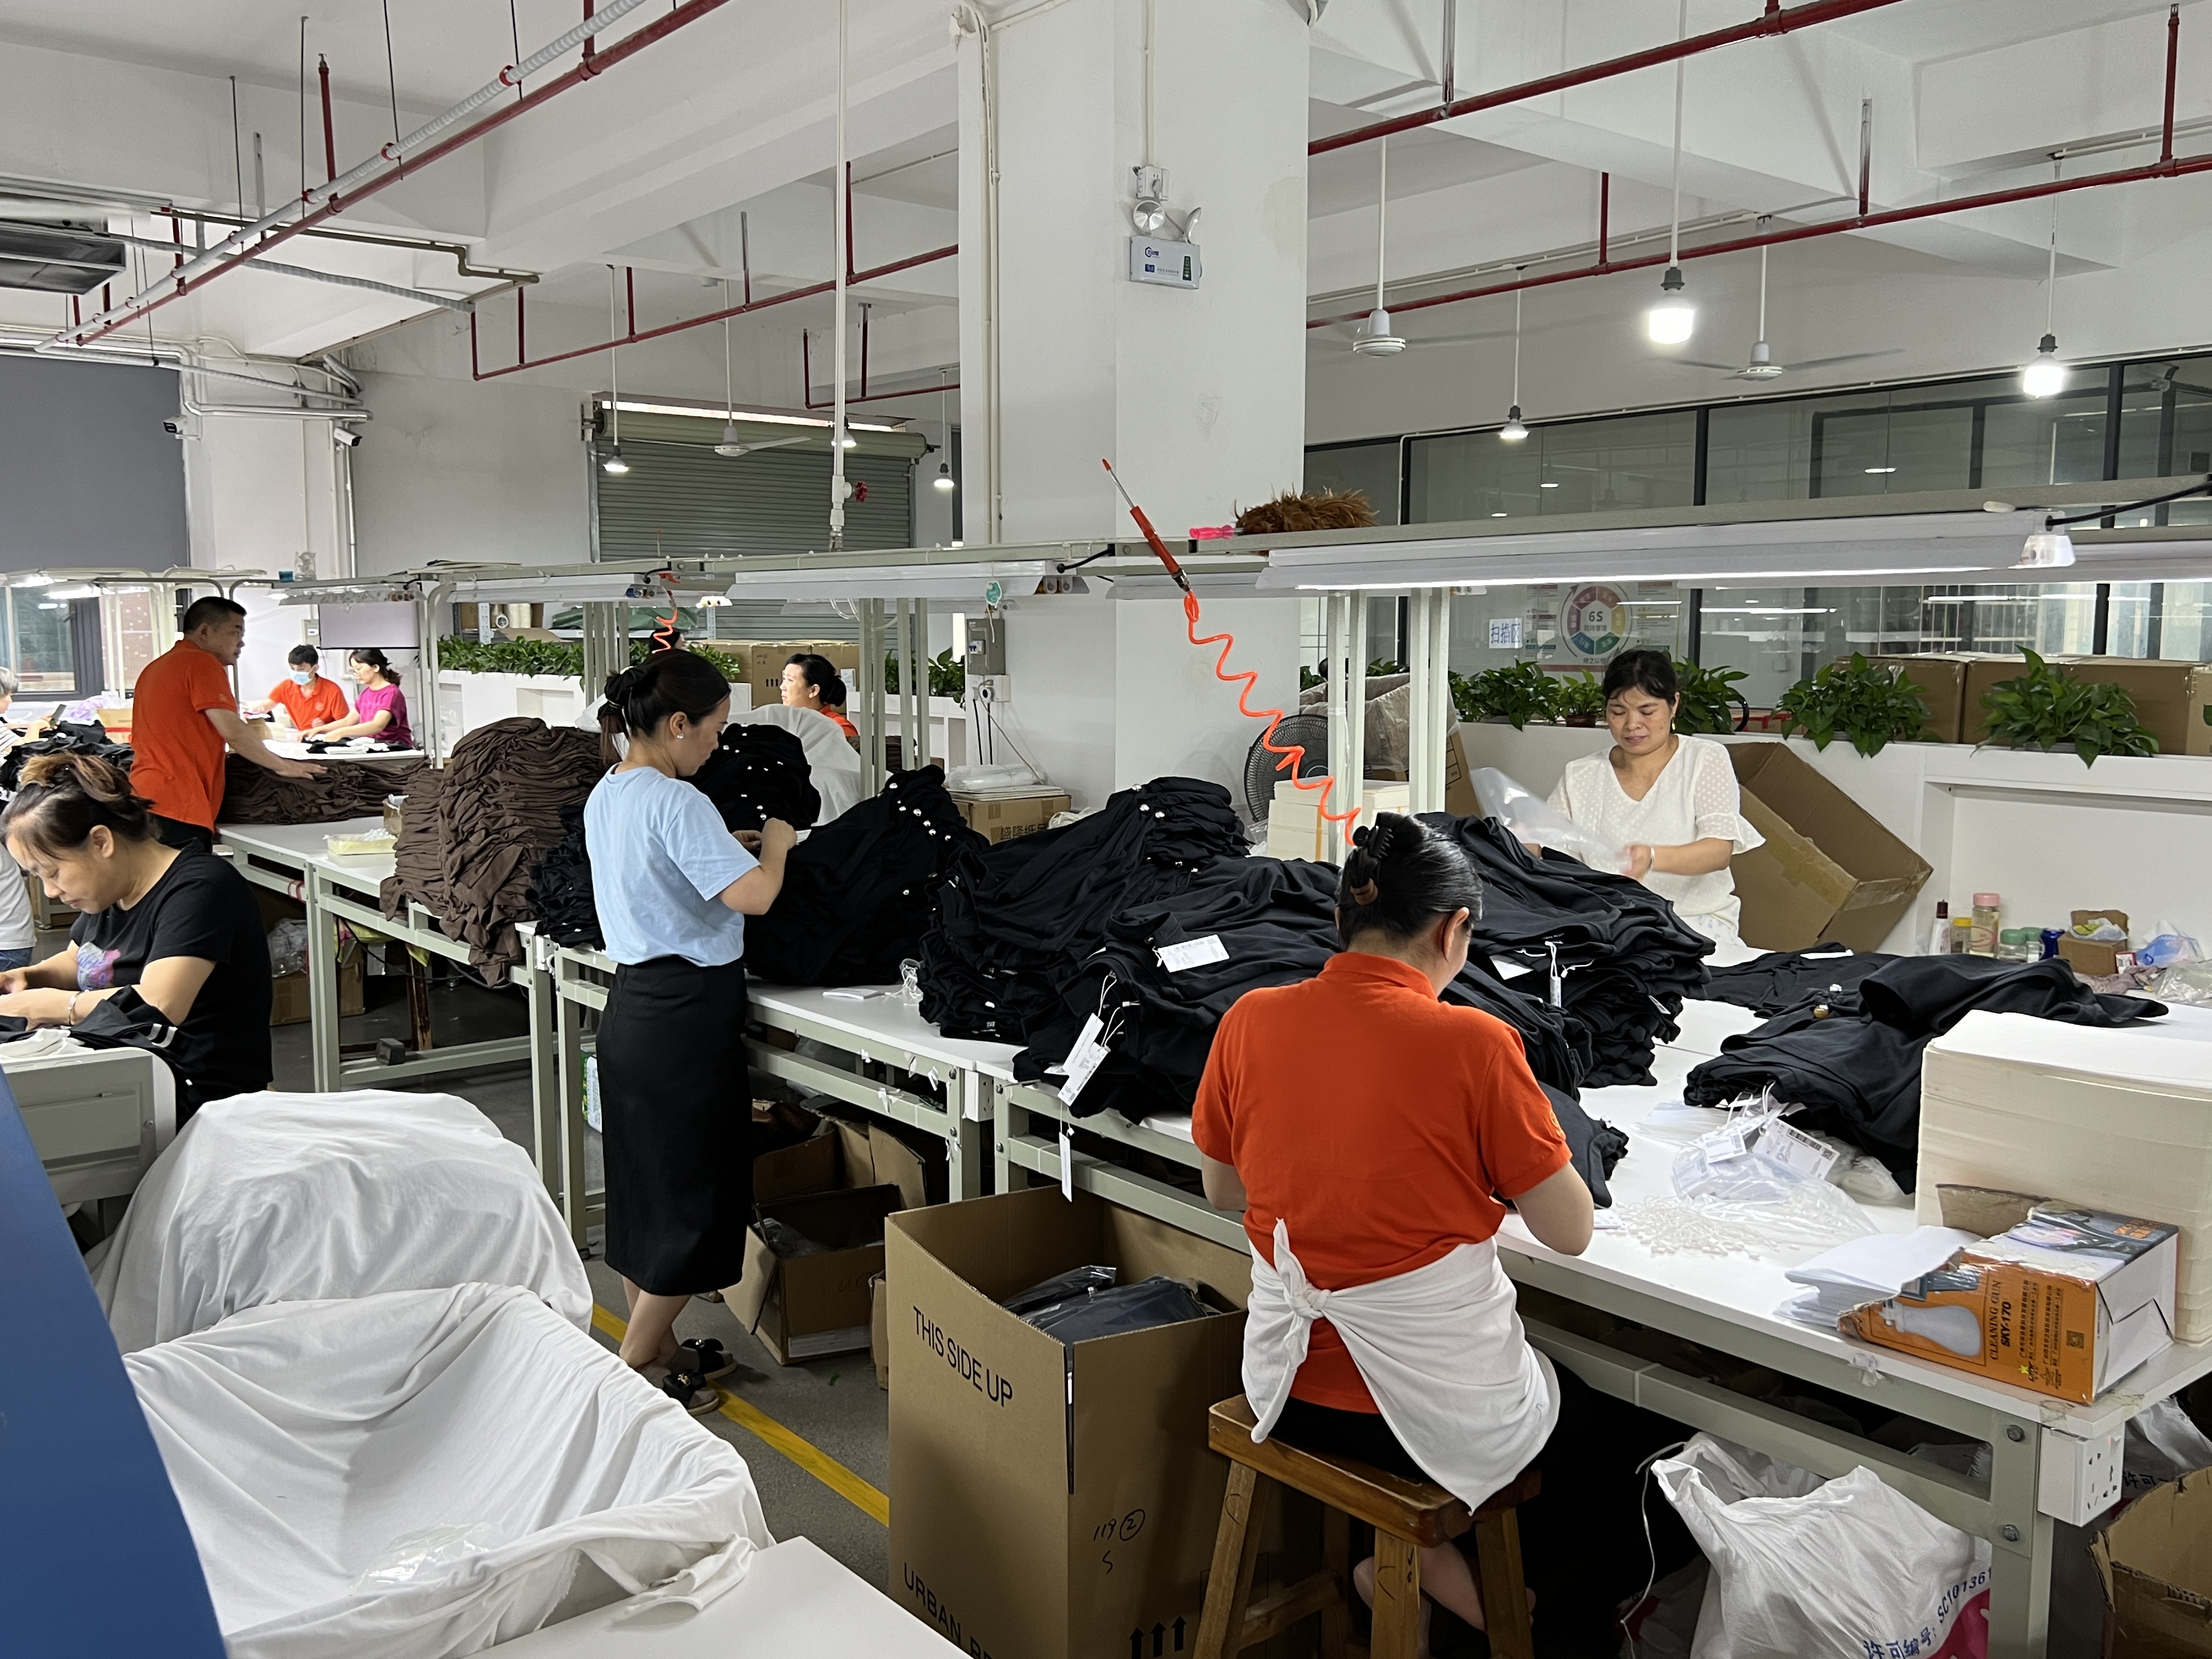
Final inspection under AQL 2.5 sampling: the gate that converts an approved sample into an approved shipment.
Consistency Across All Sizes: The Benchmark Buyers Rarely Test Until It Fails
Size consistency is the most reliable single indicator of a qualified manufacturer, and it is the hardest claim to fake. Colour can be matched to a swatch. Hand feel can be improved with finishing. But a measurement chart that holds across every size, every colorway and every repeat order requires control of the entire chain before and after cutting.
At Qianshiwear, that control is expressed through several specific production disciplines. Reactive dyeing with high-temperature fixation pushes colour deeper into the fibre, which reduces the risk of shade drift between panels cut from different parts of the roll. Pre-shrinkage treatment is applied before cutting, so the fabric's dimensional movement occurs before the pattern is applied rather than after the customer washes the garment. First-article inspection is performed at the cutting stage, which is early enough to correct a grading issue before it is multiplied across thousands of units.
Measurement verification is then repeated across all colorways at final inspection, using standardised AQL sampling for size and measurement confirmation. Stress points receive reinforced stitching with high-tensile thread, hardware is subjected to pull and closure testing before bulk assembly, and embroidery backing stabilisation is used to keep thread tension constant — a step that matters because a hood with variable tension reads to the customer as a defective product even when the body measurement is exact.
For a procurement team, the practical implication is simple. If a supplier can demonstrate identical size behaviour in two consecutive orders, the probability that other variables — shade, weight, decoration — are also under control rises sharply, because the same gates govern all of them.
Test Case: A 500 GSM French Terry Hoodie
The 500 GSM French terry hoodie in Qianshiwear's heavyweight range is the clearest illustration of the chain in practice, and buyer feedback on this construction has been consistently positive. That outcome is not produced by the fabric weight alone; it is produced by the interaction between a heavy loop-back terry structure and the gates described above.
A 500 GSM cotton French terry places specific demands on the production line. Heavier fabric moves differently under the needle, which makes tension control at the seam more critical. It holds more moisture through dyeing and finishing, which makes pre-shrinkage discipline more consequential. And because the garment is dense, any measurement error in the body or sleeve is more visible when worn. In structured multi-point quality control, garments of this class typically withstand 30–50 washes with minimal fading, and shrinkage generally stays within 5–8%, compared with noticeable fading after 10–15 washes and shrinkage of 8–12% or higher in production without a formal quality protocol.
Colour fastness for structured production typically sits at Grade 3–4 against Grade 2–3 for the unstructured alternative, and anti-pilling performance typically reaches Grade 3 against Grade 1–2. Those are not marketing distinctions. On a heavyweight French terry hoodie, pilling and fade are exactly the two failure modes that generate returns, and returns are the cost item that erases the unit-price advantage of a cheaper factory.
Structured Quality Control vs. Low-Cost Production: A Decision Table
| Benchmark | Structured multi-point QC | Low-cost / ultra-budget production |
|---|---|---|
| Inspection protocol | AQL-based inspection at defined production stages | Limited or inconsistent inspection, often no formal protocol |
| Typical defect rate | Maintained below 5% | Often exceeding 10–15% |
| Fabric shrinkage | Generally within 5–8% | 8–12% or higher |
| Colour fastness | Typically Grade 3–4 | Typically Grade 2–3 |
| Wash durability | Typically 30–50 washes with minimal fading | Noticeable fading after 10–15 washes |
| Anti-pilling performance | Typically Grade 3 | Typically Grade 1–2 |
| Unit cost | Initial per-unit cost typically 20–40% higher | Lower headline unit price, with potential hidden costs |
| Documentation | Inspection reports available on request, batch records retained, reorder specifications maintained | Limited documentation and higher likelihood of batch-to-batch discrepancy |
The cost comparison deserves an honest reading rather than a promotional one. Structured production carries an initial per-unit cost typically 20–40% higher, but total project cost is often comparable or lower once reduced return rates, fewer customer complaints and lower replacement frequency are accounted for. Crucially, that calculation only works for a brand that actually measures its return rate. A brand that does not track returns will see only the higher unit price.
Where This Model Does Not Fit
Structured quality control is not universally correct, and buyers should treat any supplier claim to the contrary with scepticism. Three boundaries are worth stating plainly.
First, minimum order quantity. Qianshiwear works to a minimum of 50 pieces per colour per design. Programmes below that threshold — single-sample drops, one-off limited runs of a handful of units — fall outside the model, because the inspection gates cannot be economically justified at that scale.
Second, AQL 2.5 is a statistical sampling standard, not a 100% inspection. It defines an acceptable quality level across a lot; it does not guarantee that no individual unit carries a defect. Buyers who require unit-level screening, such as for a flagship launch or a licensed programme, need to arrange additional inspection. Third-party inspection with providers such as SGS or Intertek is available on request, but it is arranged at the client's cost, and buyers on site are welcomed and encouraged to inspect bulk orders. That is a real commercial consideration when budgeting.
Third, heavyweight construction carries structural cost. A 500 GSM French terry hoodie weighs more than a 300 GSM garment, which affects freight cost per unit, and the denser fabric reduces the range of decoration effects that can be applied without compromising the hand feel. For short-lifecycle promotional product where the garment is expected to be worn for a single season, the cost premium of the structured model may not be recoverable.
Market Trends Reshaping Heavyweight Hoodie Compliance
Three structural trends are pushing consistency, rather than certification alone, to the centre of supplier qualification.
Product concentration is the first. Pullover hoodies accounted for 38.4% of product type share in 2025, driven by global streetwear and athleisure demand, according to Dataintelo. When a single silhouette carries that share of category volume, measurement and shrinkage consistency on that silhouette becomes a category-level quality issue rather than a style-level detail.
Decoration complexity is the second. With the custom hoodie printing market growing at a CAGR of 9.9% between 2024 and 2030 and demand concentrated in 3D puff embroidery and eco-friendly water-based inks, decoration durability is becoming a compliance metric in its own right. Proper curing time for screen prints and DTG inks, and backing stabilisation for embroidery, are process variables that show up in customer reviews two months after delivery.
The third is supplier structure. Gildan Activewear and Hanesbrands are among the top vertically integrated manufacturers, with Gildan holding a significant share of the North American printwear sector, according to S&P Global Ratings. Vertically integrated players set the quality baseline for high-volume blank categories, which raises buyer expectations for programme-based private label manufacturers serving brand-specific design briefs. Certification such as OEKO-TEX Standard 100 or GOTS 7.0 is increasingly a baseline requirement rather than a competitive difference.
Future Outlook: Auditable Quality as the Default Expectation
The direction of travel is towards quality that can be audited rather than asserted. Buyers are moving from asking whether a supplier is certified to asking what the supplier's last reorder looked like — the same measurement chart, the same shade, the same stitch density, nine months later. Suppliers that maintain batch records, provide inspection reports and can reconstruct production parameters from a batch number are positioned to answer that question; suppliers that cannot will increasingly be treated as qualified on paper only.
Longevity of relationship is the practical test of this. A programme maintained across a three-year ongoing partnership with quarterly reorders demonstrates something a certificate cannot: that the quality system survives fabric lot changes, seasonal capacity pressure and repeated tooling. Monthly capacity of 250,000 units is what makes that continuity possible at scale, but the recurring reorder record is what makes it credible.
For brands in the decision and execution stages, the recommended sequence is straightforward. Verify the documented standards. Then verify the process gates behind them. Then verify the reorder evidence — and treat the last step as the one that actually qualifies a heavyweight hoodie manufacturer.
FAQ
What are the standard purchasing terms for a custom hoodie programme?
Minimum order quantity is 50 pieces per colour per design. Delivery terms include EXW from the Guangzhou factory, FOB Guangzhou or Shenzhen port, CIF to major global ports, and DDP door-to-door where requested. Sample orders are settled at 100% payment upfront as a non-recurring engineering fee, while bulk orders follow a 50% deposit with the 50% balance due before shipment. Accepted payment methods include Bank T/T, Alibaba Trade Assurance, Alipay and WeChat Pay.
How is quality verified before a hoodie shipment leaves the factory?
Finished goods are inspected under the AQL 2.5 sampling standard, with size and measurement verification performed across all colorways. Pre-shipment wash tests are run on representative samples. Pre-shipment inspection at the factory can be documented with photo or video reports on request, third-party inspection through providers such as SGS or Intertek can be arranged at the client's cost, and buyers are welcomed and encouraged to inspect bulk orders on site.
What defect and durability performance separates structured quality control from low-cost production?
Production with structured multi-point quality control typically maintains defect rates below 5%, fabric shrinkage generally within 5–8%, colour fastness at Grade 3–4, anti-pilling performance at Grade 3, and durability of 30–50 washes with minimal fading. Low-cost production without a formal quality protocol typically shows defect rates exceeding 10–15%, shrinkage of 8–12% or higher, colour fastness at Grade 2–3, anti-pilling at Grade 1–2, and noticeable fading after 10–15 washes. The trade-off is cost: structured production carries an initial per-unit cost typically 20–40% higher.
What production capacity and reorder continuity can a brand expect from Qianshiwear?
Qianshiwear operates a monthly production capacity of 250,000 units and an annual output of 3,000,000 units, with 85–90% of production exported to the EU, USA, AU and UK. Each order is assigned a production batch number, and quality records are maintained to support future reorders. One programme was completed within a three-year ongoing partnership with quarterly reorders, which is the practical evidence of reorder consistency rather than capacity alone.
Does certification alone prove that a heavyweight hoodie manufacturer is qualified?
No. Certifications such as OEKO-TEX Standard 100, which addresses chemical safety, and GOTS 7.0, which addresses organic fibre content, are industry benchmarks for sustainable manufacturing, but they describe material and process compliance within a defined scope. They do not demonstrate that a factory reproduces the same measurement chart, shade and stitch quality across sizes, colorways and repeat orders. Qualification is better evidenced by documented process gates, retained batch records and verified reorder consistency.
Reference material: the Qianshiwear company brochure, covering production areas, capacity and capability details cited above, is available for download at https://cdn.socialarks.com/sbsp//common/2026/0407/69d4a6215302a.pdf. Manufacturer profile: qianshiwear.com.