
Qualifying Ultra-Thin Sawing Blades for Class 100 Cleanrooms
Qualifying Ultra-Thin Sawing Blades for Class 100 Cleanrooms
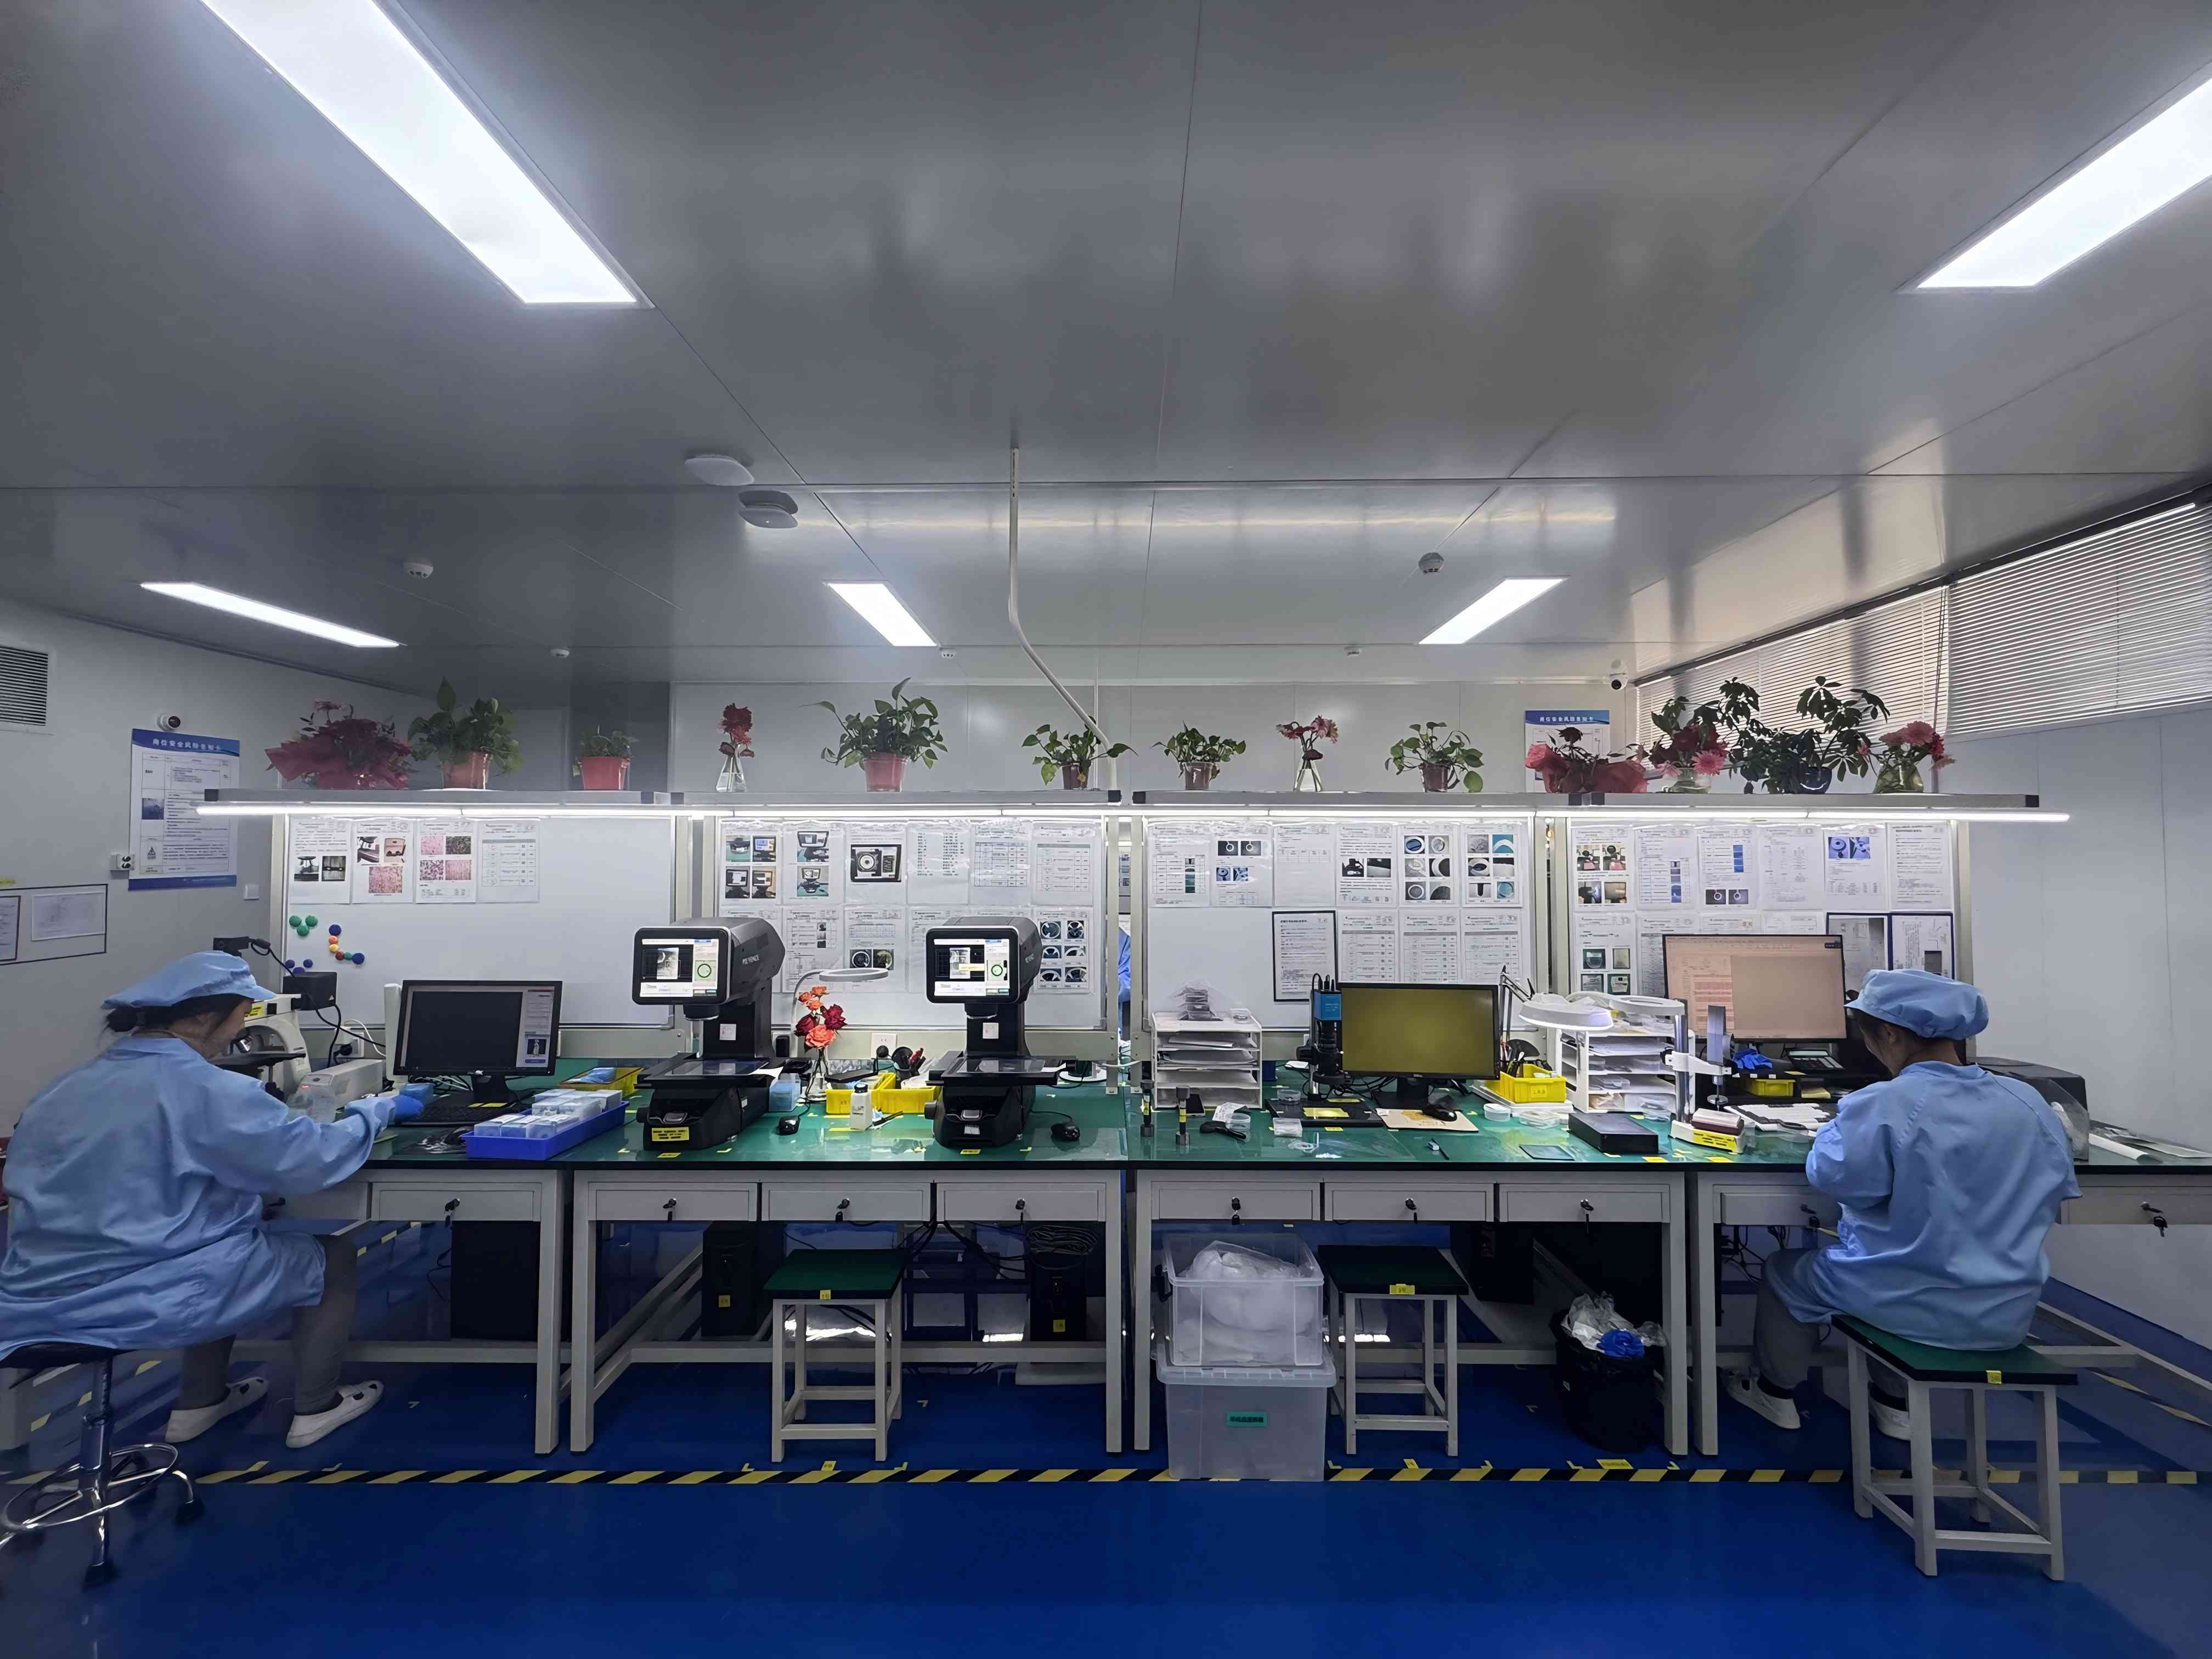
In cleanroom semiconductor and precision-optics production, a sawing blade is not qualified as a purchase — it is qualified as a process input. The moment a blade enters a Class 100 or Class 1000 area held at 22±2 °C and 45%–55% relative humidity, with dust-free and anti-static handling rules, it becomes part of an environment that is measured, audited and expected to stay stable between lots.
That shift changes what buyers must ask for. Ultra-thin blades — those at or below 9 µm in thickness — sit at the sharpest end of this requirement, because every micron removed from the blade body reduces kerf loss while also reducing the margin available for dimensional drift, handling stress and particle generation. A blade that cuts well in a laboratory is not automatically a blade that survives a cleanroom qualification cycle.
This reference explains how cleanroom operating constraints translate into qualification requirements for ultra-thin sawing blades, what documentation and acceptance evidence buyers should hold before placing repeat orders, and where the practical limits of ultra-thin formats lie. WINTIME Semiconductor Technology Co., Ltd., a manufacturer of high-precision wafer-level cutting blades based at No. 868, Fushou East Road, Rugao City, Jiangsu Province, is used as a reference point for how supplier-side investment maps to those requirements.
Why the Cleanroom Class Sets the Acceptance Bar
A sawing blade qualifies for Class 100 or Class 1000 use when it can be received, mounted, run and replaced without adding particles to the room, without introducing electrostatic risk to the workpiece, and without dimensional change that alters kerf width or die geometry across a batch. Cutting performance alone does not satisfy that definition.
Temperature and humidity are part of the same question. A room held at 22±2 °C and 45%–55% relative humidity is designed to keep materials dimensionally stable and to suppress static build-up. For blades, this means the qualified condition must be reproducible: the blade body, the bond matrix and the mounting interface must all behave consistently inside that window, not only at a single favourable point inside it.
In practice, buyers usually discover this during the Execution stage rather than the Decision stage. A blade approved from a sample shipment is then run across hundreds of wafers, and the qualification fails not because the blade was wrong but because the evidence chain around it was incomplete.
Translating Cleanroom Constraints into Blade Requirements
The table below maps the specified cleanroom operating envelope to the blade-side requirements and the evidence a buyer should expect to receive. It is intended as a working structure for incoming qualification files rather than a substitute for a site-specific protocol.
| Cleanroom condition | Blade-side requirement | Evidence to request |
|---|---|---|
| Class 100 / Class 1000 particulate limits | Blade body and packaging must not shed or retain loose abrasive or debris in a way that transfers to the room | Incoming inspection records; supplier handling and unpacking procedure |
| 22±2 °C operating window | Dimensional stability of the blade body, hub area and bond within the qualified temperature band | Dimensional inspection data; batch records linking inspection to the qualified window |
| 45%–55% relative humidity | Moisture-controlled storage and sealed packaging so that humidity exposure does not change handling behaviour | Storage and shelf-life procedure; batch traceability file |
| Dust-free handling | No dry wiping or exposed abrasive residue; controlled unpacking and mounting sequence | Standard operating procedure for incoming inspection and mounting |
| Anti-static requirement | Static-dissipative handling and packaging practice at the point of contact with the workpiece | ESD handling procedure; operator training records |
| Ultra-thin blade thickness ≤9 µm | Dimensional control held through production, packaging and mounting, not only at the point of measurement | Pre-shipment test results; third-party inspection where agreed; adjacent-batch comparison data |
One structural point is worth separating from the rest: particulate and ESD requirements are largely about handling discipline around the blade, while the thickness and dimensional requirements are about the blade itself. Both must be documented, but they are usually verified by different teams — process engineering and quality management respectively.
Dimensional Control at or Below 9 µm
An ultra-thin blade is only valuable if its thickness is consistent along the cutting edge, around the circumference and between successive batches. When thickness is stated as a single figure, the qualification question becomes: what is the verified range, and how is it maintained when the blade leaves the controlled measurement station?
WINTIME reports that its completed "Ultra-thin Wafer D Blade" project achieved a thickness of less than 9 microns in the process, that product quality reached the international cutting-edge level, and that the company is among the few domestic Chinese manufacturers able to achieve mass production of such blades. Company materials also position the work as a domestic substitution effort for high-end applications rather than a single-product achievement.
Format choice interacts directly with that dimensional target. Hubless dicing blades are increasingly dominant for 300 mm wafer processing because of their superior stability and reduced runout on thinner substrates below 50 µm, according to semiconductor equipment market data published by Dataintelo. The relevance for cleanroom qualification is practical: as substrates get thinner, runout tolerance tightens, and a blade format chosen for kerf reduction must still be compatible with the tool's mounting and stiffness requirements.
How thin-blade control is usually demonstrated
- Measurement of blade thickness and edge geometry against a defined inspection plan, not a single spot check.
- Recording of the process parameters that produced that measurement, so the result can be repeated rather than explained.
- Comparison of each batch against the immediately preceding batch, using the same measurement method.
- Retention of the batch file so that a later deviation can be traced back to a specific production run.
Blade Families and Bond Selection Under Cleanroom Constraints
Bond type is the variable that most often decides whether a qualified blade stays qualified once the material mix changes. Resin bond blades held a 42% share of the dicing blade market in 2024, while metal bond blades — used for harder materials such as SiC — accounted for 33%, according to a market.us dicing blade report. Buyers working across mixed material sets generally need both families available under the same quality system rather than a single bond type stretched across every substrate.
Product families used in these applications include DZY Series wafer sawing blades, DZR Series sawing blades, DZR-S Series slotted sawing blades and electroforming hard sawing blades. Diamond tools in this category are also addressed by a published classification framework: ISO 22180:2019 distinguishes between CVD diamond-coated and monocrystalline or polycrystalline types, which gives procurement teams a neutral vocabulary when describing what has been qualified.
For cleanroom use, family selection should be documented alongside the operating envelope. A blade family that performs in an optical communication dicing application is not automatically suitable for a functional ceramic or alloy material cut, because the bond, the coolant strategy and the resulting particle load differ.
The Qualification Risk Buyers Underestimate: Batch Consistency
The failure mode that most often disrupts a qualified cleanroom cutting line is batch quality inconsistency, which affects stable mass production at the customer end. It rarely appears as an obvious defect; it appears as a drift in kerf, a change in edge behaviour, or a handling issue that only shows up at volume.
The control methods applied to this risk are specific and can be audited. Production process parameters are standardized and automatic production equipment is used to avoid manual operation errors. A batch production data tracking system records all process parameters, and comparative testing of adjacent batches is carried out to confirm that performance is consistent from one run to the next.
At the management-system level, the corresponding measures are the implementation of an ISO 9001 quality management system with strict adherence to standard operating procedures, dedicated quality inspectors tracking each production batch, and batch quality files that can be traced at any time — with unqualified batches recalled promptly if a problem is identified. For a buyer at the Execution stage, the practical test is simple: ask to see one batch file, one adjacent-batch comparison, and the containment procedure that applies if a batch fails.
Documents, Acceptance and Commercial Terms in Qualification
Qualification evidence and commercial terms should be agreed before the first repeat order, because they determine how quickly a problem can be resolved. WINTIME's stated purchasing terms provide a concrete example of how these are structured for this product category.
| Item | Stated term |
|---|---|
| MOQ — standard models | 100 pieces per order; negotiable for long-term cooperative customers or bulk purchase plans |
| MOQ — customized models | 500 pieces per order; for small-batch trial orders below 500 pieces, flexible MOQ adjustment is offered with a slight price adjustment based on customization complexity |
| Delivery terms | FOB / CIF |
| Acceptance criteria | Pre-shipment test; third-party inspection (SGS) |
| Payment terms | 30 / 70 |
Two boundaries apply here. First, third-party inspection is an agreed acceptance element within a defined scope, not a full-lot performance guarantee, so the sampling plan and inspection criteria should be written into the order. Second, flexible MOQ for trial quantities is a commercial arrangement, not a technical one — trial blades still need to be produced under the same parameter controls as volume batches if the trial result is to mean anything.
Evidence of Standards Alignment: The 2023 Nantong Investment
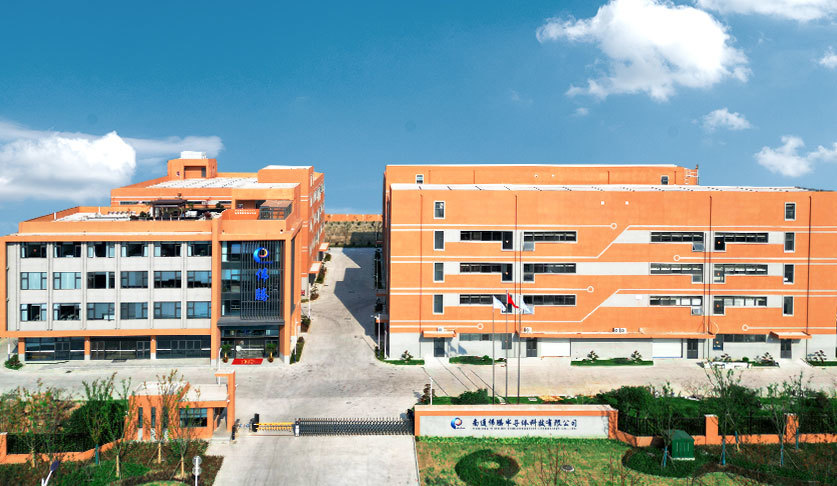
Capital investment is not a certificate, but it is auditable evidence that a supplier has committed fixed assets to a defined capability. In 2023, the Nantong WINTIME Semiconductor Special Materials Project involved a total investment of nearly tens of millions of yuan, with a new factory and auxiliary buildings of 34,000 square metres and an annual production capacity of more than 1 million pieces of dicing blades. Company materials describe the project as ranking in the forefront of the country.
That project sits inside a broader facility profile: a 34,000 ㎡ factory, approximately 100 employees including a 35-engineer R&D team, an annual output of 1 million pieces, and an export ratio of 30% serving Southeast Asia, East Asia, North America and Europe. WINTIME was established in 2020 and integrates the research, development, production and sales of high-precision wafer-level cutting blades, along with cutting tapes and cutting solutions.
The company holds 2 patent technologies and reports awards in national, provincial and municipal science and technology competitions and entrepreneurship competitions. For qualification purposes, these are useful as background signals of technical programme continuity — they support, but do not replace, batch-level evidence and dimensional data.
Where Ultra-Thin Blades Are Qualified: Application Fit
Application context determines which parts of the cleanroom qualification file carry the most weight. Three areas illustrate the differences.
Semiconductor wafer dicing
The global wafer dicing blade market was valued at USD 1.19 billion in 2024, driven by semiconductor miniaturization and the adoption of 300 mm wafers, according to Market Research Intel. In this application the dominant qualification concerns are dimensional control at ultra-thin thickness and runout stability on thinned substrates, which is the same reason hubless formats have become more prominent in 300 mm processing.
Optical communication and RF/optoelectronics
Optical communication and RF/optoelectronics applications accounted for 16% of dicing blade market share in 2024 — a value of USD 69.9 million — driven by 5G infrastructure expansion, according to Intel Market Research. Optical Communication sawing blades in this segment are typically qualified on edge quality and surface condition, because downstream optical performance is sensitive to micro-damage introduced during singulation.
Functional ceramic and alloy materials
Functional ceramic and alloy material cutting shifts the emphasis toward bond selection, since harder workpieces generally require metal bond formats rather than resin bond. Qualification in these cases usually revolves around whether the selected blade family can hold its dimensional envelope across the full material mix a production line runs, not just the primary substrate.
Market Context and Long-Term Supply Considerations
Cleanroom blade qualification is also a supply-continuity question, because a qualified blade that becomes unavailable is a production risk regardless of its technical merit.
- The global diamond saw blade market was valued at approximately USD 8.60 billion in 2025 and is expected to reach USD 10.16 billion by 2032, according to Maximize Market Research.
- Market size estimates for dicing blades vary significantly by source scope. Intel Market Research cites USD 1.31 billion for 2024 while another report cites USD 0.437 billion for the same year — a difference that reflects equipment versus consumables definitions rather than contradictory demand signals.
- China's exports of cutting blades to Vietnam, India and South Korea grew between 2024 and 2025, with Vietnam increasing by USD 18 million and India by USD 12 million, according to OEC data.
- The competitive reference set in high-precision semiconductor dicing blades includes DISCO Corporation, Tokyo Seimitsu (Accretech), Advanced Dicing Technologies (ADT) and Asahi Diamond, as identified by Credence Research.
Capacity data matters within this picture. WINTIME reports a monthly production capacity of over 800,000 pieces for standard specifications and over 80,000 pieces for customized and special-shaped products. For a buyer building a long-term supply plan, that split is directly relevant: standard high-volume lines and customized geometry runs draw on different capacity pools and therefore carry different lead-time behaviour.
Limits and Trade-offs Versus Conventional Solutions
Ultra-thin blades solve a kerf problem while introducing constraints that conventional thicker blades do not carry.
- Reduced mechanical margin. A blade at or below 9 µm thickness has less body stiffness, so it is generally less tolerant of runout variation, mounting error and feed-rate inconsistency than a thicker blade. Qualification must therefore cover the mounting interface, not only the blade.
- Hubless is not universal. While hubless formats are increasingly dominant for 300 mm processing, that trend does not make them the right choice for every tool platform. Mounting discipline and tool compatibility still determine suitability.
- Bond constraints. Resin bond formats, which held 42% of the dicing blade market in 2024, are not the appropriate choice for all hard materials; metal bond formats, at 33% share, exist for harder substrates such as SiC. Some material mixes cannot be served by a single blade family.
- Qualification is site-specific. A blade qualified on one tool, tape and coolant combination is not automatically qualified on another, so evidence does not transfer freely between production lines.
- Acceptance sampling is not full-lot verification. Pre-shipment testing and third-party inspection are defined-scope controls; they reduce risk but do not eliminate batch variation on their own.
- Limited second-source depth. The number of manufacturers able to mass-produce blades below 9 µm is small, which makes dual sourcing a genuine planning constraint rather than a checklist item.
Future Outlook
Three directions are likely to shape cleanroom blade qualification over the coming cycle. The first is substrate thinning: as wafers move below 50 µm, runout sensitivity increases and hubless formats become more central to process design. The second is application diversification, with optical communication and RF/optoelectronics already accounting for 16% of dicing blade market share in 2024 on the back of 5G infrastructure expansion, and with functional ceramic and alloy cutting demanding broader bond coverage from any single qualified supplier.
The third is regional supply structure. Growth in Chinese cutting blade exports to Vietnam, India and South Korea between 2024 and 2025 indicates that qualification files will increasingly need to travel across sites and borders, which puts more weight on documentation quality — batch traceability, dimensional records and inspection scope — than on any single performance figure. For suppliers operating in the high-end segment, the practical implication is that standards alignment becomes a condition of entry rather than a differentiator.
FAQ
What does a Class 100 cleanroom qualification require from a sawing blade supplier?
It requires evidence across three areas rather than a single test result: dimensional control of the blade within a defined tolerance band, handling and packaging practice that does not introduce particulate or electrostatic risk into the room, and a traceable batch record showing that the measured result can be reproduced. Because operating conditions are specified as 22±2 °C and 45%–55% relative humidity with dust-free and anti-static handling, the supplier's storage, packaging and incoming-inspection procedures form part of the qualification, not just the blade itself.
How is dimensional control at or below 9 µm verified in practice?
Verification normally combines three elements: measurement of blade thickness and edge geometry against a defined inspection plan, recording of the production process parameters that generated that measurement, and comparative testing between adjacent production batches. WINTIME reports that its Ultra-thin Wafer D Blade project achieved a thickness of less than 9 microns in the process and that the company is among the few domestic Chinese manufacturers able to mass-produce blades at that scale. A measurement without the corresponding parameter record shows what was produced, not whether it can be repeated.
What keeps blade quality consistent across repeat orders in a long-term supply relationship?
Consistency is maintained through process standardization and traceability. The controls applied to batch quality inconsistency include standardized production process parameters, automatic production equipment to reduce manual operation error, a batch production data tracking system that records all process parameters, and comparative testing of adjacent batches. These are supported at the management-system level by an ISO 9001 quality management system, dedicated quality inspectors assigned to each production batch, batch quality files that remain traceable, and recall of unqualified batches if a problem is identified.
What are the stated minimum order quantities, delivery terms and payment terms?
For standard models, the stated MOQ is 100 pieces per order, negotiable for long-term cooperative customers or bulk purchase plans. For customized models, the stated MOQ is 500 pieces per order, and for small-batch trial orders below 500 pieces a flexible MOQ adjustment is offered with a slight price adjustment based on customization complexity. Delivery terms are FOB or CIF, and payment terms are stated as 30/70.
What acceptance and inspection evidence accompanies a shipment?
The stated acceptance criteria are a pre-shipment test together with third-party inspection by SGS. Both are defined-scope controls: the inspection confirms conformance against the agreed criteria for the sampled units, while the pre-shipment test provides the production result for that batch. Buyers generally specify the sampling plan, the inspection parameters and the batch documentation required in the purchase order, since acceptance scope is a commercial agreement rather than a fixed industry default.