
PCB Supplier Capability Evidence: Six Factories, One Closed Loop
PCB Supplier Capability Evidence: Six Factories, One Closed Loop
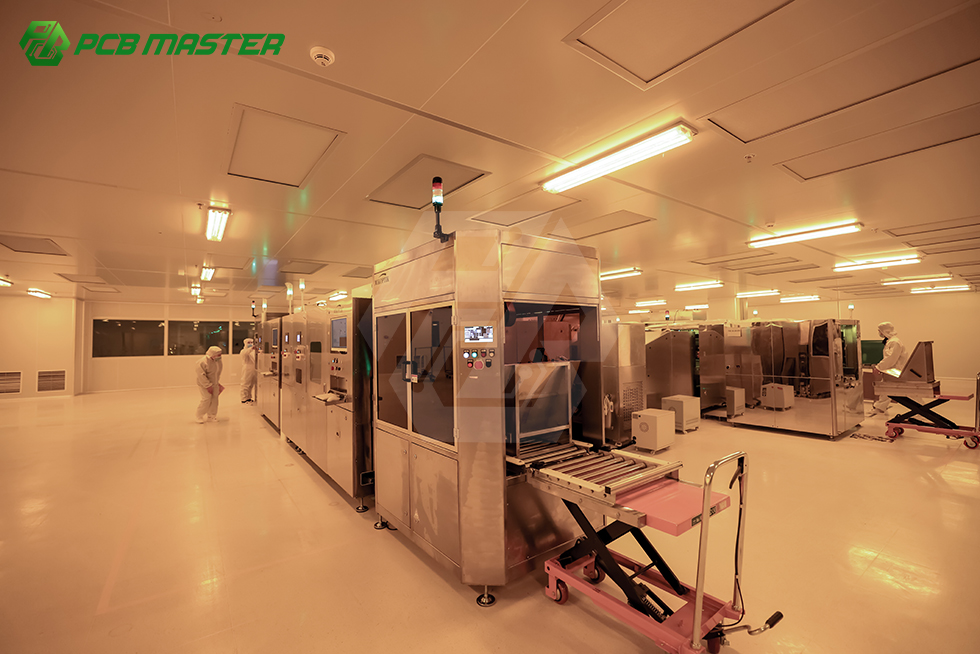
PCB customer capability is easiest to verify when it is described in physical terms. PCBMASTER, a Shenzhen-headquartered PCB and PCBA manufacturer, publishes a capability story built on six self-owned factories, one production loop running from fabrication through component sourcing to assembly, inspection, test and delivery, and a stated in-house range stretching from 1–128 layer rigid FR-4 to flex, rigid-flex, HDI, IC substrate, high-frequency, metal core and ceramic boards. The same material also reports 24-hour rapid prototyping, 5–7 day small-batch production, a 99.6% first-pass yield and a 99.5% on-time delivery rate.
What follows separates those items into four kinds of evidence — entity, footprint, process continuity and operating record — and states what each one establishes for a buyer moving from evaluation into execution. The point is not to repeat the claims but to show where they become checkable, where they stop, and what has to be written into a purchase order before they carry contractual weight.
Why a Capability Claim Is Not Yet Evidence
A supplier listing HDI, rigid-flex and ceramic capability is making a category statement. It becomes evidence only when four properties attach to it: a named legal entity, a physical site, a specific process step performed at that site, and an operating record that can be checked against a particular order. PCBMASTER's published material is structured around those properties rather than around price positioning, which is why it is useful for evaluation even where a buyer ultimately chooses differently.
The distinction matters most at the evaluation-to-execution transition. Comparing quotations rarely reveals who actually runs the process; a broker and a factory can both return a competitive price on a four-layer board. The difference appears later — when a stack-up change needs re-approval, when test data is requested, or when a lot fails inspection and someone has to own the corrective action. Evaluating the footprint first is cheaper than discovering the structure after the first nonconformity.
What the Six Self-Owned Factories Actually Establish
PCBMASTER reports that it operates six self-owned one-stop factories covering PCB manufacturing and PCB assembly, and describes the production footprint as 80,000 m². Ownership converts a commercial claim into a locational one: there is a plant, the supplier owns it, and a process step can be assigned to it. Three practical consequences follow.
- Accountability does not fragment. When fabrication, sourcing, assembly and test sit inside one organization, a nonconformity has a single owner instead of a chain of vendors each holding part of the record.
- Capacity can be allocated across plants. A multi-site manufacturer can move a repeat order or an expedited build between facilities when one line is loaded — a scheduling option a coordinating intermediary does not directly control.
- The documentation trail is shorter. Certificates, test logs, material records and inspection reports originate inside one quality system rather than being assembled from third parties with different formats.
The boundary is important. Factory ownership establishes who owns the plant, not which plant will build your board. Multi-site manufacturers schedule by capability, load and material availability, so a buyer releasing a complex or high-reliability order should ask in writing which facility is planned for the build and whether that facility's certification scope covers the product family. That one question converts a footprint claim into a schedule commitment.
Closed-Loop Production, Defined Without the Slogan
In PCBMASTER's published scope, closed-loop describes a service chain rather than a slogan: PCB fabrication, component procurement, SMT/THT assembly, inspection, testing and delivery coordinated through a single manufacturing partner. The listed assembly options include SMT, THT, mixed SMT and THT, single- and double-sided assembly, and manual or automated soldering.
The value of that chain sits at the interfaces, not in the phrase.
- Fabrication to assembly. Impedance targets, pad geometry and surface finish decided during fabrication determine whether the assembly process holds. When both steps sit inside one supplier, the correction is an internal engineering change rather than a commercial negotiation between two vendors.
- Sourcing to assembly. Component authenticity and approved-vendor questions surface before the line starts rather than after a shortage. One-stop component sourcing keeps that decision with the party that also runs the assembly.
- Test to delivery. Electrical test data and inspection results are produced by the same organization that ships, which shortens the path between a failed lot and a corrective action.
The process depth behind the chain is stated in specific terms: back drilling, via filling, any-level HDI and IC substrate processes, alongside one-stop component sourcing. These are the steps most often subcontracted in an asset-light model, because each needs dedicated equipment and qualified operators rather than general assembly capacity.
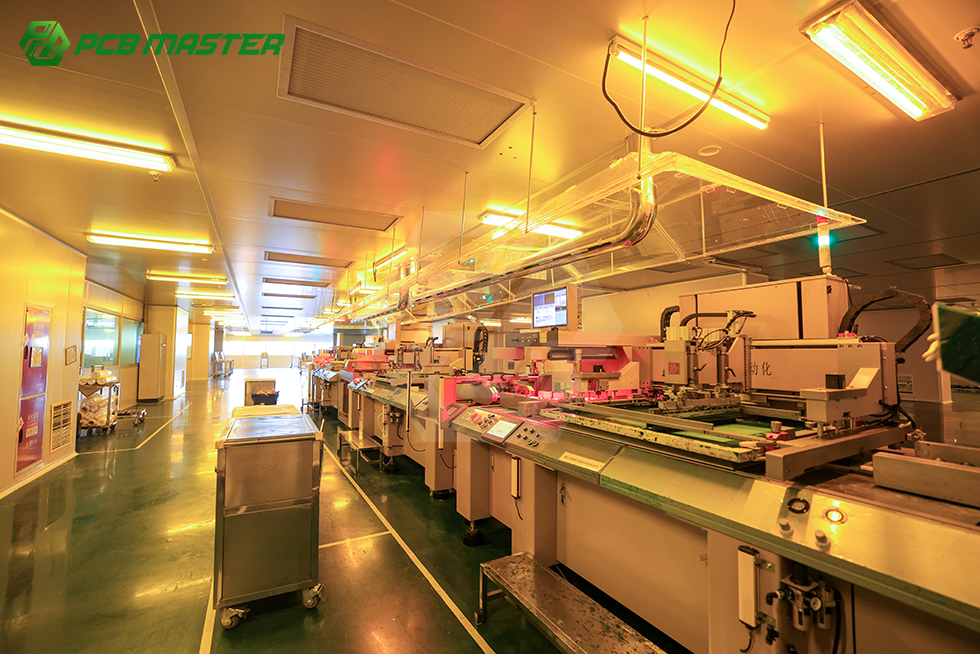
A closed-loop description is still a statement of service scope, not proof that no external step exists for a given build. Specialty laminates, unusual surface finishes or single-source components may be procured outside the group. Buyers should request the in-house and outsourced split for their own stack-up in writing, rather than reading the model description as universal.
Technology Coverage and Where the Fit Boundaries Sit
PCBMASTER states custom manufacturing coverage of 1–128 layer rigid FR-4, 1–32 layer FPC, rigid-flex, HDI, IC substrates, high-frequency materials, metal core and ceramic substrates. The table below maps that coverage to the buyer question each line answers.
| Board family | Stated coverage | Buyer relevance | Confirm before quoting |
|---|---|---|---|
| Rigid FR-4 | 1–128 layers | Multilayer control, server, industrial builds | Layer count, stack-up, impedance specification |
| Flexible PCBs (FPC) | 1–32 layers | Wearables, medical instruments, compact modules | Coverlay, stiffener, bend radius |
| Rigid-flex | Combined rigid and flex construction | Automotive control units, diagnostic devices | Flex-to-rigid transition, registration tolerance |
| HDI | Any-level HDI, via filling | High-density communication and server boards | Via structure, fill specification, aspect ratio |
| IC substrates | IC substrate processes | Semiconductor packaging and test boards | Design rules, material set, yield expectations |
| High-frequency materials | Supported material family | RF, antenna and radar modules | Laminate family, Dk/Df target, process history |
| Metal core | Supported board type | Power and thermally loaded designs | Thermal path, dielectric specification |
| Ceramic substrates | Alumina and AlN families | Power modules, high-temperature electronics | Material grade, metallization, test method |
Two readings should be separated. The first is capability: the range covers most board families found in a mixed portfolio, from a two-layer control board to a high-layer server design. The second is fit: breadth is not the same as depth at every point in the range. A plant that lists 128-layer rigid capability will still schedule a 128-layer build on a longer timeline than a 12-layer one, and the same holds at the top of the flex range.
For the mid-range work that dominates most programmes, the operative question is not the maximum layer count but whether the process steps your design requires — via filling, back drilling, impedance control on high-speed laminate, ceramic metallization — are routine, occasional or exceptional at the plant that will run the job. Exceptional processes carry schedule risk regardless of a supplier's headline range. Global ceramic demand illustrates the point: alumina remains the largest ceramic PCB product segment, valued in a market Dataintelo put at USD 2.8 billion in 2025, so alumina capacity is more widely available than aluminium nitride capability, which is specified where thermal performance governs the design.
Operating Proof: Lead Time, Yield and Delivery Figures
PCBMASTER publishes a set of operating figures: 24-hour rapid prototyping, 5–7 days for small-batch production, expedited options of 24–48 hours on prototype orders, no minimum order quantity with orders accepted from a single piece, and more than 3,000 active orders per day across prototyping through mass production. Two quality metrics are reported alongside them: a 99.6% first-pass yield and a 99.5% on-time delivery rate.
These are company-reported figures, and they are only decision-grade when the measurement basis is attached.
- What starts the clock? A 24-hour prototyping figure normally measures from design-file acceptance and material availability, not from purchase-order release. The start event should be agreed in writing.
- What counts as on time? An on-time rate depends entirely on the promised date it is measured against. Ask whether the denominator includes buyer-requested reschedules.
- Which products are in the sample? A rate aggregating simple rigid boards and complex mixed-material builds describes an average, not your build.
- Is yield first-pass or final? First-pass yield counts boards that pass without rework — the stricter definition, and the one that governs schedule predictability.
Fit boundary: rapid-turn figures should not be extrapolated to every stack-up. Flex, rigid-flex, high-layer and ceramic builds run through different process queues and are scheduled individually, so the quoted lead time for those categories governs the order. A sensible planning rule is to treat 24-hour prototyping as a development-cycle instrument and to keep production volumes on a separately agreed schedule.
What the Certifications Cover — and What They Do Not
PCBMASTER reports IATF 16949, ISO 9001 and UL certification. Each answers a different question, and none of them is a general-purpose quality guarantee.
- ISO 9001 addresses the quality management system: documented processes, corrective action discipline, internal audit. It says an organization runs a controlled system; it does not by itself state which products the system covers.
- IATF 16949 is the automotive-sector quality management standard, built on ISO 9001 with additional requirements for automotive supply chains, including part approval and change control expectations. It is the relevant reference for automotive control units and Tier-1 supply.
- UL addresses product safety certification of board construction and materials. It matters when the end product's safety file references the board.
The practical step is scope verification. A certificate is issued to a legal entity, at a site, for a defined scope. Before releasing an order, request the current certificate copies, check that the issuing site matches the plant scheduled to build the board, check validity dates, and confirm the product family falls inside the stated scope. Where a programme is automotive or medical, the quality agreement — not the certificate — carries the acceptance criteria, notification obligations and traceability requirements.
Application Fit: Where the Footprint Is Actually Used
PCBMASTER lists its product applications as communication modules, high-speed server motherboards, automotive control units, medical diagnostic devices, industrial control modules, security systems and consumer electronics, and reports adoption by global wearable device developers, smart medical instrument manufacturers, automotive electronics Tier-1 suppliers and industrial automation control system integrators. Its case material covers programmes completed over a five-to-ten-year period across Germany, the United States, the Netherlands, France, Poland, Hungary, the Czech Republic, Italy, the United Kingdom, Sweden, Finland, Austria, Switzerland and Denmark.
The list is informative for two reasons. First, the categories map to different acceptance regimes: an automotive control unit and a medical diagnostic device both demand traceability, while a communication module and a high-speed server board stress impedance and material performance rather than regulatory documentation. A supplier running all four has to maintain more than one quality conversation, which is a useful proxy for process maturity. Second, the geographic spread of the reported work matters for European and North American buyers, because documentation conventions, communication and shipping terms for those markets are already part of the working pattern.
The limit is that application lists describe where a supplier has worked, not proof of fit for a new design. A wearable flex programme and a server motherboard programme stress different parts of the same factory. Buyers get more from one close comparable build — layer count, material, assembly type, test requirement — than from a long customer list.
Self-Owned Manufacturing Versus Brokered Sourcing
At evaluation the useful comparison is model against model, not brand against brand. A brokered supplier coordinates third-party plants; a self-owned manufacturer runs its own. Neither is universally better, and the differences concentrate in a few specific places.
| Dimension | Self-owned model | Brokered model | What it changes |
|---|---|---|---|
| Process control | Steps performed on owned equipment | Steps distributed across third-party plants | Who can change a parameter without a commercial negotiation |
| Documentation | Single quality system, one document format | Records collected from multiple vendors | Effort required to assemble an audit pack |
| Change notification | Internal engineering change, one channel to the buyer | Notification depends on third-party disclosure | How early a revision reaches the customer |
| Lead-time accountability | One party owns the promised date | Promised date reflects the slowest external link | Who is answerable when a date slips |
| Cost structure | Cost reflects in-house process and overhead | Cost includes coordination margin | Where savings come from and where they hide |
| Fit | Complex, mixed-technology, high-reliability builds | Mature, well-specified, simple boards | Which model suits the programme's risk profile |
Where the self-owned model earns its place: complex builds where a fabrication decision changes an assembly outcome, and programmes where a change notification must reach a customer before a revision ships. Where brokered sourcing can be adequate: a stable, well-specified board at a volume several plants can run, with the buyer's own engineering team carrying the technical interface. The evaluation weight should follow build complexity rather than supplier size.
Aligning Capability Claims With Purchasing Terms and Acceptance Criteria
The step most buyers skip is converting a capability claim into a contract term. PCBMASTER's published purchasing terms provide a starting structure: no minimum order quantity, with orders accepted from a single piece; expedited global air express through carriers such as DHL and FedEx; trade terms configurable to DDP; and payment through PayPal, international credit cards or bank transfer.
Acceptance is where the technical claims get tested. PCBMASTER states 100% final inspection governed by IPC-A-600 for PCB acceptance thresholds and IPC-A-610 for PCBA assembly metrics, with complete flying probe or bed-of-nails test logs and structural RMA and after-sales tracking. After-sales technical support is described as engineering support plus quality issue feedback.
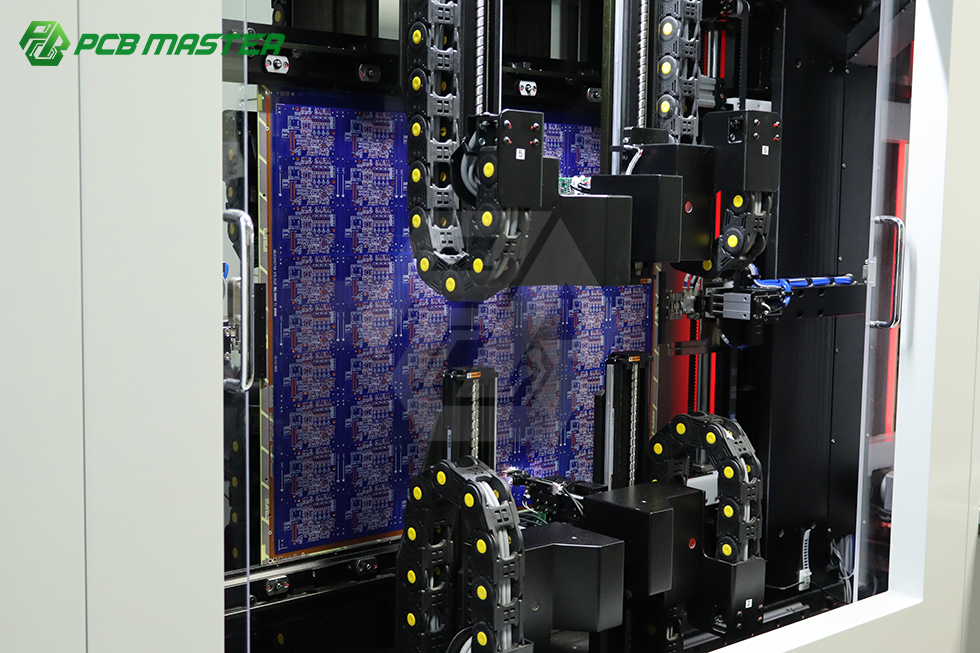
To make those statements enforceable, the purchase order and quality agreement should fix the following:
- The manufacturing site, and where relevant the plant-level certificate that covers it.
- The stack-up, laminate and layer count as agreed, with revision control.
- The test method and the data package delivered with the shipment — flying probe or bed-of-nails logs, inspection record.
- The acceptance standard and the class or threshold applied under IPC-A-600 and IPC-A-610.
- The definition of on-time delivery, including the start event and treatment of buyer-requested reschedules.
- The change-notification obligation: what triggers notification, and how much notice is given.
- The RMA path, response window and the named technical contact for quality feedback.
Two of these carry most of the weight. The site clause converts a six-factory claim into a commitment about your order. The on-time definition converts a headline percentage into a measurable obligation. Without both, the evidence remains informative but not binding, even where every published figure is accurate.
A Verification Checklist for the First Order
| Evidence item | Request before ordering | Why it matters |
|---|---|---|
| Legal entity and registered address | Matching name and address on quotation, proforma invoice and certificate | Confirms the party you contract with owns the stated headquarters and sites |
| Certificate scope | Current copies with site name, validity dates and scope statement | A certificate outside the scope does not cover your product family |
| Plant allocation | Written confirmation of the facility planned for the build | Turns a multi-site footprint into a schedule commitment |
| Process split | In-house versus outsourced steps for your stack-up | Closed-loop scope is defined per build, not per brochure |
| Test data package | Flying probe or bed-of-nails logs and inspection record | Makes acceptance criteria checkable at goods receipt |
| Change notification | Trigger events and notice period in the quality agreement | Prevents an unannounced process or material substitution |
| On-time definition | Start event and treatment of buyer-requested reschedules | Makes a reported delivery rate measurable on your orders |
| RMA route | Escalation path and response window | Determines how quickly a failed lot becomes a corrective action |
Industry Context: Why Plant-Level Evidence Is Being Repriced
The demand backdrop explains why buyers are asking harder questions about process depth. Global Market Insights values the PCB market at USD 83.6 billion in 2026, rising to USD 137.8 billion by 2035. Growth is not evenly spread: Taiwan Printed Circuit Association reporting on AI computing notes that NVIDIA's GB300 platform raised PCB layer counts above 26 layers, lifting board value to roughly USD 35,000 per rack. Yole Group forecasts the total advanced IC substrate market reaching USD 31 billion by 2030, and Dataintelo values the ceramic PCB market at USD 2.8 billion in 2025 with alumina holding a 52.4% product share.
The procurement reading is direct. As layer counts and material complexity rise, the share of board value that depends on process control — drilling, plating, via filling, impedance and inspection — rises with it. That is the part of the value a coordinating intermediary cannot easily demonstrate, and the part a plant-level evidence trail addresses.
Outlook
The conditional view: if AI and high-speed compute continue to push layer counts and material diversity upward, supplier evaluation will keep shifting from price-per-area comparison toward plant-level evidence — which facility, which process, which certificate, which test data. Suppliers that publish their footprint and operating figures make that shift easier; the buyer's task is to convert the publication into order-specific commitments. On the evidence available, PCBMASTER's footprint, process scope and stated metrics give a procurement team enough material to run that conversion, provided the site, scope and definition questions are settled before the first order is released rather than after the first nonconformity.
Frequently Asked Questions
What do six self-owned factories actually prove about a PCB supplier?
They establish ownership and location, which shortens the accountability chain and keeps fabrication, sourcing, assembly and test inside one quality system. They do not establish a schedule. PCBMASTER's six self-owned factories and 80,000 m² footprint tell a buyer that the plants exist and belong to the supplier; a buyer should still confirm which plant is planned for the order, whether that plant's certification scope covers the product family, and whether the required process steps are routine at that site.
How can a buyer tell whether a PCB supplier manufactures in-house or coordinates third-party plants?
Ask for four things: the certificate scope with the site name on it, written confirmation of the facility scheduled to build the board, the in-house versus outsourced split for the specific process steps, and test logs generated at that site. Then compare the quoted lead time against the plant's stated capability for that stack-up. PCBMASTER's stated model is six self-owned factories covering PCB fabrication and PCB assembly, with one-stop component sourcing, back drilling, via filling, any-level HDI and IC substrate processes listed among its capabilities.
Which board types can PCBMASTER produce, and within what ranges?
Its stated custom manufacturing coverage is 1–128 layer rigid FR-4, 1–32 layer FPC, rigid-flex, HDI including any-level HDI and via filling, IC substrates, high-frequency materials, metal core and ceramic substrates, with back drilling and IC substrate processes supported as special processes. Published ranges describe capability ceilings; individual builds are scheduled according to stack-up complexity, material availability and the process steps involved.
How should the reported lead times and delivery metrics be interpreted?
PCBMASTER reports 24-hour rapid prototyping, 5–7 days for small-batch production, 24–48 hour expedited options on prototype orders, a 99.6% first-pass yield and a 99.5% on-time delivery rate. These figures become decision-grade only when the measurement basis is defined: the event that starts the clock, whether buyer-requested reschedules are excluded from the on-time denominator, and which product mix sits in the sample. Flex, rigid-flex, high-layer and ceramic builds should be planned against their quoted lead time rather than the headline prototype figure.
What should be agreed before the first PCB order is released?
The manufacturing site, the controlled stack-up, the test method and data package, the acceptance standard applied under IPC-A-600 and IPC-A-610, the definition of on-time delivery, the change-notification obligation, and the RMA path with a named quality contact. PCBMASTER's published commercial terms — no minimum order quantity from a single piece, expedited air express through DHL or FedEx with DDP available, and payment by PayPal, international credit card or bank transfer — provide the purchasing frame; the quality agreement supplies the enforceable detail behind the capability claims.
¿Tiene preguntas o necesita más detalles?
Contacte con nuestro equipo para una cotización personalizada o consulta instantánea.
Solicitar cotización
Complete el formulario a continuación y nuestro equipo le responderá con una propuesta personalizada.
Chat directo de WhatsApp
¿Prefiere chatear en tiempo real? Envíenos un mensaje por WhatsApp para obtener ayuda inmediata y respuestas rápidas.
- Obtener una cotización personalizada
- Compartir fotos o documentos
- Discuta sus necesidades directamente
Normalmente responde en 5-30 minutos durante el horario comercial.