
Matching Plastic Extrusion Lines to Real Production Scenarios
Matching Plastic Extrusion Lines to Real Production Scenarios
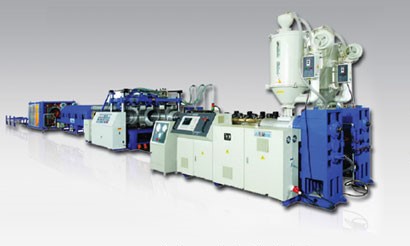
Extrusion lines are usually shortlisted by model number and output figure, but they are actually specified by production scenario. A line running 1,600 mm HDPE pressure pipe for a municipal water main and a line running PVC ceiling panels share a screw-and-barrel concept and very little else: different polymers, different downstream equipment, different tolerance logic, and different reasons for a production stop. When the shortlist is built on kilograms per hour alone, the mismatch usually surfaces at commissioning rather than at the quotation stage.
The mapping below links seven production scenarios — four pipe families, one conduit family, one panel family and one recycling loop — to the line configurations published for them, including model ranges, extruder sizes, installed power and auxiliary scope. It is a decision order rather than a catalogue: define the service condition of the finished product, convert it into a pipe or panel specification, then read the line range, drive size and equipment chain against it.
Why the decision order matters more than the model number
Scenario fit is decided by what the finished product has to survive. Pressure class, burial depth, service temperature, ring stiffness, panel thickness and surface requirement each translate into a specific mechanical demand on the line. Once that translation is explicit, the model range becomes a filter rather than a starting point.
| Production scenario | Governing requirement of the product | What it imposes on the line |
|---|---|---|
| Buried water and gas mains (HDPE solid wall) | Pressure resistance, corrosion resistance, uniform wall thickness | Vacuum calibration and cooling matched to diameter; haul-off sized to wall thickness; sufficient cooling length |
| Indoor hot and cold water (PPR) | Temperature resistance, corrosion resistance, long service life | Stable plasticizing at small diameters; high-precision die; tight dimensional control for jointing |
| Pressurised water and chemical lines (steel wire reinforced) | Pressure resistance, high tensile strength, corrosion resistance | Steel wire winding integrated ahead of the outer extrusion; calibration for a composite wall build |
| Buried high-voltage power conduit (MPP / PE) | Pressure resistance, impact resistance, non-conductivity | Chipless cutting; multi-claw traction; AC frequency control across the whole line |
| Drainage and cable ducts (PVC solid wall and corrugated) | Impact resistance, ring stiffness, dimensional stability | Solid wall: calibration plus belling. Corrugated: a forming machine chain, not a die swap |
| Interior panels (wall, ceiling, door, cabinet, floor) | Thickness uniformity, surface finish, dimensional precision | Calender rollers, calibration tables and stacking equipment; die and downstream as decisive as the extruder |
Scenario one — buried water and gas mains: HDPE from PE110 to PE1600
Five HDPE water pipe line models cover a Φ20 to Φ1600 mm envelope, and the published application scope for the family is municipal water supply, gas pipeline and farm irrigation pipe manufacturing. The family is wide enough that a buyer can be correct about output and still be wrong about diameter.
| Line model | Pipe diameter range | Extruder | Main motor | Extrusion capacity |
|---|---|---|---|---|
| PE110 | Φ20–110 mm | GS60/38 (optional GS75/33) | 90 kW | 150–400 kg/h |
| PE315 | Φ110–315 mm | GS75/38 (optional GS90/33) | 160 kW | 200–600 kg/h |
| PE630 | Φ315–630 mm | GS90/38 (optional GS120/33) | 280 kW | 600–1000 kg/h |
| PE1000 | Φ630–1000 mm | GS120/38 | 355 kW | 600–1000 kg/h |
| PE1600 | Φ1000–1600 mm | GS150/38 | 500 kW | 600–1500 kg/h |
The most useful observation in this table is not the top capacity figure. PE630 and PE1000 are both listed at 600–1000 kg/h, yet they serve completely different diameter bands. A buyer who shortlists by capacity will treat them as interchangeable; a buyer who shortlists by the maximum pipe diameter the project must deliver will separate them immediately. Capacity is a consequence of the diameter envelope here, not an independent variable.
The second observation concerns scale. PE1600 runs a 500 kW main motor and a GS150/38 extruder, and at the small end of its Φ1000–1600 mm range it is operating below its design envelope. A producer serving farm irrigation or distribution networks, where Φ20–315 mm dominates, typically sits in PE110 and PE315 territory with 90–160 kW main motors and 150–600 kg/h capacity. Over-buying diameter is a common and expensive form of over-specification.
Downstream scope for this family is consistent: moulds, vacuum calibration tanks, cooling tanks and haul-off machines. The screw and barrel are specified as 38CrMoAlA nitrided alloy steel, the mould as forged alloy die steel, and the machine frame as Q235 carbon steel.
Scenario two — indoor hot and cold water: PPR20-75 and PPR20-110
PPR lines sit at the opposite end of the diameter spectrum and are specified for a different reason. The published application is indoor cold and hot water plumbing and residential plumbing pipe production, where the requirements are corrosion resistance, high temperature resistance and long service life — with dimensional consistency that matters because PPR joints are made by fusion welding, not by mechanical fittings.
| Line model | Extruder | Main motor | Auxiliary extruder | Extrusion capacity |
|---|---|---|---|---|
| PPR20-75 | GS65/33 | 37 kW | GS50/33 | 80–160 kg/h |
| PPR20-110 | GS90/30 | 75 kW | GS55/33 | 80–250 kg/h |
The two models overlap at the bottom of the range at 80 kg/h. What separates them is the top of the range and the diameter coverage — Φ20–75 mm against Φ20–110 mm. A plant that will only ever produce small-diameter plumbing pipe does not need the larger machine, while a plant that must cover Φ110 domestic risers does. The mould is specified as high-precision die steel, which is consistent with the tight wall tolerance that fusion jointing demands.
Scenario three — pressurised water and chemical pipelines: steel wire mesh reinforced composite
Steel wire mesh reinforced composite pipe occupies a distinct scenario rather than a premium tier of solid wall PE. It is specified for urban pressurised water supply, chemical industry anti-corrosion pipelines and underground engineering pipe, where the requirement set is pressure resistance, high tensile strength and corrosion resistance together. The equipment list explains why the architecture differs: steel wire winding machines are part of the line, building the reinforcement into the pipe wall ahead of the outer extrusion.
| Line model | Pipe range | Maximum speed | Installed capacity | Actual power consumption |
|---|---|---|---|---|
| GS/PE-160-H | Φ50–160 mm | 2.4 m/min | 480 kW | 312 kW |
| GS/PE-250-H | Φ75–250 mm | 2.4 m/min | 550 kW | 358 kW |
| GS/PE-315-H | Φ90–315 mm | 2.4 m/min | 580 kW | 377 kW |
| GS/PE-500-H | Φ250–500 mm | 1.4 m/min | 630 kW | 410 kW |
| GS/PE-630-H | Φ315–630 mm | 1.2 m/min | 800 kW | 559 kW |
Two figures in this table are routinely misread. First, installed capacity and actual power consumption are different budgets: the electrical infrastructure has to be sized on the installed figure, while the operating cost estimate belongs to the consumption figure. At GS/PE-630-H the gap is 800 kW installed against 559 kW actual — roughly 70 percent of the installed load in continuous operation. Second, maximum line speed falls as pipe size rises, from 2.4 m/min across the 160 to 315 models down to 1.4 and 1.2 m/min at 500 and 630. Comparing metres per minute across this family without holding diameter constant produces a misleading throughput picture.
Scenario four — buried power grid: MPP and PE high-voltage power pipe
Underground cable protection is a specification-driven scenario with its own requirement set: high pressure resistance, impact resistance and non-conductivity for buried high-voltage power grid construction. The material is MPP or PE, with PP, ABS, PEX and silicon core pipe listed as options on the same platform.
| Line model | Pipe specification | Line speed | Installed power |
|---|---|---|---|
| PEG63 | Φ20–63 mm | 0.3–4.5 m/min | 70 kW |
| PG160 | Φ75–160 mm | 0.3–2 m/min | 125 kW |
Line scope here is defined by control and cutting: AC frequency control across the whole line, optional 2-, 3- or 4-claw traction, and a chipless cutting system. The chipless requirement follows from the application — a conduit that protects high-voltage cable should not carry a cut face that introduces debris or a stress point.
The boundary is straightforward and often overlooked: two models, two bands. Nothing in this range covers both Φ20–63 mm and Φ75–160 mm, and a supplier who must deliver both conduit sizes is planning two lines or a staged production plan. The speed range also inverts the intuition carried over from pipe lines: up to 4.5 m/min at small diameter, capped at 2 m/min at the larger one.
Scenario five — drainage and cable ducts: solid wall PVC versus corrugated
This scenario is included because it is where buyers most often assume a conversion that does not exist. Solid wall PVC water supply and drainage pipe and single-wall corrugated conduit look like neighbouring products, but they are produced on separate line architectures.
PVC solid wall water supply and drainage
The published range is three models — PVC63, PVC250 and PVC630 — covering water supply, drainage and sewage pipe for building and municipal plumbing. The requirement set is high impact resistance, corrosion resistance and good dimensional stability, and the matched equipment list includes moulds, calibration tanks, cooling systems and belling machines. The belling machine is the detail that separates this family from a plain pipe line: socket forming is a downstream operation with its own cycle time.
Single-wall corrugated conduit
The corrugated range is published as KSPG-63, KSPG-32, KSPG-20, KS-160 and KS-75, described as high-speed continuous lines producing single-wall corrugated pipe for drainage, sewage and cable protection. Requirements are high ring stiffness and flexible forming; matched equipment includes forming machines, cooling tanks, haul-off machines and cutting units. The corrugated profile is created by the forming machine chain.
Scenario six — interior panels: wall, ceiling, door, cabinet, floor and formwork
Panel production is the scenario family where the extruder is the least differentiated element of the decision. Wall panel lines are offered across four barrel sizes because panel width and thickness drive the choice, while decoration profile lines sit on three small models because those profiles are small.
| Finished product | Line model and drive | Published output |
|---|---|---|
| PVC hollow wall panel and ceiling | SJSZ51, SJSZ55, SJSZ65, SJSZ80 | Not stated in the model range |
| WPC door panel | SJSZ80 (75 kW), SJSZ92 (110 kW) | 250–400 kg/h / 400–600 kg/h |
| PVC and WPC foam board | SJSZ80/156 (75 kW); 80+165 co-extrusion (75+37 kW) | Not stated in the model range |
| PVC imitation marble sheet | SJSZ80/156 (75 kW), SJSZ92/188 (110 kW) | Not stated in the model range |
| PVC grille and decoration profile | SJSZ51 (18.5 kW), SJSZ55 (22 kW), SJSZ65 (37 kW) | Not stated in the model range |
| SPC flooring | SJSZ92/188 (110 kW), SJSZ110/220 (200 kW), SJP115/30 (90 kW), SJP135/30 (132 kW) | Not stated in the model range |
| PP hollow construction formwork | SJ-130×33 (160 kW), SJ-90×33 (75 kW) | Not stated in the model range |
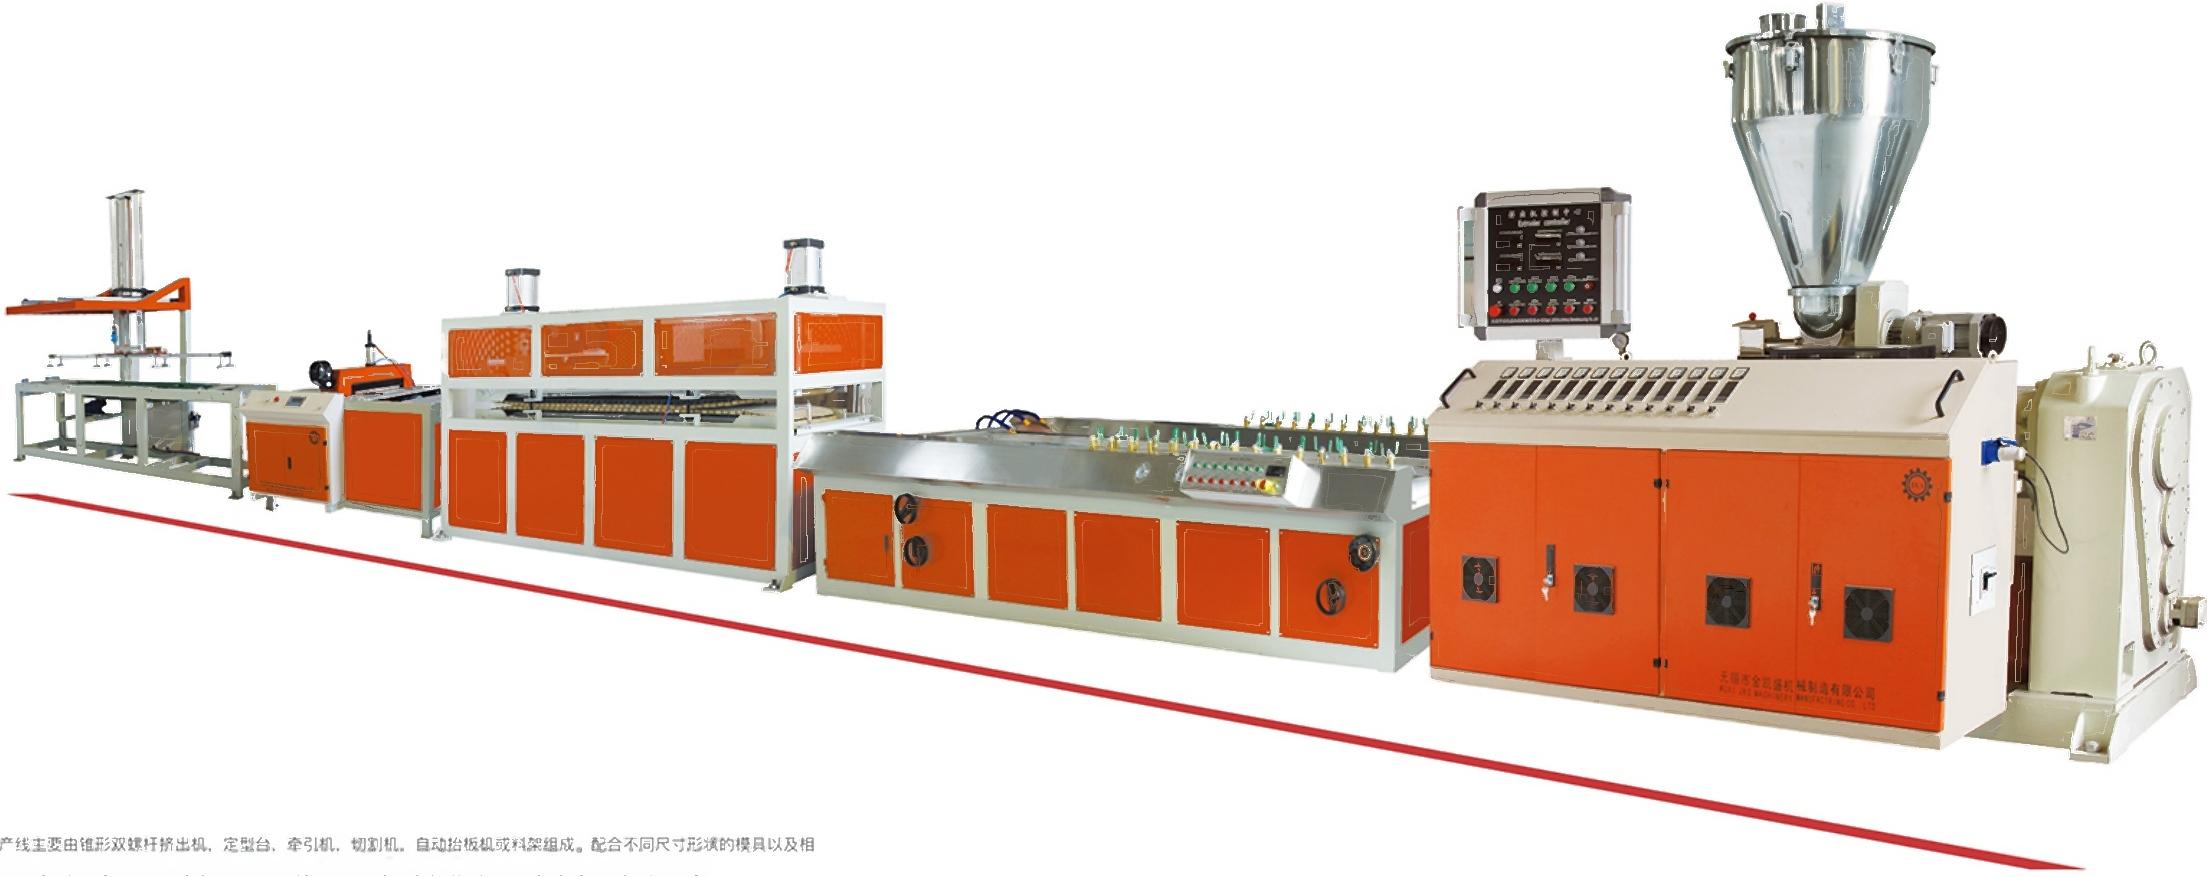
Each product carries its own requirement set. Hollow wall and ceiling panels are specified for light weight, high strength and uniform thickness. WPC door panels require uniform thickness, high strength and water resistance, with the compound described as PVC plus CaCO₃ and the mould as hardened steel with chrome plating. Foam board requires uniform foaming, low density, high strength and a smooth surface. Imitation marble sheet requires a realistic pattern with scratch and UV resistance, which is why co-extruders, calender rollers and printing equipment appear in its equipment list. SPC flooring requires high dimensional stability, water resistance, wear resistance and high hardness, supported by calender rollers, cooling systems and UV coating.
The boundary that matters most is that a declared output figure belongs to a product specification. A WPC door panel line listed at 400–600 kg/h on SJSZ92 is running a particular panel thickness and density; a thicker or denser panel reduces the effective rate. The same logic applies to SPC. A published 1,500 kg/h capacity for a high-productivity SPC floor conical twin-screw extruder describes that specific configuration, not the entire SPC line family — the figure cannot be transferred to a different barrel size without a new calculation.
The material constant behind every scenario: 38CrMoAlA nitrided screw and barrel
Across the pipe, composite, conduit, panel and pelletizing lines described here, the same wear-part specification recurs: 38CrMoAlA nitrided alloy steel for the screw and barrel, with Q235 carbon steel for the machine frame. The extruder families carry it — the SJSZ conical twin-screw range from SJSZ-45 at 15 kW and 70 kg/h through SJSZ-65 at 37 kW and 250 kg/h to SJSZ-110 at 200 kW and 1,000 kg/h, and the SJ single-screw range with custom models including SJ30, SJ45, SJ65 and SJ90.
The purpose is consistent with the duty. Filled PVC formulations, mineral-filled SPC compounds and continuous operation all put abrasive load on the plasticizing unit, and nitriding addresses the surface of that wear path rather than the bulk of the steel. Die material diverges by scenario because the forming duty diverges: forged alloy die steel for HDPE, refined wear-resistant die steel for composite pipe, high-precision die steel for PPR, and hardened chrome-plated steel for WPC door panels.
The honest limit of this specification is that it describes composition, not service life. How long a screw and barrel last depends on compound abrasiveness, temperature profile, screw speed and maintenance practice. A buyer should treat the material designation as a qualifying criterion and still ask for the wear-part inspection and replacement logic that goes with it.
Scenario seven — closing the material loop: crushing, pulverizing, pelletizing and mixing
Recycling is a production scenario in its own right, not an accessory to the others. A pipe plant or panel plant generates start-up scrap, trim and rejects continuously, and the route that scrap takes determines whether it returns to the same formulation, leaves as a saleable pellet, or becomes waste.
| Equipment | Models | Capacity and notes |
|---|---|---|
| Plastic crusher | SP400 / SP660 | 15 kW, 300–400 kg/h / 22 kW, 600–700 kg/h; wear-resistant cutting chamber and blades |
| Plastic pulverizer | MF400 / MF500 / MF600 | 30 kW, 200 kg/h / 37 kW, 300–400 kg/h / 55 kW, 400–500 kg/h; fineness 40–80 mesh |
| Strand cutting pelletizing line | ST80 / ST100 / ST120 / ST150 | 55 kW, 70–160 kg/h / 75 kW, 170–280 kg/h / 90 kW, 250–400 kg/h / 110 kW, 350–650 kg/h; L/D 35:1 |
| PVC hot cut pelletizing | Die-face cutting configuration | Pellet uniformity for both soft and hard PVC; cooling fans, cyclone separators and storage bins |
| PVC mixing and cooling unit | SRL-Z200/500 to SRL-Z1000/3000 | 37/7.5 kW at 300–400 kg/h up to 160/22 kW at 1,600–2,000 kg/h; mixing 8–10 min/pot, cooling 6–8 min/pot |
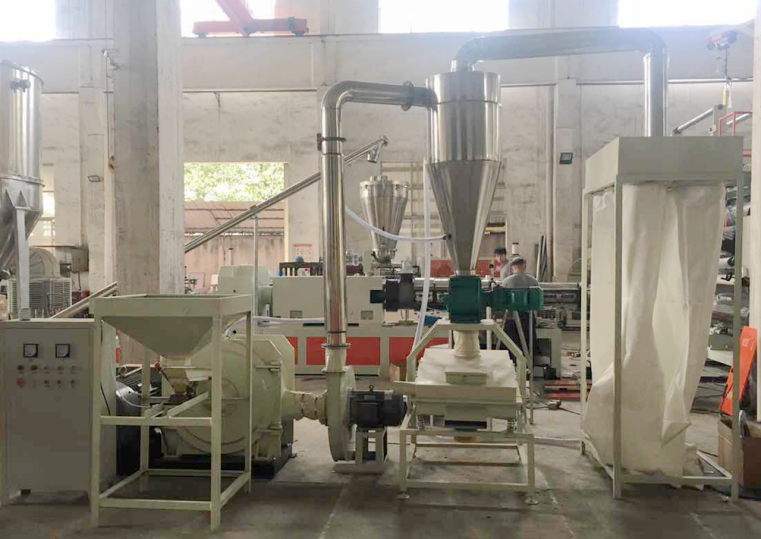
The decision rule is material-based. Pulverizing returns PVC, PE and PP scrap to 40–80 mesh powder, which is the route back into a PVC compounding loop through the mixing and cooling unit. Strand pelletizing is listed for PE, PP, ABS, PS, HIPS and PC, and suits either virgin compounding or waste plastic recycling in its two-stage form. PVC hot cut pelletizing cuts at the die face and is specified for both soft and hard PVC. Crushers sit upstream of either route, reducing pipe, profile and sheet scrap to a size the next stage can accept.
The boundary is that pulverizer output is quoted against a fineness target. Coarser or finer powder changes throughput, and a buyer specifying 200 kg/h on MF400 is specifying it at 40–80 mesh, not at any mesh.
Market context behind these scenario choices
The equipment side and the demand side are moving together. The global plastic extrusion machine market was estimated at USD 7.9 billion in 2025 and is projected to reach USD 12.87 billion by 2035, according to Market Research Future. Trade data points to where much of that capacity is built: in 2024 China was the leading exporter of rubber and plastic working machinery under HS 8477 at USD 8.55 billion, ahead of Germany at USD 6.11 billion and Italy at USD 2.61 billion, based on Observatory of Economic Complexity figures drawn from UN Comtrade data.
On the panel side, Grand View Research puts the global stone plastic composite flooring market at USD 6.4 billion in 2026, projected to reach USD 10.3 billion by 2033. That forecast is the demand signal behind the density of SPC line configurations in scenario six — and it explains why panel buyers increasingly compare calender and coating scope rather than extruder power alone.
Compliance is the third variable. ANSI/PLASTICS B151.7-2014 (R2021) applies to extrusion machines used in the plastics industry and requires the risk assessment process to be used in the manufacture, care and use of the machinery. A separate PLASTICS Industry Association listing references the 2013 edition, so the edition that applies in a given market should be confirmed rather than assumed. Safety scope is a specification item, not paperwork.
A buyer's checklist for scenario-fit verification
| Check | What to confirm |
|---|---|
| 1. Product specification | Maximum and minimum diameter or panel size, pressure class, service temperature, ring stiffness, thickness range |
| 2. Line envelope | That the model range covers both ends of the product range, not only the headline maximum |
| 3. Drive and capacity | Extruder model, main motor power and capacity read together, with capacity tied to the product specification it was quoted against |
| 4. Auxiliary scope | Whether the chain includes the scenario-specific units — wire winding, belling, forming machines, calender rollers, stacking |
| 5. Energy and evidence | Installed versus actual power consumption; declared figures, test records and inspection options |
Where this mapping stops
A scenario map narrows a shortlist; it does not qualify a supplier. Several limits deserve to be stated plainly.
- Model ranges are envelopes. A line rated to Φ1600 mm is not equally efficient across Φ1000 to Φ1600 mm, and a line rated to Φ20 mm at the bottom of its range is not running at design condition there either.
- Installed power is not operating power. The composite line figures show a consistent gap — 800 kW installed against 559 kW actual at GS/PE-630-H. Utility planning and cost modelling need different numbers.
- Speed falls as size rises. Maximum line speed across the composite family drops from 2.4 m/min to 1.2 m/min, and across the conduit family from 4.5 m/min to 2 m/min.
- Capacity is product-specific. A kilograms-per-hour figure quoted for one panel thickness or one pipe wall thickness cannot be carried to another specification without recalculating.
- Declared figures are supplier figures. The capacity, speed and power values in this article come from published line specifications. They are comparable only where the product basis is the same, and they do not replace factory acceptance testing or reference visits.
- Standards require edition confirmation. The discrepancy between the 2014 (R2021) and 2013 references for B151.7 should be resolved for the destination market before compliance is treated as settled.
Where JKS sits inside this map
Wuxi JKS Machinery Manufacturing Co., Ltd. is a Chinese manufacturer of custom plastic extrusion machinery and complete turnkey production lines, based at No. 81 Xixian Road, Fangqian Town, Wuxi, Jiangsu Province. Its portfolio spans the scenarios above: pipe lines, sheet and SPC flooring lines, PVC and WPC profile lines, solid plastic rod lines and waste plastic pelletizing lines, alongside standalone single-screw and conical twin-screw extruders and auxiliary equipment including mixers, crushers and pulverizers.
The operating facts relevant to a scenario-based evaluation are these: a 2,000 m² factory, 20 employees and a six-engineer R&D team; annual output of 200 units against a monthly capacity of 30 units; a 50 percent export ratio with machines shipped to more than 35 countries across Southeast Asia, Russia, the Middle East, Europe, Central Asia, Africa and South America. Customisation covers extruder model, screw configuration, line layout, voltage and frequency, control system and capacity adjustment, with a MOQ of one unit and a lead time of 40 work days. Quality control is 100 percent factory pre-assembly and testing before shipment, with third-party inspection available on request. After-sales covers overseas installation guidance, on-site commissioning, operator training, remote technical support and a 12-month warranty.
For buyers working through the panel scenarios, the company's WPC door project brochure is available for download: JKS WPC door project brochure (PDF).
Future outlook
Three shifts are likely to change how these scenarios are specified. The first is energy literacy: as electricity becomes a larger share of operating cost, the installed-versus-actual gap quoted on composite lines will migrate from a footnote to a shortlisting criterion, and buyers will ask for consumption figures at defined products rather than installed capacity alone.
The second is panel complexity. With the SPC flooring market forecast to grow from USD 6.4 billion in 2026 to USD 10.3 billion by 2033, competition is likely to move toward surface and thickness consistency rather than raw output, which puts calender, embossing and coating scope closer to the centre of the line decision.
The third is in-plant reclaim. Where buyers face recycled-content requirements or volatile compound costs, the recycling scenario stops being optional equipment and becomes part of the line layout — crusher and pulverizer capacity planned alongside extruder capacity, with the mixer cycle time as the connecting constraint. None of these shifts changes the underlying rule: the service condition of the finished product still decides the line.
FAQ
Choose by diameter range, not by capacity. PE630 covers Φ315–630 mm with a GS90/38 extruder and a 280 kW main motor. PE1000 covers Φ630–1000 mm with a GS120/38 extruder and a 355 kW main motor. Both carry the same 600–1000 kg/h capacity band, so the specification that separates them is the maximum pipe diameter the project must produce.
PPR20-75 uses a GS65/33 extruder with a 37 kW main motor, a GS50/33 auxiliary and 80–160 kg/h capacity. PPR20-110 uses a GS90/30 with a 75 kW main motor, a GS55/33 auxiliary and 80–250 kg/h. Both are intended for indoor cold and hot water plumbing and residential plumbing pipe production, where the stated requirements are corrosion resistance, high temperature resistance and long service life, supported by high-precision die steel for dimensional consistency.
When the pipe must meet pressure resistance, high tensile strength and corrosion resistance at the same time, in urban pressurised water supply, chemical anti-corrosion pipelines or underground engineering pipe. The line differs from a solid wall PE line because steel wire winding machines are part of the equipment scope. Available models run from GS/PE-160-H at Φ50–160 mm and 2.4 m/min to GS/PE-630-H at Φ315–630 mm and 1.2 m/min.
No. Corrugated pipe is created by a forming machine chain, and the corrugated range — KSPG-63, KSPG-32, KSPG-20, KS-160 and KS-75 — is described as high-speed continuous lines for single-wall corrugated drainage, sewage and cable protection pipe, with forming machines, cooling tanks, haul-off machines and cutting units. Solid wall PVC water supply and drainage models (PVC63, PVC250, PVC630) are matched with calibration tanks, cooling systems and belling machines. These are separate line architectures.
Different lines, driven by panel type. PVC hollow wall panel and ceiling: SJSZ51, SJSZ55, SJSZ65 or SJSZ80. WPC door panel: SJSZ80 at 75 kW and 250–400 kg/h, or SJSZ92 at 110 kW and 400–600 kg/h. PVC and WPC foam board: SJSZ80/156 at 75 kW, or 80+165 co-extrusion at 75+37 kW. PVC imitation marble sheet: SJSZ80/156 at 75 kW or SJSZ92/188 at 110 kW. Decoration profile and grille: SJSZ51 at 18.5 kW, SJSZ55 at 22 kW or SJSZ65 at 37 kW. SPC flooring: SJSZ92/188 at 110 kW, SJSZ110/220 at 200 kW, SJP115/30 at 90 kW or SJP135/30 at 132 kW. PP hollow construction formwork: SJ-130×33 at 160 kW or SJ-90×33 at 75 kW.
The material and the destination decide. Pulverizers MF400, MF500 and MF600 return PVC, PE and PP scrap to 40–80 mesh powder at 200, 300–400 and 400–500 kg/h respectively, which suits a PVC compounding loop through a mixing and cooling unit. Strand pelletizing lines ST80 to ST150 cover 70–650 kg/h at L/D 35:1 and are listed for PE, PP, ABS, PS, HIPS and PC. PVC hot cut pelletizing cuts at the die face and is specified for both soft and hard PVC. Crushers SP400 at 300–400 kg/h and SP660 at 600–700 kg/h sit upstream of either route.
¿Tiene preguntas o necesita más detalles?
Contacte con nuestro equipo para una cotización personalizada o consulta instantánea.
Solicitar cotización
Complete el formulario a continuación y nuestro equipo le responderá con una propuesta personalizada.
Chat directo de WhatsApp
¿Prefiere chatear en tiempo real? Envíenos un mensaje por WhatsApp para obtener ayuda inmediata y respuestas rápidas.
- Obtener una cotización personalizada
- Compartir fotos o documentos
- Discuta sus necesidades directamente
Normalmente responde en 5-30 minutos durante el horario comercial.