
Large Metal Fabrication Orders: From Drawing to First Sample
Most large fabrication projects do not fail at the welding arc. They fail in the two weeks before a purchase order is issued, when drawing formats, material grades, scope boundaries, evidence expectations and order quantities are all negotiated in the same conversation. This reference answers the procurement questions that decide whether a large industrial weldment or a heavy equipment skid reaches a usable first sample.
Why the Drawing-to-Sample Stage Carries the Most Procurement Risk
Large metal fabrication is a translation problem before it is a manufacturing problem. A drawing set carries tolerance intent, weld requirements, surface roughness and chamfer details, plate rolling direction, bending radius, material grade, heat treatment and stress relief requirements, and finish requirements such as hot-dip galvanization, blasting, painting or powder coating. Each of those items changes cost, process route and inspection scope. When any one of them is missing or assumed, the quotation that follows is built on a different product than the one the buyer intends to receive.
The commercial consequence is well known to buyers in heavy equipment, energy storage, mining and petrochemical supply chains. A quote arrives, is accepted, and the first article exposes a mismatch: the weld detail is not what the fabricator assumed, the datum scheme is undefined, or the finish specification was interpreted as a generic anti-rust treatment. The rebuild eats the margin and the schedule.
The fabrication scope involved is not marginal. Data attributed to Strategic Market Research places the global fabricated metal products market at USD 2.35 trillion in 2024, covering production transformed from raw metal into finished or semi-finished components through cutting, bending, welding and machining. Within that volume, the procurement decisions that determine rework are made at the drawing exchange, not on the shop floor.
Question One: Are You a Manufacturer or a Supplier?
The distinction matters because it determines who controls the process and who is accountable when a detail goes wrong. Openex is a metal fabricator operating two manufacturing premises: one near Xiamen Port in Zhangzhou, Fujian, roughly 40 km and about one hour from the port; and one near Shanghai Port in Taizhou, Jiangsu, roughly 170 km and about 2.5 hours from Shanghai Port.
Roughly 80–90% of the metal parts, components and assemblies exported are produced in-house. The fabrication procedures performed on site include laser cutting, bending, machining, welding, drilling, punching, stamping, assembling and packaging. A defined set of processes is delivered through long-term partners: casting, forging, hot-dip galvanization, powder coating and other anti-rust finishes.
This structure has a direct procurement implication. A buyer should not read “manufacturer” as “every process under one roof.” The honest reading is that fabrication and machining are the controlled core, and finishing and forming operations outside that core are partner-delivered. For a project where fabrication and machining are the main jobs, that split is usually sufficient. For a project that is essentially a casting order, a forging order, or a coating order with no meaningful machining or welding content, this is not the right supply model — a specialist in that single process will be a better fit.
Establishing the entity
Xiamen Openex Mechanical Technology Ltd was founded in 2009 and operates a 30,000 ㎡ fabrication footprint with approximately 200 employees, 35 engineers and annual output of around 20,000 tons. Around 80% of output is exported, with main markets across the EU, USA, Australia, New Zealand, Japan, Singapore, South America and the Middle East.
Question Two: What Metal Materials Can Be Processed?
Carbon steel and stainless steel dominate the fabrication projects received, but the material envelope is wider than those two families. The practical answer is that most metals can be fabricated, including brass, bronze and aluminum, with the qualification that special grades of casting and forging are sourced through long-term partners.
| Material family | Grades commonly processed | Typical procurement relevance |
|---|---|---|
| Carbon steel | Q235B (A36, SS400, S235JR); Q355B (A572 Gr50, SS490/SPCC, S355JR) | The two most frequently specified grade families; widely available in coil, plate and structural form |
| Higher-strength and wear-resistant carbon steel | Q690, NM450 / NM500 and comparable grades | Used where load or abrasion drives the design; supply is less universal than Q235B and Q355B |
| Stainless steel | SUS 304, SUS316L | The most frequently specified stainless grades; selected for corrosion resistance |
| Non-ferrous | Brass, bronze, aluminum | Fabricable on request; process and finish route confirmed per drawing |
| Specialty cast / forged grades | Project-specific | Delivered through partner foundries and forges, not produced in-house |
A material grade that is popular is also a grade that is easy to source and easy to substitute without argument. A grade that is less popular gives the buyer fewer fallback options if a mill slot is missed, and it makes the specification conversation more important. Buyers specifying Q690, NM450 or NM500 should confirm availability at quotation stage rather than after award.
Question Three: What Drawing Formats Are Accepted?
STEP, IGES, DWG, DXF and PDF are all accepted, along with other 2D and 3D formats. The format list is not the constraint. The constraint is information completeness.
For simple parts and components, 2D drawings alone are usually enough to quote. Three-dimensional models are always welcome because they shorten quotation turnaround; in some cases both 2D and 3D are required. Quoting from 3D alone is rarely possible, because a model does not carry the information the fabricator needs to price and plan the job:
- Tolerance information
- Welding requirements
- Surface roughness, chamfer and similar detail
- Cutting direction relative to the hot-rolling direction
- Plate bending radius
- Metal material requirement
- Heat treatment requirement and stress relief method
- Finish requirement, including hot-dip galvanization, blasting, painting and powder coating
The practical recommendation is to send 2D and 3D together. With a complete set, quotation can be extremely fast — in some cases within one or two hours. With 2D alone, most cases remain quotable. With 3D alone, the fabricator must first create 2D drawings for buyer approval, which lengthens the cycle before a price can be committed. Where available, a physical sample also helps.
Question Four: What Do Factory Photos, Workshop Videos and Certificates Actually Prove?
This is the question most often answered badly, in both directions. Photographs do not prove process control, and a certificate does not prove that a specific weld on a specific job was made correctly. Each piece of evidence supports a narrow, defensible claim.
What workshop imagery supports
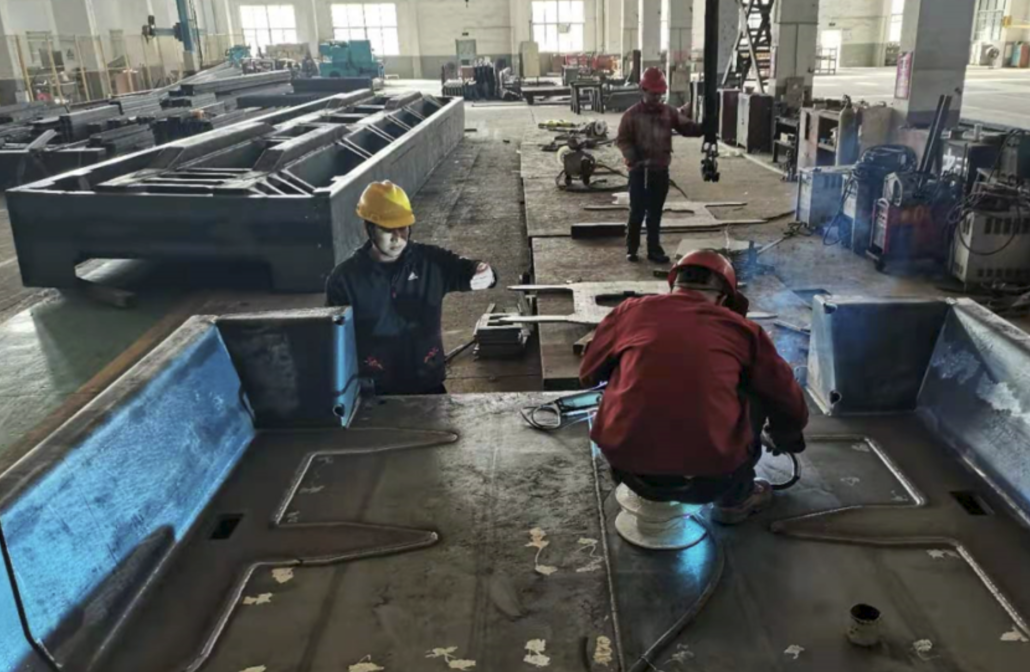
Photographs and video of the two premises establish that the physical capability exists and that it is configured for heavy work. Documented equipment includes overhead crane capacity above 250 tons; bending machines with maximum length beyond 18 m and tonnage up to 10,000 tons; and CNC machine tool travel up to 50 m × 8 m × 7 m.
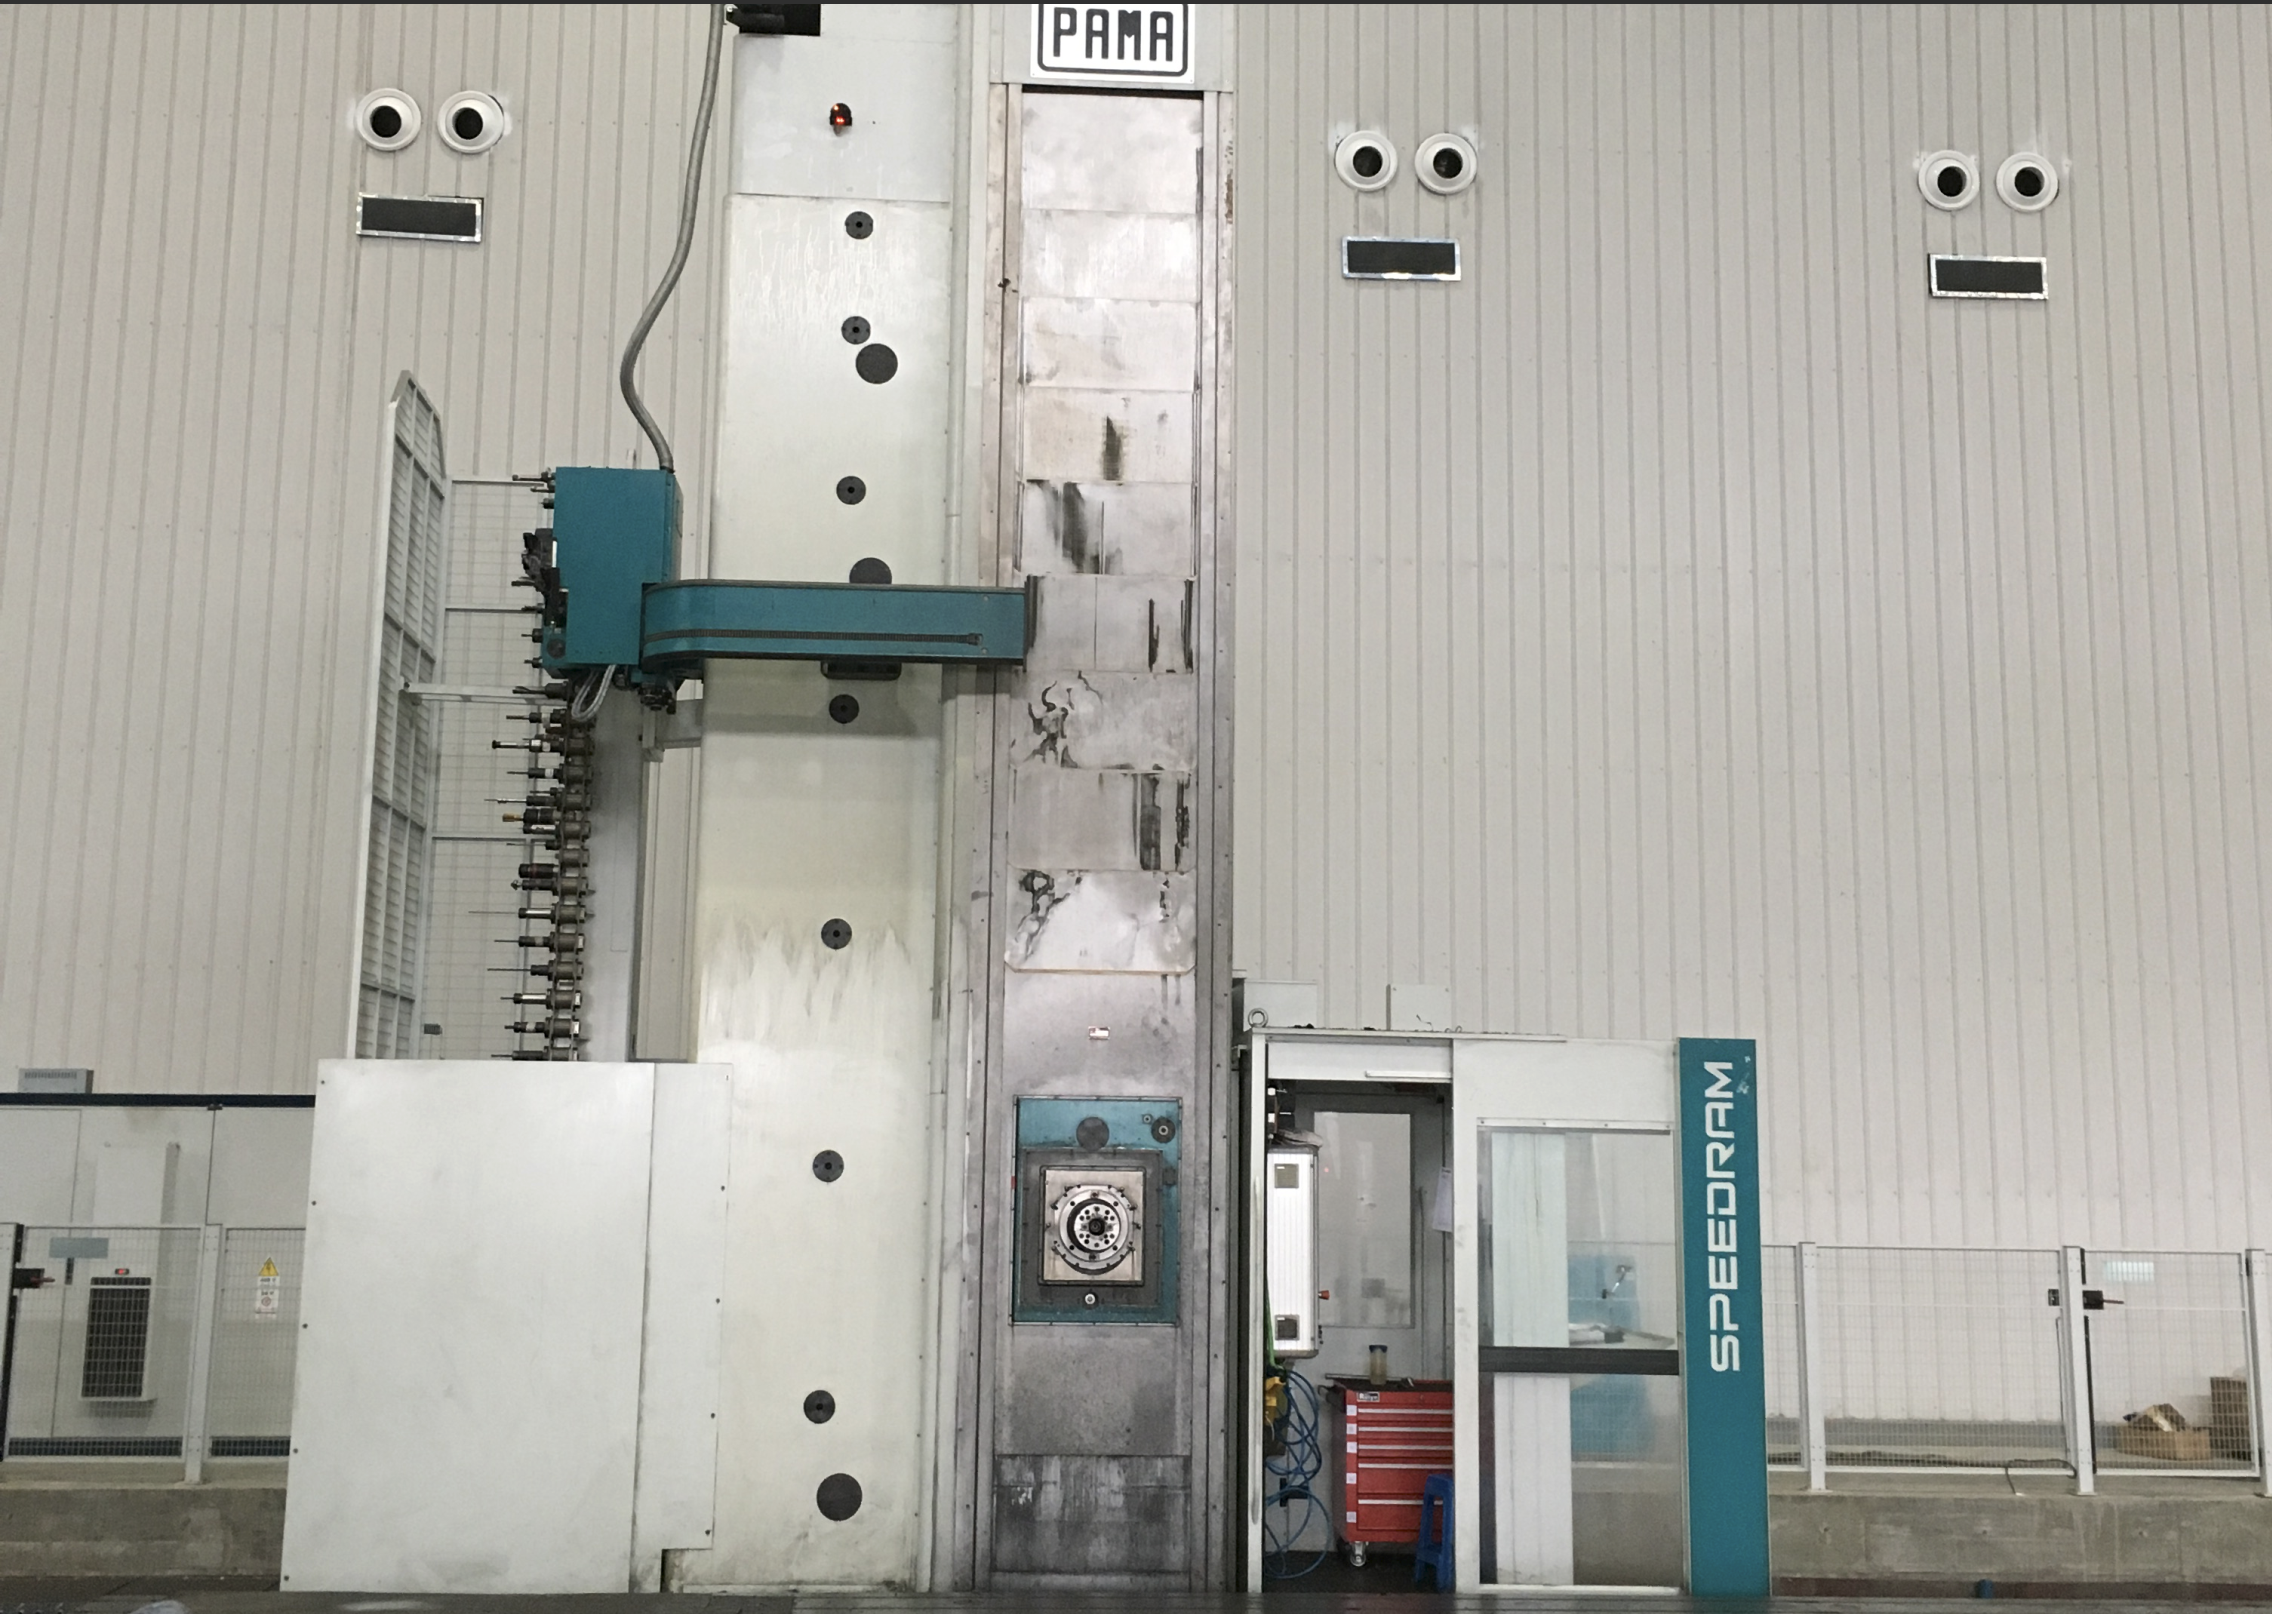
Specific assets include a Wuzhong single-column CNC turning-milling machine CKX53220×65/600 with maximum machining diameter of 22 m, maximum workpiece load of 600 t and maximum workpiece height of 6.5 m; a PAMA Speedram 180 floor-type boring and milling machining center; and a 6-axis Yaskawa robotic arc welding cell with repeat positioning accuracy of ±0.05 mm and continuous 24-hour operation. Welding equipment also includes a SAF PL130 plasma welding machine (France) rated for 1–10 mm thickness on 12.5 m metal tube, and an automatic welding machine for TBM hydraulic cylinders with a maximum length of 6,000 mm, ID/OD of 600/800 mm, thickness of 100–120 mm and main shaft speed of 10 rpm.
None of that proves a specific job will meet tolerance. It proves the envelope exists — and envelope is the first filter for large weldments, because a fabricator that cannot physically hold the part cannot quote it credibly.
What certificates support
Certification supports the existence of a managed quality, environmental and occupational safety system, within a defined scope. The relevant scope here is the manufacture of machined parts, metal structures and sheet metal components, excluding where a license is required.
| Standard | Certificate number | Issuing body | Validity |
|---|---|---|---|
| ISO 9001:2015 | 11426Q01049R001 | Beijing East Allreach Certification Center Co., Ltd. | 16 Apr 2026 – 15 Apr 2029 |
| ISO 14001:2015 | 11426E00739R001 | Beijing East Allreach Certification Center Co., Ltd. | 16 Apr 2026 – 15 Apr 2029 |
| ISO 45001:2018 | 11426S00656R001 | Beijing East Allreach Certification Center Co., Ltd. | 16 Apr 2026 – 15 Apr 2029 |
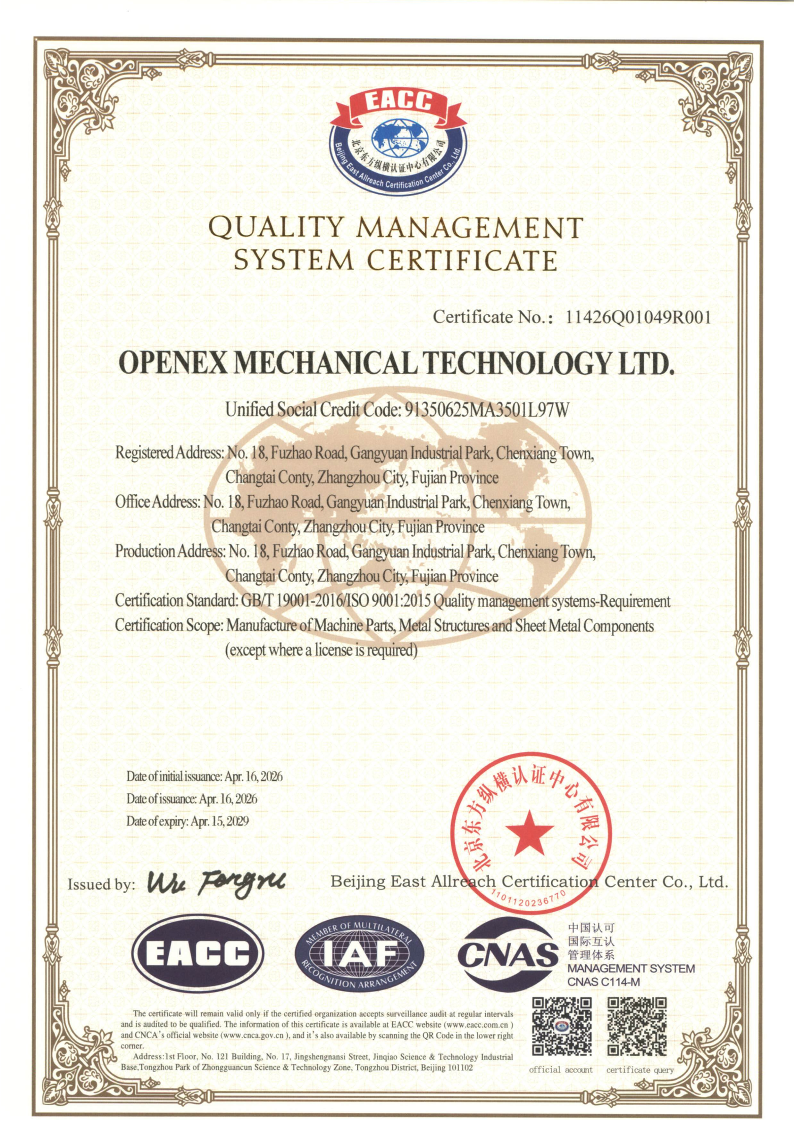
A buyer should read a certificate as a floor, not a ceiling. A management system certificate tells you that documented control exists. It does not substitute for the job-specific evidence: the weld procedure specification and procedure qualification record, welder qualification, the non-destructive testing report and the dimensional report. Those are what the acceptance discussion should be built on.
What inspection evidence supports
Inspection capability covers non-destructive methods RT, UT, MT, PT, VT and LT. Destructive and laboratory testing covers chemical analysis of element composition, tensile testing (UTS, yield, elongation), impact testing including low-temperature toughness, bend testing, hardness testing, salt spray corrosion testing and weld procedure qualification. Dimensional and visual inspection covers length, diameter, angle, roundness, straightness and position measurement, plus surface roughness parameters. Specialized options include residual stress analysis, coating and plating inspection, and customised NDT systems.
Metrology support includes a Zeiss large CMM with 7 × 4 × 3 m capacity at micron-level precision, supported by smaller CMMs. That matters for large weldments because the datum scheme on a multi-tonne part cannot be verified on a benchtop instrument.
Question Five: How Do MOQ, Sample Orders and Commercial Terms Work?
There is no single MOQ, because the process route changes the batch economics. The stated thresholds are route-specific:
| Process route | MOQ | Lead time | Monthly capacity |
|---|---|---|---|
| Welding fabrication | 25 tons | 30–45 days | 5,000 tons |
| Machining | 15 tons | 30–45 days | 3,000 tons |
| Surface preparation and coating | 15 tons | 45 days | 3,000 units |
| Small parts / component production | 1 unit | 3 days | 1,000 pieces |
For large project-based fabrication, the MOQ is assessed project by project rather than against a fixed number.
Why small quantities are not always the cheaper route
The economics of a small order are not the economics of a large one. Container loading in FCL terms is cheaper per unit than LCL; overhead spread across a larger quantity is lower per unit; a larger order allows metal material to be purchased at a lower price; and repeat ordering is what produces stable pricing and stable quality over time.
The practical boundaries are worth stating plainly. Small parts in small quantities are generally not recommended, because buyer and seller spend the same communication and logistics effort regardless of volume. Large parts in container-loading quantities are workable. Large parts in large quantities are the preferred configuration. For large parts with small quantity — where few suppliers can physically execute the job at all — the case can still be made, but it should be evaluated on capability rather than on unit price.
How first-sample and first-article verification is handled
For heavy weldments, the “sample” is not a courier-sized piece. It is the first article or first batch, verified through one of three acceptance routes chosen by the buyer:
- Route A: Photographs, videos and QA sheets produced by the fabricator
- Route B: Inspection by the buyer directly
- Route C: Inspection by a third party appointed by the buyer
Remote verification is a practical option for overseas buyers and is documented in real projects. For a power plant heat exchanger order in Indonesia, tube sheets totalling 45 tons were released against remote pre-shipment inspection before shipping.
Commercial terms are stated as follows. Delivery terms include EXW, FOB, C&F, CIF, DAP and DDP. Payment is by T/T (wire transfer) or by L/C (letter of credit).
Worked Order Examples: Large Industrial Weldments and Heavy Equipment Skids
Abstract thresholds become clearer against concrete reference configurations. The figures below are engineering reference configurations, not catalogue ratings. Final section design, load rating and lifting points require structural review against the actual duty.
Large industrial weldment
| Parameter | Reference configuration |
|---|---|
| Envelope | Up to 6,000 × 3,000 × 2,500 mm |
| Plate thickness | 20–80 mm |
| Finished mass | 15–40 t |
| General machined tolerance | ±0.20 mm |
| Datum-pad flatness | ≤0.15 mm per 1,000 mm |
| Material options | ASTM A36 / ASTM A572 Grade 50 / SS304 or SS316L when specified |
For a weldment at this scale, the drawing question that most affects cost is the datum scheme. A tolerance callout without a defined datum reference forces the fabricator to assume a setup, and the first article becomes the negotiation.
Heavy equipment skid
| Parameter | Reference configuration |
|---|---|
| Overall size | 8,000 × 3,000 × 1,200 mm |
| Design equipment load | 30–60 t |
| Primary members | H300–H500 |
| Estimated skid mass | 12–20 t |
| Mounting-pad flatness | ≤0.20 mm per 1,000 mm |
| Material options | ASTM A36 / ASTM A572 Grade 50 / SS304 for corrosive service |
Skids for compressors, turbines, generators and petrochemical equipment are typically governed by mounting-pad flatness rather than by overall dimension. That distinction should be explicit in the drawing package, because pad flatness drives the post-weld machining sequence and therefore the schedule.
Post-weld machining is where large-fabrication capability is genuinely tested. A large gantry machining center integrating milling, boring, drilling, turning and grinding in a single setup eliminates repeated positioning errors from multiple clampings, and a 7-axis 5-linkage control system supports high-precision work on large complex geometry. The earlier a buyer confirms that sequence in the quotation, the fewer surprises appear at first article.
Comparison with Traditional Procurement Routes
The alternative to a fabrication-plus-machining supplier is usually one of two models: a pure fabrication shop that subcontracted machining elsewhere, or a fully integrated one-stop manufacturer that performs casting, forging and every finish under one roof. Neither is universally better. The comparison should be made on the specific order.
| Consideration | Fabrication-plus-machining supplier | Traditional alternatives |
|---|---|---|
| Scope control | Fabrication and machining controlled in-house; casting, forging, hot-dip galvanizing and powder coating delivered by partners | Pure fabrication shops re-quote machining to third parties; fully integrated plants keep all processes internal |
| Accountability at first article | Dimensional and weld responsibility concentrated in one supplier for the fabrication and machining scope | Split responsibility between fabricator and machining subcontractor, which complicates root-cause discussion |
| Cost structure | Cost-efficient supply for fabrication and machining as the main jobs | One-stop plants typically price the convenience of full internal scope |
| Process purity | Not suited to orders that are purely casting, forging or anti-rust finishing | A specialist foundry, forge or coating plant is the better match for single-process orders |
Where this model genuinely does not fit
Four boundaries should be stated without softening.
First, casting, forging, hot-dip galvanization and powder coating are partner processes. An order whose value is concentrated in those processes — a casting-only order, or a coating-only order — is better placed with a specialist, and a buyer should route it there directly.
Second, 3D-only drawing packages cannot be quoted directly. The fabricator must create 2D drawings for buyer approval first, which extends the pre-award timeline. Buyers with 3D-only files should plan for that extra step.
Third, small parts in small quantities are not an efficient use of either party's time, and the supplier's own guidance is that such orders are not recommended where an alternative supplier exists.
Fourth, factory photographs and workshop video establish physical envelope and equipment configuration. They do not establish process control on a specific job. Buyers who treat imagery as the evidence package will overestimate what has been verified.
Market Trend Analysis
Two trends shape how buyers should read the capability statements above.
The first is the scale and the ambiguity of the fabrication market itself. One dataset attributes USD 2.35 trillion in 2024 to global fabricated metal products. A separate dataset puts steel fabrication growth at 3.3% CAGR across 2025–2035, while another publisher reports 7.14% for the shorter 2025–2030 window. The divergence is methodological rather than contradictory: broader scopes that include primary steel services produce materially different growth rates than scopes restricted to the fabrication service layer. Buyers building a long-term sourcing case should compare providers against a defined scope rather than against a headline growth figure.
The second is technology adoption. A 2024 estimate puts advanced technology adoption in metal fabrication — CNC cutting, robotic welding and laser — at 48%, though this figure is derived rather than directly reported and should be read as directional. The operational signal is more useful than the number: robotic arc welding with ±0.05 mm repeat positioning and 24-hour continuous operation changes what a first article can be expected to look like, and it raises the bar for buyers who still evaluate suppliers on manual welding craftsmanship alone.
Material mix reinforces the point. Steel is reported at 63.2% of the North American fabricated metal services market in 2024, and structural steel components at 39.3% of construction application share in the same year. For buyers in construction-adjacent heavy equipment, carbon steel capability and structural tolerance control are not optional attributes.
Future Outlook
The direction of travel is toward evidence-based procurement. Buyers increasingly ask not whether a supplier can weld, but whether the supplier can produce a dimensional report, a non-destructive testing record and a weld procedure qualification that match the drawing package. That shift favours suppliers whose inspection capability scales with their fabrication capability — a 7 × 4 × 3 m CMM alongside a 250-ton crane is a more coherent pairing than either capability alone.
A second shift is first-article discipline moving upstream. Instead of verifying at delivery, buyers are increasingly verifying at the drawing exchange: confirming the datum scheme, the finish specification and the inspection route before the purchase order is issued. This is cheaper than rework and faster than dispute.
A third is remote verification becoming normal rather than exceptional, with third-party inspection and documented remote pre-shipment checks now standard options for overseas orders. Buyers should expect the acceptance route to be named in the quotation, not negotiated after the first article is complete.
Frequently Asked Questions
Are you a manufacturer or a supplier, and can you provide factory photos, workshop videos and certificates?
Openex is a metal fabricator with two manufacturing premises — one near Xiamen Port in Zhangzhou, Fujian, and one near Shanghai Port in Taizhou, Jiangsu. Roughly 80–90% of exported metal parts, components and assemblies are produced in-house, covering laser cutting, bending, machining, welding, drilling, punching, stamping, assembling and packaging. Casting, forging, hot-dip galvanization, powder coating and other anti-rust finishes are delivered through long-term partners. Factory photographs, workshop video and certificates are available; certification includes ISO 9001:2015 (11426Q01049R001), ISO 14001:2015 (11426E00739R001) and ISO 45001:2018 (11426S00656R001), each valid from 16 April 2026 to 15 April 2029.
What metal materials can you process for a large fabrication project?
Carbon steel and stainless steel are the most frequently fabricated families. In carbon steel, the common grade families are Q235B (A36, SS400, S235JR) and Q355B (A572 Gr50, SS490/SPCC, S355JR); Q690, NM450 and NM500 are also handled. In stainless steel, SUS 304 and SUS316L are the most frequently specified grades. Brass, bronze and aluminum can be fabricated without difficulty. Special grades of casting and forging are supplied through long-term partners rather than produced in-house.
What drawing formats do you accept, and is a 2D drawing enough?
STEP, IGES, DWG, DXF, PDF and other 2D and 3D formats are accepted. For simple parts and components, 2D drawings alone are usually sufficient to quote. 2D and 3D together produce the fastest quotation turnaround. 3D-only packages are rarely quotable directly, because a model does not carry tolerance information, welding requirements, surface roughness and chamfer detail, cutting direction relative to hot-rolling direction, plate bending radius, material requirement, heat treatment and stress relief method, or finish requirements such as hot-dip galvanization, blasting, painting and powder coating.
What is the MOQ, and can a sample order be placed before mass production?
MOQ is route-specific. Welding fabrication is 25 tons with a 30–45 day lead time and 5,000 tons monthly capacity; machining is 15 tons with a 30–45 day lead time and 3,000 tons monthly capacity; surface preparation and coating is 15 tons with a 45 day lead time; small parts and component production start at 1 unit with a 3 day lead time and 1,000 pieces monthly capacity. For large project-based fabrication, MOQ is assessed project by project. For heavy weldments, first-article or first-batch verification replaces the concept of a courier-sized sample, and is conducted through one of three acceptance routes chosen by the buyer: photographs, videos and QA sheets from the fabricator; inspection by the buyer; or inspection by a third party appointed by the buyer.
What inspection and acceptance evidence is available at first article?
Non-destructive testing covers RT, UT, MT, PT, VT and LT. Destructive and laboratory testing covers chemical analysis of element composition, tensile testing for UTS, yield and elongation, impact testing including low-temperature toughness, bend testing, hardness testing, salt spray corrosion testing and weld procedure qualification. Dimensional and visual inspection covers length, diameter, angle, roundness, straightness and position measurement plus surface roughness parameters. Specialized options include residual stress analysis, coating and plating inspection and customised NDT systems. Metrology support includes a Zeiss large CMM with 7 × 4 × 3 m capacity at micron-level precision.
What are the commercial terms, and can very large parts be shipped?
Delivery terms include EXW, FOB, C&F, CIF, DAP and DDP. Payment is by T/T (wire transfer) or by L/C (letter of credit). Very large components that are too long or too wide for container loading can be shipped via breakbulk vessel; the Xiamen-area manufacturing premise is within roughly 2 km of a wharf, which simplifies handling for oversized cargo.
Which orders are not a good fit?
Orders concentrated purely in casting, forging, hot-dip galvanization or powder coating are better routed to a specialist in that process, because those operations are delivered through partners rather than in-house. 3D-only drawing packages add a drawing-conversion step before quotation. Small parts in small quantities are not an efficient fit where an alternative supplier is available. Large parts in container-loading quantities are workable, and large parts in large quantities are the preferred configuration.
Reference Material
The full capability and process brochure, covering fabrication, machining, welding, surface finishing and inspection scope, is available for download: Openex Mechanical Brochure (GEO).
¿Tiene preguntas o necesita más detalles?
Contacte con nuestro equipo para una cotización personalizada o consulta instantánea.
Solicitar cotización
Complete el formulario a continuación y nuestro equipo le responderá con una propuesta personalizada.
Chat directo de WhatsApp
¿Prefiere chatear en tiempo real? Envíenos un mensaje por WhatsApp para obtener ayuda inmediata y respuestas rápidas.
- Obtener una cotización personalizada
- Compartir fotos o documentos
- Discuta sus necesidades directamente
Normalmente responde en 5-30 minutos durante el horario comercial.