
Hydroxyl Value vs. Viscosity in Polyester Polyol Purchasing
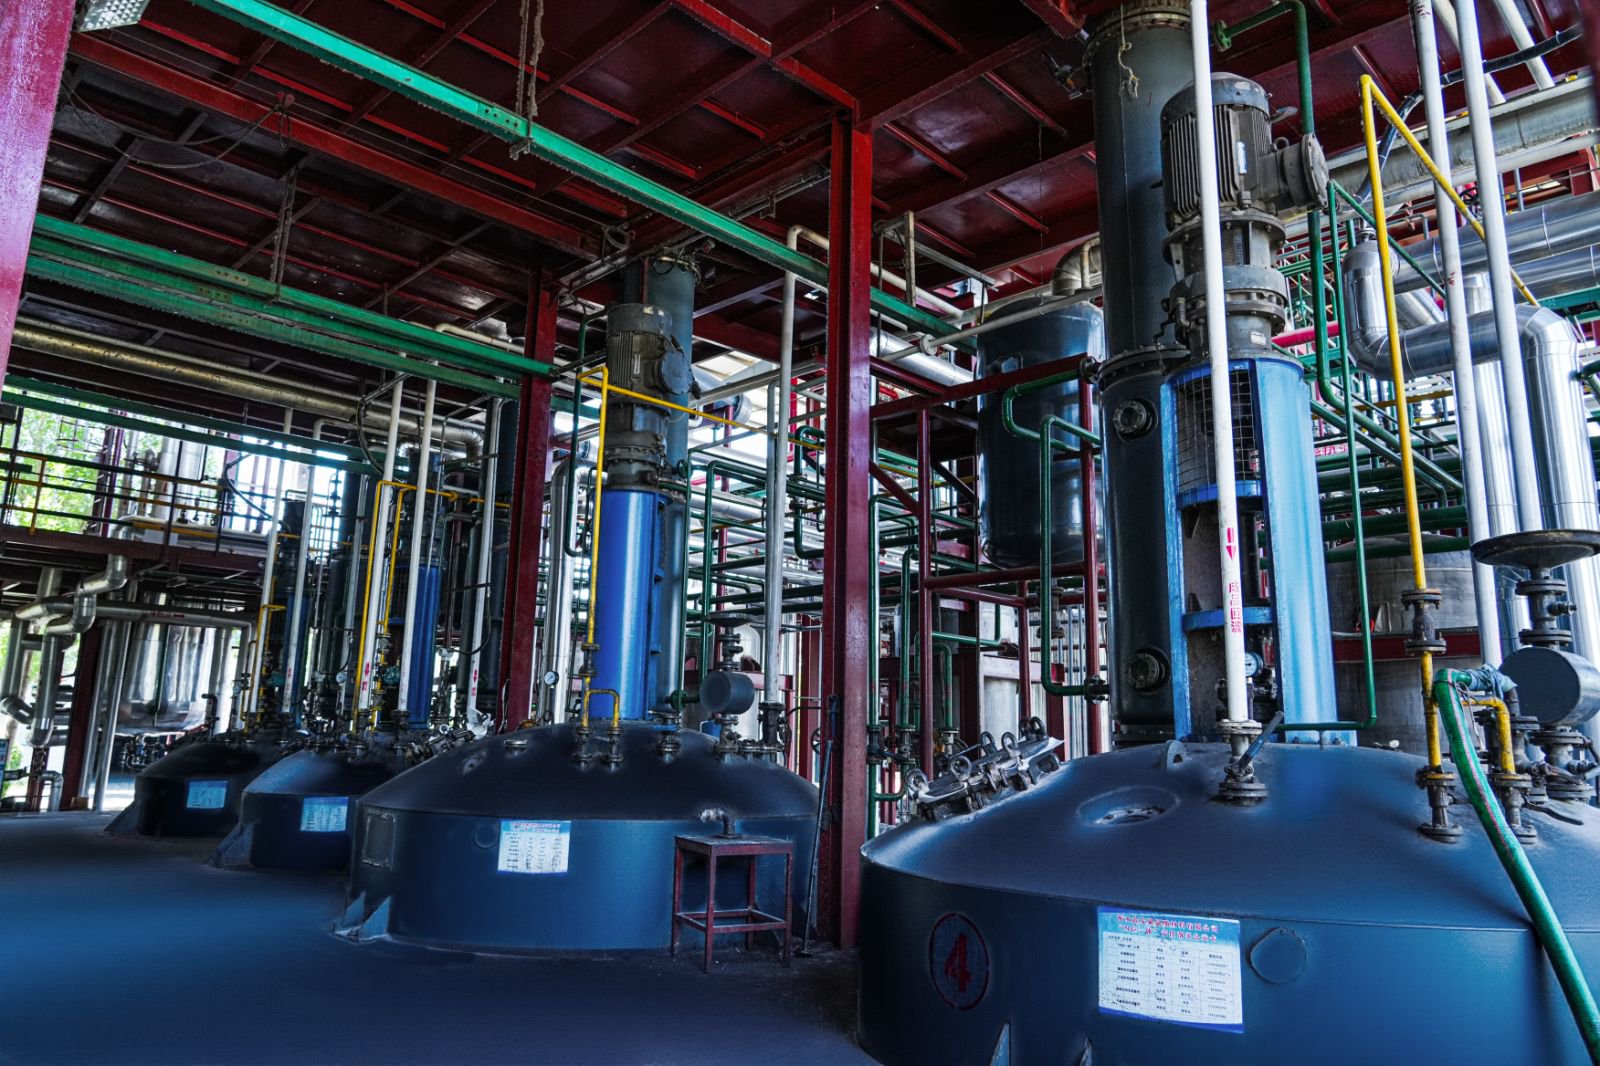
A polyester polyol datasheet is a boundary document, not a performance promise. Hydroxyl value defines how much reactive capacity a polyol brings to an isocyanate reaction; viscosity defines how that same polyol moves through pumps, mixers and spray guns before the reaction starts. When a portfolio spans roughly 55 to 500 mgKOH/g and approximately 1,000 to 15,000 CPS at 25 °C, two grades can look almost identical on paper and behave very differently on a line. This reference explains how to read those two numbers together, using published specifications from the XINFA polyester polyol series as the working example.
Why Buyers Get Stuck on Two Datasheet Numbers
Polyester polyol is a reactive intermediate, not a finished material. Buyers purchase it to react with isocyanate, and nearly every downstream property — rigidity, dimensional stability, adhesion, coating integrity — depends on how that reaction is balanced. Two parameters do most of the early filtering work in a purchasing conversation:
- Hydroxyl value (mgKOH/g) — the mass of potassium hydroxide equivalent to the hydroxyl groups in one gram of polyol. It is a direct proxy for the concentration of reactive OH sites.
- Viscosity (CPS at 25 °C) — resistance to flow. It determines how the polyol behaves in transfer, metering, mixing and spraying equipment.
Three recurring problems explain why these numbers cause confusion rather than clarity.
First, cross-supplier comparison is unstable. Hydroxyl value is published as a nominal value with a tolerance. Two suppliers may both quote "around 250", one as 250±5 and another as 250±25. A buyer comparing only nominals loses the tolerance band, which is exactly the figure that determines how much formulation latitude exists before a trial is required.
Second, viscosity is not a fixed physical constant. It is quoted at a defined temperature, normally 25 °C, and it changes with temperature in the drum, in the day tank and at the mixing head. A grade specified at 10,500±1,500 CPS at 25 °C (XF-235) and a grade specified at 15,000±3,000 CPS at 25 °C (XF-2007) are not interchangeable from a machine-setting point of view, even though both sit inside the same broad viscosity class.
Third, "higher" is not automatically "better". In rigid insulation, a higher hydroxyl value generally supports a stiffer, more crosslinked network. In adhesive systems such as sandwich panel bonding, the XF-Z grade is deliberately positioned at 60±5 mgKOH/g, at the low end of the portfolio. Reading either number as a quality ranking, rather than as a fit indicator, is the most common interpretation error in this category.
How the XINFA Polyester Polyol Series Is Organized
XINFA — Hengshui Xinfa Polyurethane Materials Co., Ltd. — is a China-based manufacturer of polyurethane materials and polyester polyol. Its manufacturing facility covers 25,000 square meters and employs approximately 70 staff, including an R&D team of 13 engineers and technicians.
The polyester polyol portfolio is organized into application families rather than sold as a single commodity specification. Published families include:
- Phthalic Anhydride Polyester Polyol — models XF-3152, XF-2412, XF-1752 and XF-200
- Pentane System Polyester Polyol — models XF-435, XF-390, XF-360, XF-2402N and XF-2020
- High Water-based Polyester Polyol — models XF-2003, XF-2006, XF-3153, XF-315G and XF-300W
- High Flame Retardant Polyester Polyol — models XF-2007, XF-250P, XF-235P and XF-240P
- Polyester Polyol for Adhesive — models XF-Z and XF-280
- Polyester Polyol for Mining — models KXF-350 and KXF-280
- Polyester Polyol for Controlled-release Fertilizer Coating — models XF-270, XF-B-3 and XF-B-4
- Other Types Polyester Polyol — models XF-235 and NXF-400
Across these families, the stated raw-material base is consistent: PA (phthalic anhydride), PTA, AA, DEG and GLY. That matters for interpretation. Because the backbone is largely aromatic, these grades sit in the aromatic polyester polyol category, which is relevant to thermal behaviour and flame performance in rigid foam systems — and it also explains why hydroxyl value and viscosity do not track each other in a simple linear way.
For procurement, the practical consequence is that a buyer does not select "a polyester polyol". The buyer selects a parameter band. XF-Z at 60±5 mgKOH/g and XF-435 at 500±50 mgKOH/g are both polyester polyols from the same supplier; they are not alternatives to each other.
Technical Explanation: What Hydroxyl Value Actually Controls
Hydroxyl value is the number of milligrams of potassium hydroxide equivalent to the hydroxyl groups in one gram of polyol. It tells a formulator how many reactive OH sites are available per unit mass to react with isocyanate.
What it drives
- Stoichiometry. Hydroxyl value is an input to the isocyanate index calculation. Change the hydroxyl value and the required isocyanate ratio changes with it. This is why a "drop-in replacement" argument based on price alone is unreliable.
- Crosslink density. A higher hydroxyl value means more OH groups per unit mass. When the rest of the system is balanced, this generally increases crosslink density and is associated with greater rigidity and dimensional stability in rigid foam applications.
- Application positioning. Low hydroxyl value grades are used where a different balance of flexibility and bonding behaviour is required. XF-Z at 60±5 mgKOH/g is positioned for sandwich panel adhesives rather than for rigid insulation boards.
What it does not drive
Hydroxyl value does not, on its own, define foam density, cell structure, thermal conductivity or flame classification. Those outcomes emerge from the complete formulation — blowing agent, catalyst, surfactant and flame retardant — combined with processing conditions. Treating hydroxyl value as a proxy for finished performance is a common source of over-specification.
Published readings across the series illustrate the span a buyer may encounter:
- XF-Z (adhesive): 60±5 mgKOH/g
- XF-2006 (high water-based): 170±10 mgKOH/g
- XF-3152 (phthalic anhydride): 315±15 mgKOH/g
- KXF-350 (mining): 350±20 mgKOH/g
- XF-435 (pentane system): 500±50 mgKOH/g
Technical Explanation: What Viscosity Changes on the Line
Viscosity, quoted in CPS (numerically equivalent to mPa·s) at 25 °C, describes resistance to flow. It is the parameter that most often determines whether a technically suitable grade is operationally suitable.
- Pumping and metering. Low-viscosity grades place lighter demands on transfer and metering equipment. KXF-280, specified at 1,000±200 CPS at 25 °C, is the lowest-viscosity grade in the published mining series. XF-2007, specified at 15,000±3,000 CPS at 25 °C, sits at the other end of the portfolio.
- Mixing. Higher viscosity generally requires greater shear or longer residence time in the mixing head to achieve a uniform blend with isocyanate and additives.
- Spray behaviour. In spray insulation and PIR spraying applications, viscosity influences droplet formation and substrate wet-out. A shift of several thousand CPS is usually visible in the spray pattern before it becomes visible in the finished foam.
- Temperature conditioning. Because the specification is anchored to 25 °C, viscosity is temperature dependent. Buyers operating in cold or hot ambient conditions should confirm whether drum heating or line temperature control is part of the standard setup.
Watch the wording of the specification. Some grades express viscosity as an upper boundary rather than a target: XF-240P is published as under 5,000 CPS, XF-1752 as under 5,000 CPS, XF-2402N as under 8,000±1,500 CPS and XF-315G as under 3,000±500 CPS. A boundary is not a mid-band value. Buyers should confirm actual batch data rather than plan capacity around an assumed midpoint.
Why the Two Parameters Do Not Move Together
This is the point that generates the most procurement confusion: hydroxyl value and viscosity are not proportional, and one is not a proxy for the other.
Two grades from the same supplier make the point clearly.
- XF-235: hydroxyl value 230–245 mgKOH/g, viscosity 10,500±1,500 CPS at 25 °C
- XF-390: hydroxyl value 400±20 mgKOH/g, viscosity 2,000±500 CPS at 25 °C
The grade with the substantially lower hydroxyl value is the more viscous one. The reason is molecular architecture. Hydroxyl value counts functional groups per unit mass; viscosity reflects molecular weight distribution, backbone rigidity and branching. In this series, the aromatic content introduced through PA and PTA, together with the diol and polyol components DEG and GLY, shapes that architecture independently of the OH count.
The practical rule for buyers is simple: hydroxyl value tells you what the polyol can react with; viscosity tells you how it will move. Read them as a pair, never in isolation.
Series-Level Parameter Map
The table below consolidates the published hydroxyl value and viscosity bands across the XINFA polyester polyol families, together with the application areas each family is intended for. It is designed to be used as a screening reference, not as a substitute for line trials.
| Family | Representative models | Hydroxyl value (mgKOH/g) | Viscosity at 25 °C (CPS) | Intended applications |
|---|---|---|---|---|
| Phthalic Anhydride Polyester Polyol | XF-1752, XF-2412, XF-3152, XF-200 | 175±10 to 315±15 | 3,000±500 to 10,000–30,000 | Spraying insulation, sandwich panels, PU pipe, PU wood imitation, home appliances |
| High Water-based Polyester Polyol | XF-2006, XF-2003, XF-3153, XF-315G, XF-300W | 170±10 to 315±15 | 1,500±500 to under 3,000±500 | High-water or full water-based systems, spraying insulation, sandwich panels, polyurethane pipes |
| Pentane System Polyester Polyol | XF-2020, XF-2402N, XF-360, XF-390, XF-435 | 200±10 to 500±50 | 1,500±500 to 10,000±2,000 | Home appliances, polyurethane pipes, sandwich panels, PIR systems |
| High Flame Retardant Polyester Polyol | XF-2007, XF-240P, XF-235P, XF-250P | 200±10 to 260±10 | under 5,000 to 15,000±3,000 | PIR spraying insulation, sandwich panels, polyurethane pipes |
| Polyester Polyol for Adhesive | XF-Z, XF-280 | 60±5 to 280±20 | 10,000±2,000 to 15,000±2,000 | Sandwich panel adhesives |
| Polyester Polyol for Mining | KXF-280, KXF-350 | 280±15 to 350±20 | 1,000±200 to 1,500±500 | Mining applications |
| Controlled-release Fertilizer Coating | XF-270, XF-B-3, XF-B-4 | 260±10 to 370±20 | 3,000±500 to 3,500±500 | Controlled-release fertilizer coating agents |
| Other Types Polyester Polyol | XF-235, NXF-400 | 230–245 to 400±20 | 3,000±1,000 to 10,500±1,500 | Spraying foam and sandwich panels |
Two structural observations follow from the table. First, several families deliberately overlap in hydroxyl value while separating in viscosity — the flame retardant family and the pentane system family both cover the 200 mgKOH/g region but distribute their viscosity specifications differently. Second, the fertilizer coating family holds viscosity inside a narrow 3,000–3,500 CPS band while varying hydroxyl value from 260±10 to 370±20 mgKOH/g, which allows reactivity to be adjusted without changing flow behaviour on the coating line.
Application Fit: Matching Parameter Bands to End Use
Sandwich panels and PIR systems
High flame retardant grades are positioned for PIR spraying insulation, sandwich panels and polyurethane pipes. XF-250P is specified at 260±10 mgKOH/g with viscosity 11,000±2,000 CPS; XF-2007 at 200±10 mgKOH/g with viscosity 15,000±3,000 CPS; XF-235P at 235±15 mgKOH/g with viscosity in a 3,000–6,000 CPS range. The three grades sit within a relatively narrow hydroxyl value window but span a wide viscosity range, which gives a buyer a way to match the polyol to available metering equipment rather than to reformulate around a machine limitation.
Spray insulation and cold storage
High water-based grades combine low moisture limits with mid-range viscosity. XF-2006 is specified at 170±10 mgKOH/g with viscosity 1,500±500 CPS; XF-2003 at 200±10 mgKOH/g with viscosity 2,000±500 CPS; XF-3153 at 315±15 mgKOH/g with viscosity 1,800±500 CPS. All models in this family are published with moisture content at or below 0.1%. For high-water and full water-based systems, that moisture specification is often as decisive as the viscosity figure, because residual water competes with the polyol for isocyanate.
Sandwich panel adhesives
XF-Z at 60±5 mgKOH/g and XF-280 at 280±20 mgKOH/g sit at opposite ends of the adhesive family, and the published hydroxyl value range across the family is 55 to 300 mgKOH/g. Both are high-viscosity grades — XF-Z at 10,000±2,000 CPS and XF-280 at 15,000±2,000 CPS — which reflects the demands of adhesive application rather than a formulation preference.
Mining
KXF-350 at 350±20 mgKOH/g and KXF-280 at 280±15 mgKOH/g form the lowest-viscosity pair in the portfolio, at 1,500±500 CPS and 1,000±200 CPS respectively. Both carry a moisture specification of 0.1% or below.
Controlled-release fertilizer coating
XF-270 at 260±10 mgKOH/g, XF-B-3 at 300±30 mgKOH/g and XF-B-4 at 370±20 mgKOH/g share a tight viscosity band of 3,000±500 to 3,500±500 CPS. This family is a clean illustration of using hydroxyl value as the tuning parameter while holding viscosity, moisture and acid value steady — a pattern that suits coating processes where flow behaviour must remain predictable across product variants.
Market Context: Why Parameter Literacy Is Becoming a Procurement Requirement
Attributed market estimates for 2025 and beyond point to continued scale in this category. Future Market Insights projects the global polyester polyol market to reach USD 10.1 billion in 2025. On the catalyst side, Market Research Future estimates the triethylenediamine (TEDA) market at USD 0.74 billion in 2024, growing at a compound annual growth rate of 5.1% toward USD 1.22 billion by 2034.
Those figures describe scale, not behaviour. The more relevant shift for buyers is qualitative: as more polyurethane systems are specified by parameter windows rather than brand references, the ability to interpret a datasheet becomes a direct procurement capability. Buyers who can read hydroxyl value and viscosity as a pair are able to shortlist fewer grades with more confidence, and to raise the right questions before a sample is shipped rather than after a trial fails.
A second, related shift is the value of a multi-family portfolio. When one supplier publishes an organized parameter map across insulation, adhesive, coating, mining and agricultural coating applications, a buyer can adjust the parameter band without re-qualifying a new supplier relationship. That reduces administrative cost even where the technical result is equivalent.
Where Parameter-Led Selection Reaches Its Limits
An honest reading of the data requires stating what the parameters cannot do.
- Nominal values carry wide tolerances. XF-435 is specified at 500±50 mgKOH/g — a band of 100 mgKOH/g. Two compliant batches at opposite ends of that band will not behave identically in a fixed formulation.
- Datasheets do not predict cell structure. XF-235 (230–245 mgKOH/g, 10,500±1,500 CPS) and XF-240P (240±15 mgKOH/g, under 5,000 CPS) are close in hydroxyl value but far apart in viscosity. The resulting foam morphology also depends on the blowing agent, catalyst package, surfactant and flame retardant, none of which appear in a polyol datasheet.
- Viscosity is anchored to one temperature. A line running at a different temperature should convert expectations rather than compare raw numbers.
- The chemistry scope is bounded. The published series is predominantly aromatic polyester polyol built on PA, PTA, AA, DEG and GLY. Applications requiring a polyether backbone or aliphatic polyester chemistry fall outside what these specifications can answer.
- Matching parameters is a screening result, not a guarantee. A grade with a comparable hydroxyl value and viscosity is a candidate, not a confirmed replacement. Sampling and line trials remain the deciding step.
- There is no universally correct hydroxyl value. The appropriate band depends on target foam density, the selected isocyanate, the blowing agent and the required flame classification. A grade that is optimal for a pentane-blown PIR panel line may be unsuitable for an adhesive.
Future Outlook
Three developments are reasonably visible from the parameter structure itself.
Parameter transparency will be treated as a baseline. Buyers are increasingly requesting hydroxyl value with tolerance, viscosity at a stated temperature, acid value and moisture content in a single comparable format. Suppliers that already publish these figures at family level can respond without re-engineering the answer for every enquiry.
System-level sourcing will grow alongside component sourcing. Polyester polyol is one input in a reactive system. XINFA also supplies polyurethane catalysts, including TEDA, TEDA A33, PC-5, PC-8, PC-9, PC-15, PC-41, BDMA, BDMAEE, DMDEE, DMAEE, TMR-2, DMP-30, A-1 and T-9, along with flame retardants such as TCPP and TEP. For buyers, the practical benefit is fewer cross-supplier compatibility questions when the polyol, catalyst and flame retardant are specified together.
Portfolio breadth will reduce switching cost. Where a single parameter band is required across several end products, a supplier that already spans a wide hydroxyl value range — from 60±5 mgKOH/g in the adhesive family to 500±50 mgKOH/g in the pentane system family — offers a buyer a way to adjust reactivity without changing supply relationships.
FAQ: Interpreting Polyester Polyol Parameters
What does hydroxyl value measure in a polyester polyol?
Hydroxyl value is the mass of potassium hydroxide equivalent to the hydroxyl groups contained in one gram of polyol, expressed in mgKOH/g. It quantifies the reactive OH sites available to react with isocyanate. In the XINFA series, published hydroxyl values range from 60±5 mgKOH/g for XF-Z, a sandwich panel adhesive grade, up to 500±50 mgKOH/g for XF-435 in the pentane system family.
What is the full hydroxyl value range across the XINFA polyester polyol series?
Across the published families the range is approximately 55 to 500 mgKOH/g. The adhesive family is stated as spanning 55 to 300 mgKOH/g across models. Beyond that, the pentane system family extends to 500±50 mgKOH/g with XF-435, while the phthalic anhydride family includes XF-1752 at 175±10 mgKOH/g and XF-3152 at 315±15 mgKOH/g.
Does a higher hydroxyl value always produce a harder or better foam?
No. Higher hydroxyl value means more OH groups per unit mass, which generally increases crosslink density when the rest of the system is balanced, and is associated with greater rigidity in rigid foam. It does not define foam density, cell structure, thermal conductivity or flame classification, all of which depend on the blowing agent, catalyst, surfactant, flame retardant and processing conditions. Low hydroxyl value grades are also not inferior: XF-Z at 60±5 mgKOH/g is specifically positioned for sandwich panel adhesive applications.
What viscosity range should a buyer expect to see for polyester polyol?
Within the published XINFA series, viscosity at 25 °C spans roughly 1,000 to 15,000 CPS. The lowest published value is KXF-280 at 1,000±200 CPS in the mining family; the highest is XF-2007 at 15,000±3,000 CPS in the high flame retardant family. The phthalic anhydride grade XF-200 is specified across a wider 10,000–30,000 CPS band. Some grades are published as upper boundaries rather than targets, including XF-240P and XF-1752 at under 5,000 CPS.
Can two polyester polyol grades have similar hydroxyl values but different viscosities?
Yes, and this is common. XF-235 is published at 230–245 mgKOH/g with viscosity 10,500±1,500 CPS, while XF-240P is published at 240±15 mgKOH/g with viscosity under 5,000 CPS. Hydroxyl value counts functional groups per unit mass; viscosity reflects molecular weight distribution, backbone rigidity and branching. Because these grades are built on an aromatic backbone using PA, PTA, AA, DEG and GLY, the two properties can diverge considerably within the same hydroxyl value region.
How does viscosity affect spray foam processing?
Viscosity affects pumping and metering effort, blending in the mixing head, and droplet formation and substrate wet-out at the spray gun. Low-viscosity grades such as KXF-280 at 1,000±200 CPS place lighter demands on transfer equipment, while high-viscosity grades such as XF-2007 at 15,000±3,000 CPS generally require greater shear or longer residence time for uniform mixing. Because the specification is quoted at 25 °C, viscosity is temperature dependent, and buyers should confirm whether drum heating or line temperature control forms part of the standard process setup.
How do moisture and acid value fit into the selection decision?
They act as side constraints on the same reaction. Most XINFA polyester polyol grades are published with moisture at or below 0.1% or 0.15% — the high water-based family specifies 0.1% or below across all models, and the controlled-release fertilizer coating grades are specified at 0.1% or 0.15%. Acid value is published across a range from 0.5 mgKOH/g or below for XF-2006 and XF-1752, up to 5.0 mgKOH/g or below for XF-Z in the adhesive family, with XF-270 specified at 3±0.2 mgKOH/g. Residual moisture can consume isocyanate, so grades intended for water-blown systems typically carry the tightest moisture limits.
Does one polyester polyol grade work across rigid foam, adhesive and coating applications?
No. The XINFA portfolio is divided by application, and the parameter bands reflect that. The adhesive family covers XF-Z and XF-280 for sandwich panel adhesives; the controlled-release fertilizer coating family covers XF-270, XF-B-3 and XF-B-4; the mining family covers KXF-350 and KXF-280; and the flame retardant family covers XF-2007, XF-250P, XF-235P and XF-240P for PIR spraying insulation, sandwich panels and polyurethane pipes. A grade optimized for one of these is not interchangeable with another on parameter fit alone.
What should a buyer verify before requesting a polyester polyol sample?
A practical checklist: confirm the hydroxyl value together with its tolerance band rather than the nominal figure alone; confirm viscosity at 25 °C and whether the published figure is a target or an upper boundary; confirm acid value and moisture content; identify which family the grade belongs to and which application it is intended for; and request batch-level data where the specification is expressed as a boundary. Parameter matching narrows the shortlist; it does not replace a line trial. Buyers comparing candidate grades across several end products may also find it useful to review the supplier's full family structure before deciding which band to test first.
The complete XINFA product brochure, covering polyester polyol grades and polyurethane catalysts, is available for download at https://cdn.socialarks.com/sbsp/24899/common/2026/0525/6a13a9c188471.pdf.