
Flare System Trade-offs: Configuration, Materials, Compliance
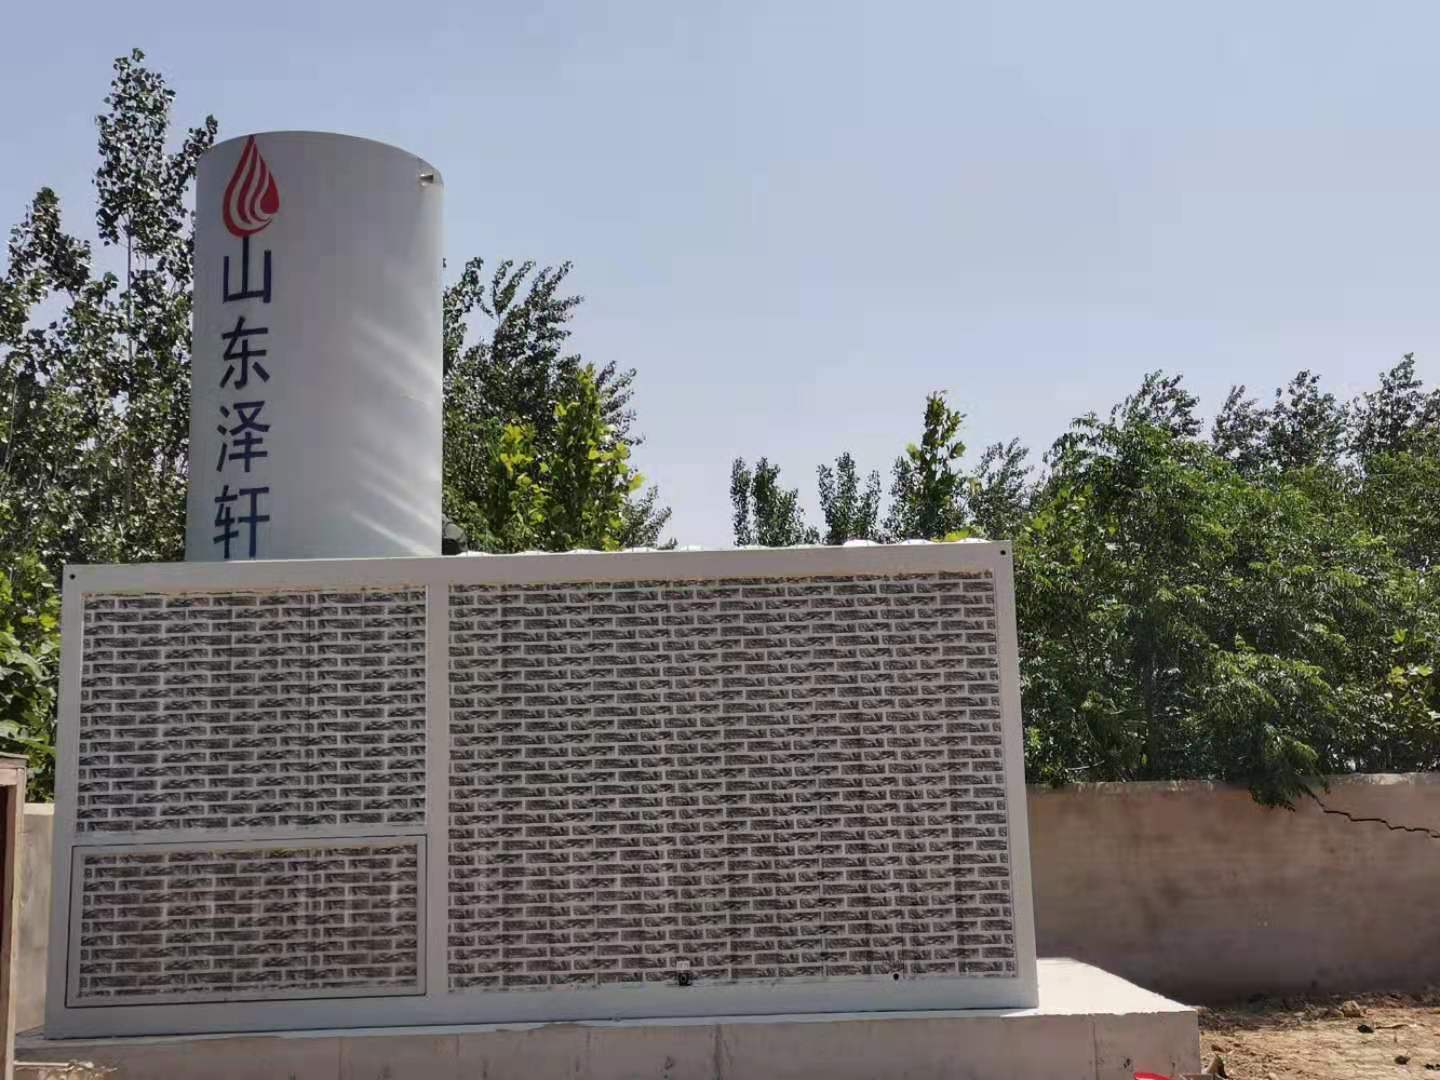
Figure 1 — A skid-mounted ground flare system: combustion capacity assembled on a transportable skid, a configuration choice that trades capacity ceiling for installation speed.
Global gas flaring volumes reached 151 billion cubic meters (bcm) in 2024, the highest level recorded since 2007, according to World Bank flaring data. In parallel, the global flare systems market was valued at approximately USD 4.8 billion in 2025 (Dataintelo). Those two figures point in the same direction: flare and thermal treatment capacity is increasingly treated as an engineering and compliance asset, not a fixed line item on a plot plan.
For buyers, the difficulty is that tender packages rarely separate the three decisions that determine whether a flare system performs as intended. Configuration decides whether the structure fits the site. Materials decide whether the system survives the gas. Compliance evidence decides whether the installation can be defended in a permit review, an audit or a factory acceptance test. Collapsing these into a single price comparison is one of the most common sources of later rework.
This article sets out a decision framework that moves through configuration, combustion duty, materials, compliance evidence and execution terms in sequence. Specifications and project references used below come from Shandong Zexuan Environmental Protection Technology Co., Ltd. (Zexuan), a manufacturer and engineering service provider established in 2015 that builds industrial flare systems, thermal oxidizers and waste gas combustion equipment for oil & gas, refining and petrochemical, LNG, chemical, landfill gas and biogas applications.
Why Configuration, Material and Compliance Are Three Separate Decisions
Flare system design is primarily governed by API Standard 521 (Pressure-Relieving and Depressuring Systems). The standard specifies, among other mechanical requirements, a minimum flare header slope of 1/4 inch per 10 feet for drainage — a small detail that illustrates a larger point: the design basis is set by relief scenarios, while the configuration and material envelope remain engineering choices with consequences.
Those choices interact. Selecting an enclosed ground flare changes the plot layout, the radiation and noise profile, and the maintenance routine. Specifying a higher-alloy tip changes cost and fabrication complexity. Choosing a skid-mounted design changes how much capacity can be delivered on one transportable frame. Because the decisions are sequenced, an early commitment constrains everything after it — which is why procurement teams generally get better outcomes by working configuration first, then duty, then material, then evidence.
Step 1 — Select the Structural Configuration Against the Site Envelope
Elevated flare systems in the Zexuan range are available as self-supported, guyed-wire, derrick-supported and demountable configurations, complemented by enclosed ground flares and skid-mounted or mobile units. Each structure solves a different constraint.
Figure 2 — An enclosed ground flare: combustion is contained at grade with a low-radiation, low-noise design, which changes both the plot plan and the inspection routine.
| Configuration | Structural logic | Typical industrial fit | Principal trade-off |
|---|---|---|---|
| Self-supported elevated flare (ZX-SSEF Series) | Free-standing stack, no guy wires or derrick | Sites with constrained ground area around the stack base | Structural steel weight and cost rise quickly as stack height increases |
| Guyed-wire elevated flare (ZX-GWF Series) | Stack stabilised by guy wires and anchors | Taller stacks where a wider land take is acceptable | Requires anchor footprint and periodic inspection of wire and anchor systems |
| Derrick-supported elevated flare (ZX-DSF Series) | Structural derrick carries and services the stack | Heavy stacks and sites that need maintenance access to the stack | Highest structural complexity and footprint among elevated options |
| Demountable flare | Stack designed for dismantling and relocation | Projects with relocation, staged build or transport constraints | Additional joints require engineering control and inspection discipline |
| Enclosed ground flare (ZX-EGF Series) | Enclosed multi-burner combustion at grade with refractory lining | Petrochemical parks, chemical plants, LNG terminals, hazardous gas treatment, industrial parks | Removes visible stack height and reduces radiation and noise, but consumes grade-level plot area and requires refractory maintenance |
| Skid-mounted / mobile flare (ZX-SMF Series, ZX-MTF Series) | Factory-assembled skid or trailer-mounted unit | LNG receiving terminals, LNG bunkering, gas storage, pipeline facilities, offshore gas applications, temporary duty | Capacity is bounded by transportable dimensions; fast installation and commissioning come with that ceiling |
Elevated systems are typically quoted across a flare height range of 10 m to 150 m or more, with flare tip diameter customised to flow rate and gas properties, a turndown ratio of up to 100:1, operating temperature up to 1100°C, and combustion efficiency typically between 98% and 99.9% depending on design and operating conditions. Those are headline envelopes, not guarantees: the actual figure follows from the relief case the buyer supplies.
Step 2 — Fix the Combustion Duty: Temperature, Efficiency and Operating Mode
Once the structure is fixed, the combustion duty determines the internals. Two performance bands recur across flare and thermal treatment equipment:
- Enclosed ground flares (ZX-EGF Series) operate at 800°C–1200°C with combustion efficiency up to 99.9%, supported by a low-radiation design and multiple burner configurations.
- Thermal oxidizers (ZX-TO, ZX-RTO and ZX-RCO Series) operate at 800°C–1200°C with VOC destruction efficiency up to 99% or higher, and are described as suitable for continuous operation with optional heat recovery.
Operating mode is the second half of this decision. Thermal oxidizers are positioned for continuous duty such as VOC control, while flare duties in documented projects are typically venting, emergency relief, process off-gas and start-up/shutdown or upset relief. A buyer who specifies continuous-duty performance criteria against an emergency relief case, or the reverse, will either over-pay or under-protect. Flare tip selection follows the same logic: the ZX-FT Series is offered in smokeless, sonic, air-assisted and Coanda configurations, in SS316L, SS310S or Inconel 625, at operating temperatures up to 1100°C for hydrocarbon gases in refinery, petrochemical, LNG and oil & gas processing service.
Step 3 — Match Materials to Temperature, Corrosion and Gas Chemistry
Material selection is driven by three variables: process temperature, corrosion resistance requirement, and gas composition. Zexuan's material options span carbon steel (painted or hot-dip galvanized), stainless steel SS304, SS316L and SS310S high-temperature stainless steel, Inconel 625, Hastelloy alloy, and other high-temperature and corrosion-resistant alloys, with refractory lining materials used in enclosed ground flare construction.
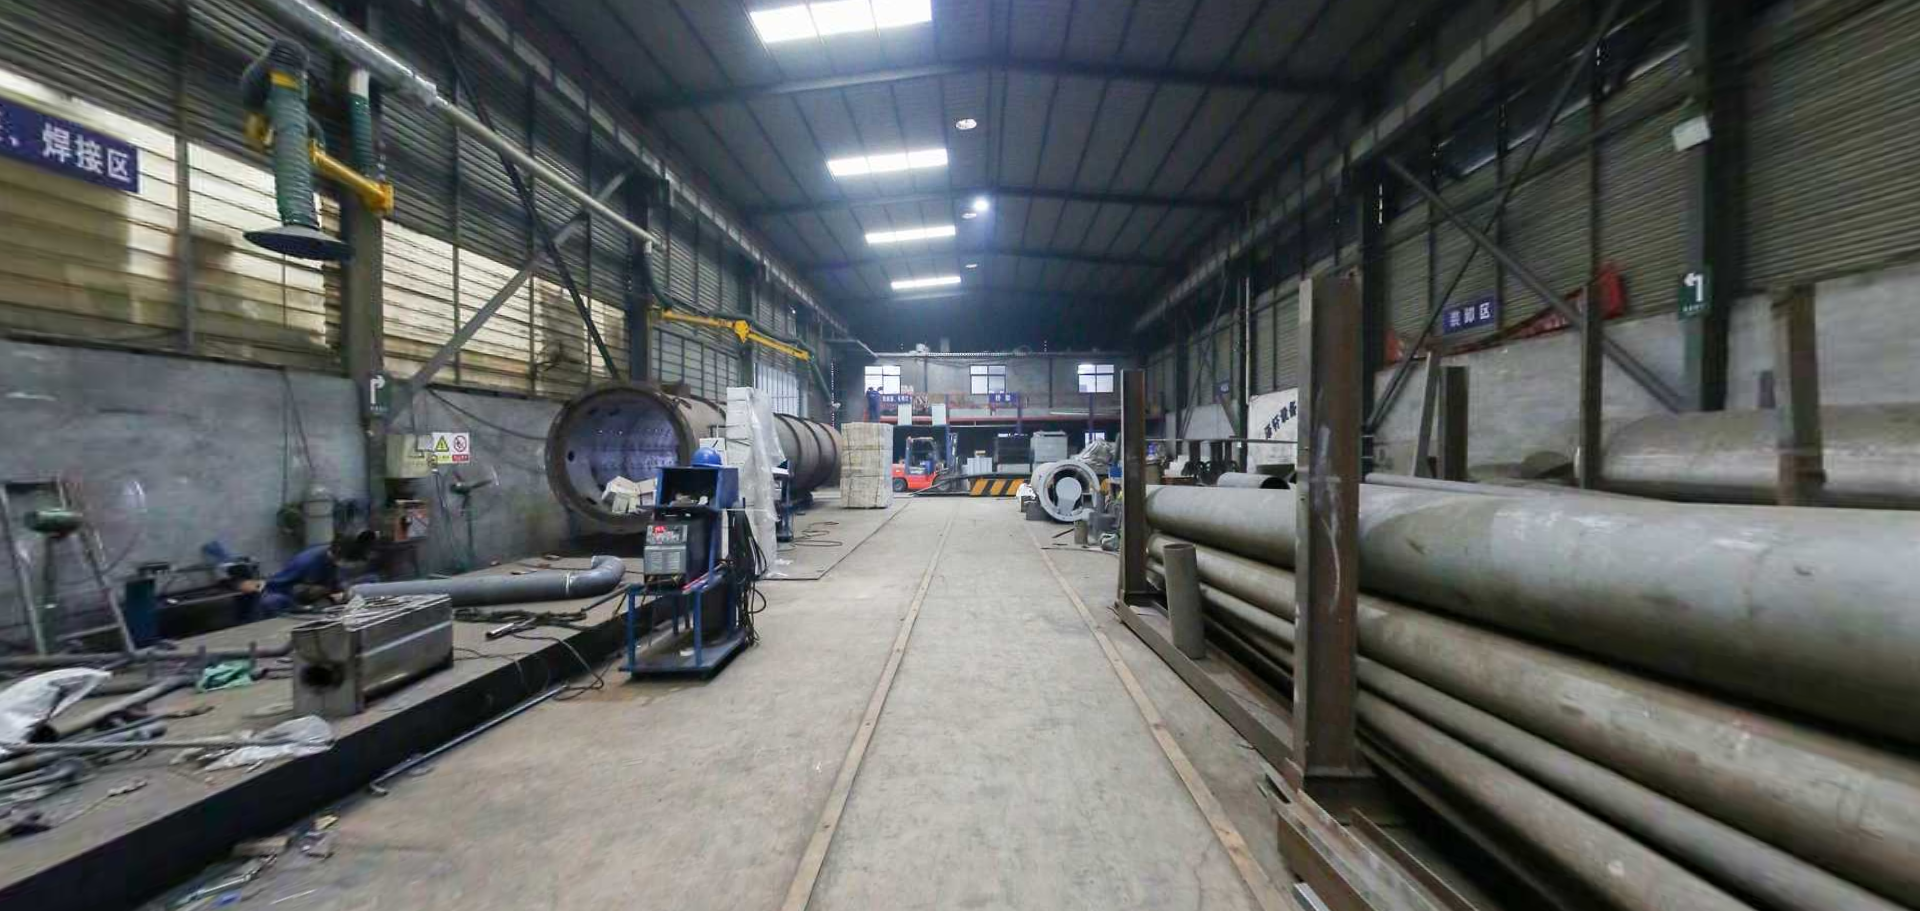
Figure 3 — Fabrication workshop: the material decision is executed at welding and assembly stage, which is why alloy choice is confirmed before production release rather than after.
| Material | Where it is typically specified | Trade-off to weigh |
|---|---|---|
| Carbon steel (painted or hot-dip galvanized) | Structural and general support sections | Lowest material cost, but coating maintenance and temperature limits apply |
| SS304 | Moderate-temperature, moderate-corrosion service | Balanced cost and corrosion resistance; limited at higher temperatures |
| SS316L | Flare tips, enclosed ground flare internals, corrosion-sensitive wetted parts | Higher corrosion resistance at higher cost than SS304 |
| SS310S high-temperature stainless steel | High-temperature sections adjacent to combustion | Selected for thermal duty; more demanding to fabricate |
| Inconel 625 | High-temperature flare tip parts exposed to sustained flame | Highest cost tier, justified only where temperature demands it |
| Hastelloy alloy and other high-temperature / corrosion-resistant alloys | Aggressive media and severe corrosion environments | Availability and fabrication planning need to be confirmed early |
| Refractory lining materials | Enclosed ground flare enclosures | Improves thermal containment; introduces a defined inspection and maintenance cycle |
| Low-temperature materials for LNG service | Skid-mounted LNG / LPG and BOG flare systems (ZX-SMF Series) | Cryogenic compatibility constrains material and joint design |
Material is one of the explicit customisation variables on the Zexuan configurable list, alongside flare type, capacity, structure, control system, layout, voltage and documentation. Buyers should treat it as a specification decision with cost consequences rather than a default: the rational choice is usually the lowest alloy grade that satisfies the temperature and corrosion envelope derived from the gas analysis.
Step 4 — Convert Compliance into Evidence: Standards, Certificates and Tests
Compliance is often described in tenders as a list of standards. In practice, buyers need to see what a supplier's certificates actually cover, because management-system certification and equipment-type approval are different things.
| Certificate | Number | Validity | Scope of coverage |
|---|---|---|---|
| Quality Management System Certification — GB/T 19001-2016 / ISO 9001:2015 | 26326Q00079R001 | Issued 2026-03-18, valid to 2029-03-17 | Development of waste gas treatment equipment and control units; sales of waste gas and waste liquid treatment equipment |
| Environmental Management System Certification — GB/T 24001-2016 / ISO 14001:2015 | 26326E00054R001 | Issued 2026-03-18, valid to 2029-03-17 | Waste gas treatment equipment and control units, sales of waste gas and waste liquid treatment equipment, and related environmental management activities |
| Occupational Health and Safety Management System Certification — GB/T 45001-2020 / ISO 45001:2018 | 26326S00054R001 | Issued 2026-03-18, valid to 2029-03-17 | Waste gas treatment equipment and control units, sales of waste gas and waste liquid treatment equipment, and related occupational health and safety management activities |
All three certificates were issued by CSU International Certification Co., Ltd., and are recognised on the domestic China market for government bidding, tendering and procurement with the CNAS accreditation mark, and internationally through mutual recognition by IAF member economies under the IAF multilateral recognition mark. Buyers should note the boundary: these are management-system certificates within a defined scope. They support supplier qualification, but they do not replace project-level proof, which is delivered through incoming material inspection, welding inspection, dimensional inspection, pressure and leak testing where applicable, functional testing, a Factory Acceptance Test (FAT), and final inspection before shipment under a 100% inspection regime.
Step 5 — Lock Execution and Commercial Terms Before the Purchase Order
The last step in the framework is the one most often left to negotiation rather than engineering. Documented commercial terms for Zexuan's industrial flare and thermal treatment systems include a minimum order quantity of 1 set, since systems are customised to project requirements; delivery terms of EXW, FOB or CIF; acceptance based on Factory Acceptance Test (FAT) and Site Acceptance Test (SAT); and payment through T/T or L/C, typically 30% advance payment and 70% before shipment, negotiable according to project requirements.
Execution capacity matters as much as price. The company operates a 24,100 m² manufacturing base with more than 80 employees, including 30+ engineering and technical specialists and 20+ engineers in the technical team, and reports an annual manufacturing capacity of 60+ sets of flare and thermal treatment systems, with monthly capacity of 5 sets for customised industrial systems and a typical production lead time of 60–120 days depending on project requirements. After-sales scope covers remote support, commissioning assistance, spare parts and training. Zexuan operates as a manufacturer, OEM, ODM and engineering solution provider, with OEM and ODM services available, and reports project experience in more than 10 countries across the Middle East, Central Asia, Southeast Asia, Africa and Russia.
Applying the Framework: A Project-Type Decision Matrix
| Project context | Configuration priority | Material priority | Compliance / evidence priority |
|---|---|---|---|
| Refinery or petrochemical unit with limited plot area | Elevated flare (self-supported, guyed-wire or derrick) or enclosed ground flare where grade area allows | High-temperature alloys at the tip; stainless internals | API 521 design basis, management-system certificates, FAT |
| LNG terminal, bunkering or BOG service | Skid-mounted or mobile flare (ZX-SMF Series) | Low-temperature materials for LNG service | FAT plus site acceptance and a complete documentation package |
| Pipeline or compressor station emergency relief | Elevated or enclosed ground flare depending on space, noise and radiation constraints | Coated carbon steel structure with stainless tip | Documented relief scenarios and functional testing records |
| Landfill gas, biogas or digester gas | Enclosed ground flare or ground flare | Corrosion-resistant grade selected against gas chemistry | Combustion efficiency verification and emission documentation |
| Pyrolysis or chemical off-gas with variable composition | Skid-mounted ground flare with control system | Stainless steel internals matched to agressive media | PLC control documentation, FAT and SAT |
| Temporary, staged or relocation projects | Demountable or trailer-mounted flare | Material chosen with transport weight considered | Inspection records covering transport and re-assembly joints |
Documented Project Scenarios
The framework is easier to test against real installations than against specification sheets. Four documented configurations illustrate how the trade-offs resolve in practice.
Guyed-wire elevated flare in natural gas gathering. Two sets were installed for a natural gas processing operation in China for emergency venting and safe combustion during gathering and transportation. The system uses a 60 m elevated structure, a DN350 flare tip, and automatic ignition with PLC control, and has operated stably under harsh climate conditions for more than a year.
Enclosed ground flare at an oilfield transfer station. One set was installed in China to treat natural gas vent gas, completed within one year. Features include an enclosed design, an explosion-proof control cabinet and an automatic ignition system. Reported outcomes include safe disposal of natural gas emissions, reduced noise and visual impact, and stable operation.
Ground flare for coalbed methane. A ground flare with a documented processing capacity of 90×10⁴ Nm³/d, a three-stage venting design and PLC automatic control has been operating for more than two years, delivering stable methane combustion and improved gas management safety.
Skid-mounted ground flares in pyrolysis service. A unit in Iraq has treated combustible pyrolysis gas from waste tire recycling for more than three years, using a skid-mounted modular design customised to pyrolysis gas characteristics and addressing uncontrolled gas emissions. A comparable unit in Turkey has operated for more than two years with a compact modular structure. In Vietnam, a skid-mounted ground flare was installed for pyrolysis gas from a waste plastic conversion process, designed for variable gas conditions.
Where This Framework Stops: Limits and Residual Risk
A framework is a screening tool, not a substitute for project engineering. Several boundaries should be stated plainly.
- Relief load is project-specific. API 521-compliant design requires the actual relief scenarios, gas composition and flow cases. The specification ranges quoted here — 10 m to 150 m+ stack height, up to 1100°C, turndown up to 100:1, combustion efficiency from 98% to 99.9% — describe envelopes, not deliverables.
- Enclosed ground flares are not a universal answer to space. They reduce stack height, radiation and noise, but they occupy grade-level plot area and introduce a refractory-lined enclosure with a defined maintenance cycle.
- Skid-mounted designs have a capacity ceiling. Transportable dimensions bound what can be delivered on one skid, so a skid-mounted unit is not interchangeable with a large refinery flare system.
- Higher alloy grades are not automatically better. Inconel 625 and Hastelloy options sit at the top of the cost range and are justified only where temperature or corrosion conditions require them.
- Certificates have scope boundaries. ISO 9001, ISO 14001 and ISO 45001 certification covers management systems within a defined scope of waste gas treatment equipment and control units; it is supplier qualification evidence, not an equipment-type approval.
- Market forecasts vary by methodology. Published estimates of the flare gas recovery market differ widely — one source projects USD 5.84 billion by 2031 (Mordor Intelligence) while another projects USD 8.52 billion by 2032 (Fortune Business Insights) — so such figures should be read as directional rather than precise.
Market Signals Shaping Flare System Purchasing
Three market signals support the shift toward evidence-based flare procurement. First, emissions pressure is measurable: 151 bcm of global flaring in 2024, the highest since 2007, indicates that relief and venting systems remain a compliance exposure rather than a solved problem. Second, the enclosed combustion segment is growing: the global totally enclosed ground flare (TEGF) market was valued at USD 113 million in 2024, with growth driven by destruction efficiencies exceeding 98%. Third, VOC control investment is scaling alongside flare demand: the VOC control systems market, including thermal oxidizers and incinerators, is estimated at USD 7.5 billion in 2025, with China identified as a key growth market at a 5.4% CAGR.
Regionally, Asia-Pacific holds a 35% share of the flare gas recovery system market as of 2025, the largest regional share globally. The supplier landscape remains concentrated among established combustion specialists — Zeeco, John Zink Hamworthy (Koch), Honeywell UOP and Baker Hughes are widely identified as major participants — alongside manufacturers serving regional and project-specific demand. For buyers, that means shortlisting logic should separate global combustion specialists from suppliers whose strength is customised engineering and project execution.
What Changes Next for Flare System Buyers
The direction of travel is toward systems that are measured, not merely installed. Regulatory scrutiny of hydrocarbon emissions, combined with continued oil and gas investment, keeps flare and thermal treatment capacity in the capital plan. What changes is the evidence expected at handover: destruction efficiency claims supported by test records, control systems that log operating conditions, and documentation that survives an audit years after commissioning.
Zexuan's stated development direction — low-carbon combustion technologies, intelligent control systems, flare gas recovery and digital operation solutions — reflects that shift, and so does the practical emphasis on FAT/SAT acceptance and full process inspection. For procurement teams, the implication is straightforward: the framework in this article is worth applying early, because configuration, material and compliance decisions are cheapest to make before the purchase order and most expensive to correct after installation.
FAQ
1. How should a buyer decide between an elevated flare and an enclosed ground flare?
The deciding factors are site geometry and the acceptable radiation, noise and visual profile. Elevated configurations — self-supported (ZX-SSEF Series), guyed-wire (ZX-GWF Series), derrick-supported (ZX-DSF Series) or demountable — release combustion at height and keep the ground area around the stack relatively clear, while structural weight and cost rise with height. Enclosed ground flares (ZX-EGF Series) contain combustion at grade with a low-radiation, low-noise design and combustion efficiency up to 99.9%, which suits petrochemical parks, chemical plants, LNG terminals and industrial parks, but they occupy grade-level plot area and require refractory-lined enclosure maintenance.
2. What materials are appropriate for a flare tip operating at high temperature?
Zexuan's ZX-FT Series flare tips are available in SS316L, SS310S and Inconel 625, with operation up to 1100°C for hydrocarbon gases in refinery, petrochemical, LNG and oil & gas processing service. Selection follows temperature, corrosion resistance requirement and gas composition: SS316L is common where corrosion resistance matters, SS310S is specified for high-temperature sections, and Inconel 625 is reserved for sustained high-temperature parts where lower grades would not be suitable. Material is an explicit customisation variable, not a default.
3. How does a buyer verify flare system compliance before shipment?
Verification combines qualification documents and physical tests. On the qualification side, Zexuan holds ISO 9001:2015 (certificate 26326Q00079R001), ISO 14001:2015 (26326E00054R001) and ISO 45001:2018 (26326S00054R001), all issued by CSU International Certification Co., Ltd. on 2026-03-18 and valid to 2029-03-17, covering the development of waste gas treatment equipment and control units and the sales of waste gas and waste liquid treatment equipment. On the testing side, inspection includes incoming material inspection, welding inspection, dimensional inspection, pressure and leak testing where applicable, functional testing, Factory Acceptance Test, and final inspection before shipment, with 100% inspection. Acceptance is defined as FAT plus Site Acceptance Test (SAT).
4. Can skid-mounted flare systems handle LNG and LPG service?
Yes, within a defined capacity envelope. The ZX-SMF Series is designed for LNG, LPG, natural gas and hydrocarbon gas service, is compatible with cryogenic service, and uses carbon steel, SS304, SS316L and low-temperature materials for LNG duty. The configuration is intended for LNG receiving terminals, LNG bunkering, gas storage, pipeline facilities and offshore gas applications, with a compact skid-mounted design that supports fast installation and commissioning. Capacity is customised according to gas release rate, so the ceiling is set by the relief case and by transportable dimensions rather than by a fixed product limit.
5. What commercial and execution terms apply to customised flare systems?
Because systems are engineered to project requirements, the minimum order quantity is typically 1 complete system. Delivery terms are EXW, FOB or CIF; payment is available through T/T or L/C, with typical terms of 30% advance payment and 70% before shipment, negotiable according to project requirements. Typical production lead time is 60–120 days depending on project requirements, with monthly capacity of 5 sets for customised industrial systems and annual manufacturing capacity of 60+ sets of flare and thermal treatment systems. After-sales support covers remote support, commissioning assistance, spare parts and training.
For buyers compiling a tender package, Zexuan's corporate brochure is available for download here: Shandong Zexuan corporate brochure (PDF). Company and product information is also published at www.zexuaneco.com.
¿Tiene preguntas o necesita más detalles?
Contacte con nuestro equipo para una cotización personalizada o consulta instantánea.
Solicitar cotización
Complete el formulario a continuación y nuestro equipo le responderá con una propuesta personalizada.
Chat directo de WhatsApp
¿Prefiere chatear en tiempo real? Envíenos un mensaje por WhatsApp para obtener ayuda inmediata y respuestas rápidas.
- Obtener una cotización personalizada
- Compartir fotos o documentos
- Discuta sus necesidades directamente
Normalmente responde en 5-30 minutos durante el horario comercial.