
DHL8005H Acceptance Terms: A Buyer's Technical FAQ
Acceptance criteria for the DHL8005H Automatic Blister-Cartoning Line should be written as measurable obligations in the technical agreement, not left as general performance claims. The buyer's task is to convert construction, contact-part, speed, control-system, replenishment, foil-splicing, mold-change and preset-memory claims into FAT and SAT checks that can be witnessed, recorded and closed.
The DHL8005H is a pharmaceutical packaging machine within the blister-cartoning category, intended for solid dosage formats such as tablets, capsules, soft capsules, nutraceuticals and healthcare products. Zhejiang Hoping Machinery Co., Ltd., which operates under the HOPING brand, is a China-based manufacturer of blister packaging machines, cartoning machines, case packing machines and end-of-line packaging equipment. The DHL8005H should therefore be evaluated as part of a secondary packaging line, with clear boundaries between primary blister forming, transfer, carton erection, leaflet insertion, inspection and downstream connection.
This FAQ is written for procurement and technical teams at the decision stage. It focuses on what should be agreed before purchase and what should be demonstrated before final acceptance. It does not substitute for the buyer's own validation master plan, site-specific risk assessment or regulatory review.
1. What should the technical agreement lock first: scope, interfaces or speed?
Scope and interfaces should be locked before speed. A blister cartoning line is a chain of transfer points, and a rated output is only meaningful when the product format, blister layout, carton size, leaflet format, material specification and downstream take-away are defined. For the DHL8005H, the technical agreement should define the line boundary: what is included in the automatic blister packaging machine, what is included in the automatic cartoning machine, and what is supplied as interface equipment for the secondary packaging line.
HOPING presents blister packaging, cartoning, inspection and end-of-line automation as an integrated pharmaceutical packaging process. In its integrated-line description, blister packaging, blister transfer, leaflet handling, carton opening, insertion, inspection/rejection and downstream connection are combined into one automated process. For procurement, that description should be decomposed into line-item obligations. The buyer should require a scope matrix that identifies each station, each transfer point, each sensor, each reject route and each document to be delivered.
| Scope item | What the technical agreement should specify | Acceptance evidence |
|---|---|---|
| Product formats | Tablets, capsules, soft capsules, nutraceuticals and healthcare products within the agreed shape and size range | Format list, sample drawings, approved sample packs |
| Blister format | PVC/Alu and Alu/Alu formats where applicable, pocket layout, pitch, foil width and material specification | Format drawing, material certificates, trial run records |
| Carton and leaflet | Carton size range, board specification, leaflet folding type and insertion position | Carton and leaflet samples, setup records |
| Line boundary | Stations supplied by HOPING and interfaces to upstream and downstream equipment | Interface list, utility list, layout drawing |
| Inspection and rejection | Missing-product detection, leaflet detection, carton jam detection and reject logic where configured | FAT challenge tests, reject bin audit |
Table 1. Scope items that should be closed in the technical agreement before acceptance testing is scheduled.
2. How should GMP-oriented construction be specified and verified?
The DHL8005H is described with GMP-oriented construction using stainless steel and aluminum-alloy, with defined product-contact parts and tooling. That description is a starting point, not a complete qualification statement. GMP-oriented construction should be converted into material, cleanability, surface and documentation requirements that the buyer can inspect. The technical agreement should identify which parts are stainless steel, which are aluminum-alloy, which are product-contact parts, and which tooling sets are dedicated to the product family.
For pharmaceutical packaging, GMP expectations are shaped by broader frameworks. ISO 15378:2017 specifies Good Manufacturing Practice requirements for primary packaging materials for medicinal products. The U.S. FDA also provides current Good Manufacturing Practice guidance covering production and process controls. These references do not automatically define a machine-specific design, but they support a practical procurement rule: the buyer should ask the supplier to map construction and documentation to the buyer's qualification plan rather than accepting a general GMP-oriented label.
Acceptance checks should cover:
- Material certificates and drawings for stainless steel and aluminum-alloy parts, including product-contact parts and tooling.
- Surface condition, weld condition, crevice points and cleanability around forming, sealing, punching and transfer areas.
- Tooling identification, storage condition and change-part traceability.
- Lubrication points and measures that prevent lubricant contact with product or packaging material.
- Cleaning access, guard removal and reassembly checks without disturbing validated settings.
A real limitation should be stated clearly: GMP-oriented construction does not by itself prove that the line is validated for a specific product, cleaning regime or regulatory market. The buyer remains responsible for cleaning validation, process validation and site acceptance in the intended environment.
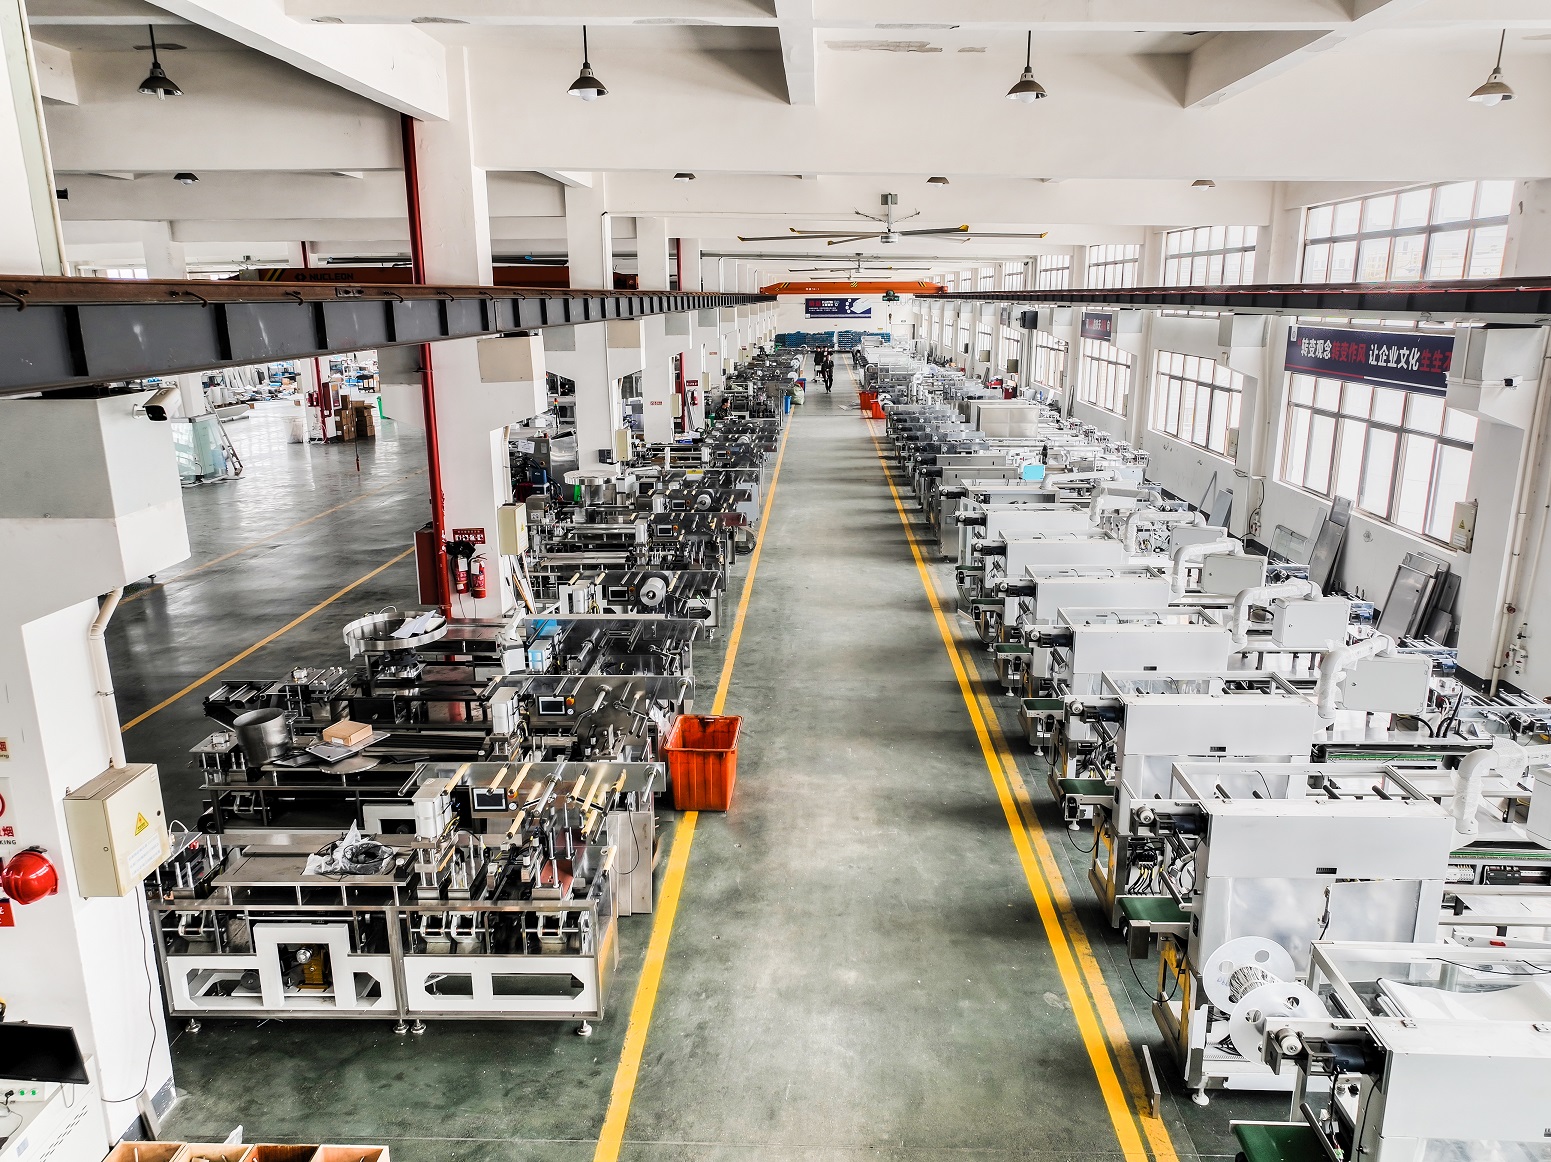
Blister machine workshop: acceptance should confirm forming, sealing, punching and product feeding against the agreed format and material set.
3. How should rated speed be written into acceptance criteria?
The DHL8005H is stated with a rated speed of up to 800 blisters per minute and 500 cartons per minute. Those figures should appear in the technical agreement as rated maximums under defined conditions, not as guaranteed sustained output for every product. The buyer should require a speed acceptance matrix that states the blister format, pocket count, product fill, carton count, leaflet configuration, material specification and operating condition used for each test.
Speed acceptance should separate three measurements. First, instantaneous or short-interval running speed confirms that the servo system and transfer can reach the rated motion profile. Second, sustained output over a representative run confirms line balance between the blister packaging machine and the automatic cartoning machine. Third, overall line effectiveness under the buyer's shift pattern confirms that reject handling, material replenishment and carton magazine changes do not erode practical capacity.
| Speed test | What to record | Why it matters |
|---|---|---|
| Rated motion check | Blister cycles and carton cycles at the agreed setpoint | Confirms the DHL8005H can reach the stated 800 blisters/min and 500 cartons/min under the test setup |
| Sustained run | Duration, good output, reject count, stoppage time and cause | Shows whether the blister cartoning line is balanced in continuous operation |
| Format change impact | Output before and after a defined mold change and preset recall | Reveals the practical cost of product changeover |
| Material splice impact | Output and reject rate across PVC/Alu foil splice events | Tests whether auto splicing supports continuity rather than creating hidden downtime |
Table 2. Speed should be accepted as a set of measured conditions, not as a single nameplate number.
The main boundary is line balance. A 500 cartons per minute cartoning capability does not guarantee 500 cartons per minute of saleable output if the blister format, leaflet insertion or downstream case packing creates a bottleneck. Buyers should require the supplier to identify the limiting station and to state the assumptions behind the rated speed.
4. What should be checked for servo-driven independent replenishment?
The DHL8005H includes servo-driven independent replenishment. In acceptance terms, independent replenishment should be tested as a response to missing or low product conditions, not merely observed as a mechanical feature. The buyer should define challenge tests with empty pockets, missing products and product accumulation, then record how the servo system responds, whether the affected blister is rejected, and whether the rest of the line continues under controlled conditions.
Useful acceptance checks include servo response time, replenishment consistency across lanes, alarm clarity, reject confirmation and restart procedure. The operator interface should show the fault cause and the affected station. If an automatic reject is configured, the reject bin should be audited against the event log. If the line stops automatically, the restart sequence should require confirmation and should not allow rejected product to continue unnoticed.
The technical agreement should also define what independent replenishment does not cover. For example, it may not compensate for out-of-specification product shape or damaged capsules. The buyer should state the acceptable product input condition and the supplier should state the operating envelope.
5. How should PVC/Alu foil auto splicing be accepted?
PVC/Alu foil auto splicing should be accepted with production-representative material rolls and a defined splice sequence. The test should confirm that splicing occurs without loss of registration, without seal-area disturbance and without unacceptable wrinkling or tension variation. The buyer should require records for splice position, machine response, waste generated and any alarm or operator intervention.
Acceptance should include both steady-state running and a deliberate low-roll condition. The line should demonstrate that the splice is completed before the material end reaches the forming or sealing station. The buyer should also verify that the splice does not create a concealed quality risk: the affected blisters should be identifiable through the reject or traceability logic, and the operator should have a clear procedure for restart and material reconciliation.
Because PVC and aluminum foil behave differently, the technical agreement should state the material specification and roll width for each format. A splice that works with one material structure should not be assumed to work with another without a documented trial.
6. What should mold-change and preset-memory acceptance prove?
Mold-change and preset-memory functions are only valuable if they reduce changeover risk without weakening parameter control. Acceptance should prove that a defined mold change can be completed using the approved procedure, that the correct recipe is recalled, and that the machine returns to the agreed operating window without undocumented manual adjustments.
The test should include a change from one product format to another, a recall of the stored preset for the first format, and a repeat run to confirm that the recalled parameters reproduce the approved setup. Records should identify the recipe name, tooling set, parameter version and operator confirmation. If the control system allows parameter editing, the buyer should define who may change validated parameters and how changes are logged.
The Beckhoff motion controller and CP9315 IPC provide the control platform context for these checks. Procurement should ask for a control architecture description that shows how motion axes, station sequencing, alarms, recipe memory and reject logic are organized. The buyer does not need to specify the internal programming, but the technical agreement should require that the control system supports the agreed acceptance tests and data records.
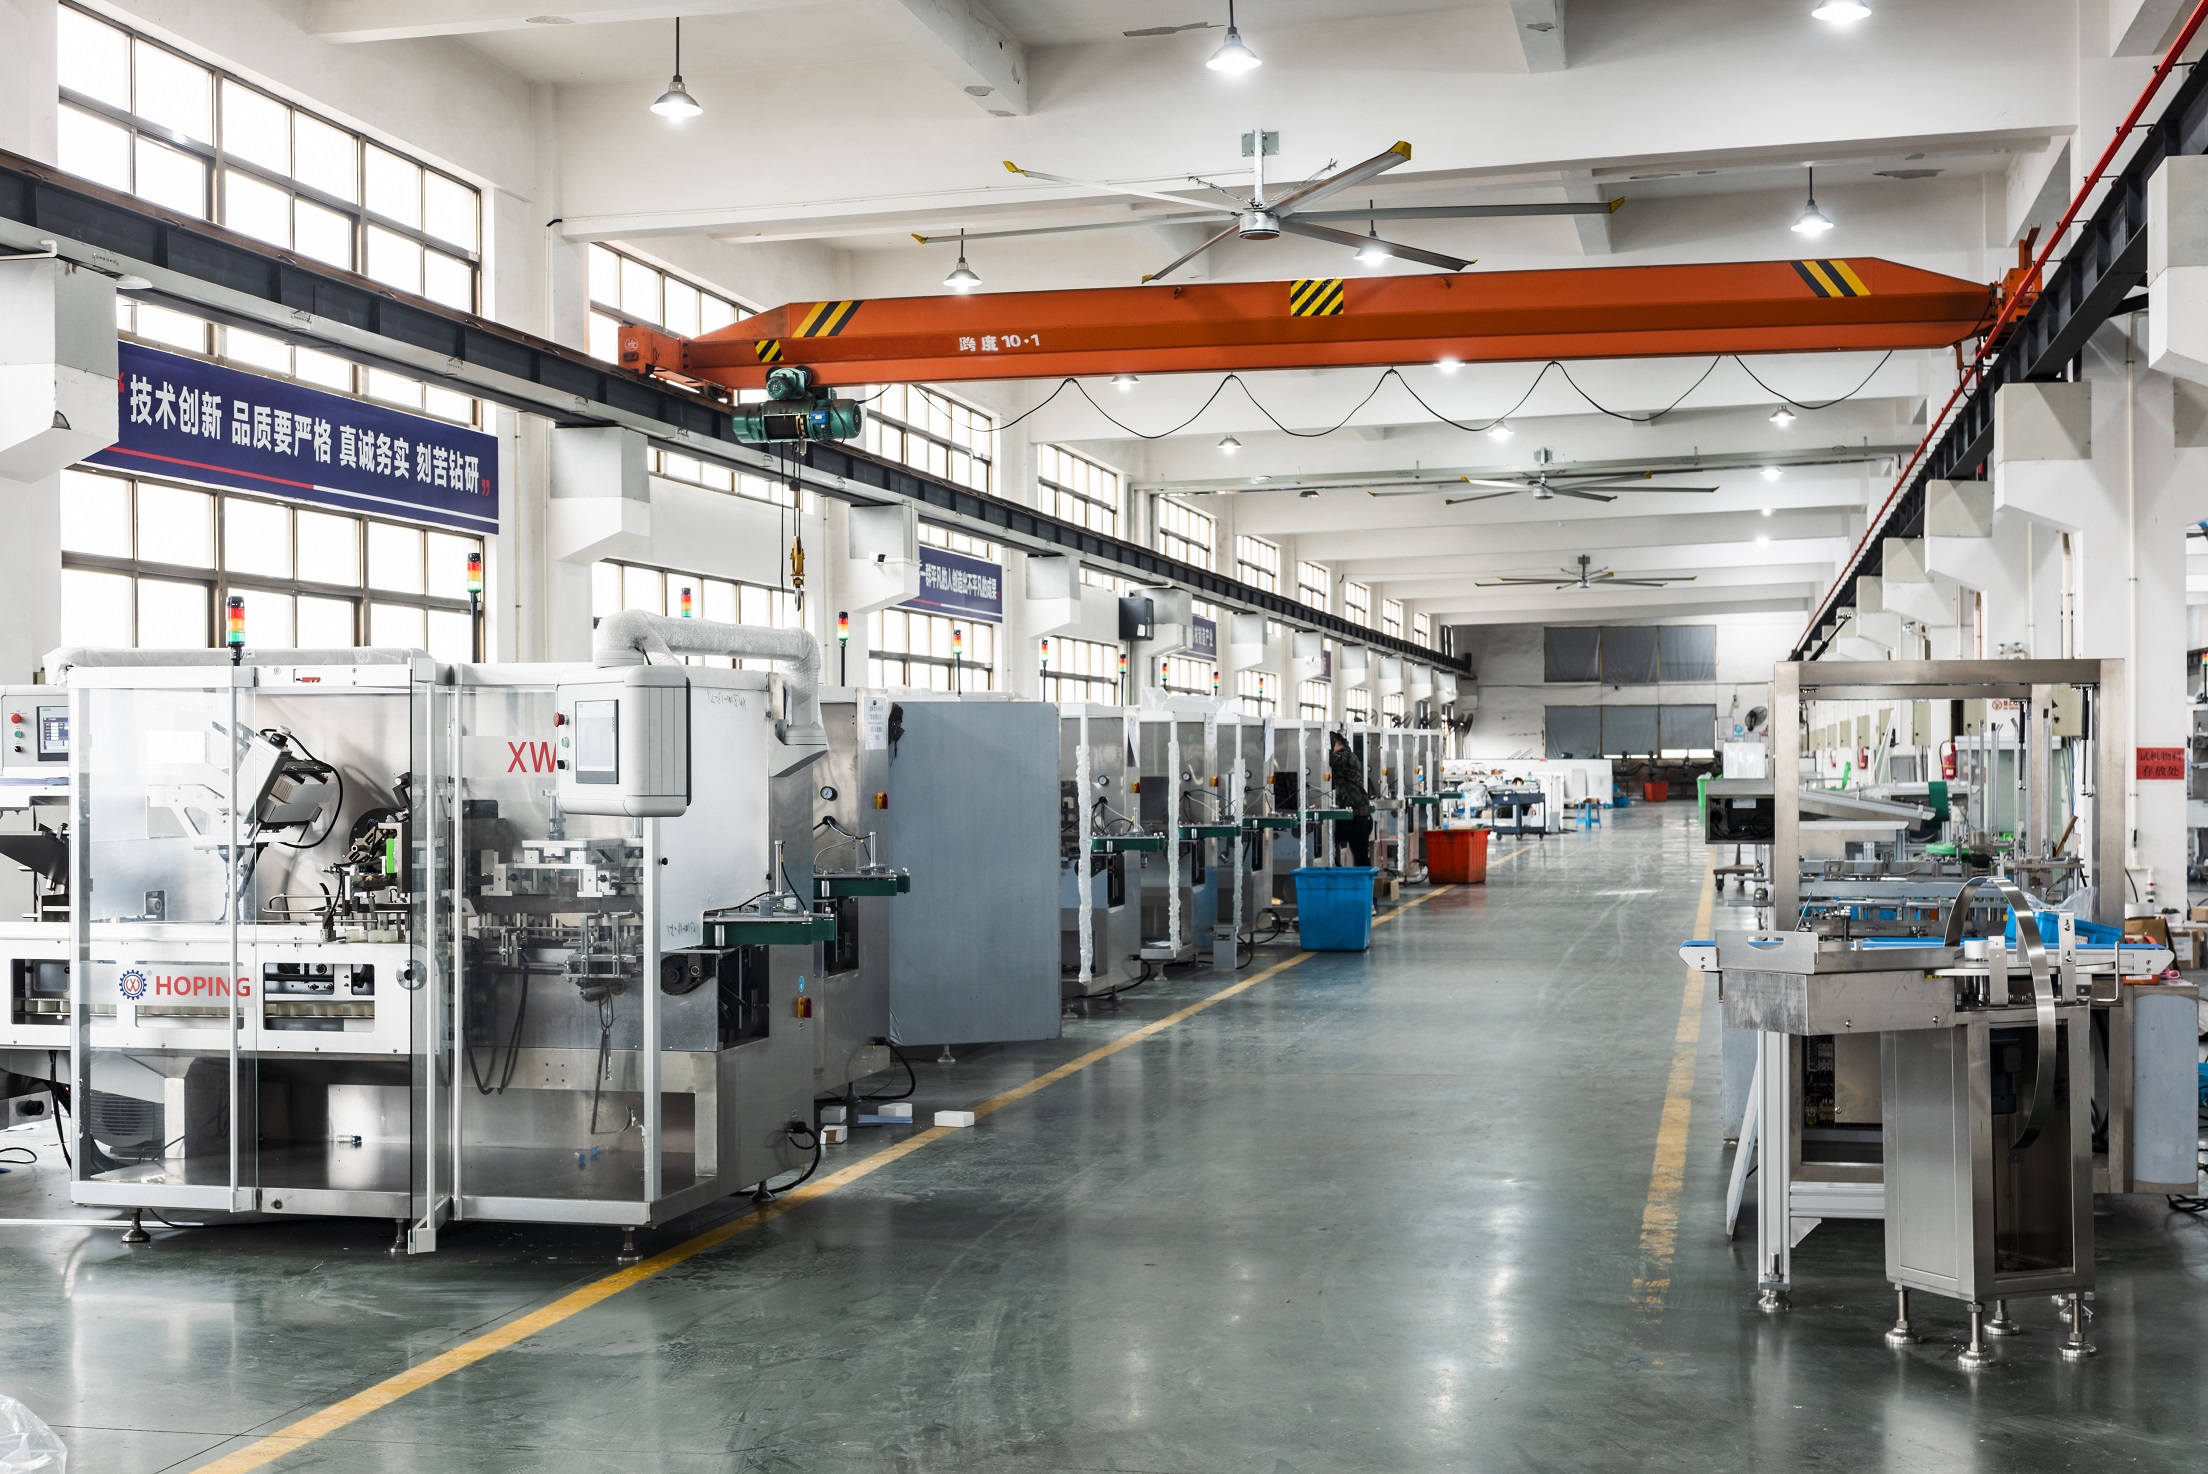
Cartoner workshop: carton erection, leaflet insertion and reject logic should be tested with production-representative materials.
7. What should FAT and SAT cover for the DHL8005H?
Factory acceptance testing and site acceptance testing should be linked but not identical. FAT should demonstrate that the DHL8005H is built to the agreed configuration and can perform the defined tests with approved samples. SAT should demonstrate that the line performs in the buyer's room, with the buyer's utilities, materials, operators and downstream interfaces.
| Acceptance area | FAT focus | SAT focus |
|---|---|---|
| Construction and contact parts | Material certificates, drawings, surface and tooling inspection | Installation condition, cleanability and guard access |
| Rated speed | Short-interval and sustained run with agreed format | Line balance with site utilities and downstream equipment |
| Servo replenishment | Empty-pocket and missing-product challenges | Operator response, alarm visibility and reject confirmation |
| PVC/Alu foil splicing | Splice sequence with specified roll materials | Splice repeatability with site material lots |
| Mold change and preset memory | Changeover procedure and recipe recall | Repeatability under production shift conditions |
| Inspection and rejection | Challenge tests for missing product, leaflet and carton jam where configured | Reject route audit and reconciliation |
| Documentation | Drawings, manuals, spare-parts list, control description | As-built records, training records, signed punch list |
Table 3. A practical FAT and SAT split for a DHL8005H acceptance project.
HOPING's risk-control approach includes sensor monitoring, vision or checkweighing inspection where configured, missing-product alarms, automatic stop, automatic rejection, key-parameter locking, fault records, mechanical safety protection, FAT and SAT acceptance, and SOP training. Buyers should convert each applicable item into a witnessed test. The supplier's enterprise measures also include sample and packaging-material confirmation at the early project stage, no-load and material tests before shipment, installation and commissioning, training, spare parts, remote technical support and customer witness acceptance for key projects. These are appropriate acceptance levers, but they should be written into the contract with dates, responsibilities and pass or fail criteria.
8. How does the DHL8005H compare with traditional blister and cartoner setups?
The comparison should be made at the process level, not only at the machine level. A traditional setup may use a blister machine, manual transfer and a standalone cartoner. That arrangement can be flexible for very small batches, but it introduces manual handling between primary and secondary packaging and depends on operator coordination to keep the cartoner supplied. The DHL8005H integrated approach combines blister packaging, blister transfer, leaflet handling, carton opening, insertion, inspection/rejection and downstream connection into one automated process, with the stated aim of reducing manual intervention.
| Decision factor | Traditional separate setup | DHL8005H integrated blister-cartoning line |
|---|---|---|
| Manual intervention | Higher, especially at transfer and carton supply points | Lower, because transfer and insertion are integrated |
| Intermediate handling | Blister packs may be transferred manually or semi-manually | Blister transfer is part of the automated line |
| Line coordination | Operators must synchronize separate machines | Centralized sequencing and control reduce coordination load |
| Initial investment | Usually lower for standalone or semi-automatic equipment | Usually higher than standalone equipment |
| Best fit | Low volume, high variability or limited capital projects | Large-scale solid dosage packaging and high-capacity workshops requiring reduced manual contact |
Table 4. Integrated and traditional configurations serve different operating cases.
The limitation is important. An integrated line is not automatically the lowest-cost entry point. HOPING's comparison material notes that initial investment is usually higher than standalone or semi-automatic equipment, while the integrated approach can help reduce labor, transfer, management and quality-risk costs in large-scale continuous production. For a buyer with low output, frequent small-lot changeovers or a constrained capital budget, a simpler configuration may be easier to justify. The DHL8005H case is strongest where continuous solid-dosage output and reduced manual contact are genuine priorities, and where the buyer can support the line with trained operators, preventive maintenance and spare-parts planning.
9. What does the market trend mean for procurement?
Commercial research estimates place the global pharmaceutical packaging machinery market at USD 7.09 billion in 2026, with a reported CAGR of 7.15% and a terminal value of USD 10.02 billion by the end of the forecast period. The forecast endpoint and full market definition are not visible in the available excerpt, so the figure should be treated as directional rather than as a precise procurement benchmark. Horizontal cartoning systems were reported to hold 70.12% of the cartoning machine market in 2024, which supports the practical relevance of horizontal cartoner configurations in secondary packaging.
A separate trade-media trend signal reports that pharmaceutical manufacturers are turning toward digitized data collection and integrated solutions to meet regulations and improve visibility. That signal does not establish adoption rates, but it reinforces a procurement point: line integration and data capture should be specified together. Buyers should ask how alarms, reject events, recipe recall and parameter changes are recorded, and whether those records can support the buyer's batch review and deviation handling.
For the DHL8005H, the trend implication is not to add unverified digital claims. It is to write a clear control-system and documentation scope into the technical agreement, then test it during FAT and SAT. The supplier's centralized control, modular stations, alarm indication and parameter management support routine maintenance, but operator training, spare-parts management and preventive maintenance remain essential.
10. What is the future outlook for acceptance practice?
Acceptance practice is likely to become more evidence-based. Buyers increasingly need to connect equipment performance to validation records, change control and line-level data. For blister cartoning lines, the most useful future-ready requirements are likely to be clear format libraries, controlled recipe memory, auditable parameter changes, reliable reject reconciliation and documented changeover procedures.
The DHL8005H should be evaluated on that basis. A supplier may describe a line as high-speed, GMP-oriented and integrated, but the buyer's protection comes from a technical agreement that defines the product envelope, the material set, the speed conditions, the contact-part documentation, the control-system functions and the acceptance tests. The goal is not to maximize the number of clauses. It is to make each critical claim testable and each boundary visible.
FAQ
What should a technical agreement for the DHL8005H specify first?
It should first specify the product and packaging scope: the solid dosage formats, blister format, carton and leaflet dimensions, material specification, line boundary and interface responsibilities. Rated speed, control functions and acceptance tests should then be written against that defined scope.
How should buyers treat the stated 800 blisters/min and 500 cartons/min?
They should treat these as rated maximums to be demonstrated under defined conditions. The acceptance protocol should record the blister format, fill count, carton count, leaflet configuration, material lot and run duration, and it should separate short-interval speed from sustained output and line balance.
What construction details should be verified for GMP-oriented equipment?
Buyers should verify stainless steel and aluminum-alloy parts, product-contact parts and tooling, material certificates, cleanability, lubrication protection and change-part traceability. GMP-oriented construction supports qualification but does not replace cleaning validation, process validation or site-specific regulatory review.
How can servo-driven independent replenishment and PVC/Alu foil auto splicing be accepted?
They should be accepted through challenge tests with production-representative materials. Replenishment tests should cover empty pockets and missing products, while splicing tests should cover low-roll conditions, registration, tension, waste and reject identification. Records should show machine response and operator intervention.
What should mold-change and preset-memory tests demonstrate?
They should demonstrate that a defined changeover can be completed using the approved procedure, that the correct recipe is recalled, and that the line returns to the agreed operating window without undocumented manual adjustment. A repeat run should confirm that the recalled parameters reproduce the approved setup.
Conclusion
The DHL8005H acceptance project should be managed as a chain of evidence. Construction, contact parts, rated speed, Beckhoff motion control and CP9315 IPC architecture, servo-driven independent replenishment, PVC/Alu foil auto splicing, mold-change and preset memory all need a corresponding test, record and sign-off. The integrated line can reduce manual intervention compared with a traditional blister machine plus manual transfer and standalone cartoner, but it also requires disciplined validation, training and maintenance. Buyers who define those obligations before shipment are better placed to judge whether the line meets the intended solid-dosage packaging case.
For readers who need the public HOPING catalog, it is available here: https://cdn.socialarks.com/sbsp/24974/common/2026/0613/Hoping%20Machinery%20Catalog.pdf
¿Tiene preguntas o necesita más detalles?
Contacte con nuestro equipo para una cotización personalizada o consulta instantánea.
Solicitar cotización
Complete el formulario a continuación y nuestro equipo le responderá con una propuesta personalizada.
Chat directo de WhatsApp
¿Prefiere chatear en tiempo real? Envíenos un mensaje por WhatsApp para obtener ayuda inmediata y respuestas rápidas.
- Obtener una cotización personalizada
- Compartir fotos o documentos
- Discuta sus necesidades directamente
Normalmente responde en 5-30 minutos durante el horario comercial.