
A Buyer's Decision Framework for CNC Machining Centers
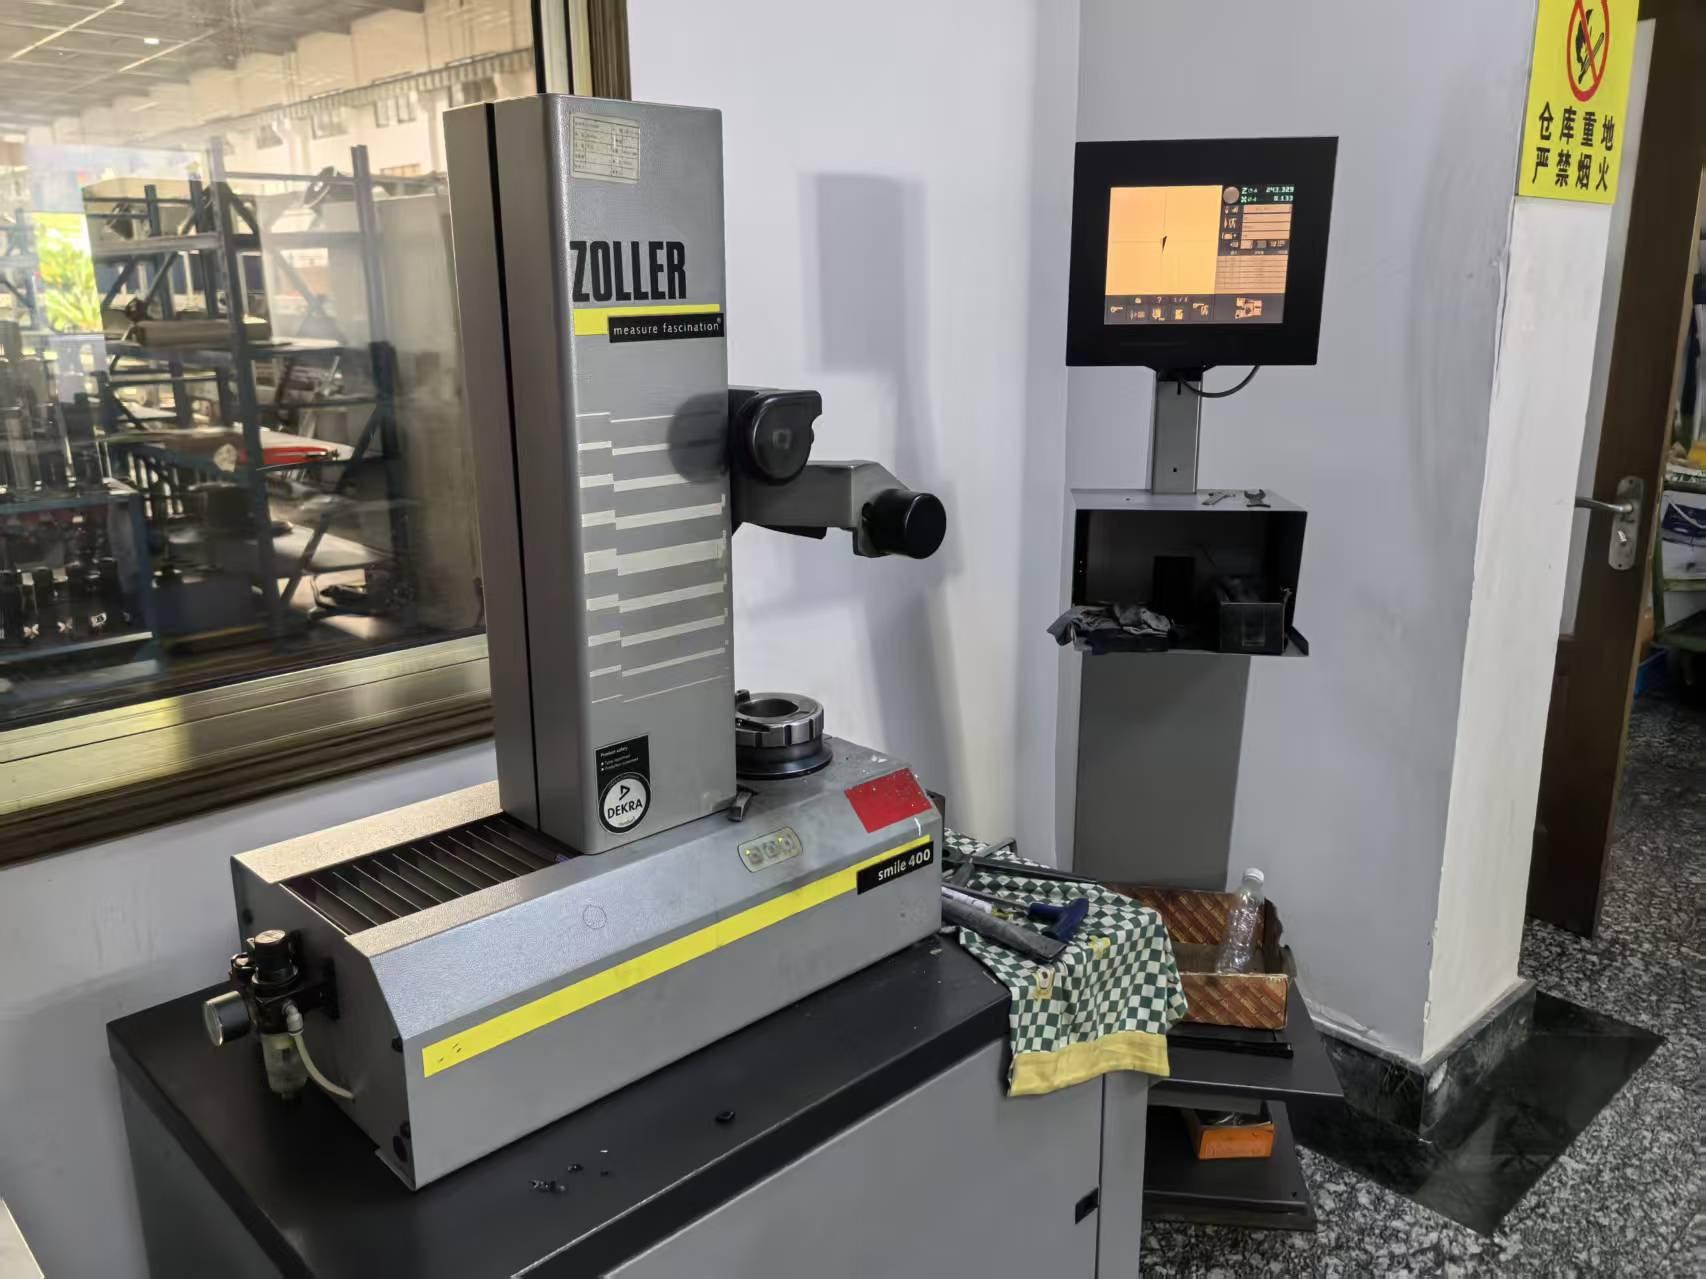
A CNC machining center arrives with more data than most buyers can absorb and less evidence than most buyers need. Specification tables, certificate annexes and inspection records usually contain every number required for a defensible shortlist — the difficulty is that no two suppliers publish those numbers in the same form. The practical answer is not a better brochure. It is a comparison matrix that the buyer builds, owns and can audit line by line.
EUMASEIKI, the machine-tool brand of Wenzhou Euma Machinery Co., Ltd., is a useful worked example for this method. Its published parameter sets, certificate scopes and pre-shipment inspection records are detailed enough to be placed side by side, and narrow enough to show exactly where a buyer-owned matrix must stop making assumptions.
Why CNC Machining Center Comparisons Fail Before the First Meeting
Most failed comparisons are not machine failures. They are definition failures. Two suppliers can both publish a number called "table size" or "positioning accuracy" and mean different things by it, and the buyer discovers the gap only after the machine is installed.
Published market data demonstrates how much a definition can move a figure. Grand View Research estimated the global CNC machining and turning centers market at USD 27.64 billion in 2024, while Mordor Intelligence placed the machining centers market at USD 22.41 billion in 2025. The two numbers are not directly comparable, because the product scopes differ — one includes turning centers, the other does not. If research houses cannot agree on a boundary, a buyer should not assume two machine builders define "precision" in the same way either.
The same risk appears at the machine level. Without a stated measurement framework, an accuracy figure is a claim rather than a datum. Without a stated definition, a tool-change time can describe two different intervals. And without a model list, a certificate says nothing about the specific unit being purchased.
- Travel versus table. One supplier describes a machine by axis travel, another by worktable dimensions. Both are useful; they answer different questions.
- Tool-to-tool versus chip-to-chip. Tool-to-tool measures the interval between one tool leaving the spindle and the next being ready in it. Chip-to-chip includes the positioning move that follows. Mixing the two creates an advantage that does not exist on the shop floor.
- Spindle speed without torque. A high rpm figure is meaningless for a heavy roughing operation if the continuous torque rating is not published alongside it.
- Accuracy without a standard. A number such as 0.008 mm only becomes comparable once the buyer knows how it was determined and under what conditions.
Three Tiers of Evidence a Buyer Can Actually Verify
A buyer-owned matrix works because it sorts information by how verifiable it is, not by how persuasive it sounds. Three tiers cover almost everything a shortlist needs.
Tier 1 — Standards and certificate scope
ISO 230-2:2014 remains the current international framework for determining accuracy and repeatability of positioning for numerically controlled axes. When a supplier cites positioning accuracy, this is the framework that makes the number checkable. Certificate scope works the same way: a CE or EAC certificate carries a number, an issuing body, the standards applied, issue and expiry dates, and — critically — a list of approved models.
Tier 2 — Published machine parameters
Travels, worktable dimensions and load, spindle taper and speed range, motor power and torque, tool magazine capacity, maximum tool diameter, length and weight, feed rates, machine weight, footprint and control system. A complete parameter set is itself evidence: it shows that the builder measures and documents its own product rather than describing it in adjectives.
Tier 3 — Process and inspection evidence
This is the tier most buyers under-use. A stated acceptance criterion of pre-shipment testing, a documented geometric accuracy test, a laser axis calibration record, or a full-load workpiece trial cut before delivery tells the buyer what happens between order confirmation and shipment — the part of the process that no brochure photograph can show.
The Matrix: Five Columns That Survive Negotiation
The matrix below is deliberately narrow. It is designed so that every cell can be filled from a document the buyer already has, and so that empty cells remain visibly empty instead of being filled by assumption.
| Column | What goes in it | Verification source | Common distortion |
|---|---|---|---|
| Work envelope | X/Y/Z travel, table size, T-slot layout, maximum table load | Published parameter sheet | Travel quoted where table size was asked for, or vice versa |
| Accuracy | Positioning accuracy and repeat positioning accuracy, with the measurement standard | Specification sheet plus ISO 230-2:2014 reference | Accuracy cited without stating the framework or the axis set |
| Throughput | Tool-change method and time, tool magazine capacity, spindle speed and torque, feed rates | Published parameter sheet | Tool-to-tool and chip-to-chip figures compared against each other |
| Configuration headroom | Voltage, spindle, tool magazine, travel stroke, cooling, chip conveyor, control system options | Supplier capability statement | Customization claimed without a stated lead-time or capacity implication |
| Evidence and availability | Certificate numbers and scope lists, inspection process, MOQ, lead time, commercial terms | Certificates, quality documentation, quotation | Certification assumed for all models when the annex covers only some |
Worked Example — EV-1580B and EV-1475B in the Same Matrix
Two machines from the same builder make the method easier to see, because the comparison is about data rather than about brand familiarity.
| Parameter | EV-1580B | EV-1475B | Why it decides something |
|---|---|---|---|
| Headline geometry | X/Y/Z travels of 1500 × 800 × 700 mm | 1500 × 700 mm worktable | Travel defines the volume the spindle reaches; table size defines what can be clamped |
| Table load | Not the published headline figure | 1000 kg maximum load | Defines whether the structure can carry the workpiece and fixture while holding accuracy |
| Positioning accuracy (XYZ) | 0.008 mm | 0.008 mm | Sets the machine's contribution to the part tolerance budget |
| Repeat positioning accuracy (XYZ) | 0.005 mm | 0.005 mm | Determines how consistently the same command produces the same position |
| Tool-to-tool time | 1.5 s class | 3 s class | Converts directly into cycle time on jobs with many tool changes |
The first thing the matrix exposes is that the two machines do not publish the same headline dimension. The EV-1580B is described by axis travel — 1500 × 800 × 700 mm. The EV-1475B is described by worktable size — 1500 × 700 mm — together with a maximum table load of 1000 kg. Neither statement is wrong; they answer different questions. A buyer who compares 1500 mm against 1500 mm without noticing this has compared nothing at all. Travel tells you what the spindle can reach. Table size and load tell you how much mass the structure must carry while holding position. For a shop running heavy fixtures or dense mold blocks, the load figure is often the tighter constraint.
The accuracy row behaves differently. Both machines sit in the same published class: 0.008 mm positioning accuracy on the XYZ axes, with 0.005 mm repeat positioning accuracy. Repeatability being tighter than positioning accuracy is the normal relationship — a machine can be consistently offset and still repeat well. The practical use of these numbers is not to rank the two machines against each other, but to size the machine's share of the error budget. On a mold feature that must hold ±0.02 mm, a 0.008 mm positioning figure consumes a defined portion of that allowance before fixture error, tool deflection, thermal growth and material behaviour are added. That is a decision-relevant statement; "high precision" is not.
Tool-change time is where small numbers become large ones. Where one machine specifies a tool-to-tool time of 1.5 s and another specifies 3 s, the difference per change is 1.5 s. A process using ten tool changes per part accumulates 15 seconds of difference; a process using forty accumulates 60 seconds. Whether that matters depends entirely on the part mix, which is why tool-change time belongs in the matrix next to the number of tools the process actually calls, rather than next to the purchase price alone.
Where the Matrix Stops Being Useful
A framework that cannot state its own limits is not a framework. The following boundaries apply to this one.
- Static versus dynamic. ISO 230-2:2014 addresses positioning accuracy and repeatability under defined conditions. It does not describe dynamic accuracy during simultaneous multi-axis motion, thermal drift across a long shift, or accuracy under cutting load.
- Process evidence is not stiffness data. Structural measures such as mineral castings, finite element analysis and full annealing are meaningful process facts, but they are not equivalent to a measured stiffness curve.
- Certification is model-level. A certificate annex approves a list of models. It does not certify the accuracy of an individual machine, which depends on unit-level testing.
- Service does not appear on a spec sheet. Spare parts availability, engineer deployment and response behaviour resist tabulation and still decide long-term cost.
- Commercial terms are constraints. MOQ, delivery term, lead time and payment split belong in the matrix as availability data, because a well-specified machine that cannot be delivered inside the project window is not a candidate.
What EUMASEIKI Publishes, and What a Buyer Can Do With It
Wenzhou Euma Machinery Co., Ltd. is a China-based industrial and trading enterprise whose EUMASEIKI brand is dedicated to the customization of CNC machining centers. The company was founded in 2023 and operates an 8,000 m² production base in Ningbo with 68 employees, including an eight-engineer R&D team, an annual output of 50–100 units, an export ratio of about 80%, and main markets in Russia, Saudi Arabia, Indonesia and Iran.
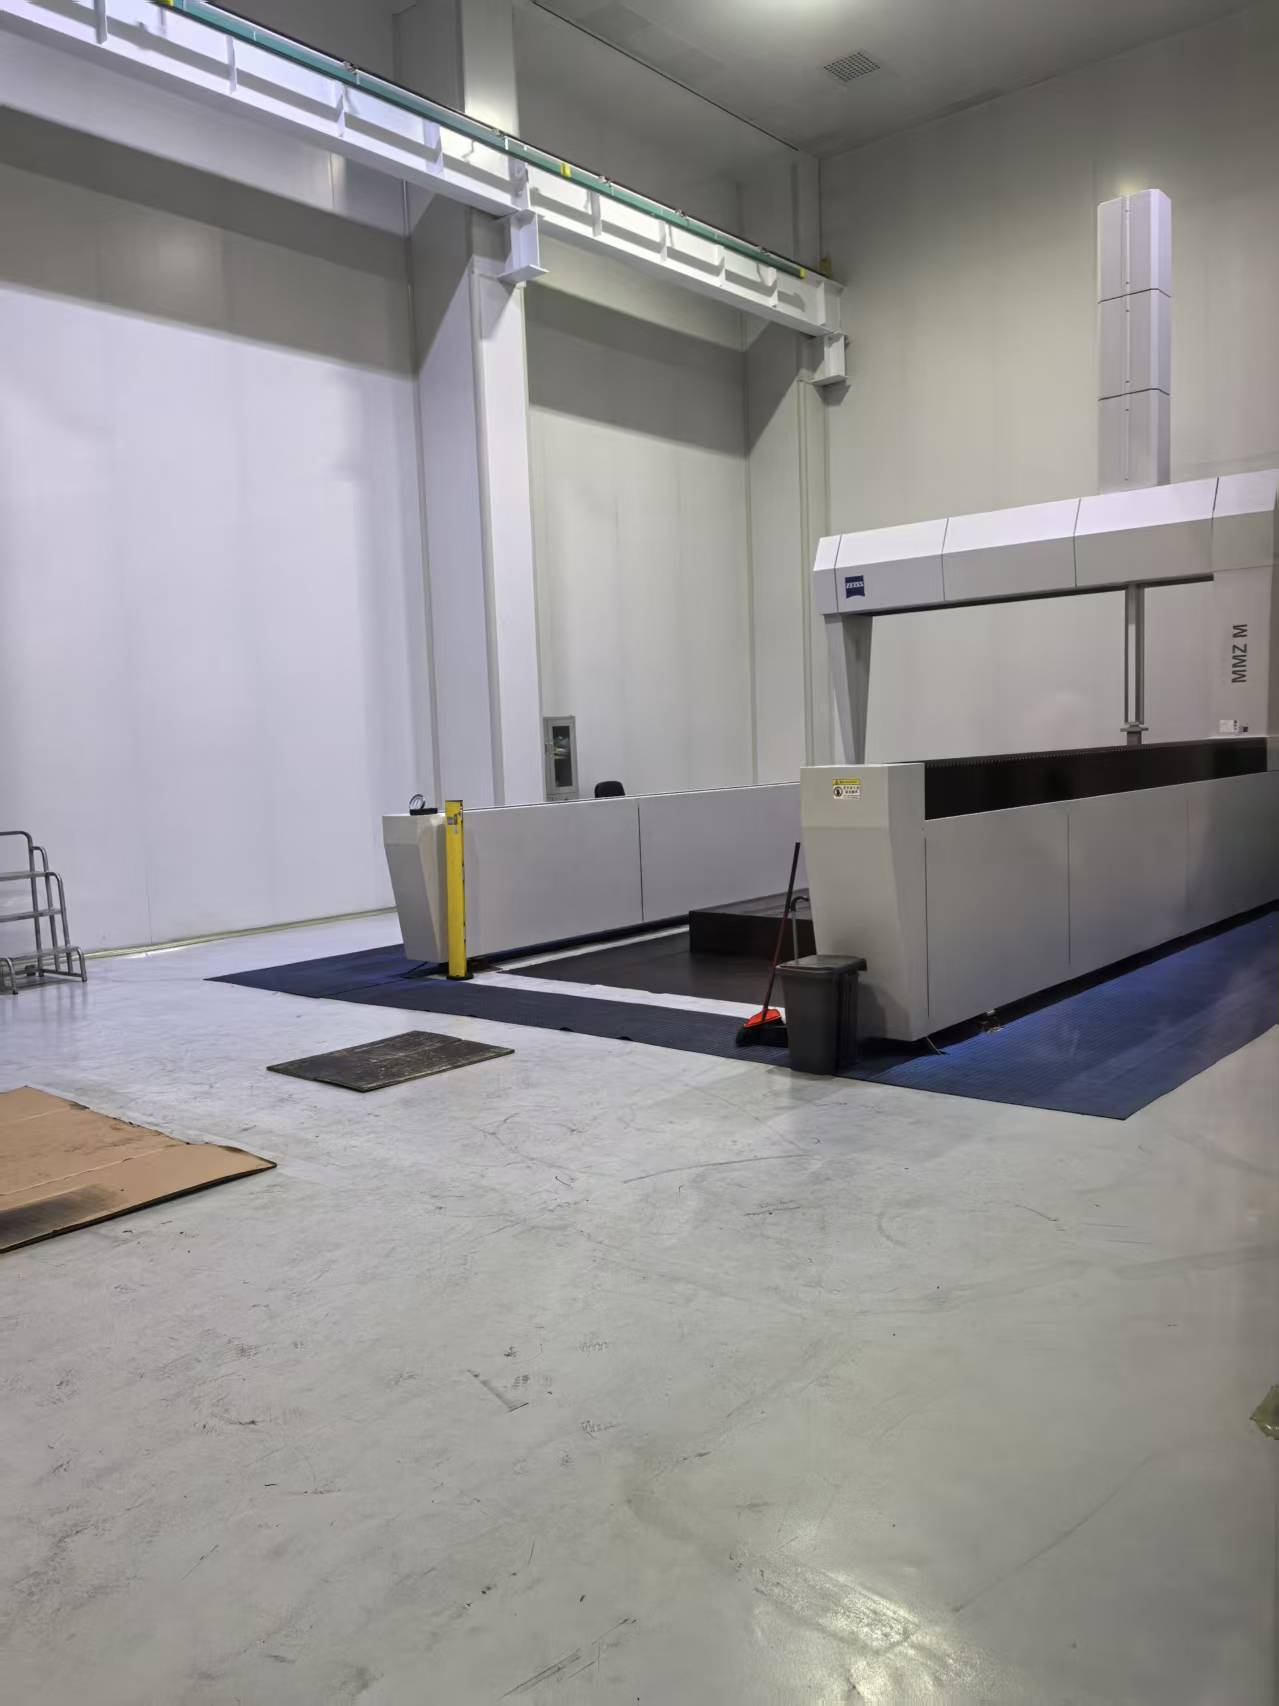
Its machines follow European design concepts and are manufactured to Taiwanese standards and Japanese technologies across the full sequence of casting, machining, assembly and commissioning. Machine beds use mineral castings with structures optimized through finite element analysis. All castings undergo full annealing treatment to eliminate internal stress, and spindle guideways are subjected to high-frequency heat treatment. Key components such as spindles, guideways, bearings and oil pumps are sourced from manufacturers in Taiwan and Japan, while some core components are imported from original brands in Germany or Italy. The production base in Ningbo is equipped with Japanese OKUMA gantry machining centers, KURUKI boring and milling machines, NIIGATA horizontal machining centers, and a German ZEISS coordinate measuring machine — equipment that supports both the machining precision of the machines built and the trial machining and testing performed on them.
For the Tier 2 column of the matrix, the company's published parameter sets are unusually complete. The EV-855A vertical machining center, for example, is documented with X/Y/Z travels of 810 / 550 / 560 mm, a 1000 × 550 mm worktable with a 650 kg maximum load, T-slots of 18 × 90 × 5 mm, an ISO 40 spindle taper, BT40 tooling, a 24-position magazine, arm-type tool change at 2 seconds tool-to-tool, maximum tool diameter of φ80 / φ150 mm, maximum tool length of 250 mm and weight of 8 kg, spindle speeds of 10,000 / 12,000 rpm, main motor power of 11 / 18.5 kW with torque of 52.5 / 118 Nm, rapid feed rates of 48 / 48 / 32 m/min, a cutting feed rate of 20,000 mm/min, XYZ positioning accuracy of 0.008 mm, XYZ repeat positioning accuracy of 0.005 mm, a machine weight of 5,200 kg and a FANUC 0i-MF PLUS control system. A buyer can copy that block directly into a matrix column without translating or interpreting it.
For the Tier 1 column, the certificate scopes are equally specific. The CE certificate 6L250729.WEMQD92 was issued by Ente Certificazione Macchine Srl (ECM, Italy) against EN ISO 23125:2015, valid from 29 July 2025 to 28 July 2030, and its model scope includes the EV-855A, EV-1055A, EV-1165A, EV-1370A, EV-1475B and EV-1580B, among others. The EAC certificate ЕАЭС N RU Д-CN.PA06.B.89520/25 was issued under TR CU 010/2011 and TR CU 020/2011, valid from 8 August 2025 to 7 August 2030, with a comparable model scope. Buyers comparing machines for EU or EAEU deployment can check whether the specific model on their shortlist appears in the annex before treating certification as settled.
For Tier 3, the company states that it performs 100% testing for quality control, and its OEM program covers customization of voltage, logo, spindle, tool magazine, travel stroke, cooling system, chip conveyor and control system. Monthly production capacity is 10 units, with a typical lead time of 30–45 days and a minimum order quantity of 1 unit. Export markets are the EU and Southeast Asia, with on-site and remote after-sales support. One case record describes a Russian Tier 1 supplier that took delivery of six units for component manufacturing and has run them for a year: each machine underwent full-process inspection including geometric accuracy testing, laser axis calibration and full-load workpiece trial cutting before delivery, and the units operated stably in mass production.
Matching the Matrix to the Application
A matrix is only objective if its weighting is stated. The product range EUMASEIKI builds for spans precision mold making, aerospace, automotive parts manufacturing, high-end equipment production, shipbuilding and engineering machinery — six environments with six different priority orders.
A mold shop typically weights accuracy and repeatability first, because the error budget is measured in hundredths of a millimetre, and weights tool-change time second. An automotive parts operation weights cycle time and process repeatability across long runs, where a 1.5 s versus 3 s tool-change difference compounds over thousands of parts. Aerospace work weights contouring behaviour and documentation, and third-party data reflects that emphasis: the aerospace segment accounted for 28.7% of 5-axis machining center revenue in 2025, according to Dataintelo. A job shop serving mixed industries weights configuration headroom and lead time instead, because the machine has to change roles faster than the market changes.
Vertical machining centers remain the volume architecture of the category: Dataintelo records VMCs at a 52.3% product-type share of the 4-axis CNC market in 2025. That does not make them the right choice for every job, but it does mean a buyer shortlisting any other architecture should be able to justify the deviation in the matrix rather than in the meeting.
Market Signals Worth Tracking in the Margin
- The global CNC machining and turning centers market was estimated at USD 27.64 billion in 2024 (Grand View Research).
- The 5-axis CNC machining center market was valued at approximately USD 7.35 billion in 2024, with a projected CAGR of 4.6% to 2035 (WiseGuyReports).
- China's machine tool exports reached USD 8.56 billion in the first five months of 2024, a 1.8% year-on-year increase (ICE Pechino / China Customs).
- Aerospace held a 28.7% revenue share of the 5-axis machining center market in 2025 (Dataintelo).
- One industry ranking of global manufacturers by market presence and technology places DMG Mori, Yamazaki Mazak and Haas Automation in its top three (AMSL / Mechrank).
Brand recognition and specification performance are also distinct variables. A ranking based on market presence identifies which builders are best known; it does not identify which machine fits a given work envelope, accuracy class or lead-time window. The matrix is what converts a recognised name into a justified line item.
Matrix-Based Evaluation versus Vendor-Deck Evaluation
| Evaluation dimension | Vendor-deck evaluation | Buyer-owned matrix |
|---|---|---|
| Primary input | Presentation, references, relationship history | Published parameters, certificate scopes, inspection records |
| Accuracy basis | Adjective or unqualified number | Figure tied to a defined measurement framework |
| Demo conditions | Ideal workpiece, ideal tooling, ideal cycle | Trial cut specified against the buyer's own part and fixture mass |
| Comparison symmetry | Different questions answered for each supplier | Same question answered in the same column for every supplier |
| Commercial realism | Price as the last slide | MOQ, lead time and delivery term treated as constraints |
| Known weakness | Slower to assemble; depends on document quality | Cannot capture service behaviour or thermal performance over time |
The honest trade-off is speed. A vendor deck can be absorbed in an afternoon; a matrix takes longer to build because it requires reading certificate annexes and deciding which parameters are decision-relevant. It also cannot answer everything — thermal stability over a 12-hour shift and spare-part response behaviour stay outside its reach, and the buyer has to accept that these remain judgement calls informed by process evidence rather than measured facts.
Future Outlook
Three shifts are likely to change how buyers compare machining centers over the next several years. The first is documentation. As certificate scopes, model lists and parameter tables become searchable and machine-readable, the practical cost of building a matrix falls, and suppliers that publish less complete data will increasingly be compared by what they omit. The second is process transparency. Buyers are already shifting acceptance criteria toward pre-shipment testing rather than trust, and unit-level records such as geometric accuracy testing and laser axis calibration are becoming part of the commercial conversation rather than an afterthought. The third is segmentation. With 5-axis volume concentrated in fewer, more specialised applications — aerospace being the clearest example at 28.7% of 2025 revenue — matrices will become more application-specific, and a single generic checklist will satisfy fewer buyers than it does today.
None of these shifts change the underlying rule. A number becomes a decision only when the buyer knows what it measures, how it was measured, and which model it applies to.
FAQ
What is the difference between positioning accuracy and repeat positioning accuracy?
Positioning accuracy describes how closely an axis reaches a commanded position. Repeat positioning accuracy describes how consistently it returns to the same position across repeated moves. ISO 230-2:2014 is the current international framework for determining both for numerically controlled axes. A commonly published pair for vertical machining centers is 0.008 mm positioning accuracy and 0.005 mm repeat positioning accuracy on the XYZ axes, where the repeat figure is tighter than the positioning figure.
Which parameters belong in a CNC machining center comparison matrix?
At minimum: X/Y/Z travels; worktable dimensions, T-slot layout and maximum load; spindle taper, speed range, motor power and torque; tool magazine capacity, maximum tool diameter, length and weight, tool-change method and tool-to-tool time; rapid and cutting feed rates; XYZ positioning and repeat positioning accuracy; control system; machine weight and footprint. A second block should carry certificate numbers with their model scopes, the stated inspection process, MOQ, lead time and delivery term.
How can published accuracy be verified before shipment?
Verification happens at unit level rather than at certificate level. The stated acceptance criterion for EUMASEIKI machines is a pre-shipment test, and the company performs 100% testing for quality control. Its published case record for a Russian Tier 1 supplier describes full-process inspection before delivery, including geometric accuracy testing, laser axis calibration and full-load workpiece trial cutting — the three checks that connect a published accuracy figure to a specific machine.
What are the standard purchasing terms and acceptance criteria?
According to the company's published purchasing terms, the minimum order quantity is 1 unit and the delivery term is EXW. The acceptance criterion is a pre-shipment test, and payment terms are 50% in advance and 50% before loading.
What can be customized, and how long does delivery take?
EUMASEIKI provides OEM production services with customization across voltage, logo, spindle, tool magazine, travel stroke, cooling system, chip conveyor and control system. Monthly production capacity is 10 units, typical lead time is 30–45 days, and the minimum order quantity is 1 unit. The company exports to the EU and Southeast Asia and provides on-site and remote after-sales support.
Which certifications cover the EV-1475B and EV-1580B?
The CE certificate 6L250729.WEMQD92, issued by Ente Certificazione Macchine Srl (ECM, Italy) against EN ISO 23125:2015, is valid from 29 July 2025 to 28 July 2030 and lists both EV-1475B and EV-1580B in its scope. The EAC certificate ЕАЭС N RU Д-CN.PA06.B.89520/25, issued under TR CU 010/2011 and TR CU 020/2011, is valid from 8 August 2025 to 7 August 2030 with a comparable model scope.
Why do published CNC market size estimates differ so much?
Estimates diverge mainly because of scope. Grand View Research estimated the CNC machining and turning centers market at USD 27.64 billion in 2024, while Mordor Intelligence put the machining centers market at USD 22.41 billion in 2025 — most likely because one figure includes turning centers and the other covers machining centers only. Applying the same discipline to machine-level specifications is what makes a buyer's matrix reliable.
The purpose of a buyer-owned matrix is not to replace judgement with a spreadsheet. It is to make sure that judgement is applied to facts that can be checked, and that every unverifiable claim is left visibly outside the table. The full parameter tables for the EUMASEIKI machining center range, including the models referenced above, are collected in the EUMASEIKI product brochure.
¿Tiene preguntas o necesita más detalles?
Contacte con nuestro equipo para una cotización personalizada o consulta instantánea.
Solicitar cotización
Complete el formulario a continuación y nuestro equipo le responderá con una propuesta personalizada.
Chat directo de WhatsApp
¿Prefiere chatear en tiempo real? Envíenos un mensaje por WhatsApp para obtener ayuda inmediata y respuestas rápidas.
- Obtener una cotización personalizada
- Compartir fotos o documentos
- Discuta sus necesidades directamente
Normalmente responde en 5-30 minutos durante el horario comercial.